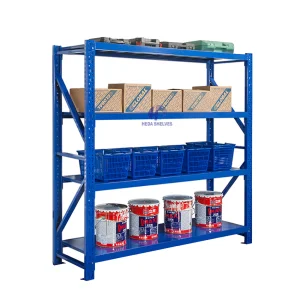
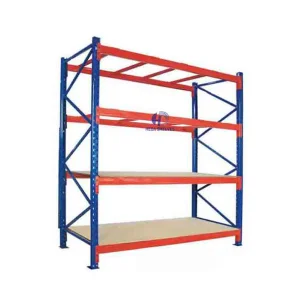
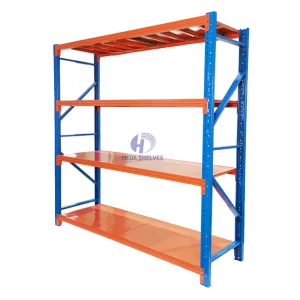
Explore our high-demand heavy-duty storage configurations designed for maximum spatial optimization and safety compliance.
Built on precision engineering, rigorous QA testing, and global export compliance.
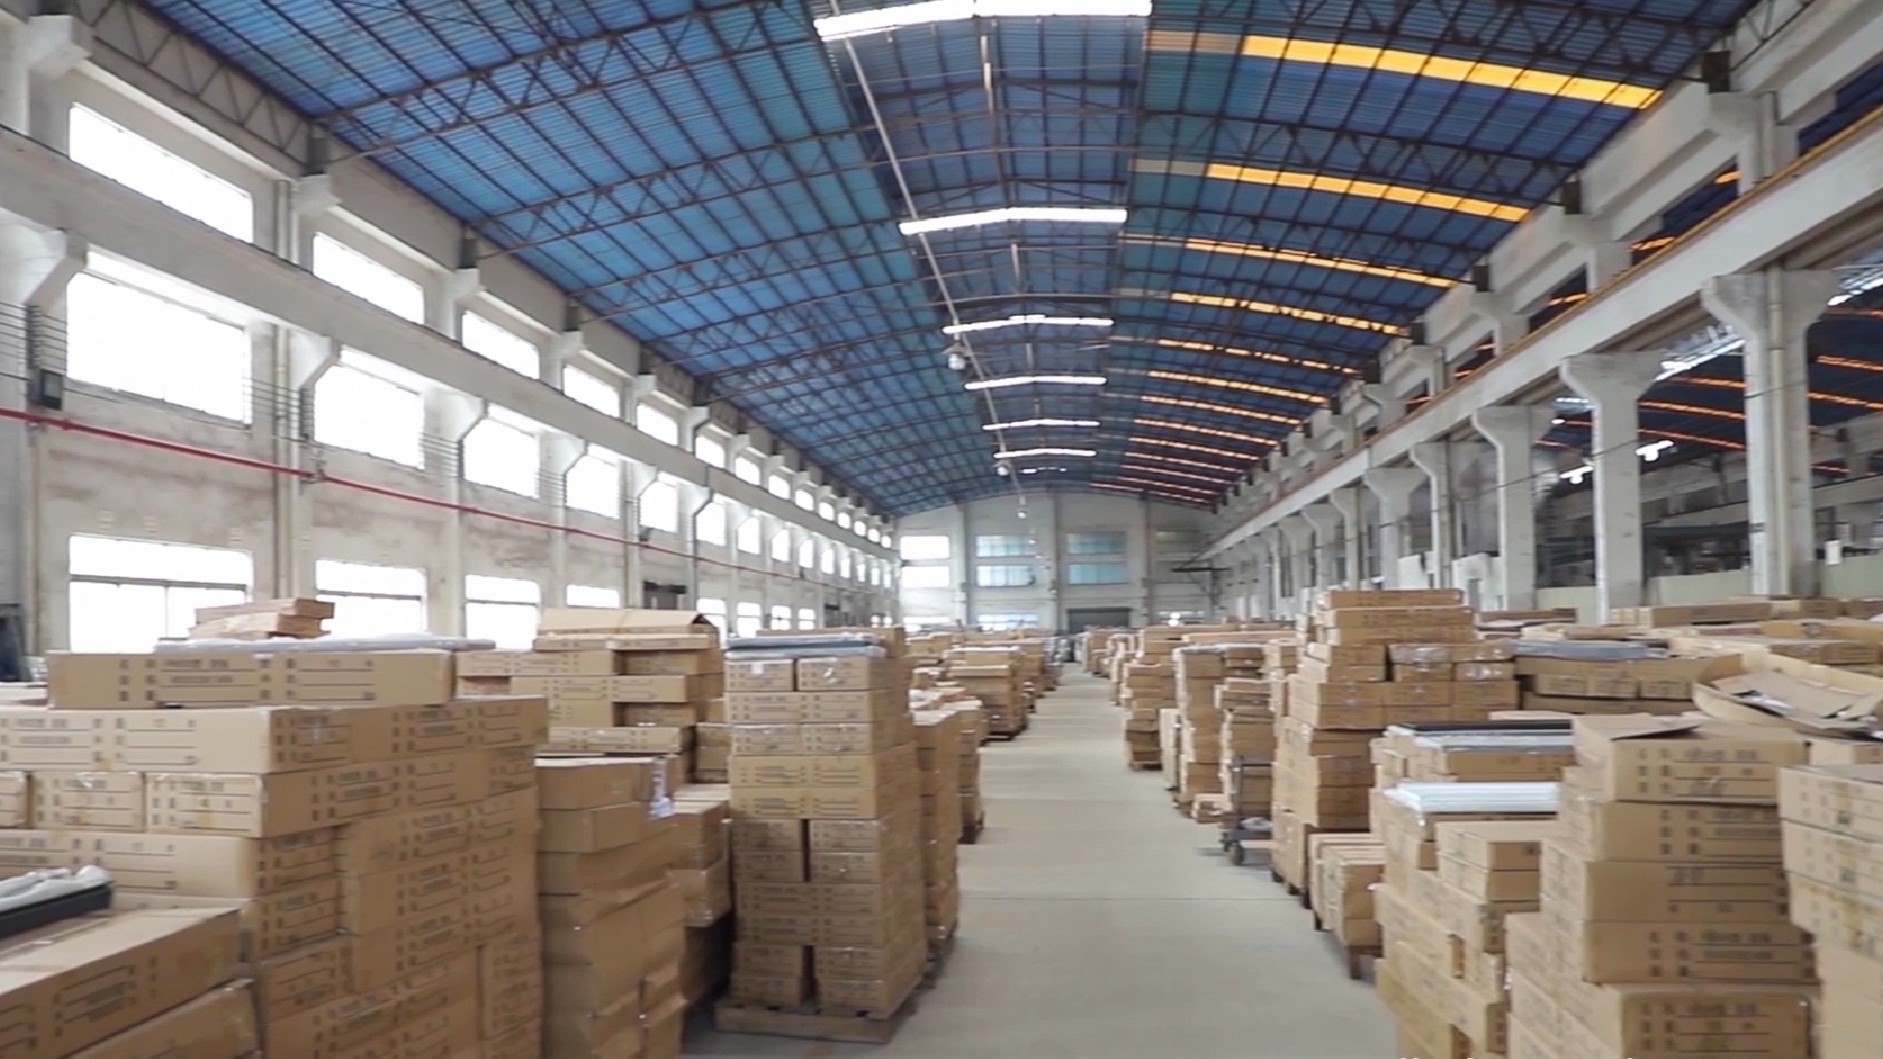
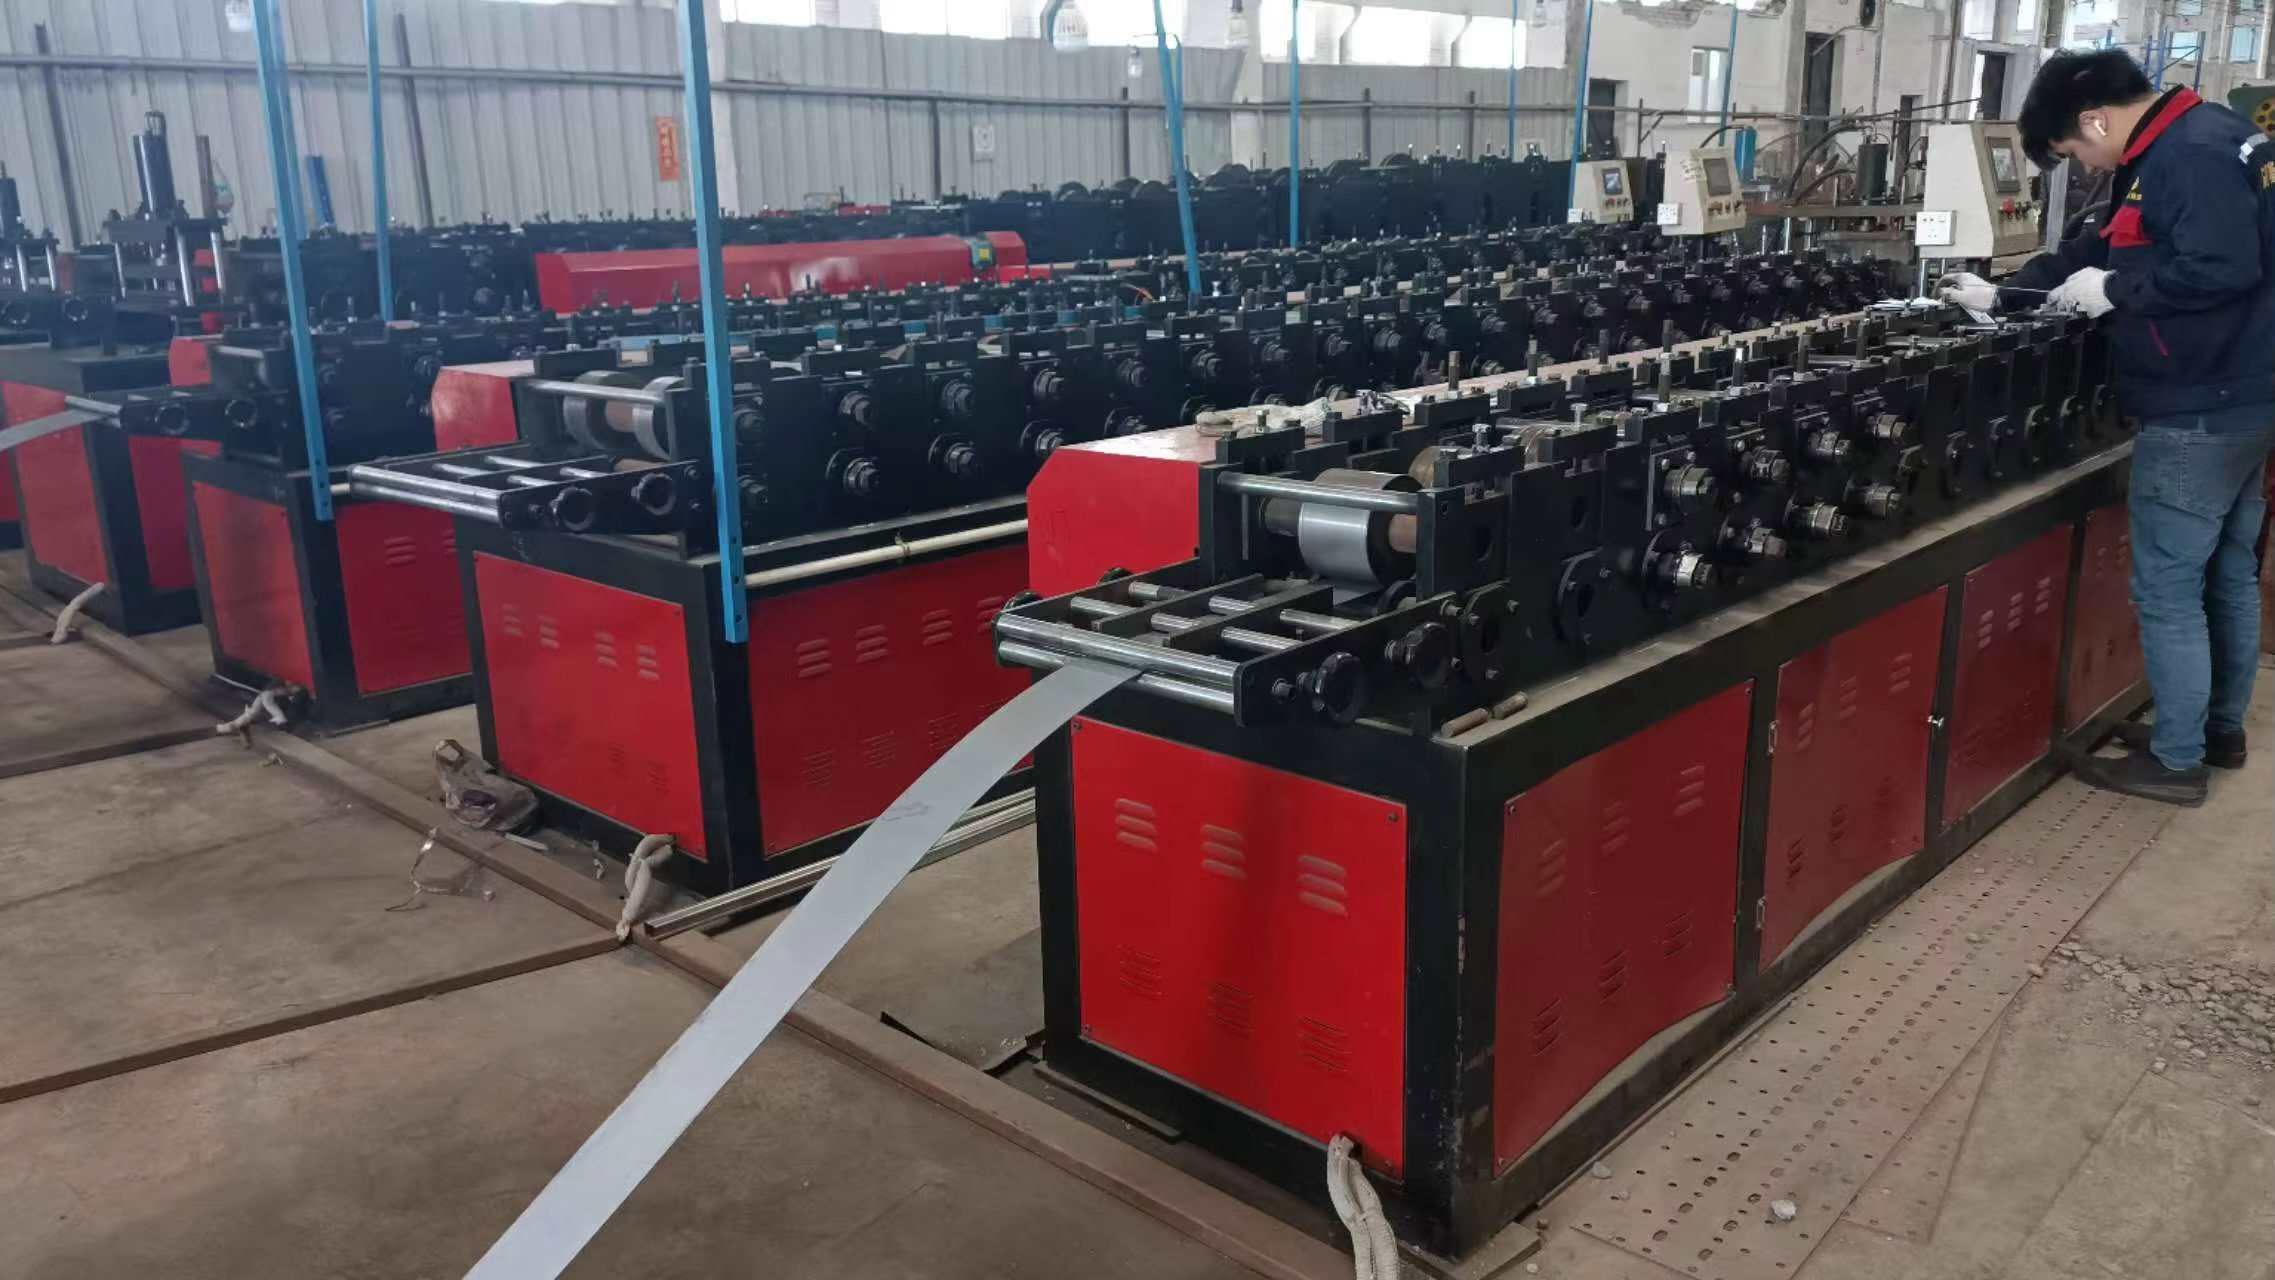
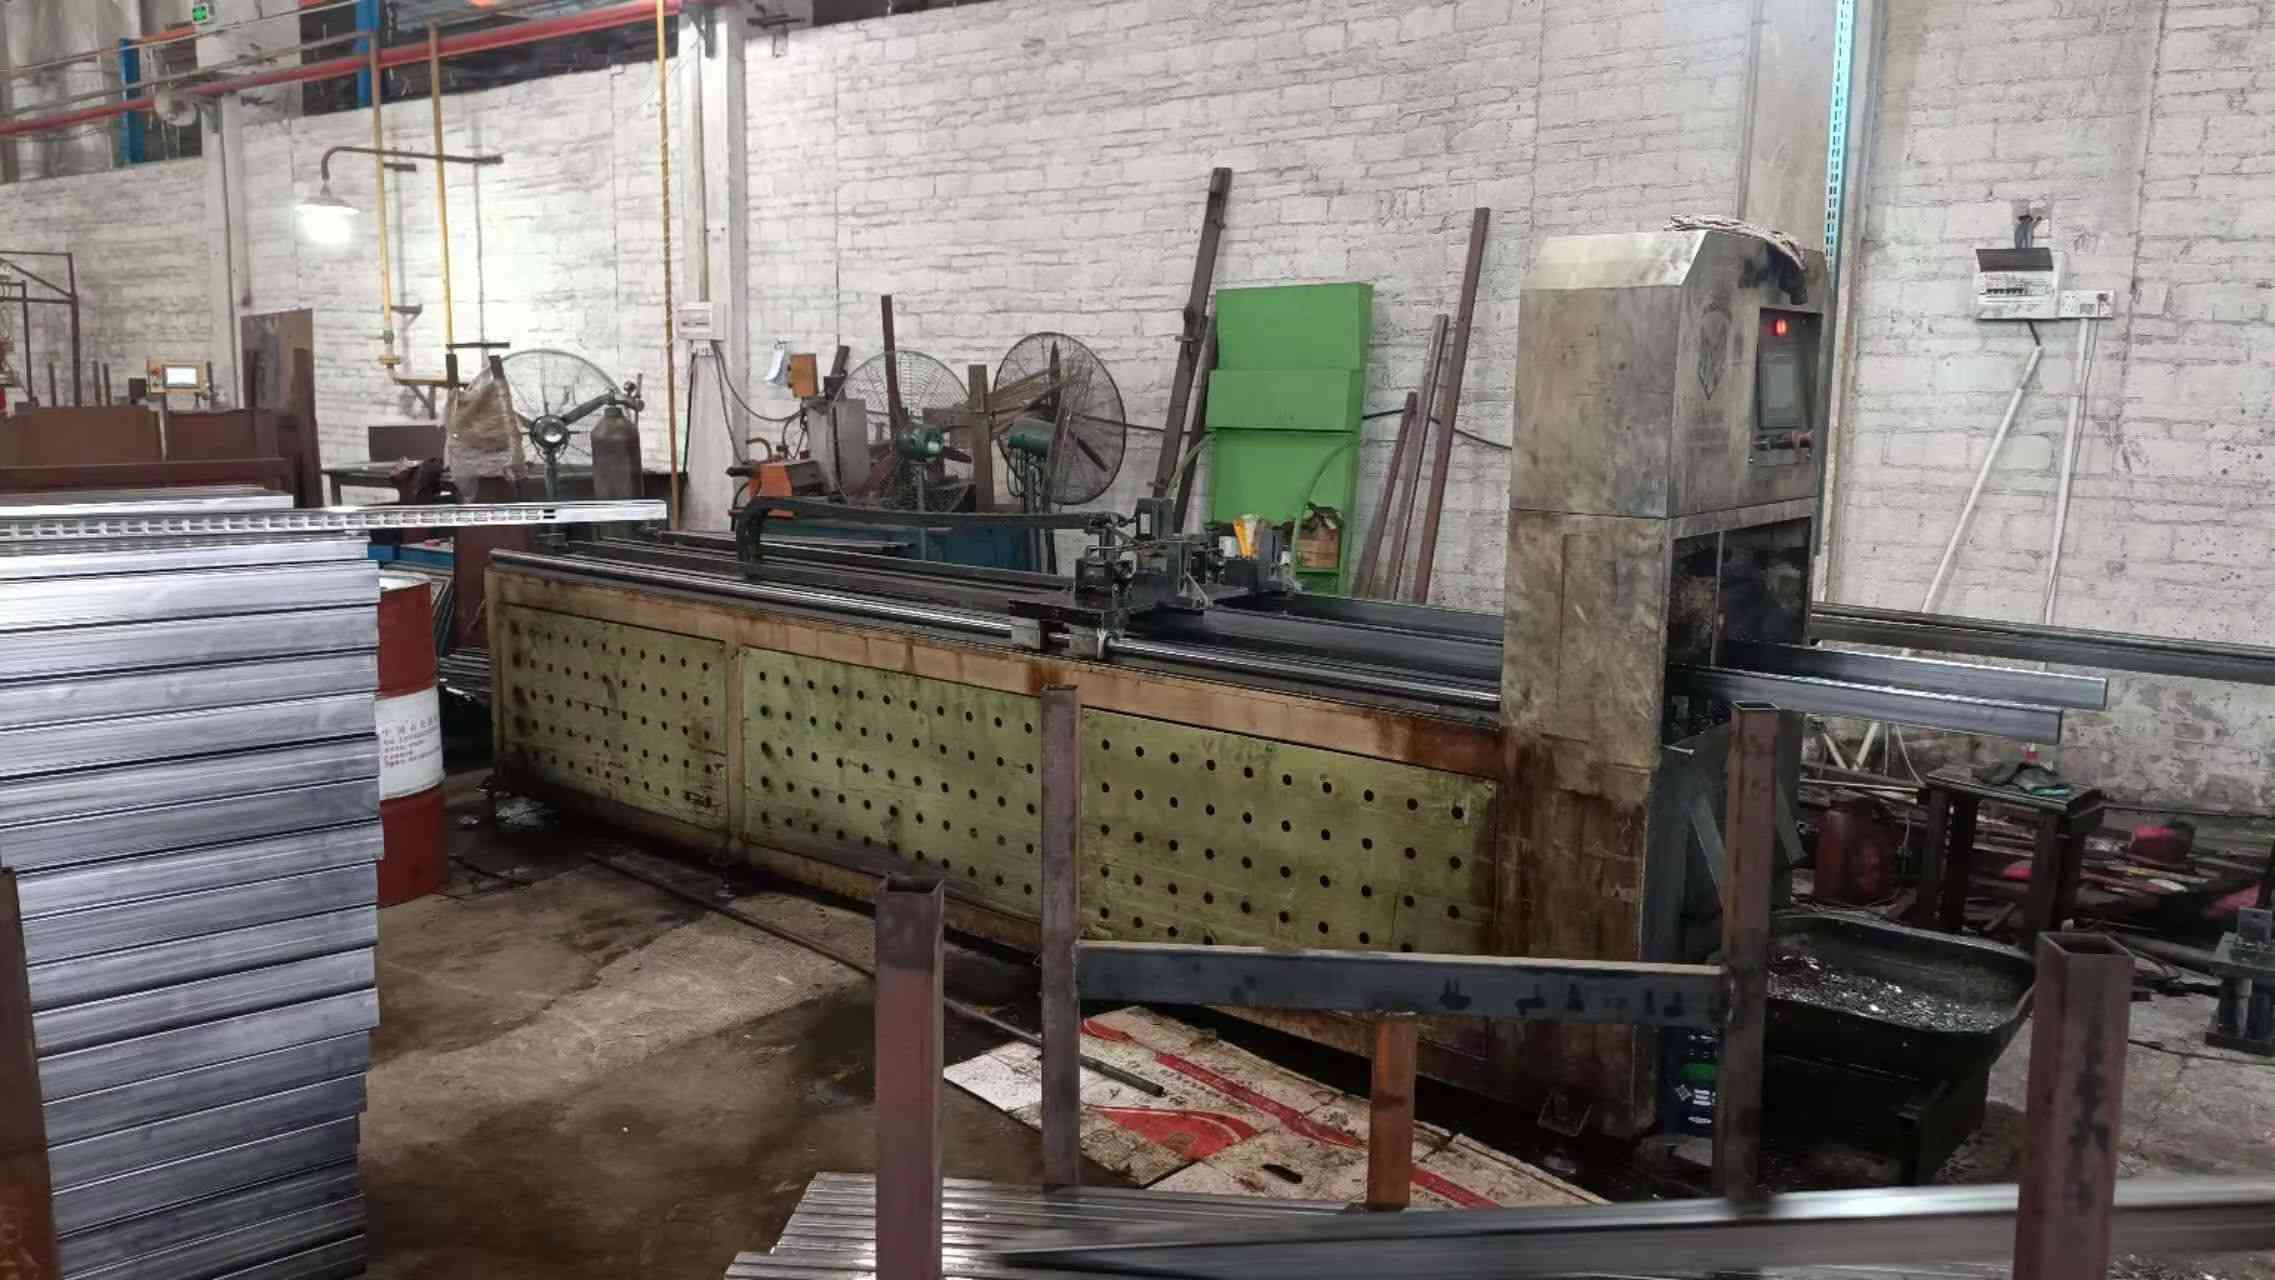
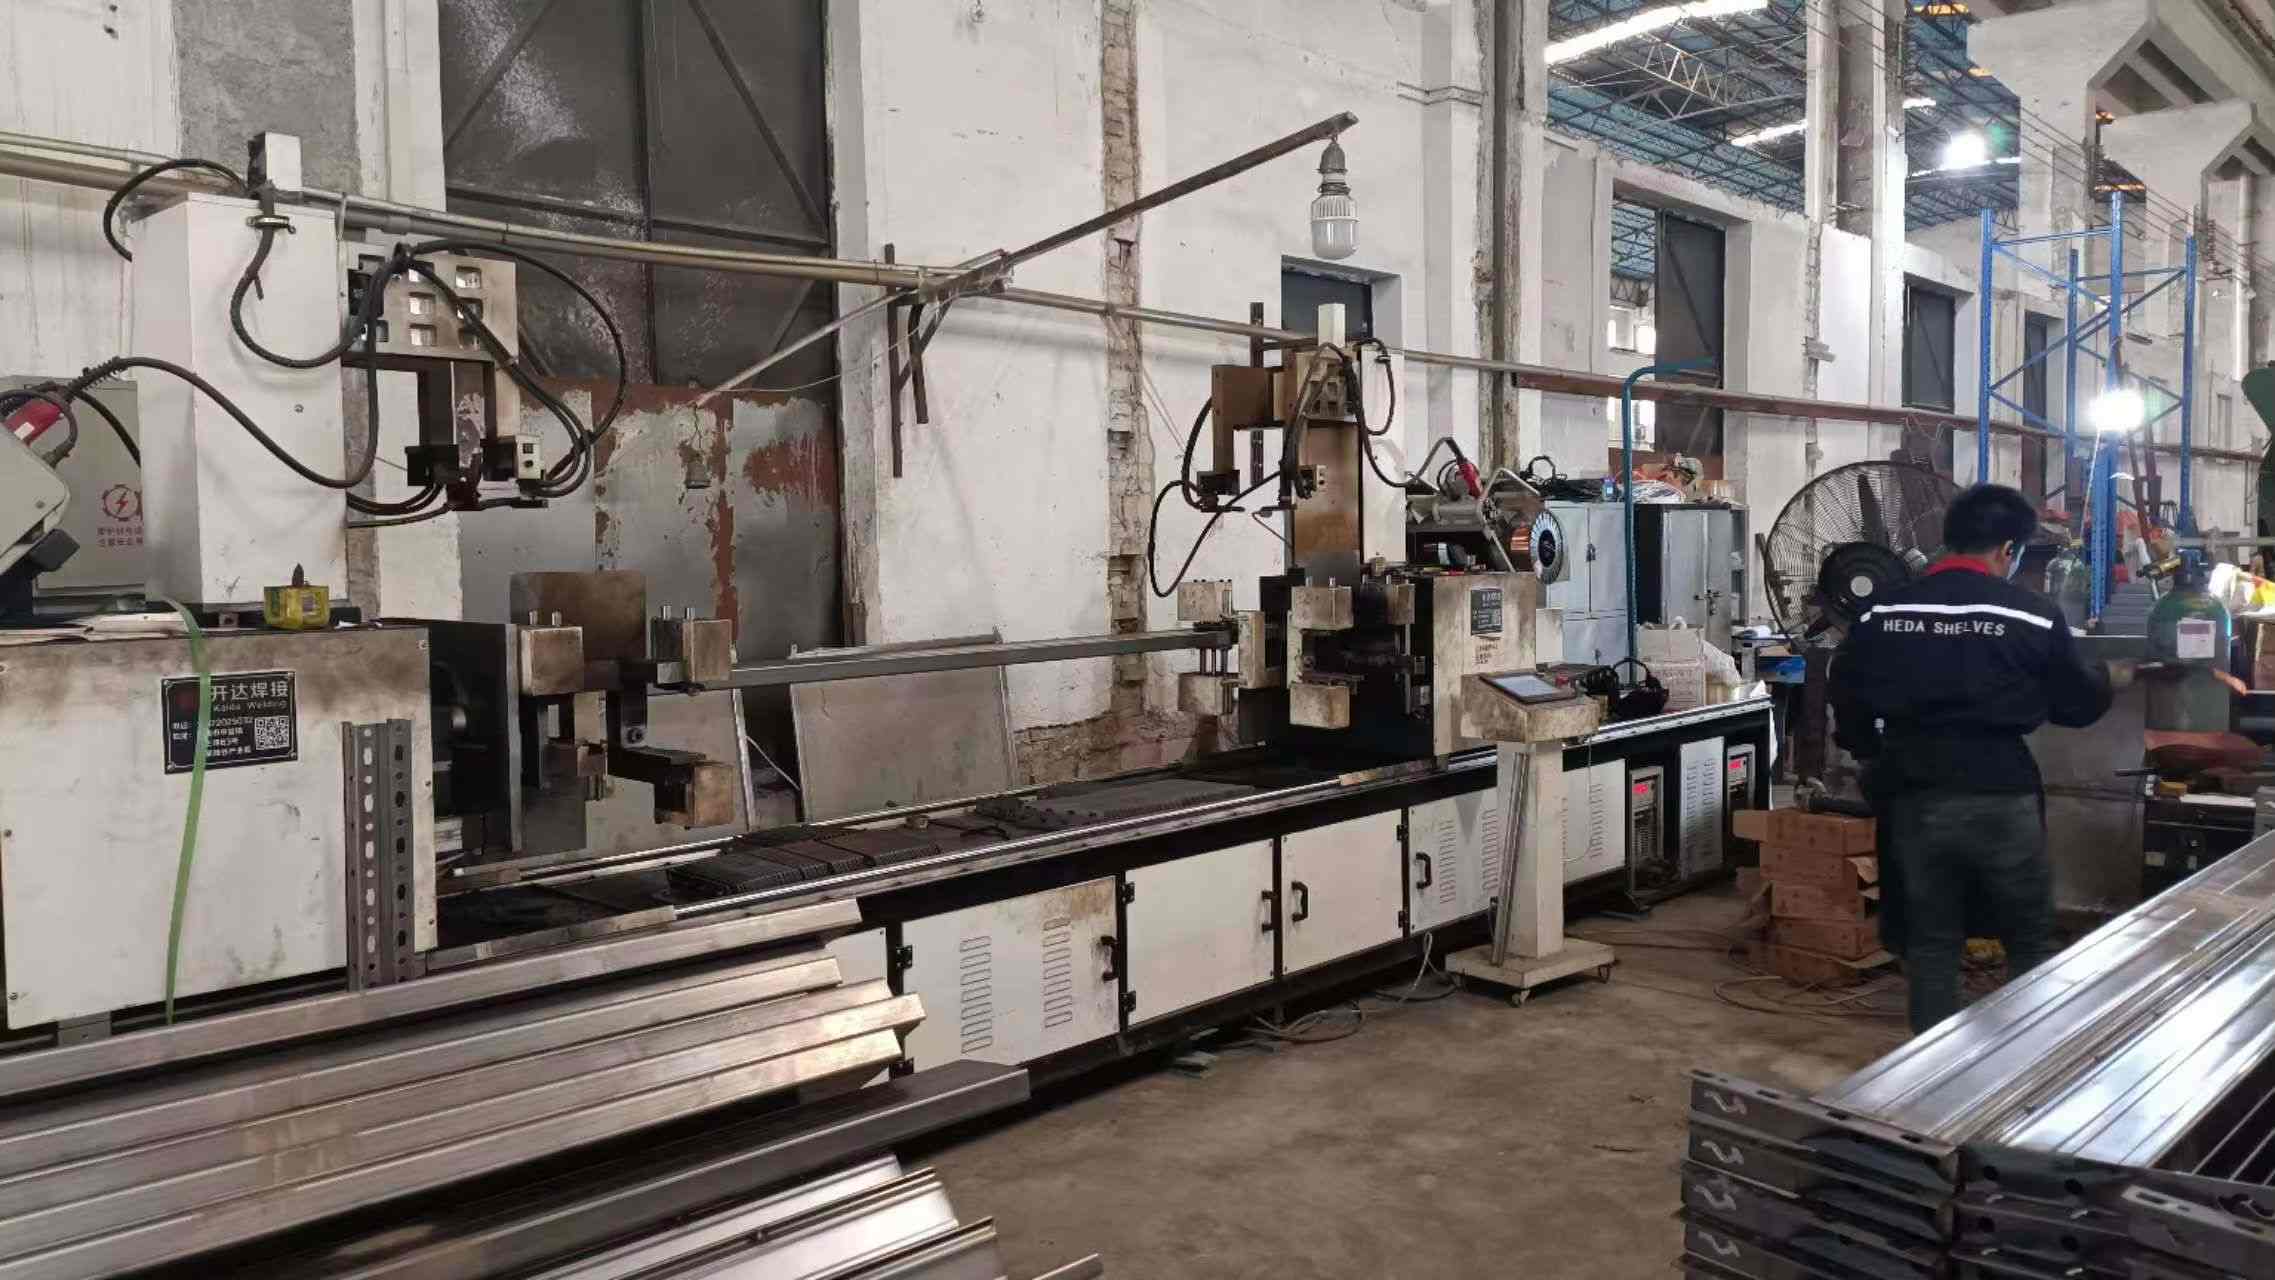
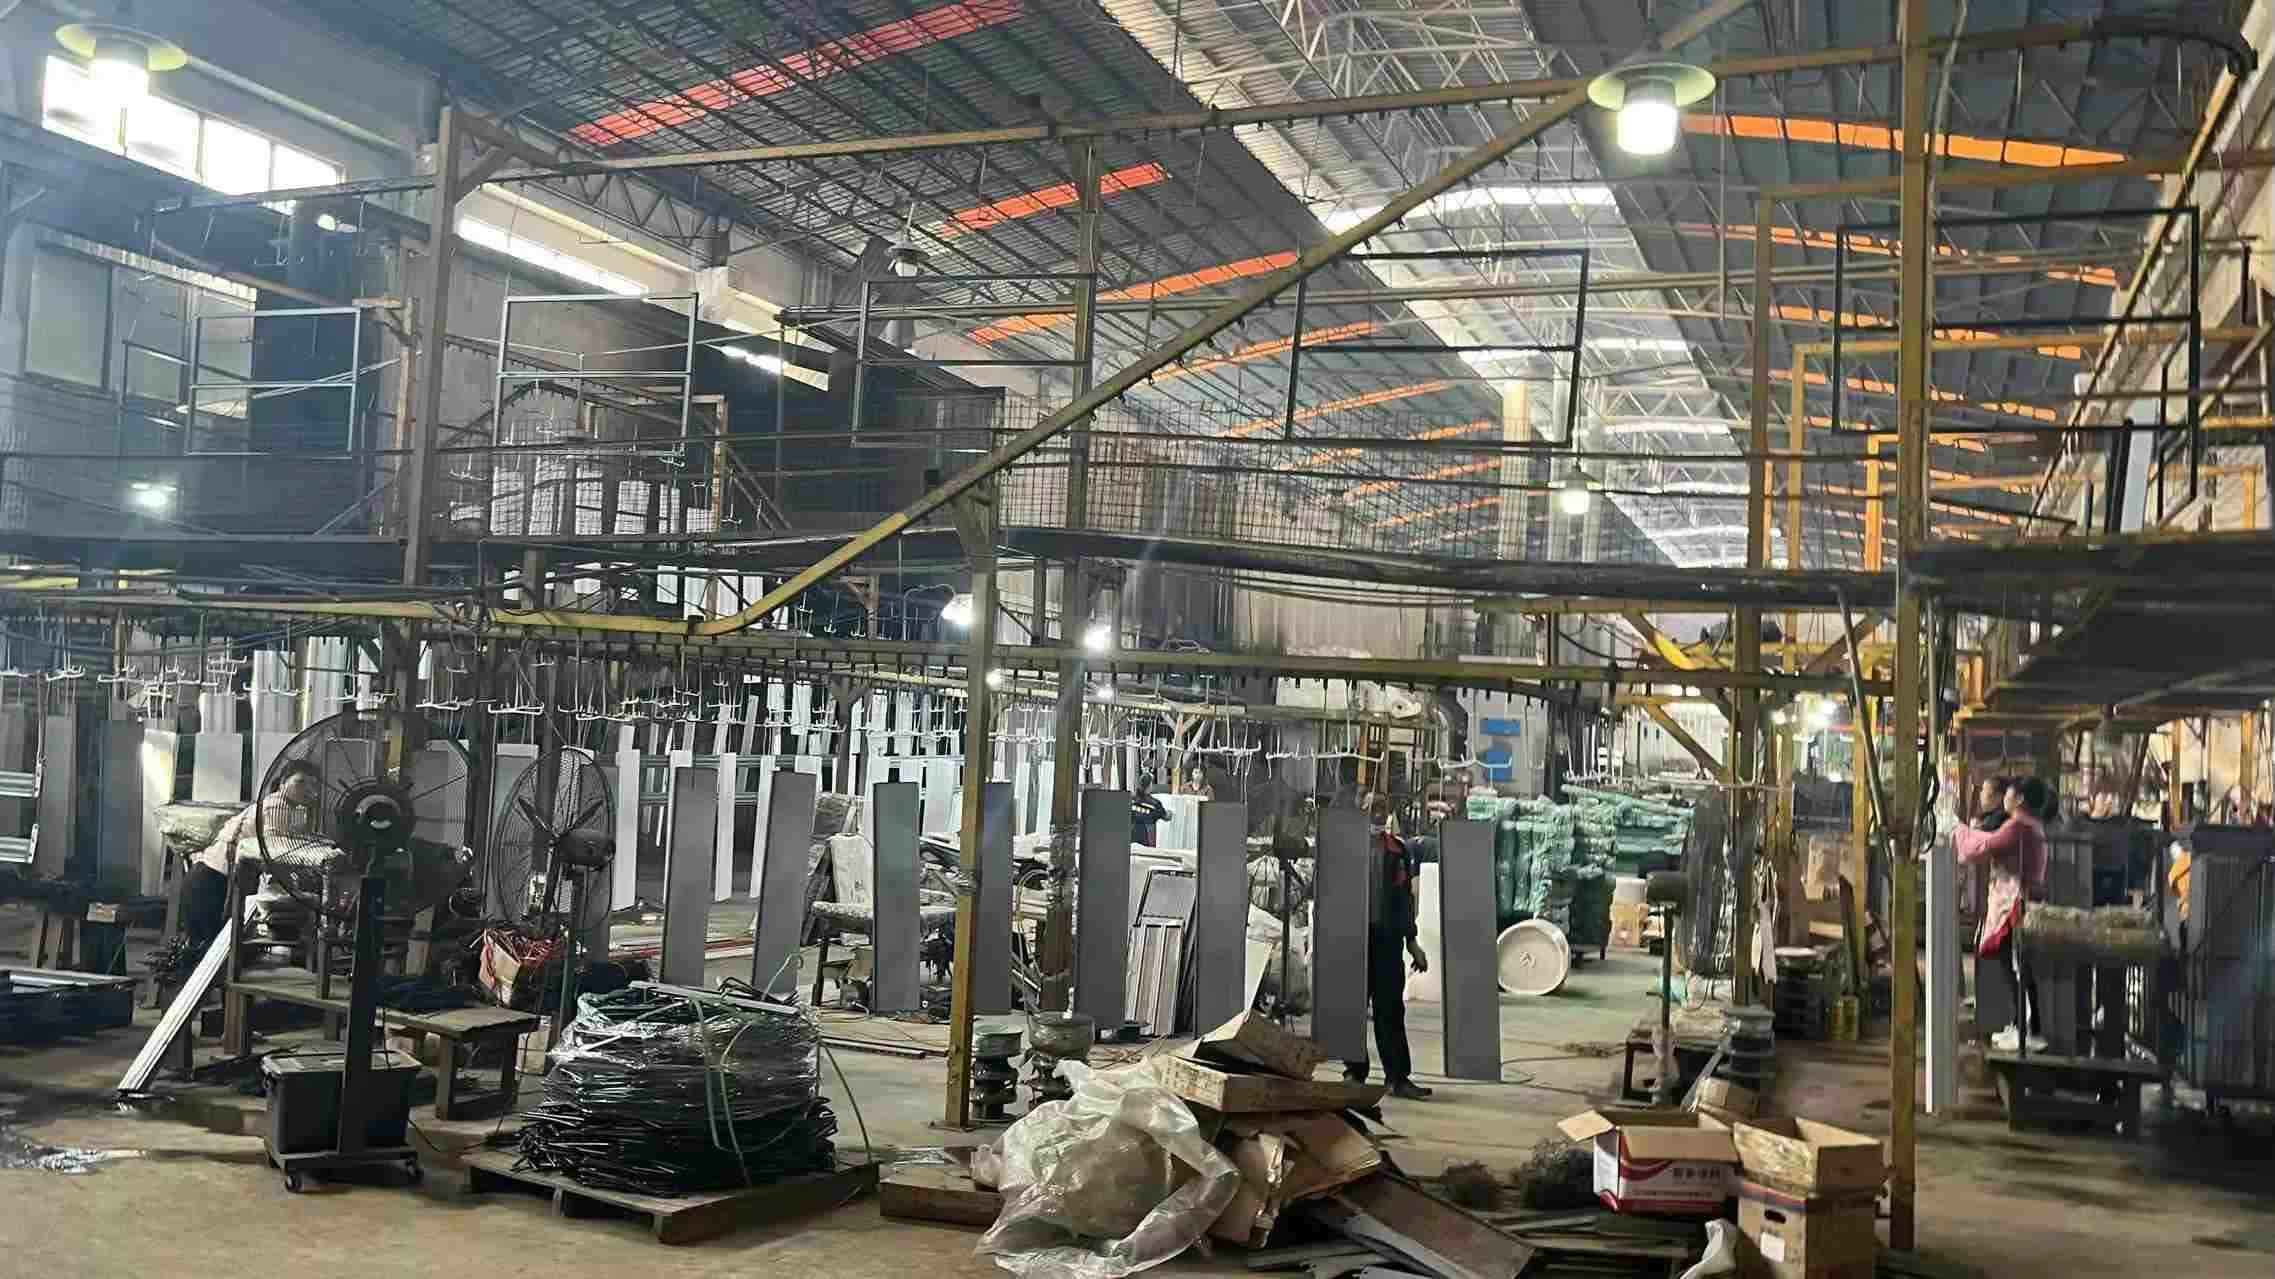
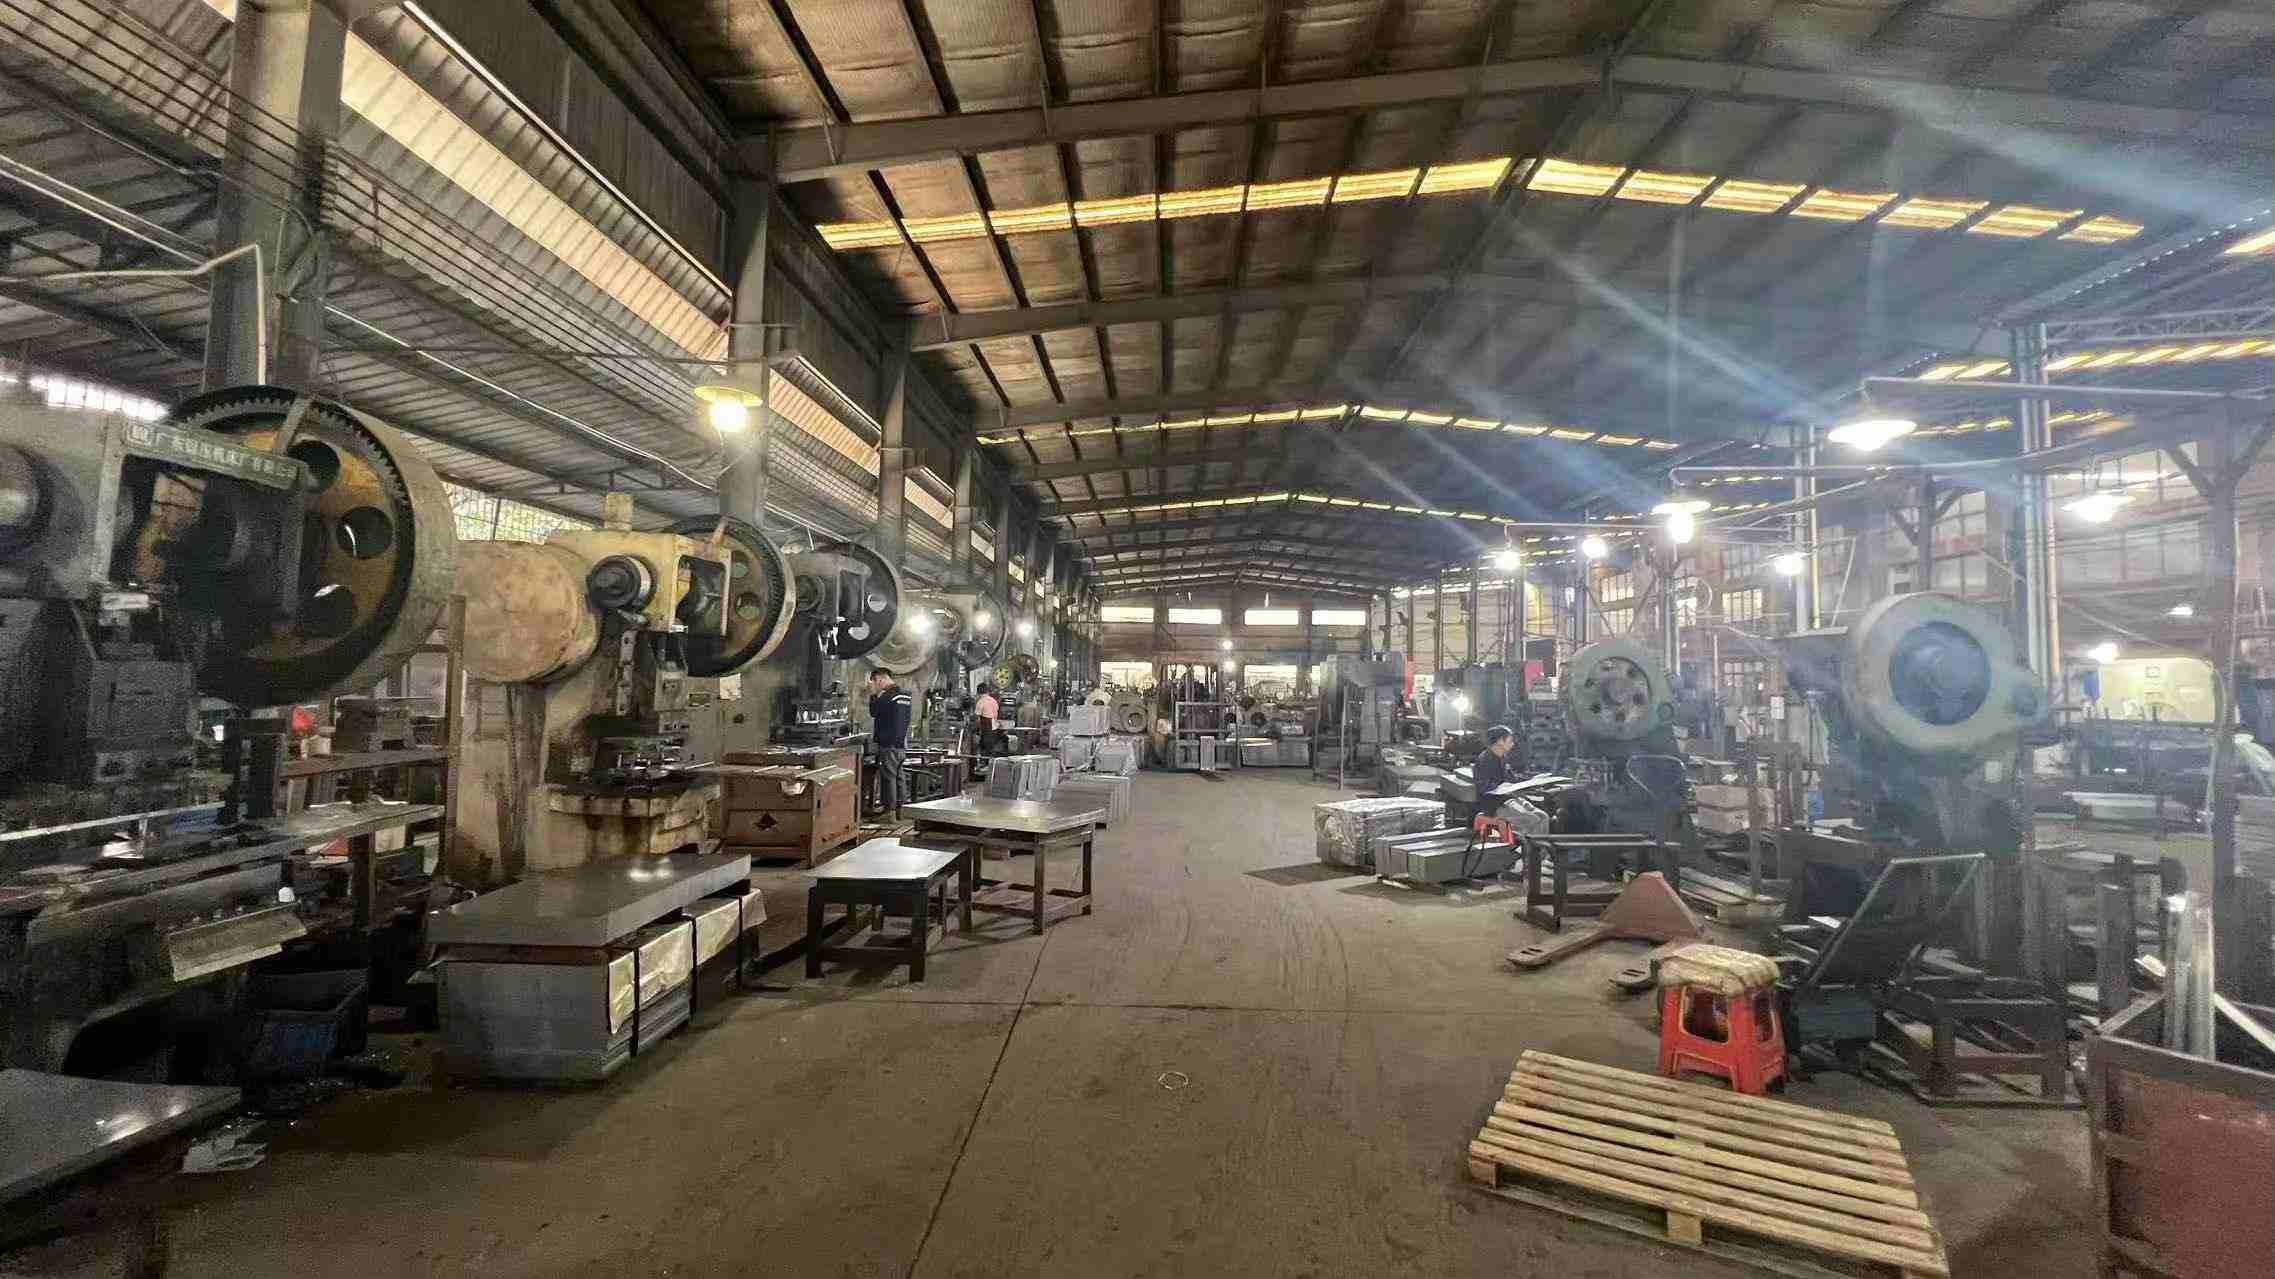
Established in 2014, Shenzhen Heda Warehouse Equipment Co., Ltd. is a premier manufacturer specializing in heavy-duty warehouse racking and industrial storage solutions. Spanning a modern manufacturing facility of 35,000 m², our enterprise integrates R&D, design, production, and international marketing to serve diverse storage needs worldwide. With 12 years of industry experience and 8 years of dedicated export expertise, we deliver high-caliber storage systems that generate over $28 million in annual export revenue.
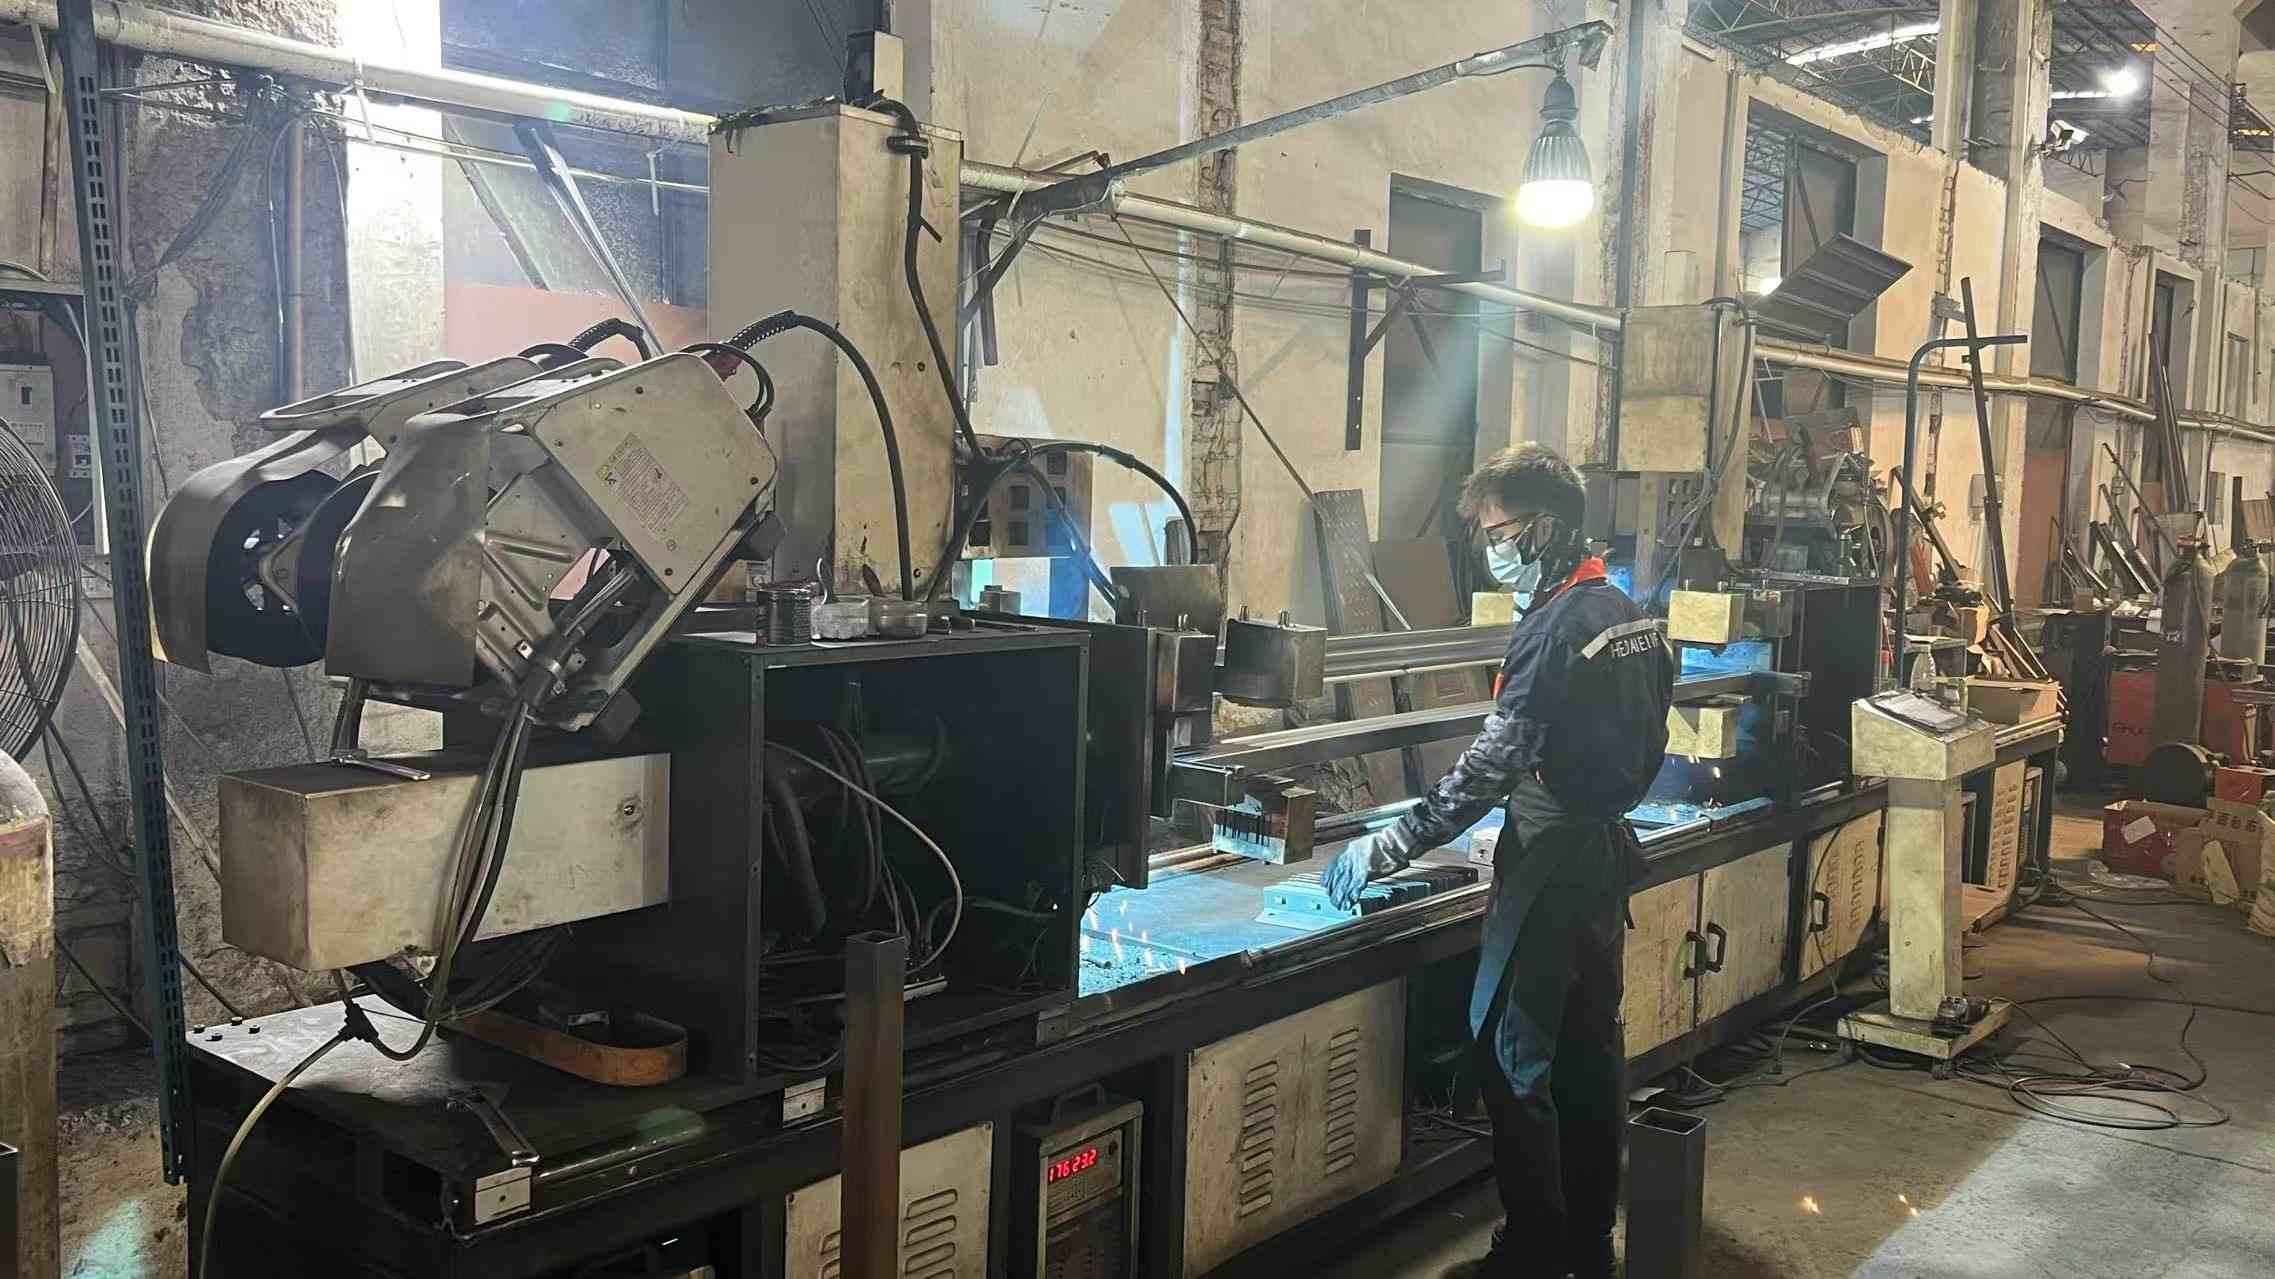
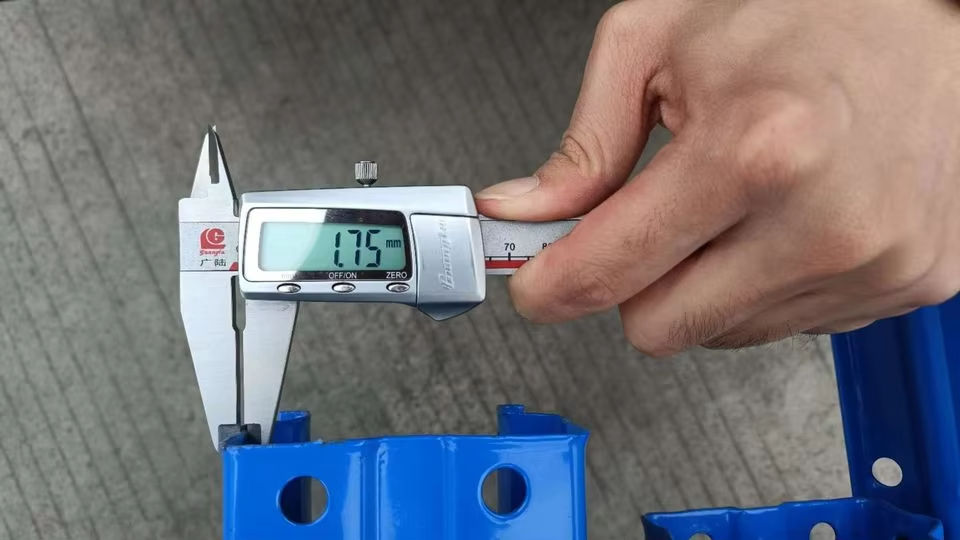
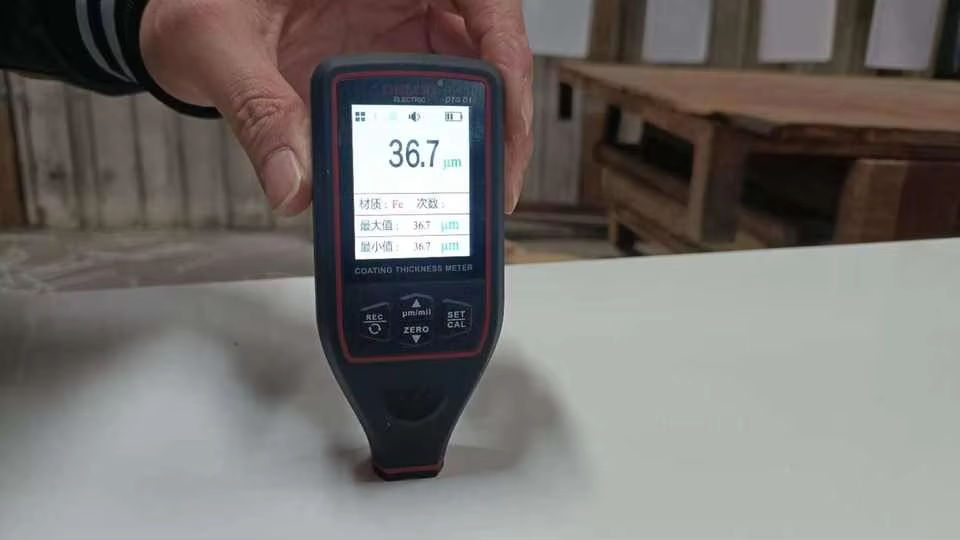
At Heda, quality control and engineering innovation drive our core operations. Our robust QC department comprises 45 skilled inspectors utilizing rigorous testing methods, including raw material tensile testing, automated weld flaw detection, layer load-bearing stress analysis, and salt spray surface corrosion testing. Supported by a professional R&D team of 28 senior structural engineers, we maintain strong full-customization capabilities (OEM/ODM)—offering tailored rack dimensions, load capacities, surface coatings, and layout designs. Driven by continuous innovation, we launched over 120 new dynamic storage products and component upgrades last year.
Operating with a strong direct-factory and international trade background, we have built a resilient ecosystem supported by over 800 supply chain partners. Our products are exported to major global markets, including North America, Western Europe, Southeast Asia, and the Middle East. We proudly serve a diverse clientele ranging from third-party logistics (3PL) providers and large distribution centers to industrial manufacturers and wholesale equipment distributors.
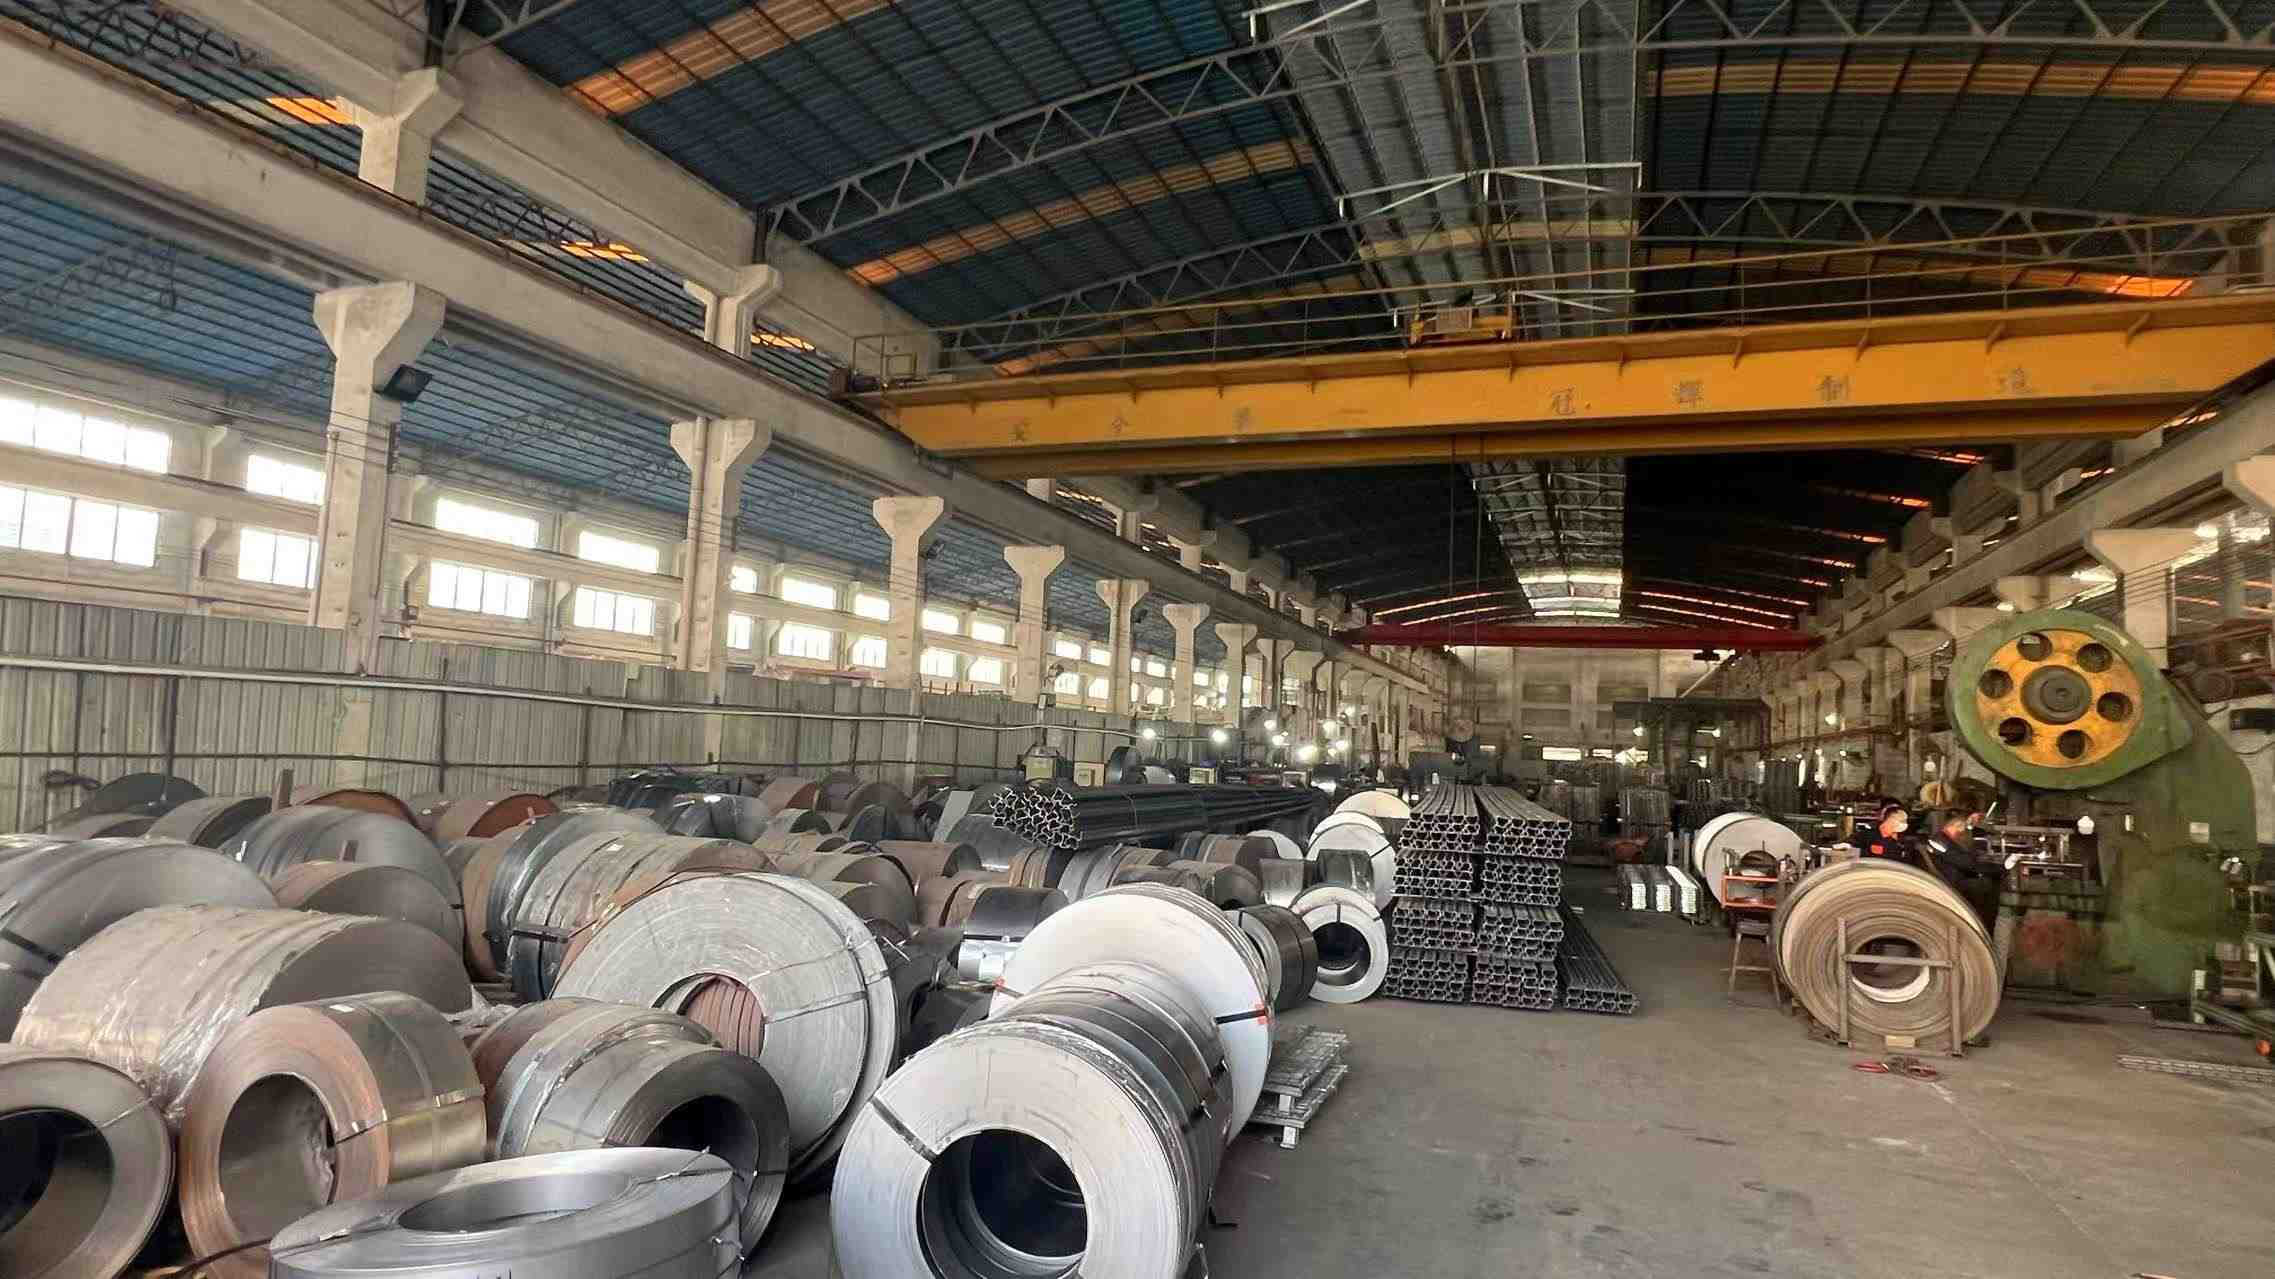
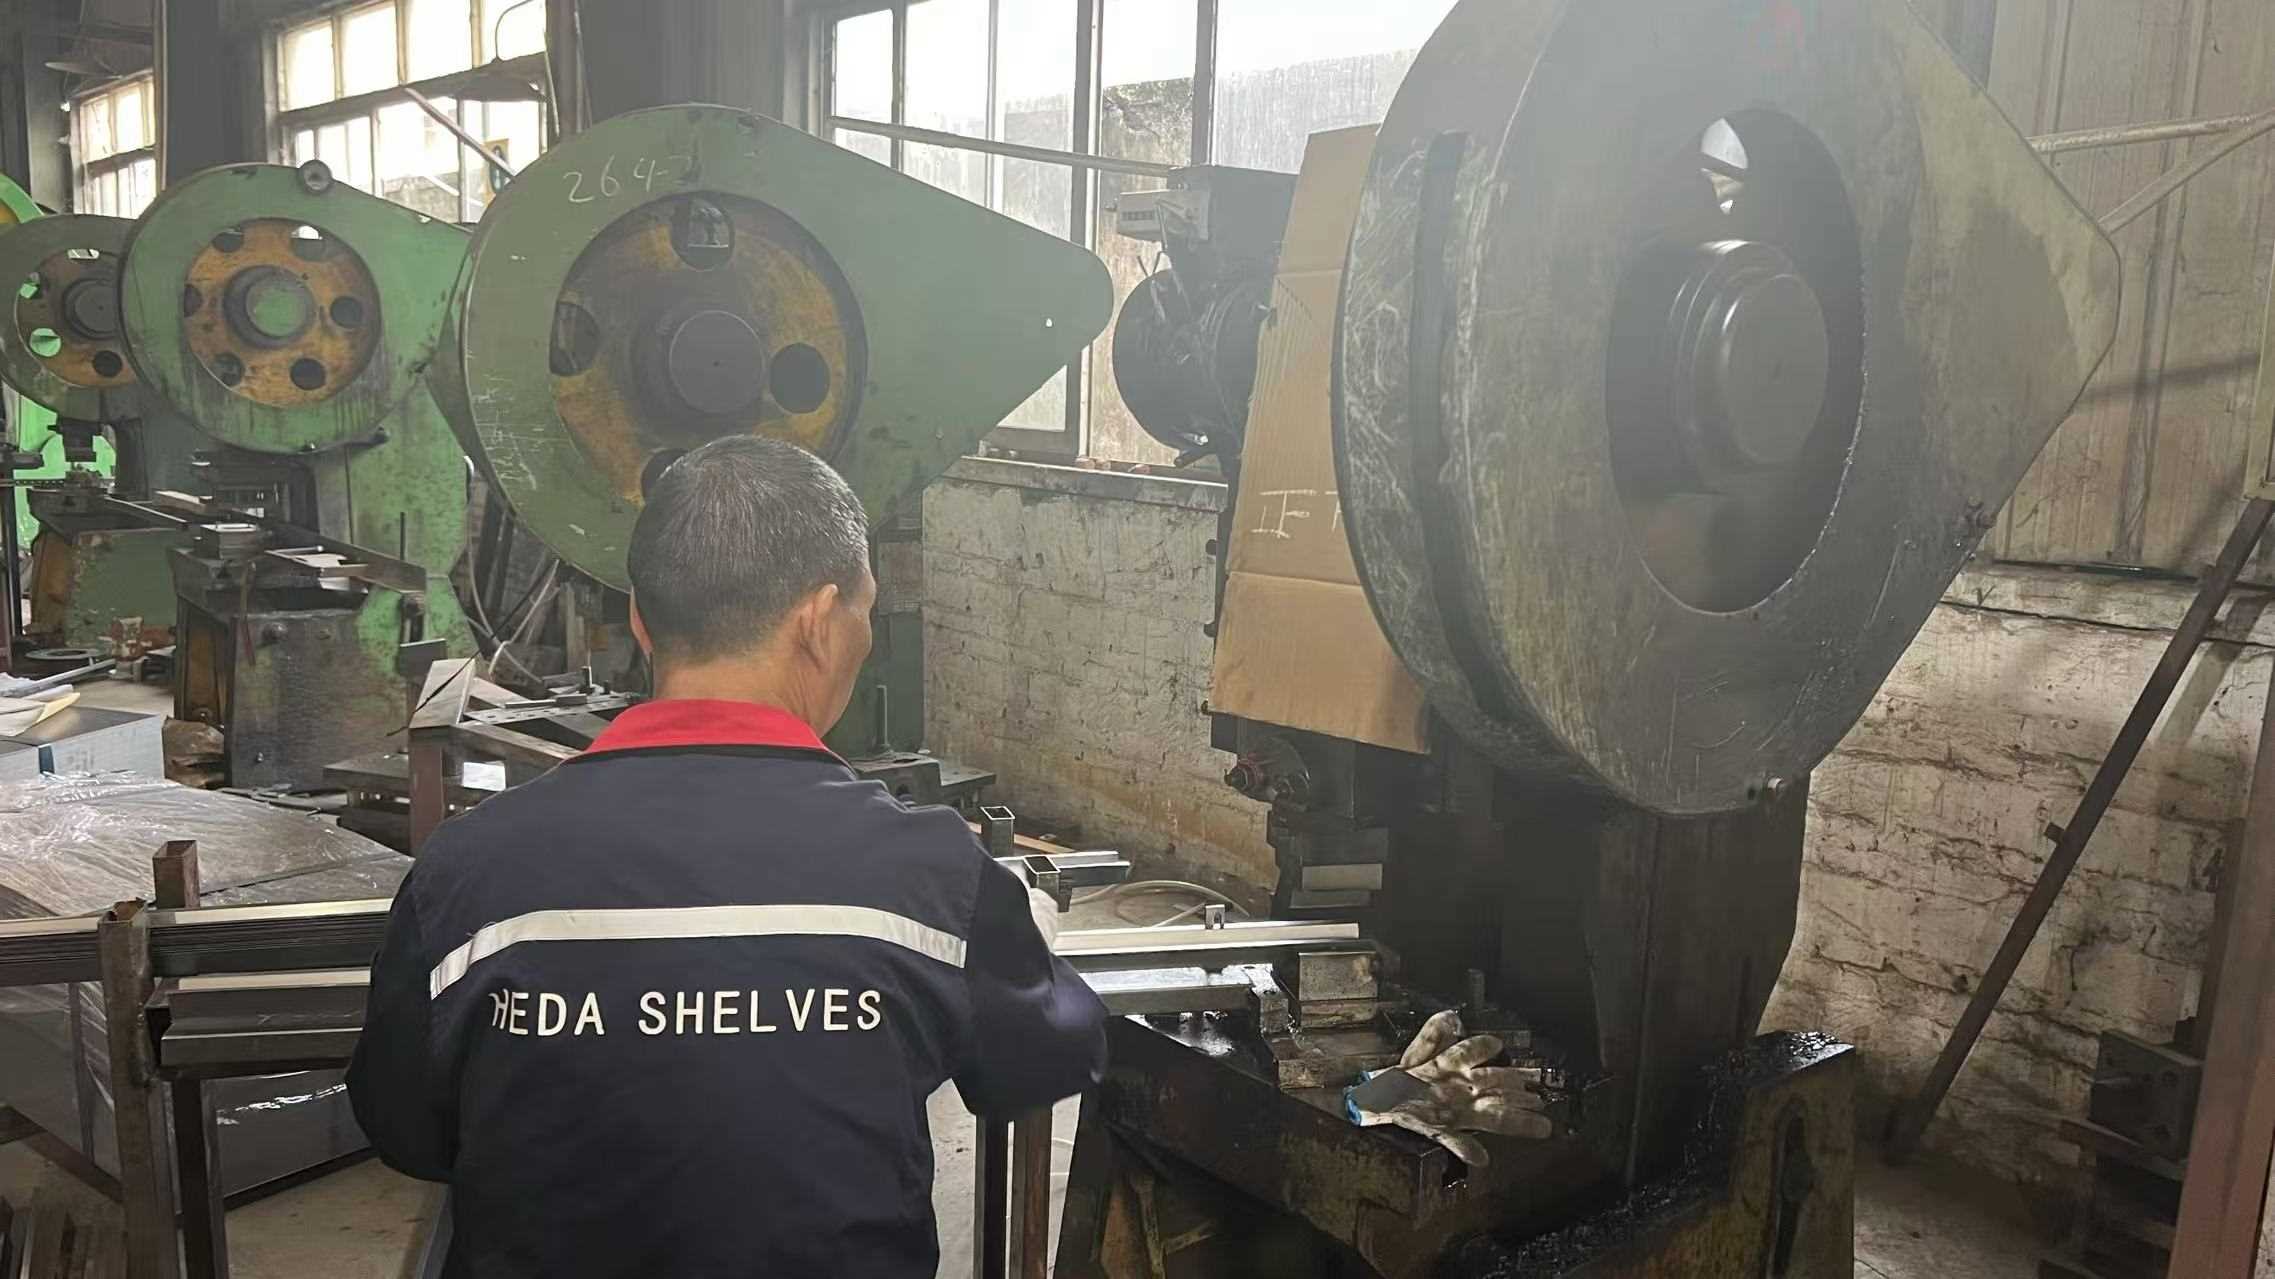
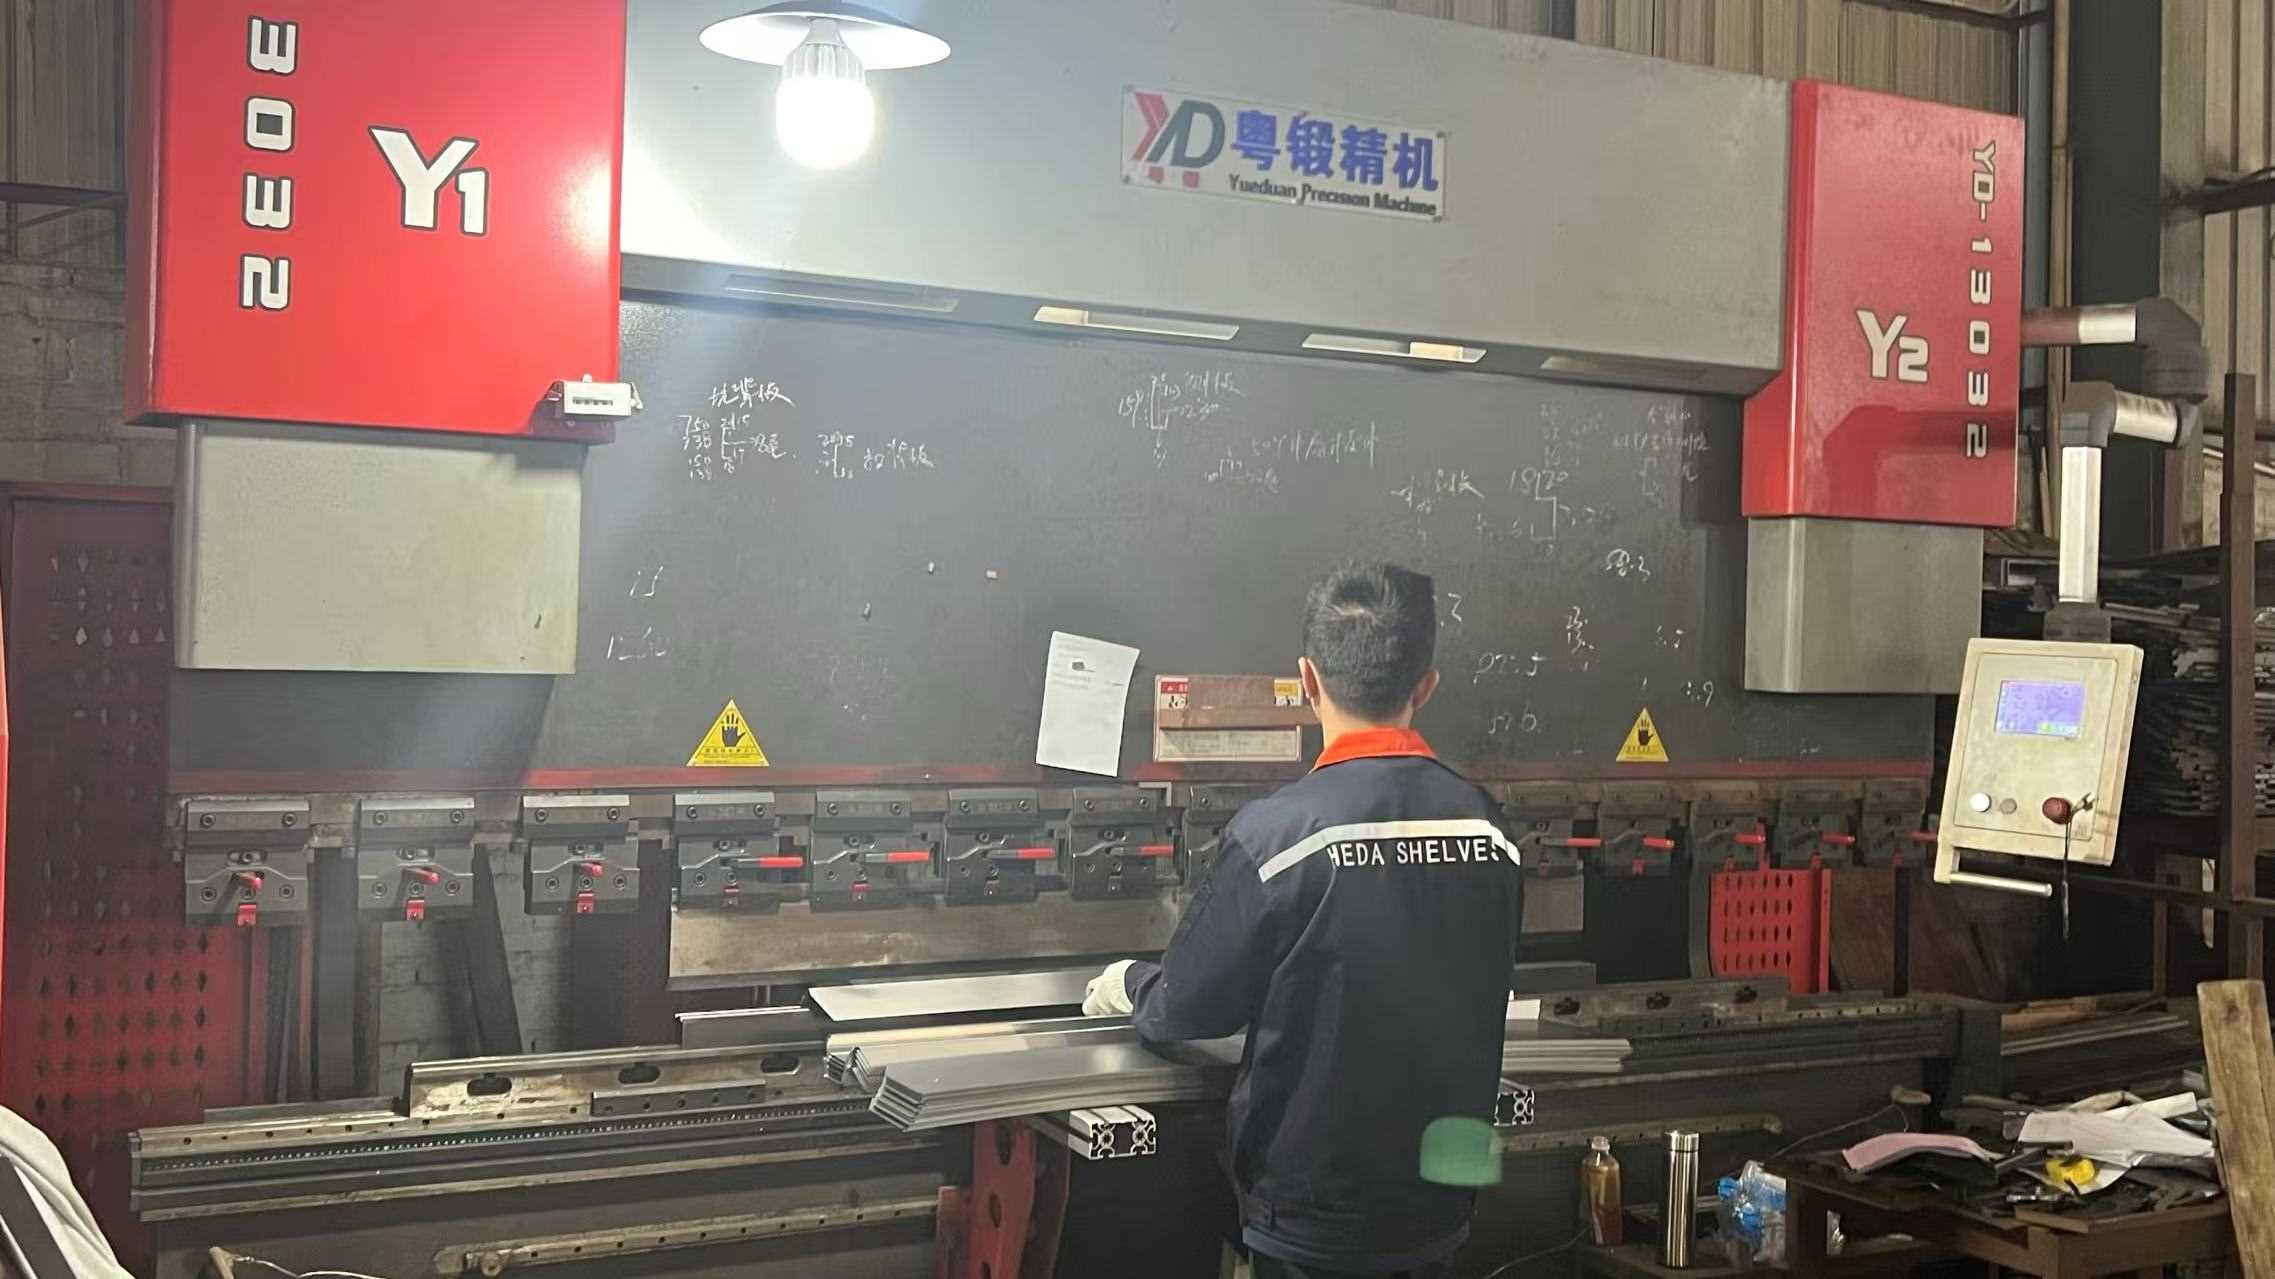
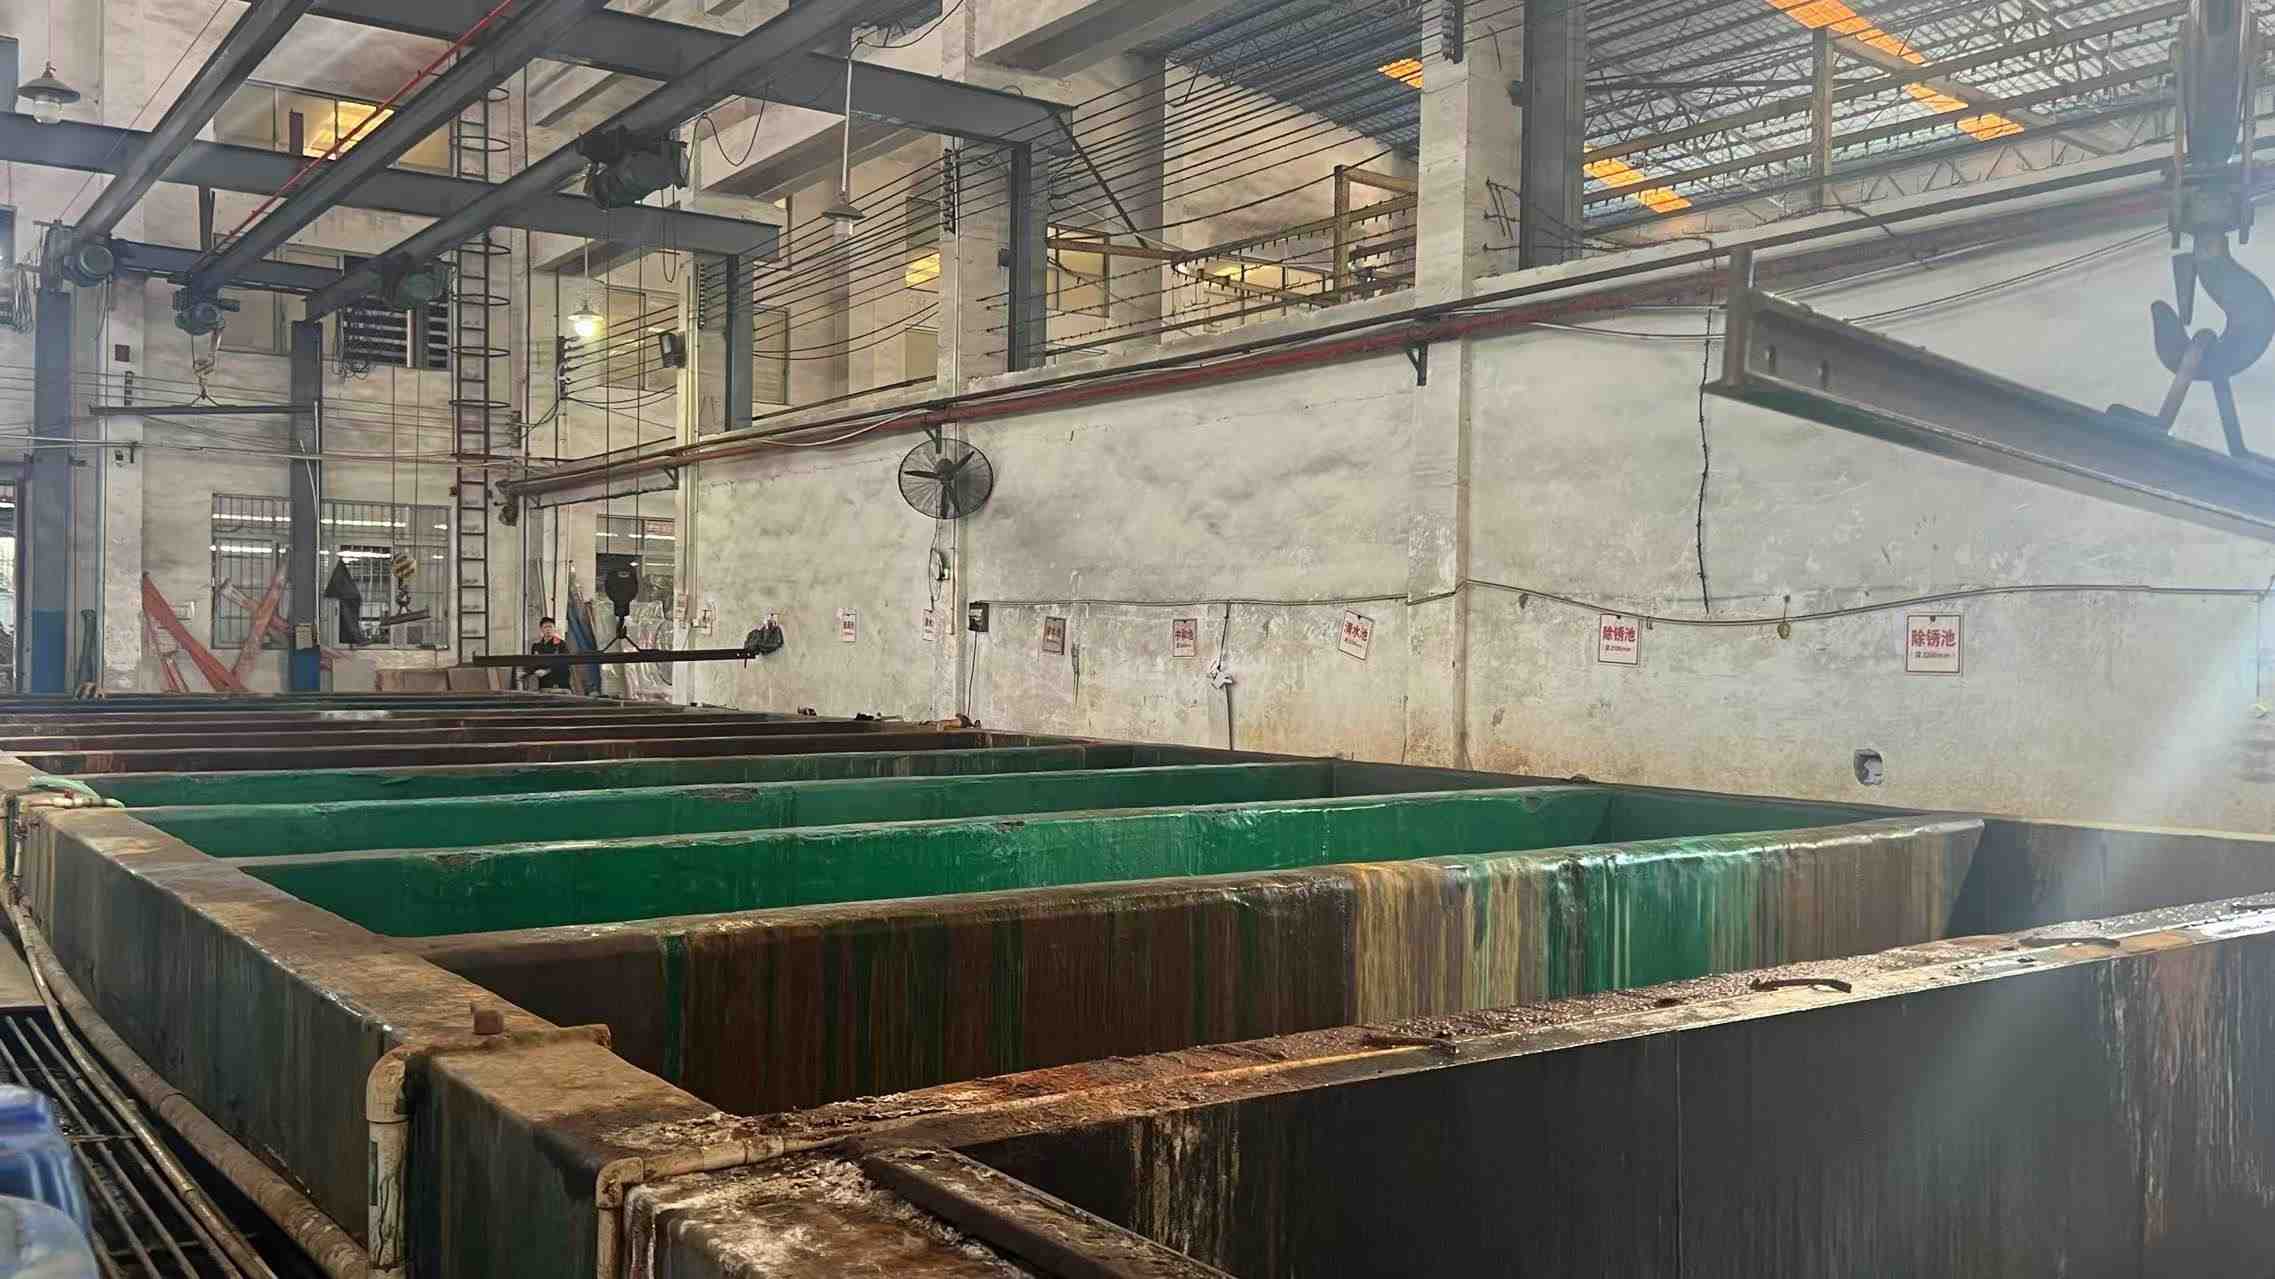
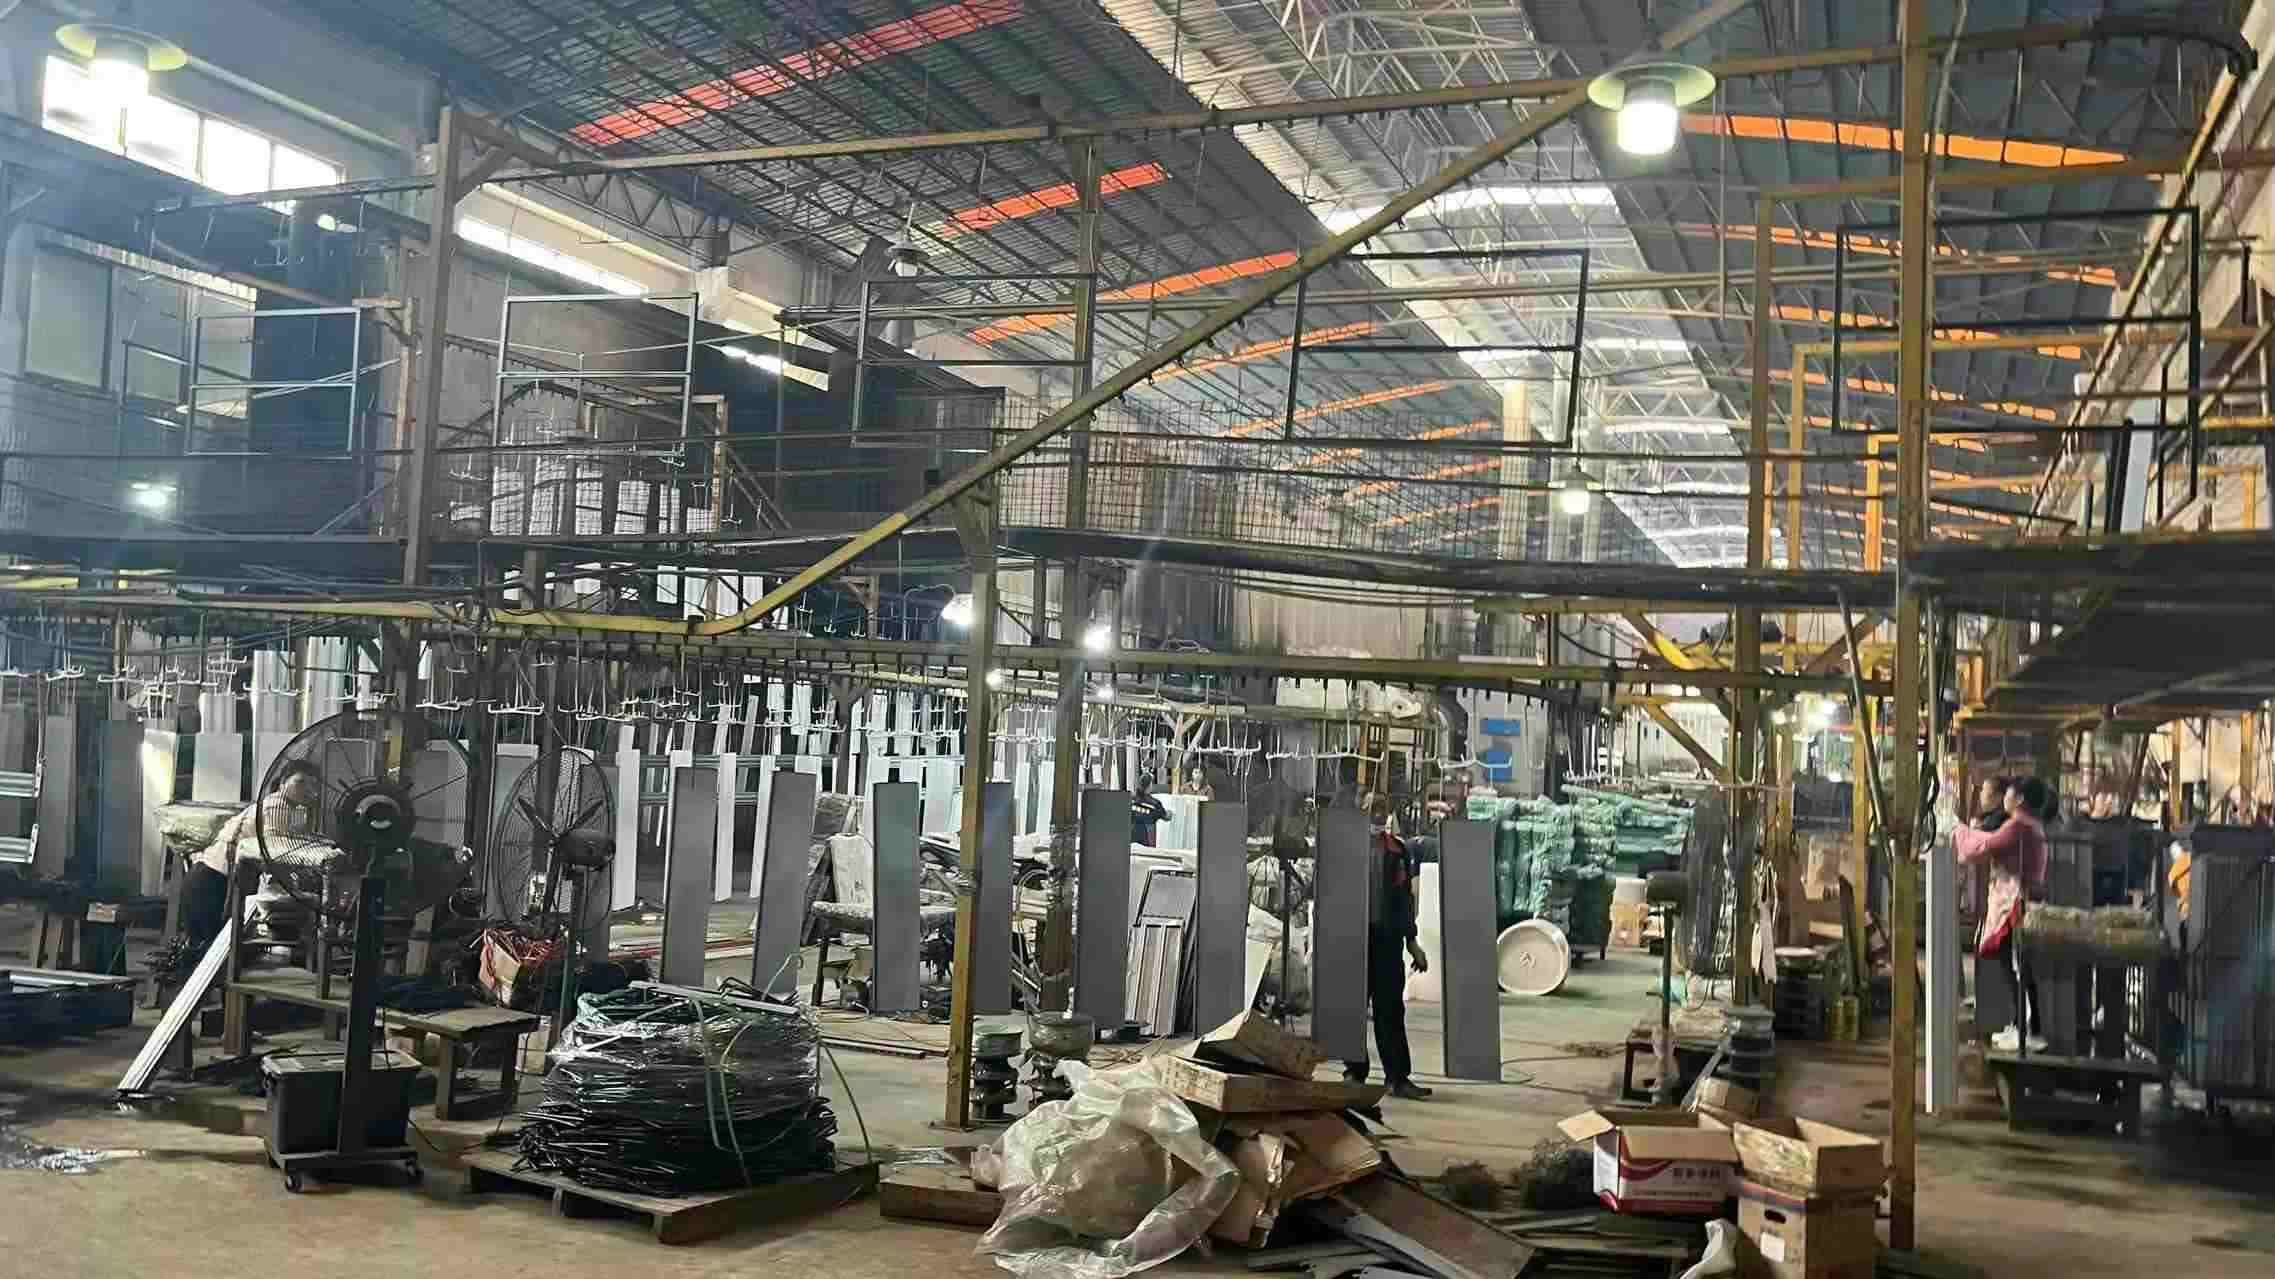
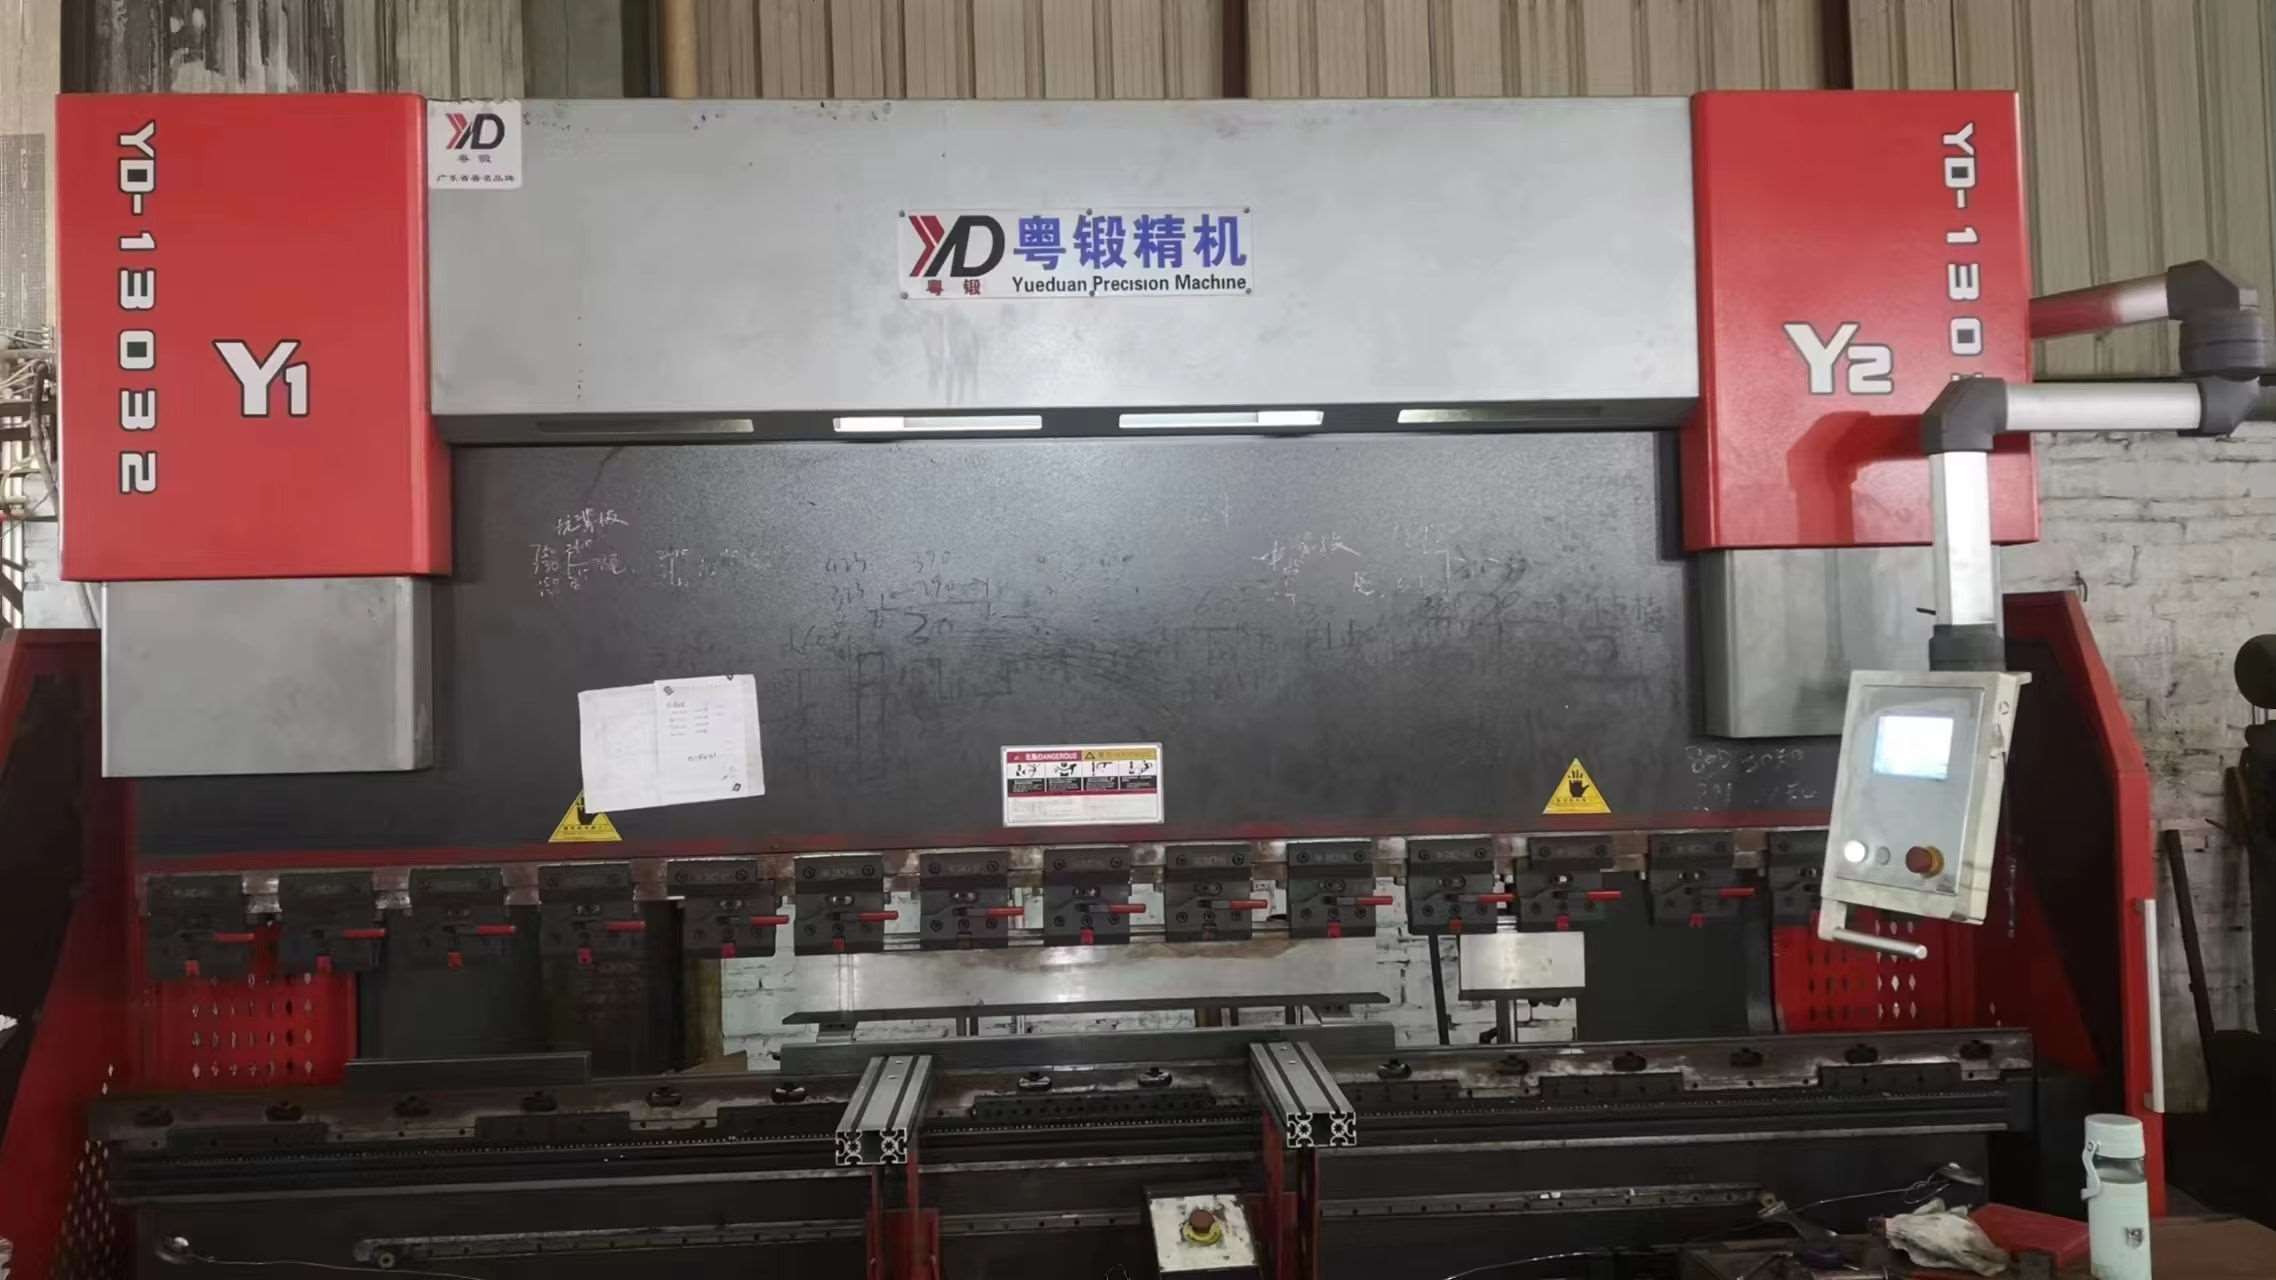
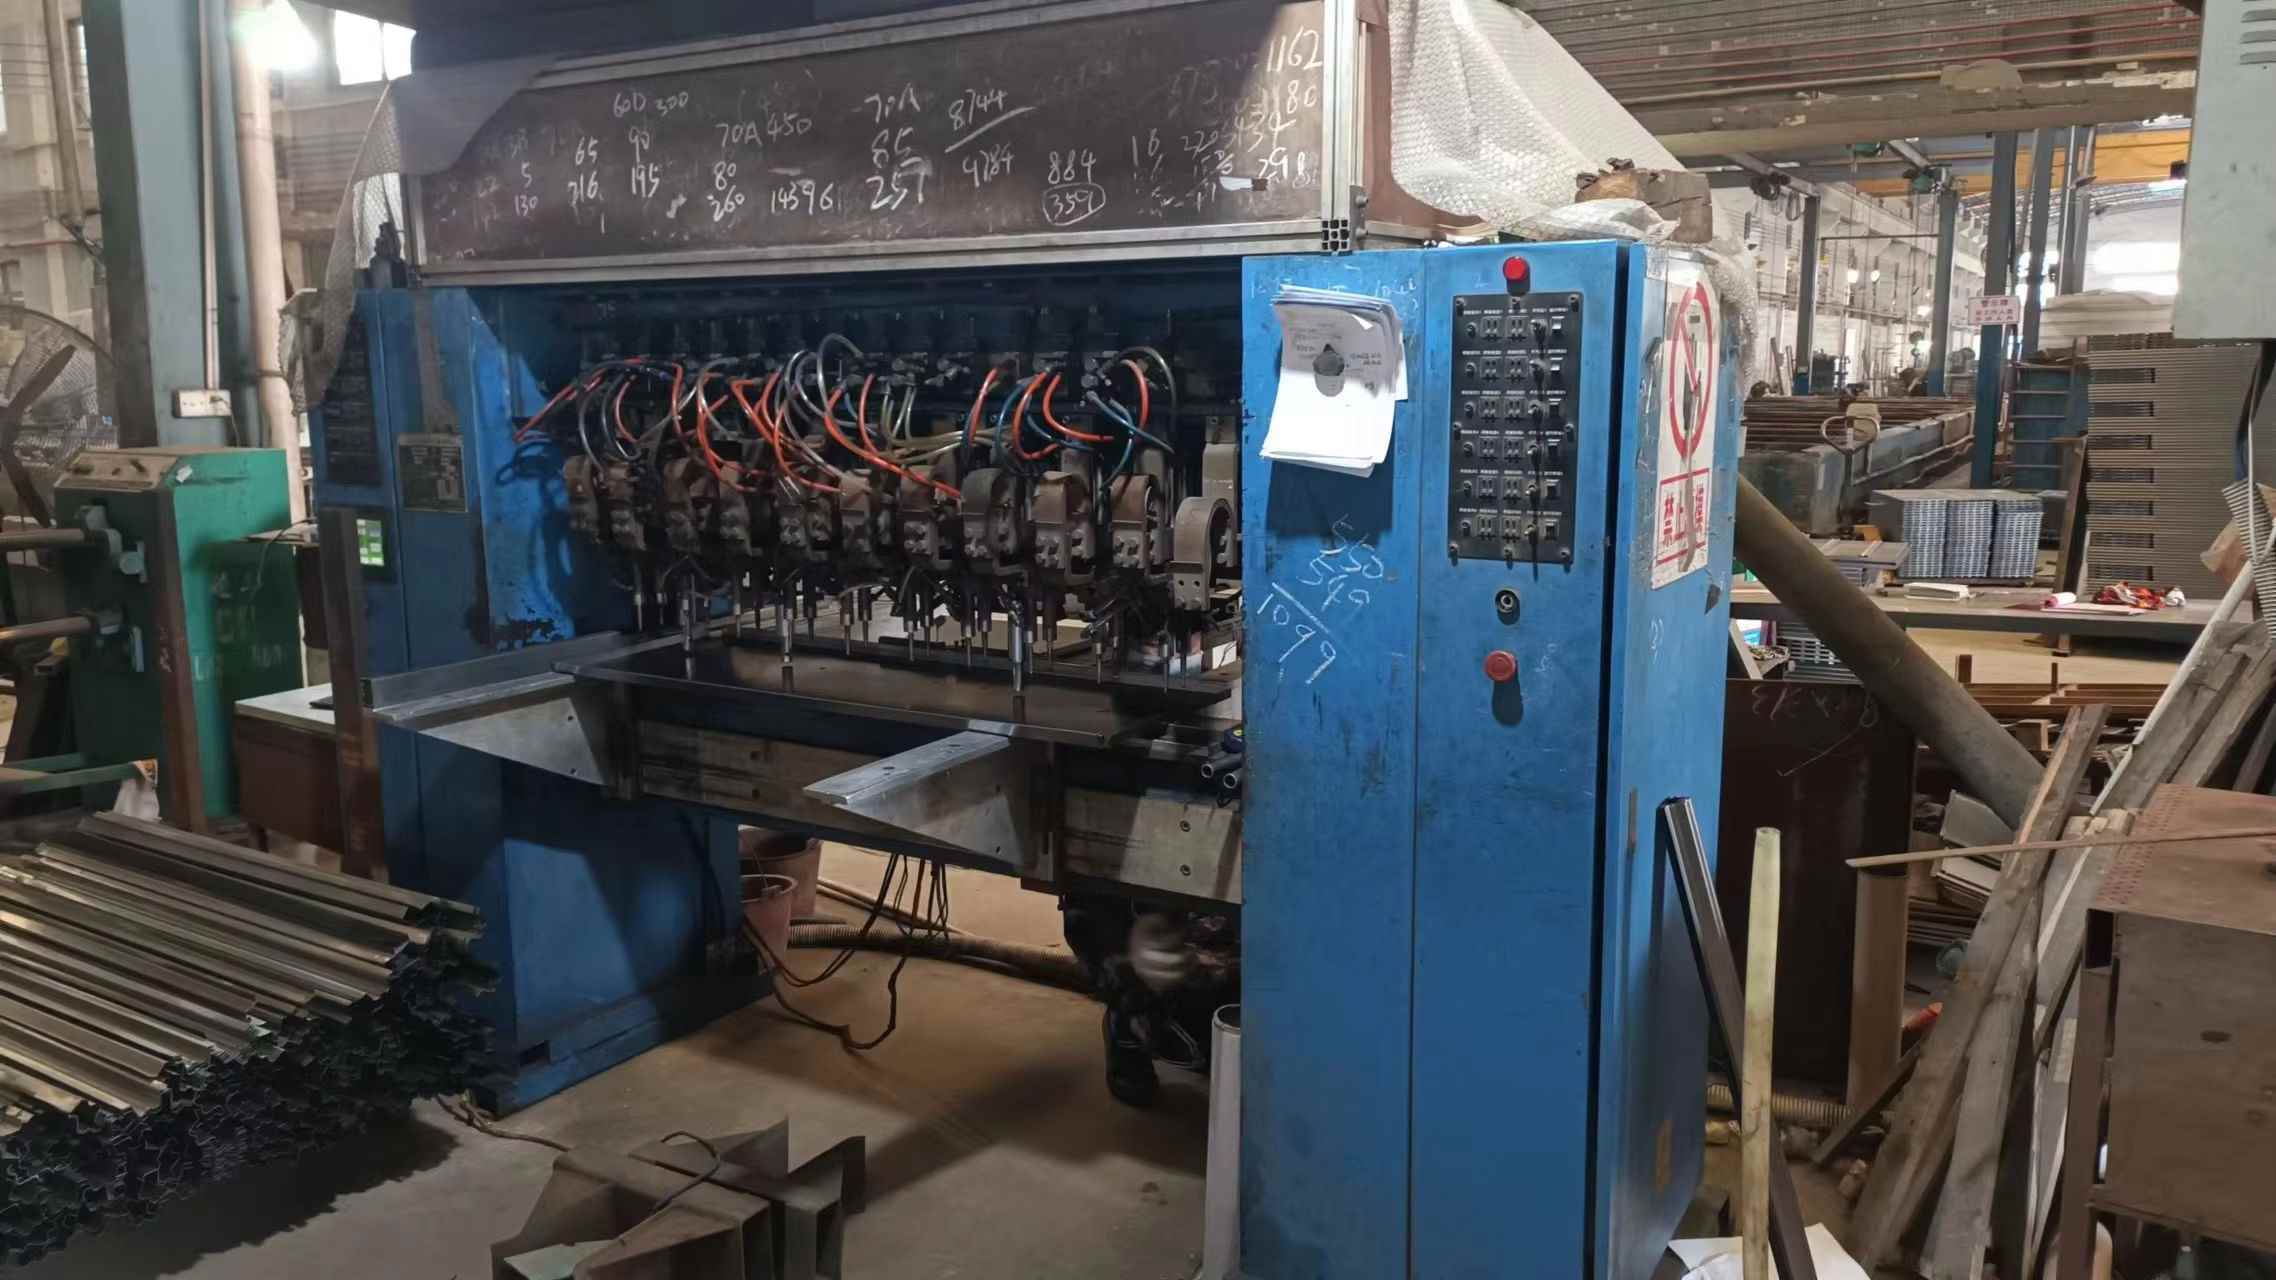
State-of-the-art machinery and multi-stage testing protocols ensuring ultimate durability and safety.
Addressing the complex requirements of worldwide enterprises across diverse verticals.
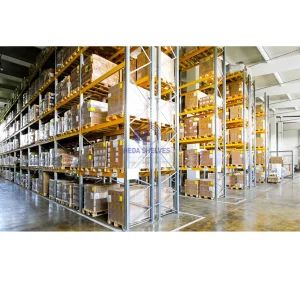
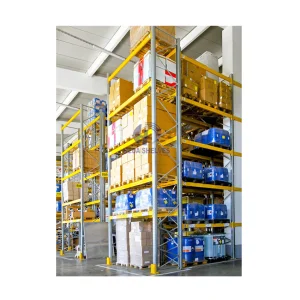
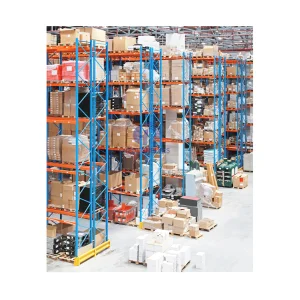
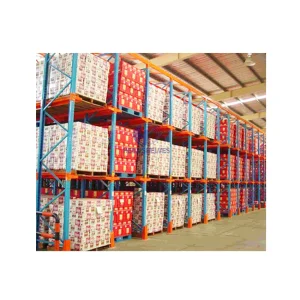
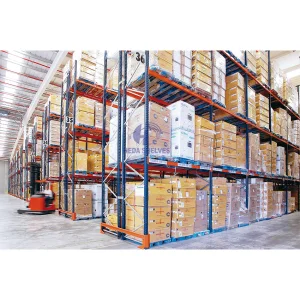
Modern supply chains demand ultra-high-density storage solutions. Our selective and drive-in pallet racking systems optimize cubic capacity, enabling rapid pick-and-pack fulfillment for global e-commerce and third-party logistics hubs.
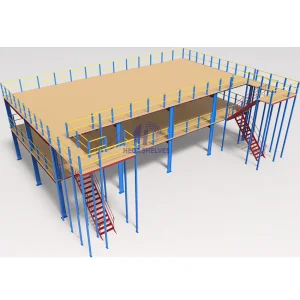
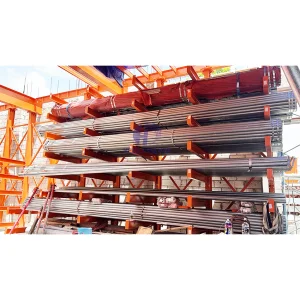
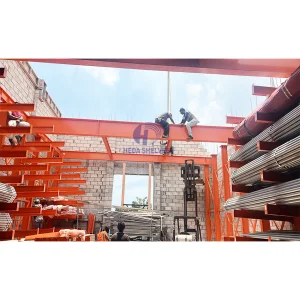
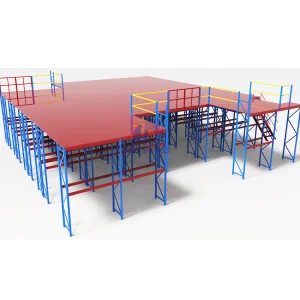
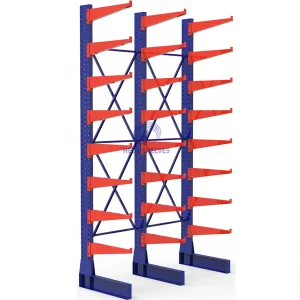
Heavy-duty cantilever racks and mezzanine floor systems provide robust structural support for bulky raw materials, steel beams, and heavy machinery parts, ensuring structural integrity and workplace safety.
CE-certified shop display racks and versatile shelving units combine aesthetic appeal with heavy load capacities, enhancing product visibility and merchandise turnover in high-traffic retail environments.
Pioneering the evolution of smart warehousing and automated storage integration.
Integration of high-tensile alloy steels and advanced anti-corrosion parkerising treatments to extend structural lifespan by over 35% in harsh industrial climates.
Adapting modular racking tolerances to seamlessly interface with Automated Storage and Retrieval Systems (AS/RS), AGVs, and robotic picking arms.
Deploying smart sensor nodes within upright frames to monitor real-time load distribution and predict structural fatigue before safety thresholds are reached.
Transitioning our 35,000 m² facility towards solar-powered automated powder coating lines and sustainable green manufacturing practices.
Meeting international engineering standards and offering dedicated global project support.
Our racking systems adhere to stringent international standards, including CE certification, ISO9001 quality management, FEM (European Federation of Materials Handling) structural design codes, and RMI (Rack Manufacturers Institute) guidelines, ensuring hassle-free customs clearance and site inspection approval worldwide.
From initial CAD layout drafting and seismic load calculation to export packaging and on-site installation supervision, our team of 28 senior structural engineers provides end-to-end technical consultation for overseas commercial and industrial projects.
Expert insights on customization, load capacities, installation, and international shipping.
Discover our complete portfolio of high-efficiency cantilever racks, longspan shelving, and multi-tier mezzanine floors.
 Hedaracking