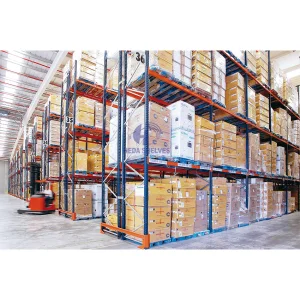
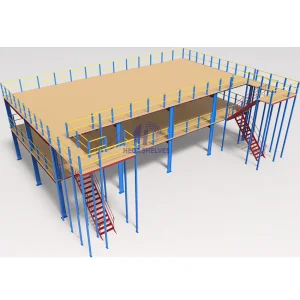
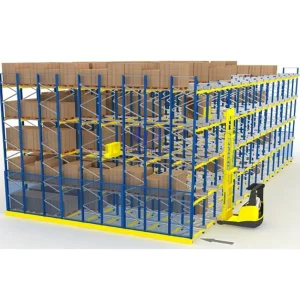
Discover our elite collection of engineered heavy-duty racking systems, robotic shuttle structures, and automated industrial storage units designed for maximum density and throughput.
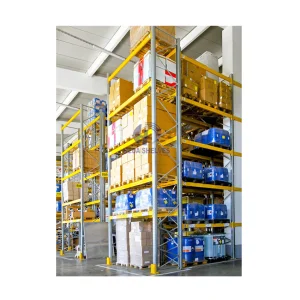
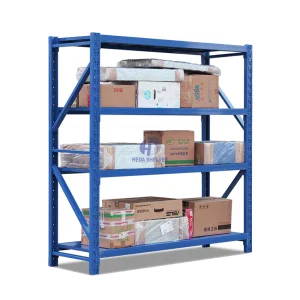
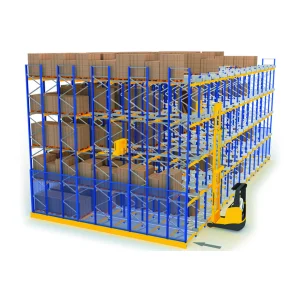
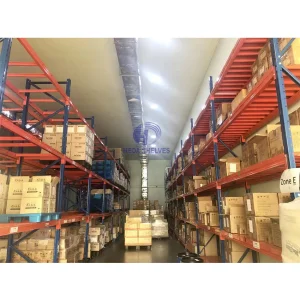
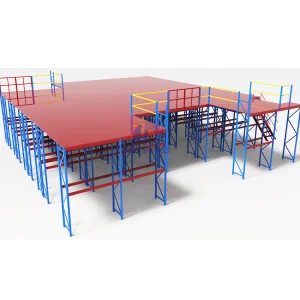
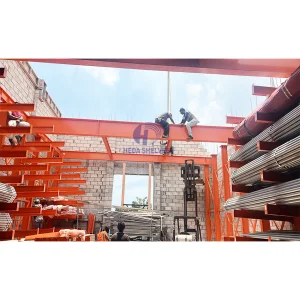
Backed by rigorous engineering excellence, automated manufacturing pipelines, and a dedication to global compliance, Heda Warehouse Equipment stands at the pinnacle of international storage solution manufacturing.
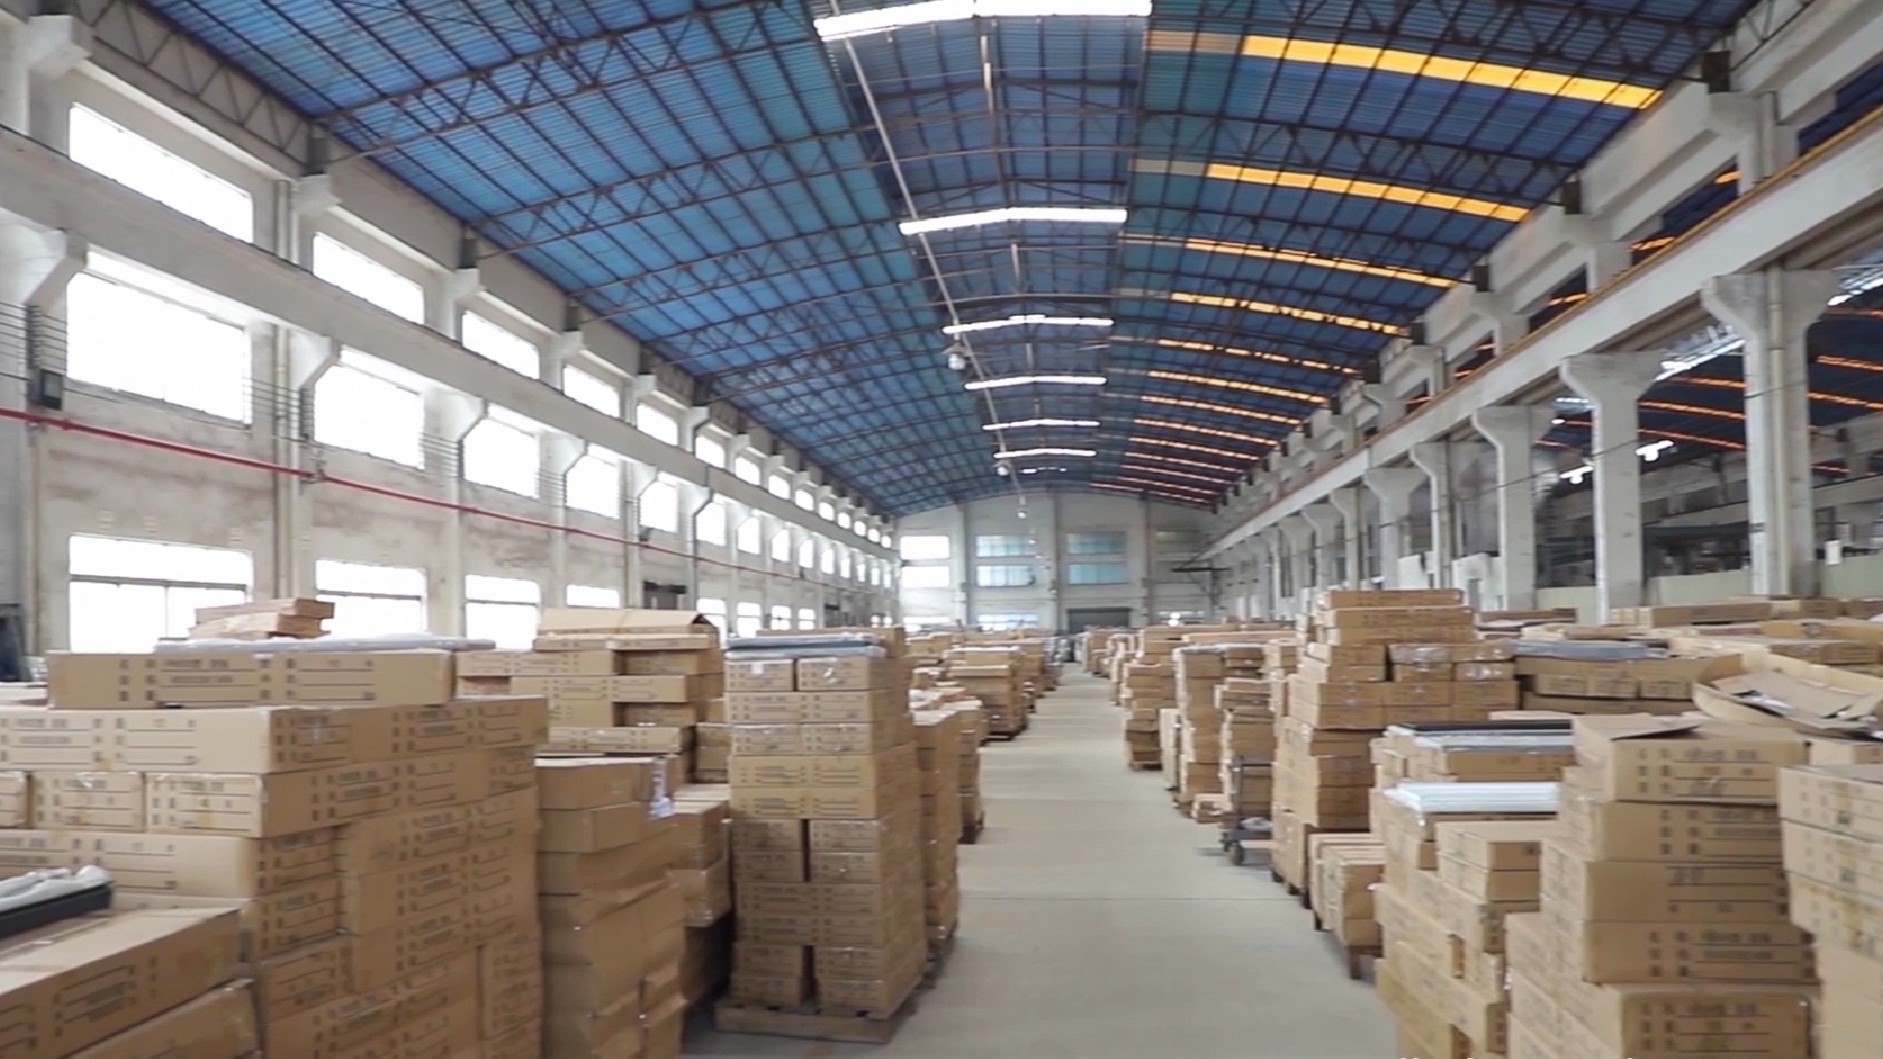
Established in 2014, Shenzhen Heda Warehouse Equipment Co., Ltd. is a premier manufacturer specializing in heavy-duty warehouse racking and industrial storage solutions. Spanning a modern manufacturing facility of 35,000 m², our enterprise integrates R&D, design, production, and international marketing to serve diverse storage needs worldwide. With 12 years of industry experience and 8 years of dedicated export expertise, we deliver high-caliber storage systems that generate over $28 million in annual export revenue.
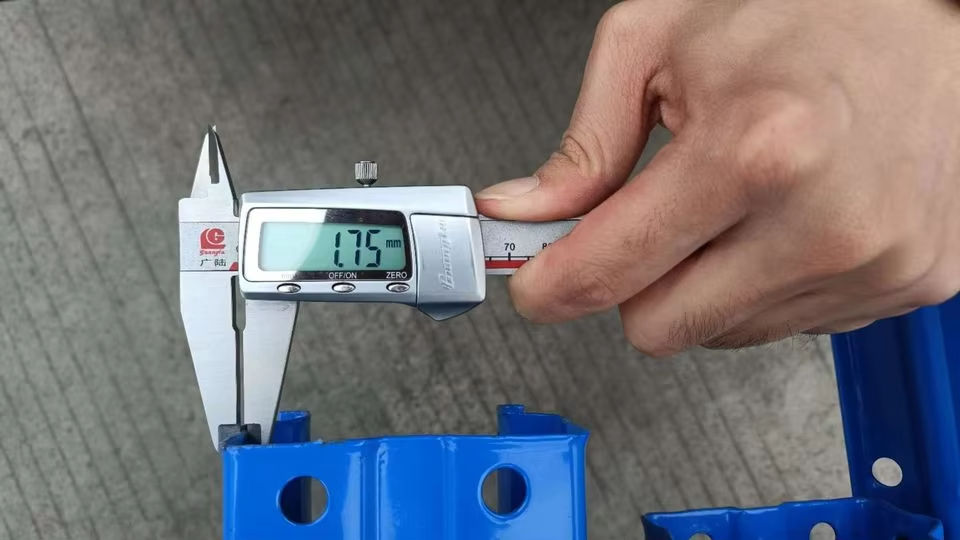
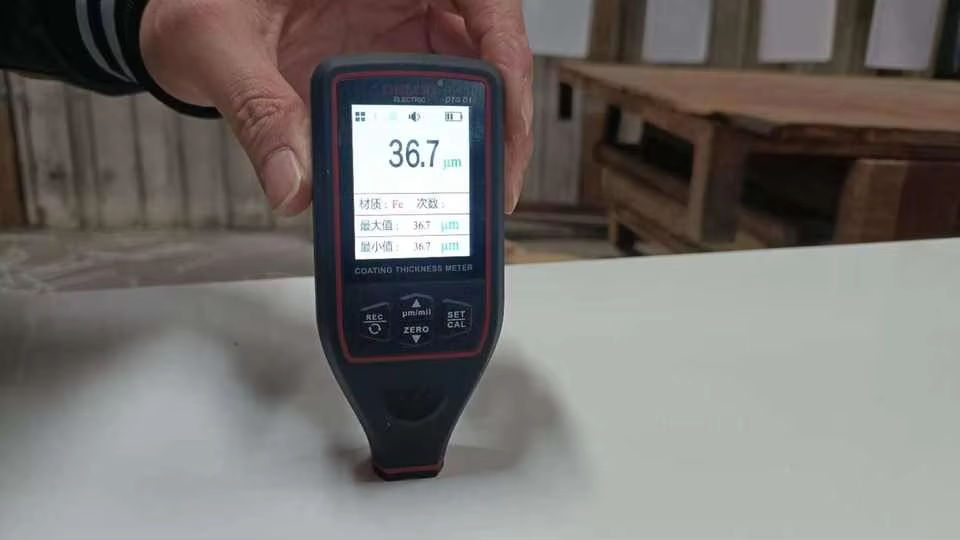
At Heda, quality control and engineering innovation drive our core operations. Our robust QC department comprises 45 skilled inspectors utilizing rigorous testing methods, including raw material tensile testing, automated weld flaw detection, layer load-bearing stress analysis, and salt spray surface corrosion testing. Supported by a professional R&D team of 28 senior structural engineers, we maintain strong full-customization capabilities (OEM/ODM)—offering tailored rack dimensions, load capacities, surface coatings, and layout designs. Driven by continuous innovation, we launched over 120 new dynamic storage products and component upgrades last year.
Operating with a strong direct-factory and international trade background, we have built a resilient ecosystem supported by over 800 supply chain partners. Our products are exported to major global markets, including North America, Western Europe, Southeast Asia, and the Middle East. We proudly serve a diverse clientele ranging from third-party logistics (3PL) providers and large distribution centers to industrial manufacturers and wholesale equipment distributors.
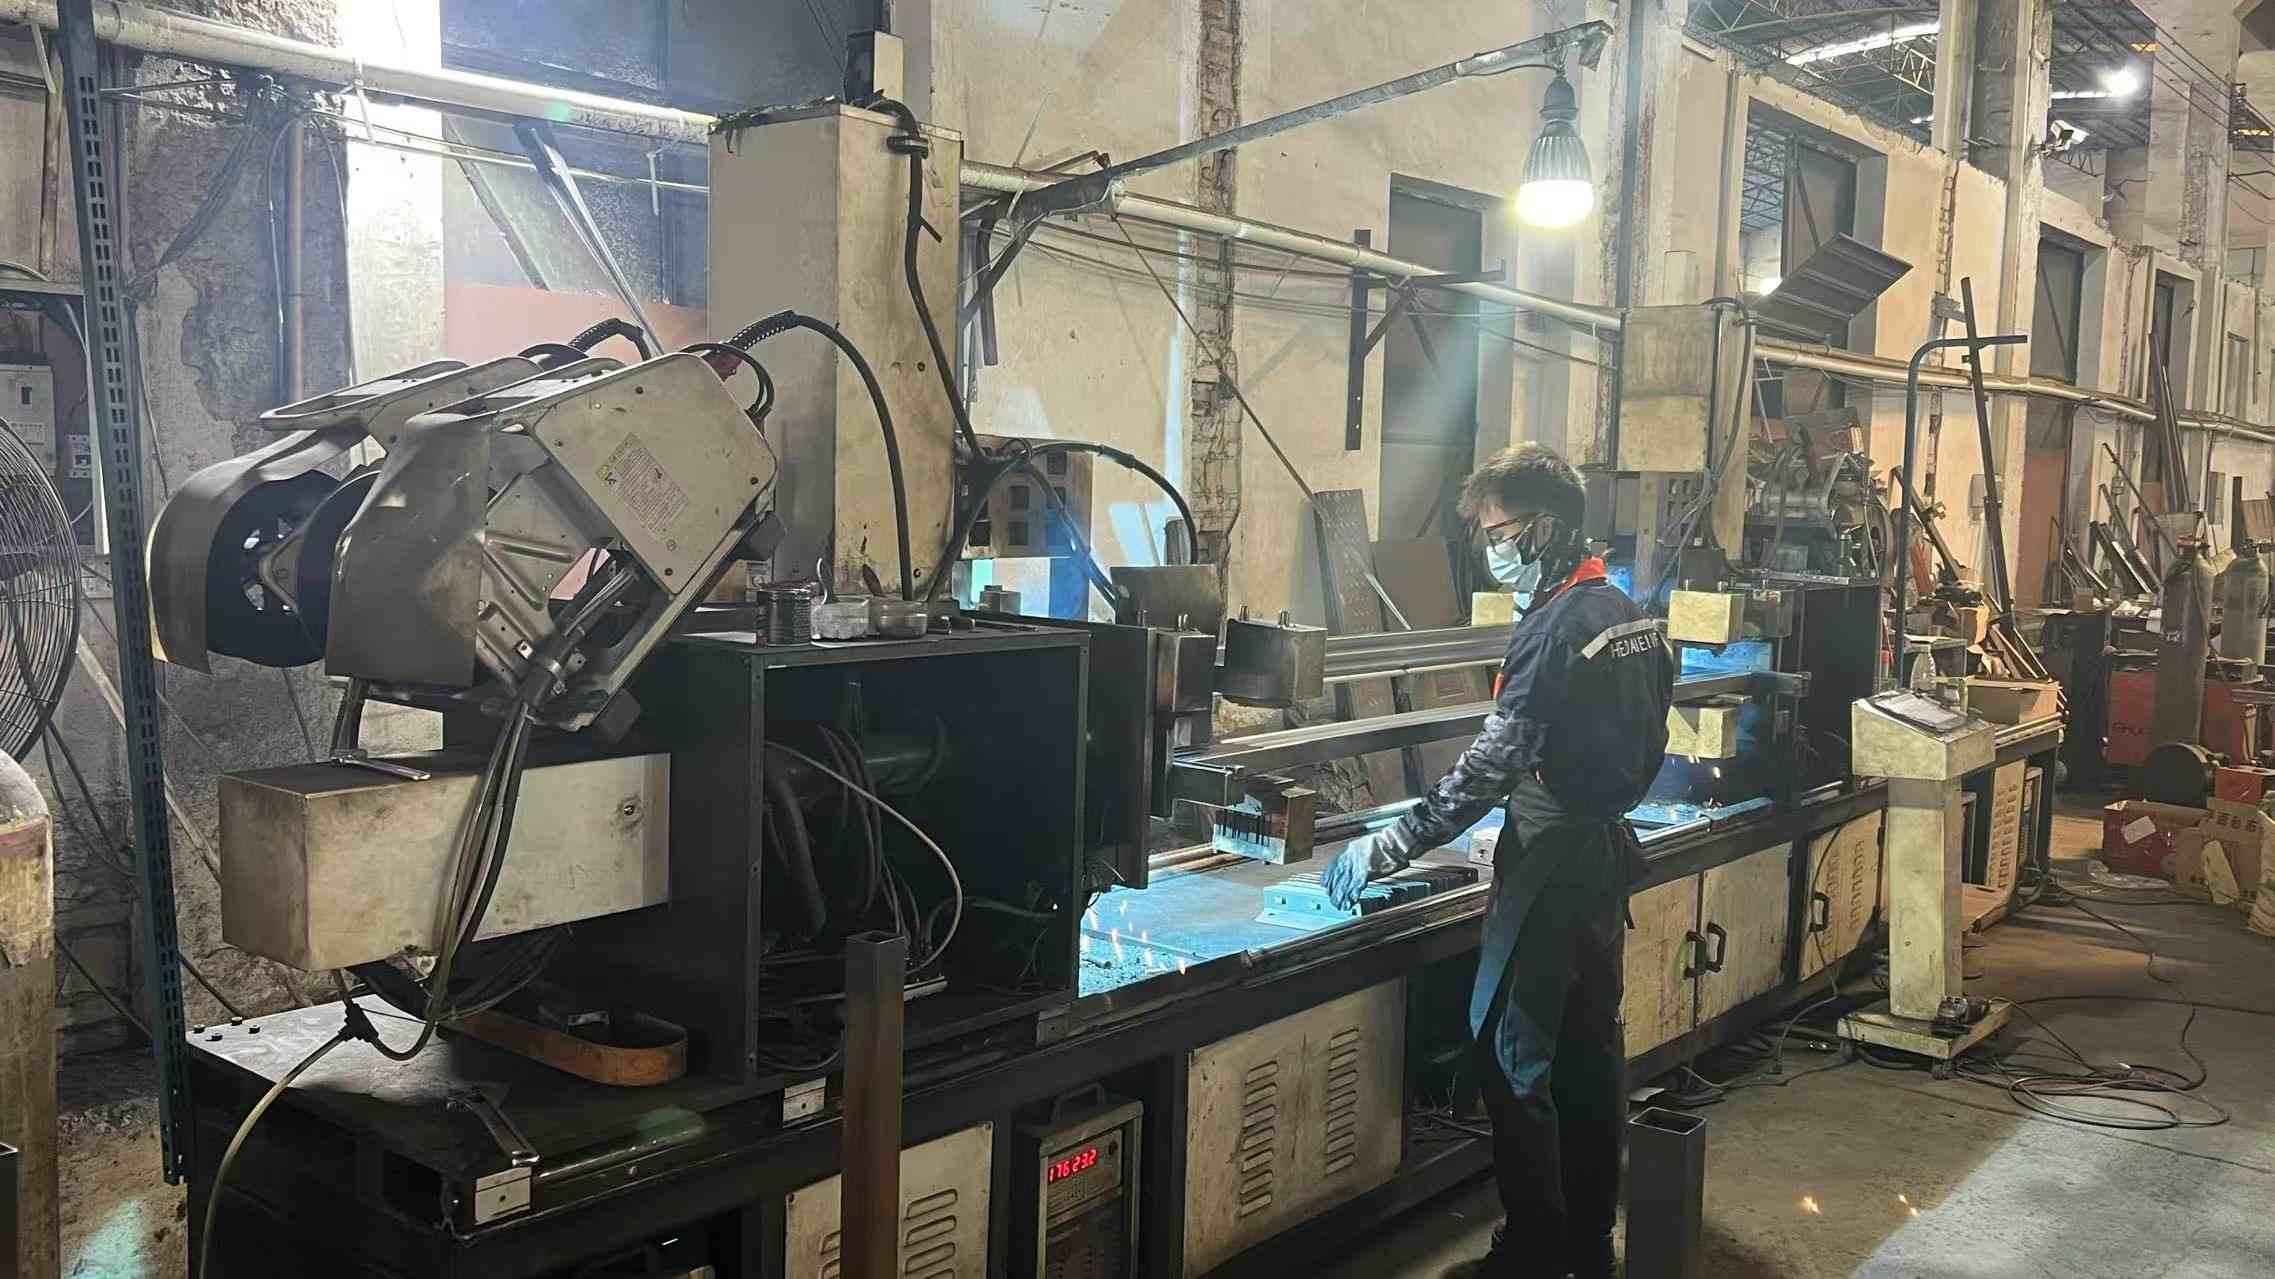
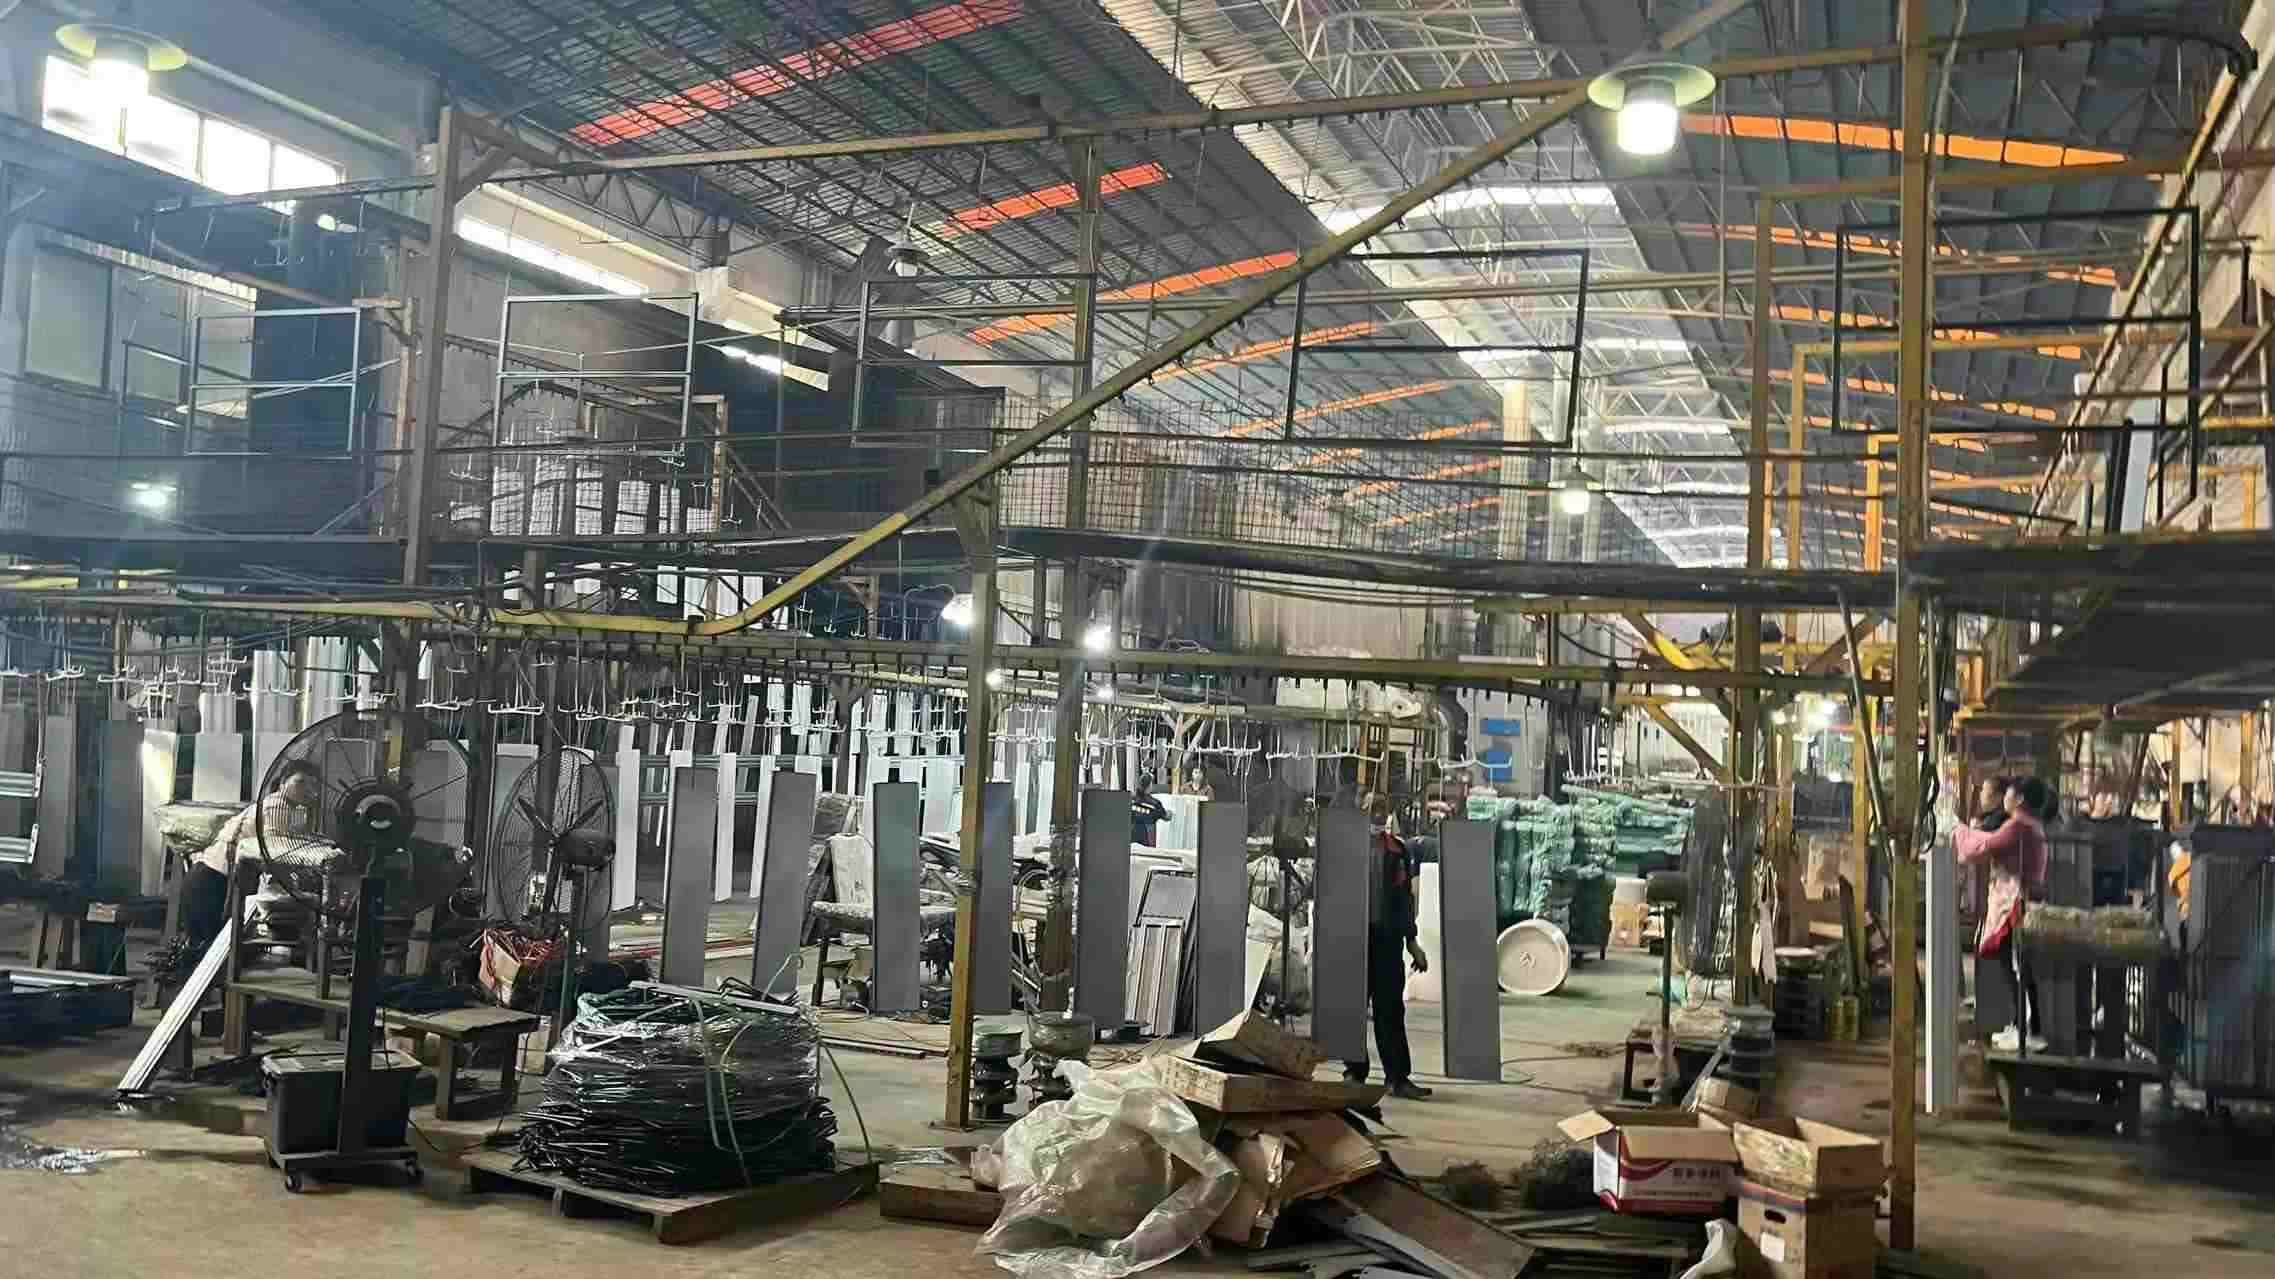
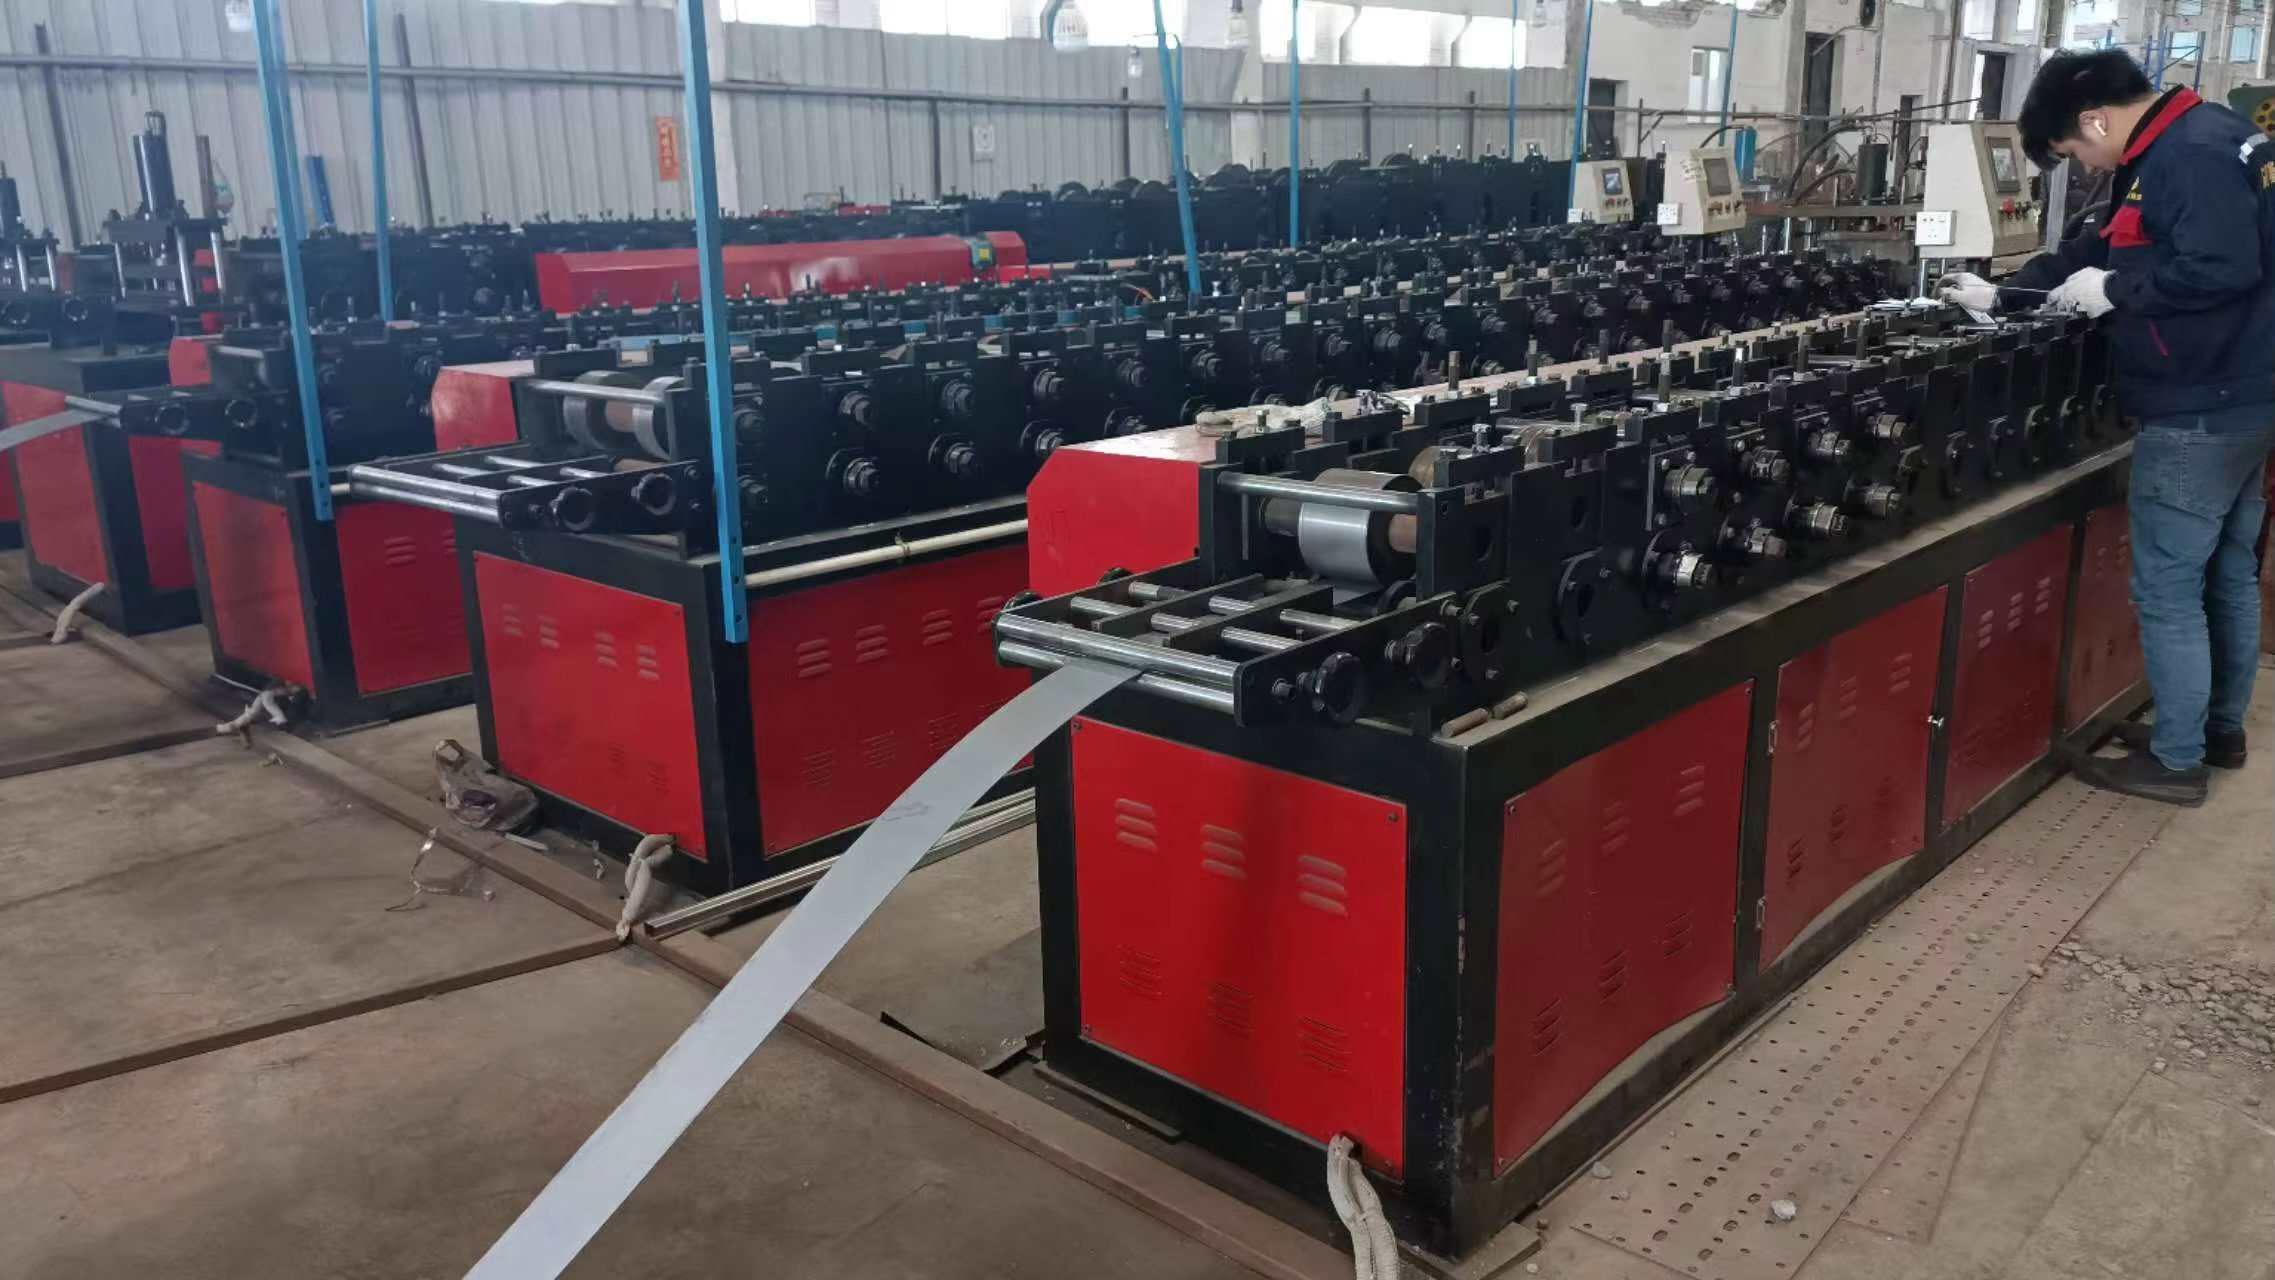
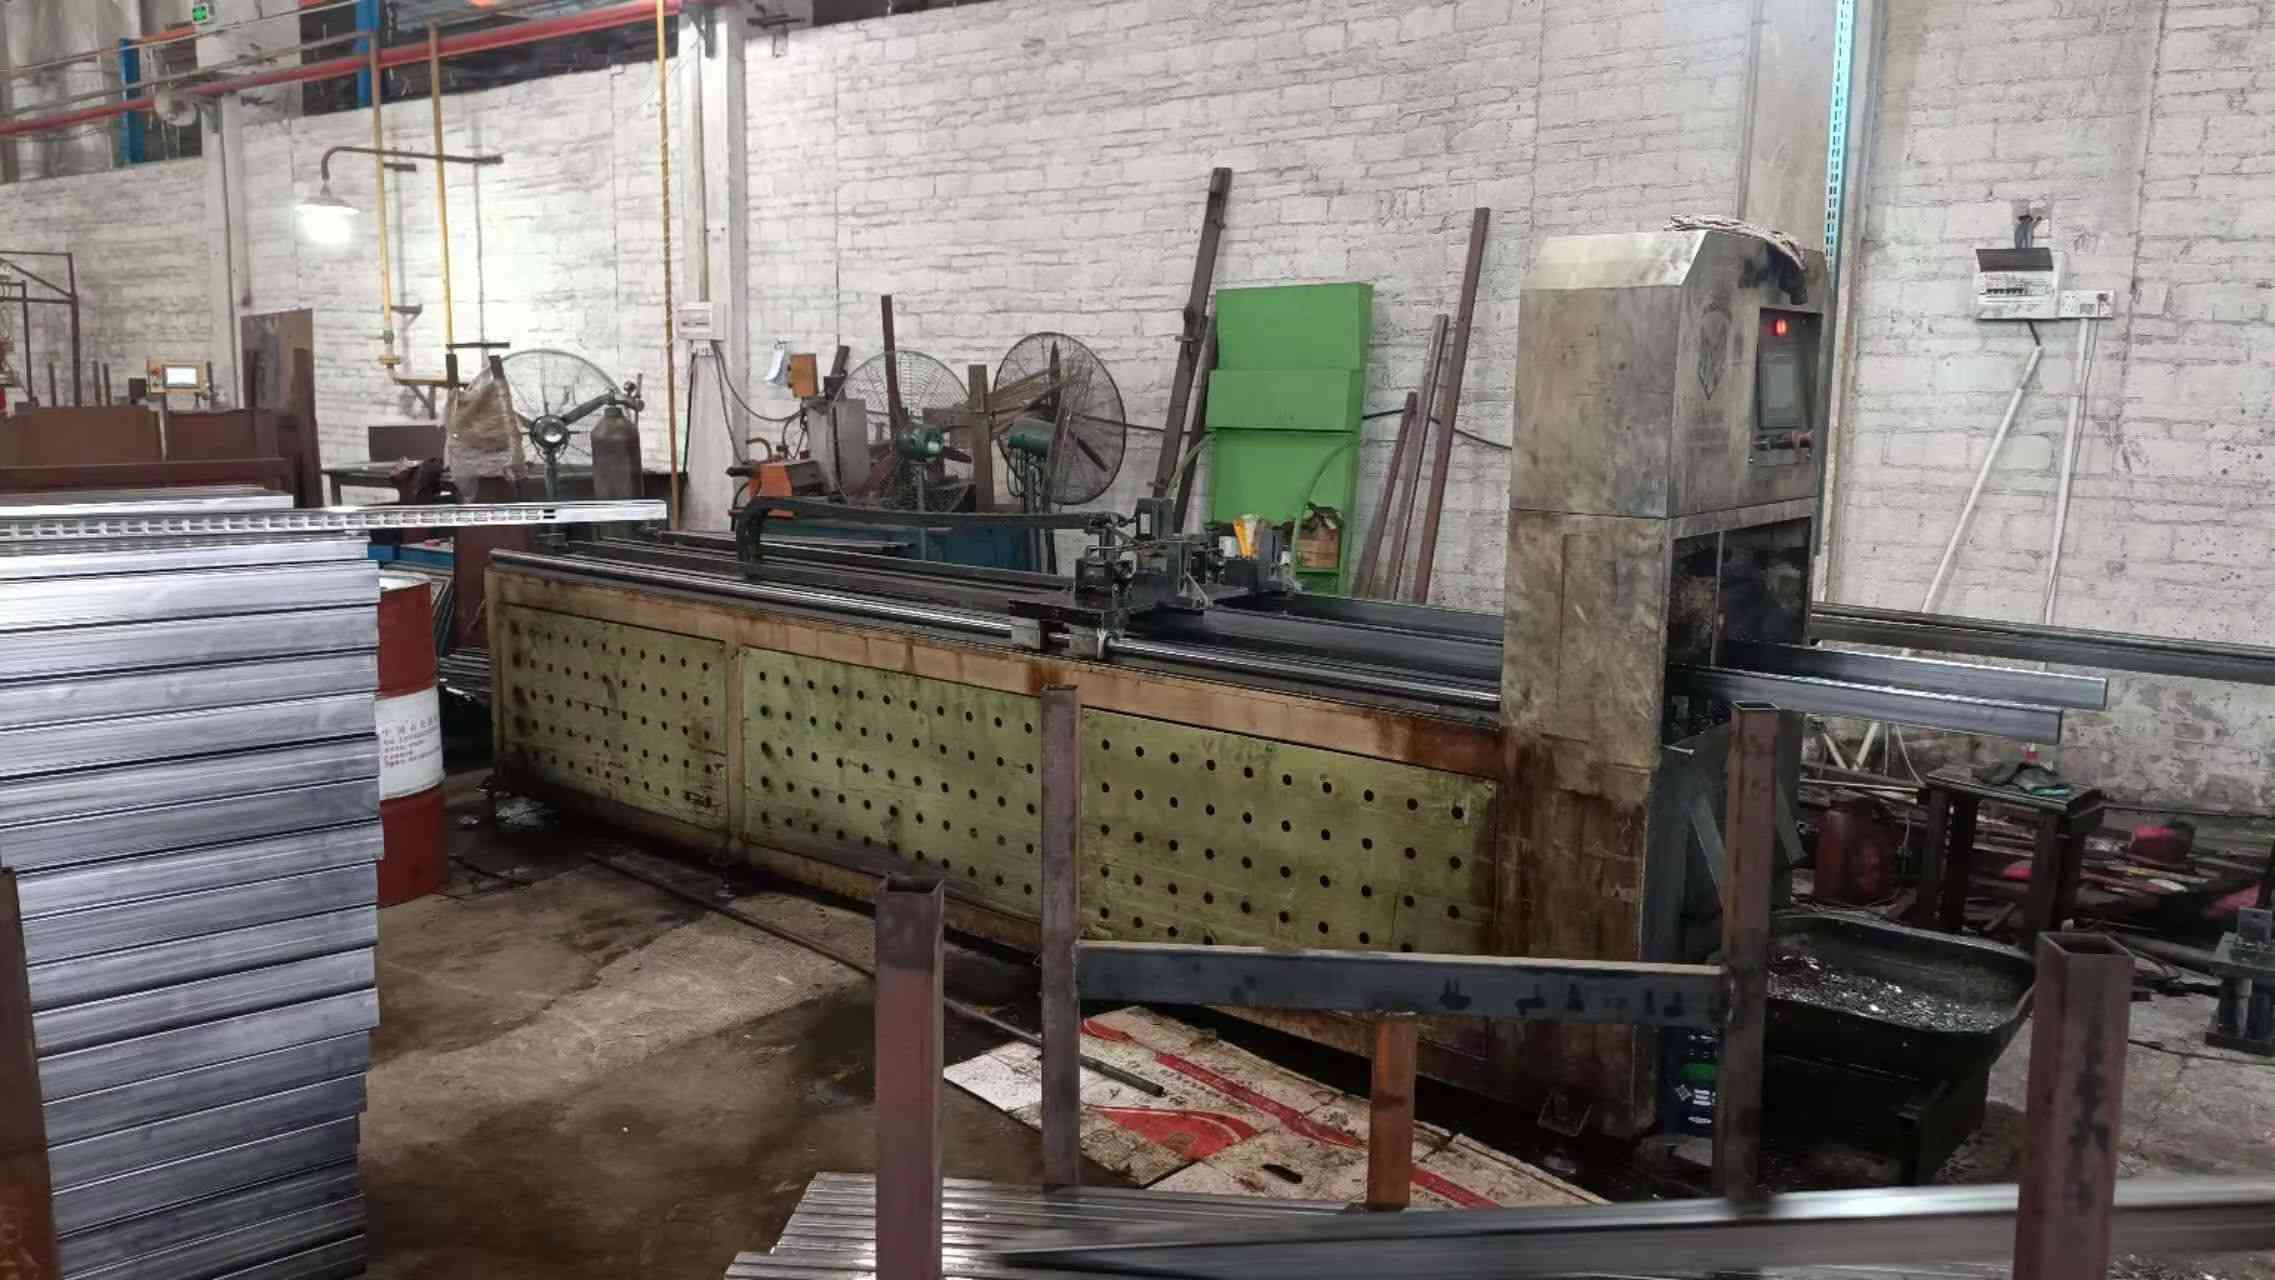
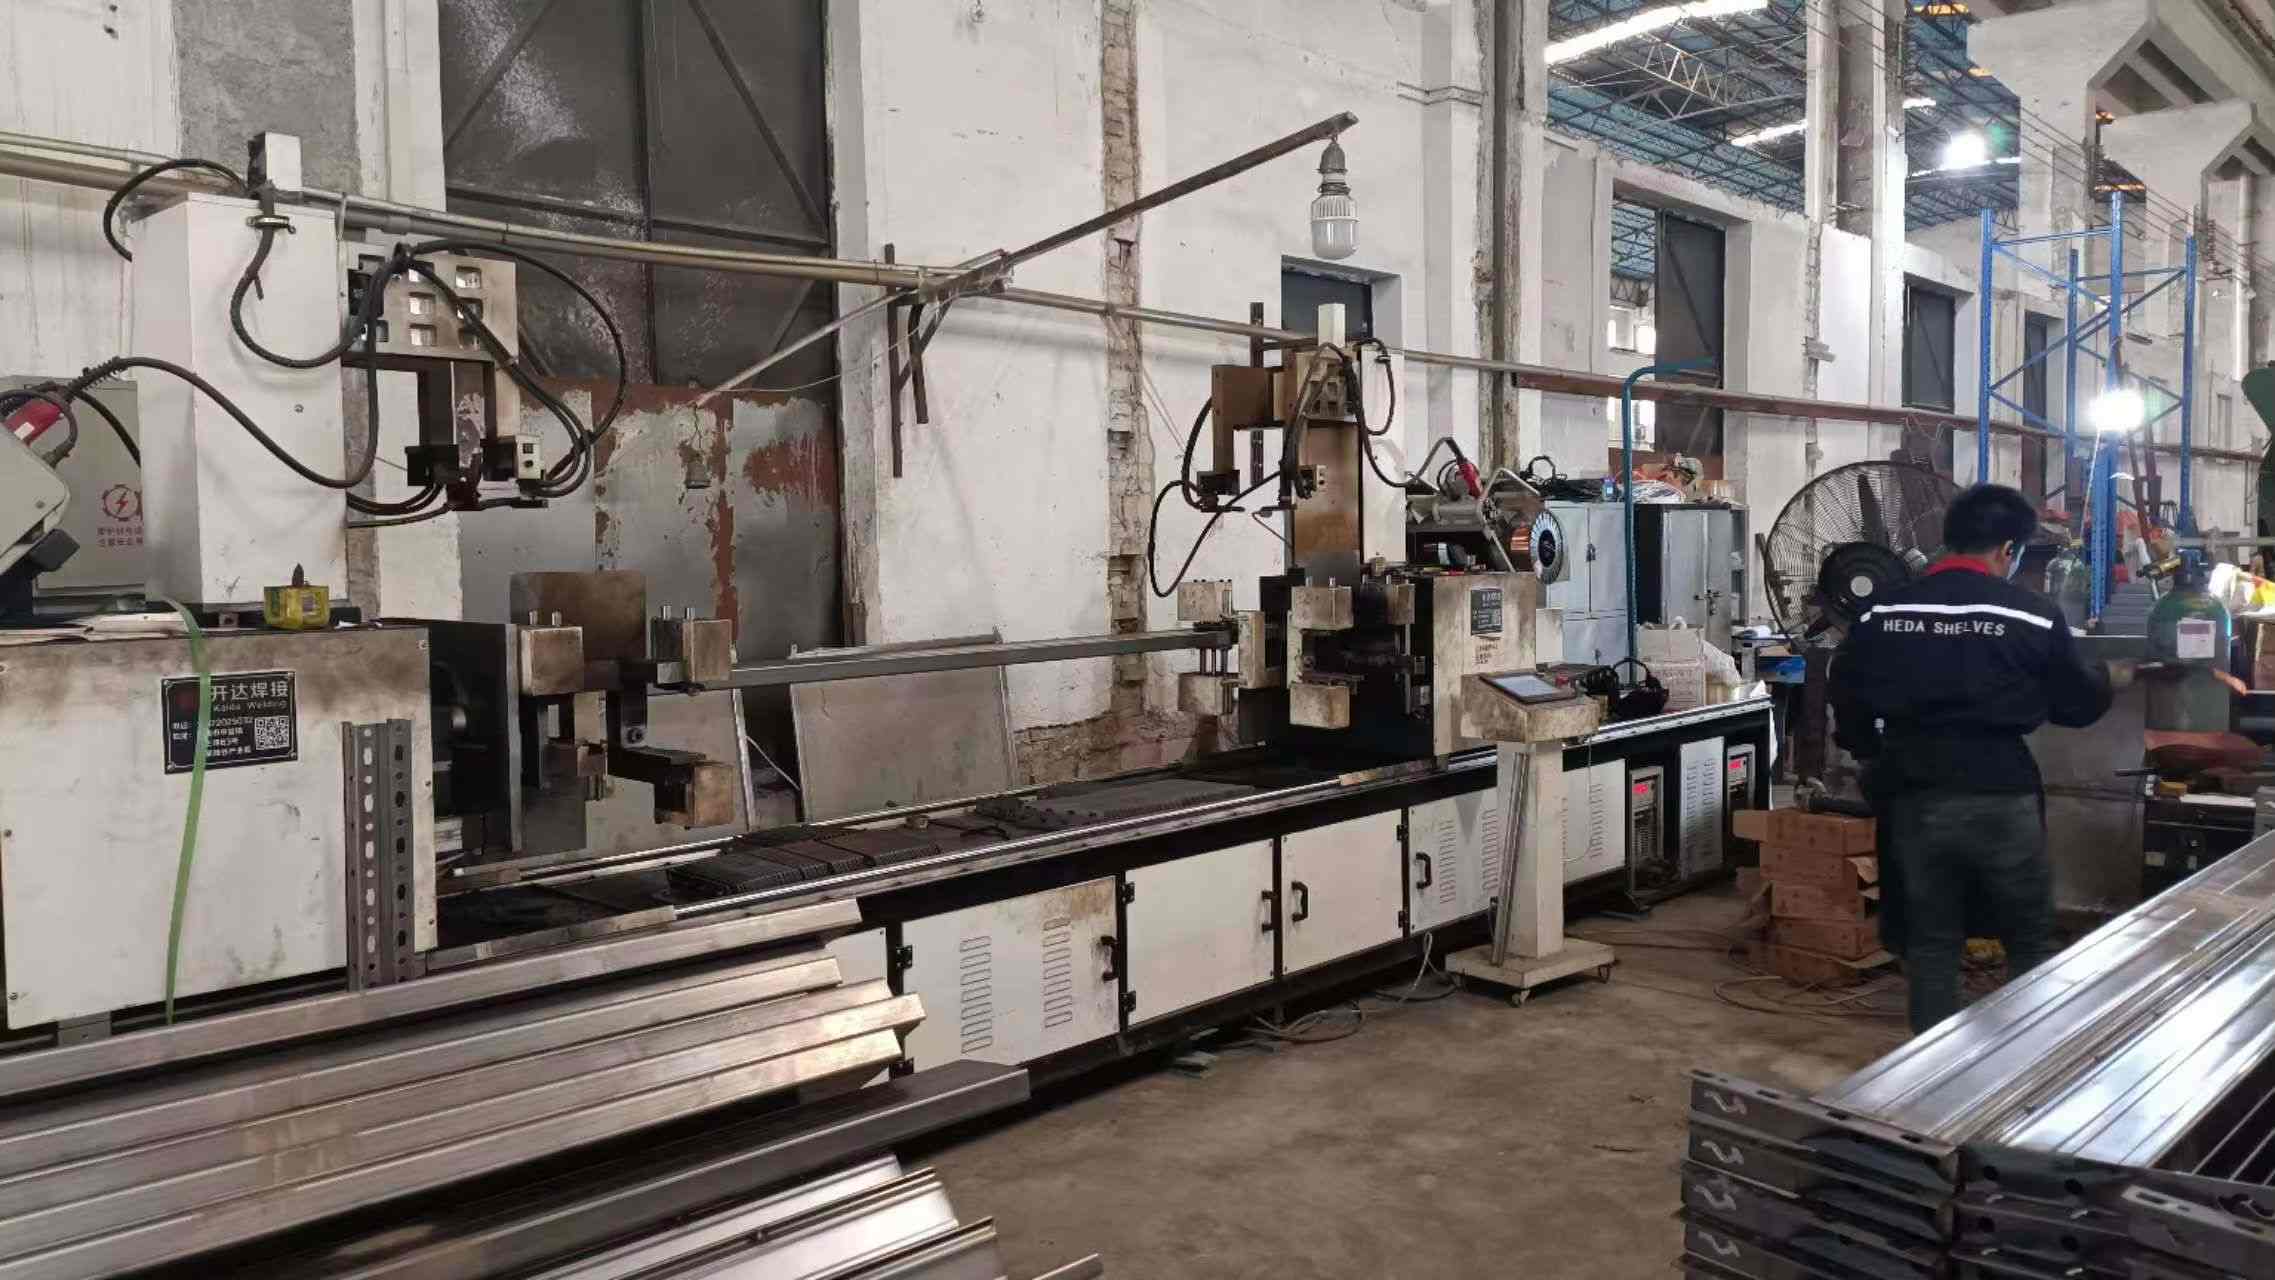
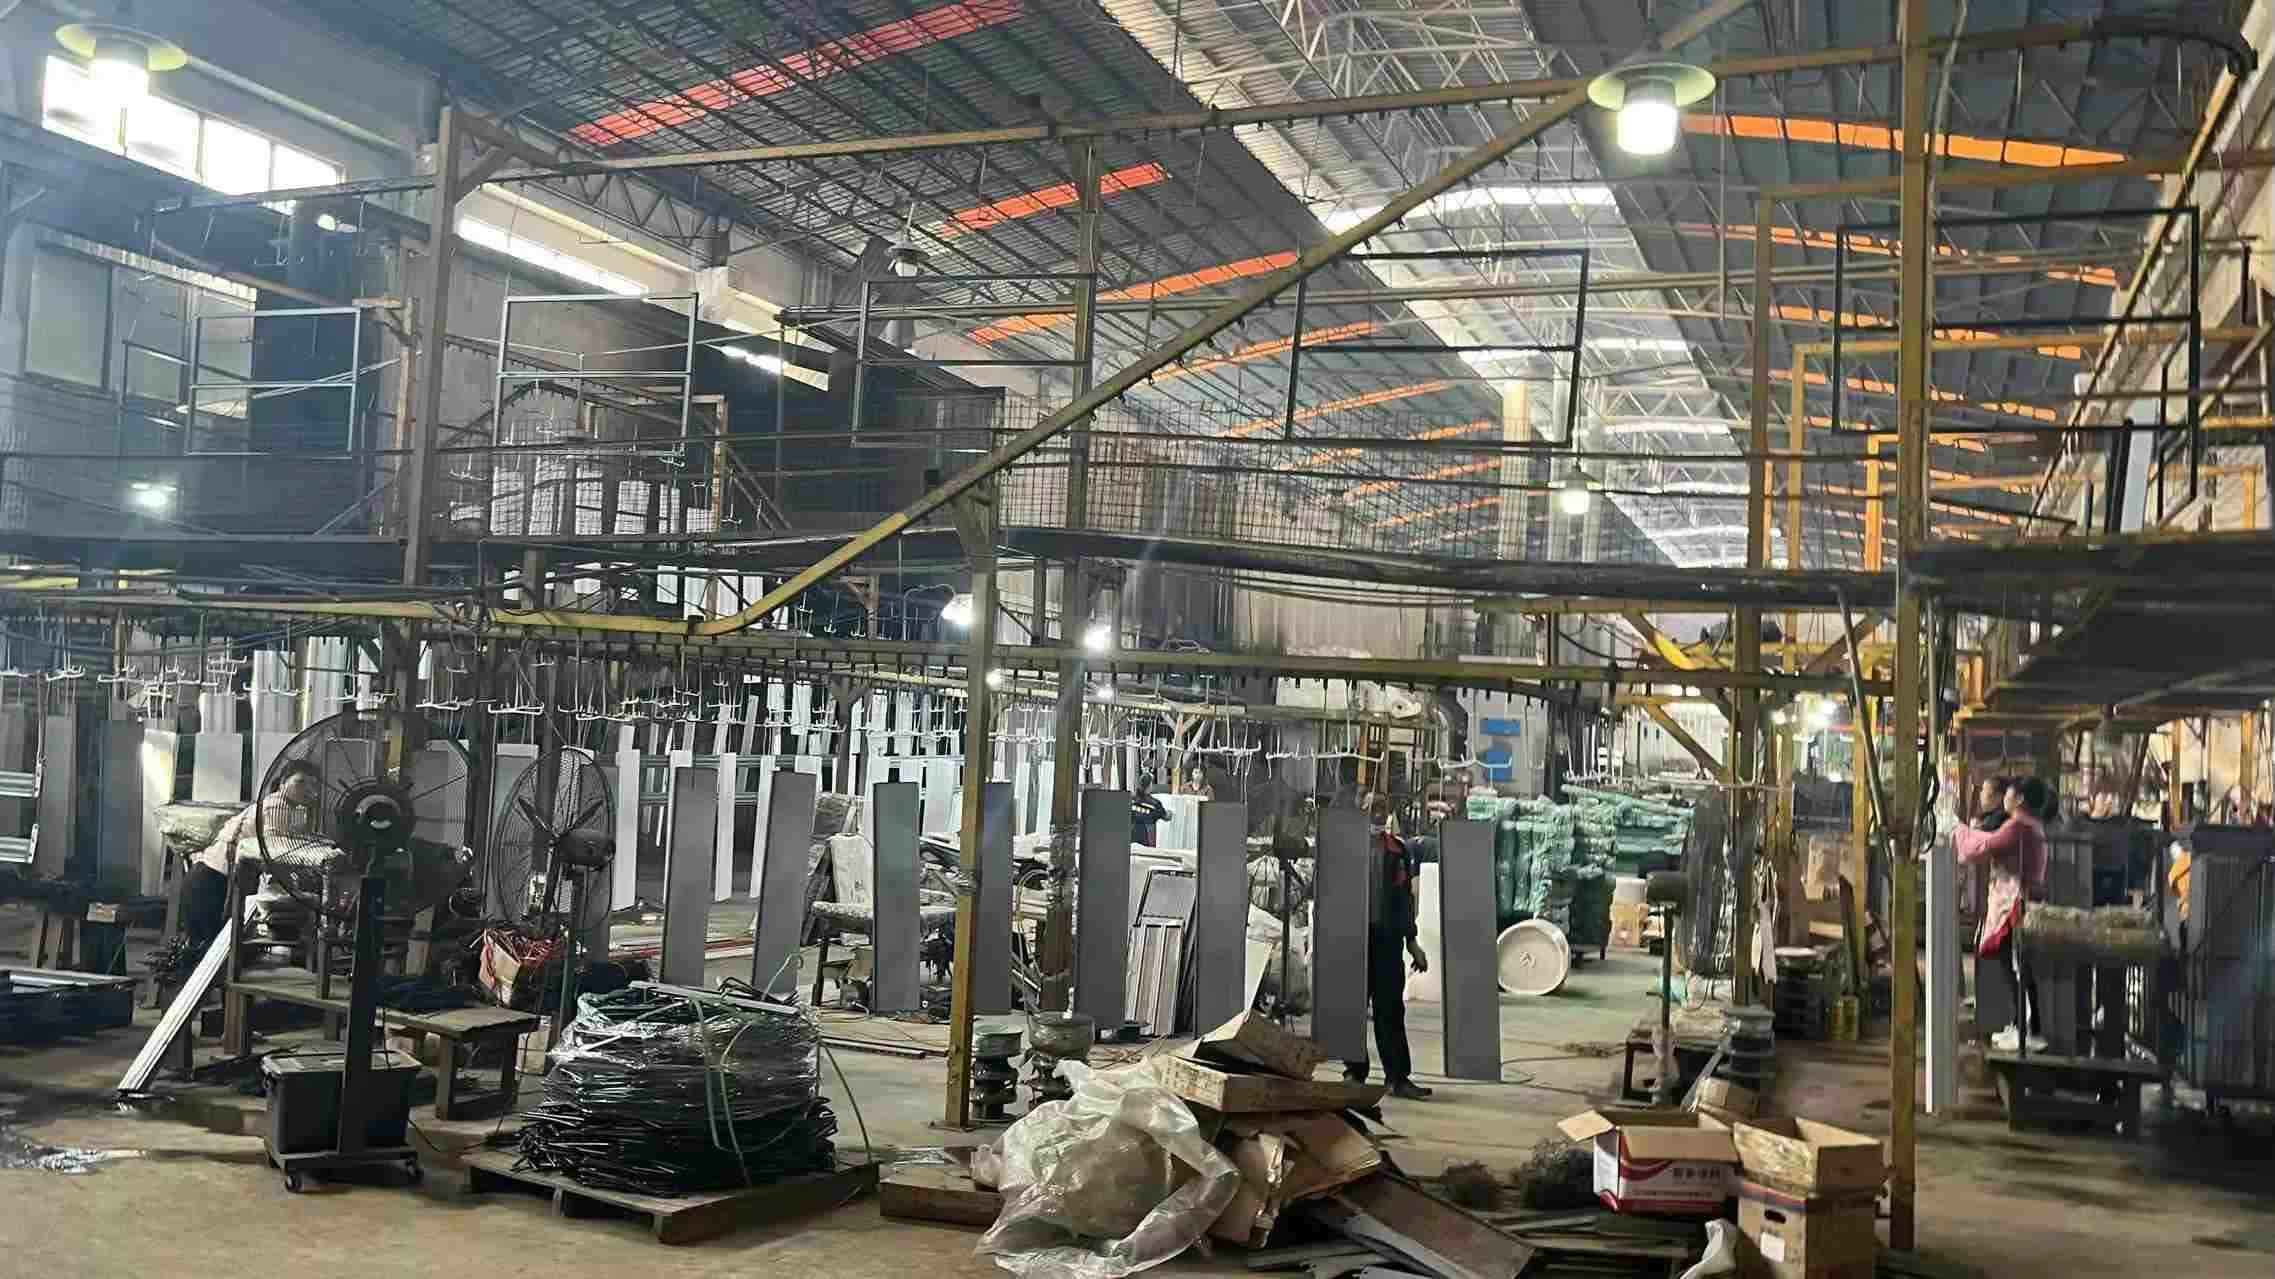
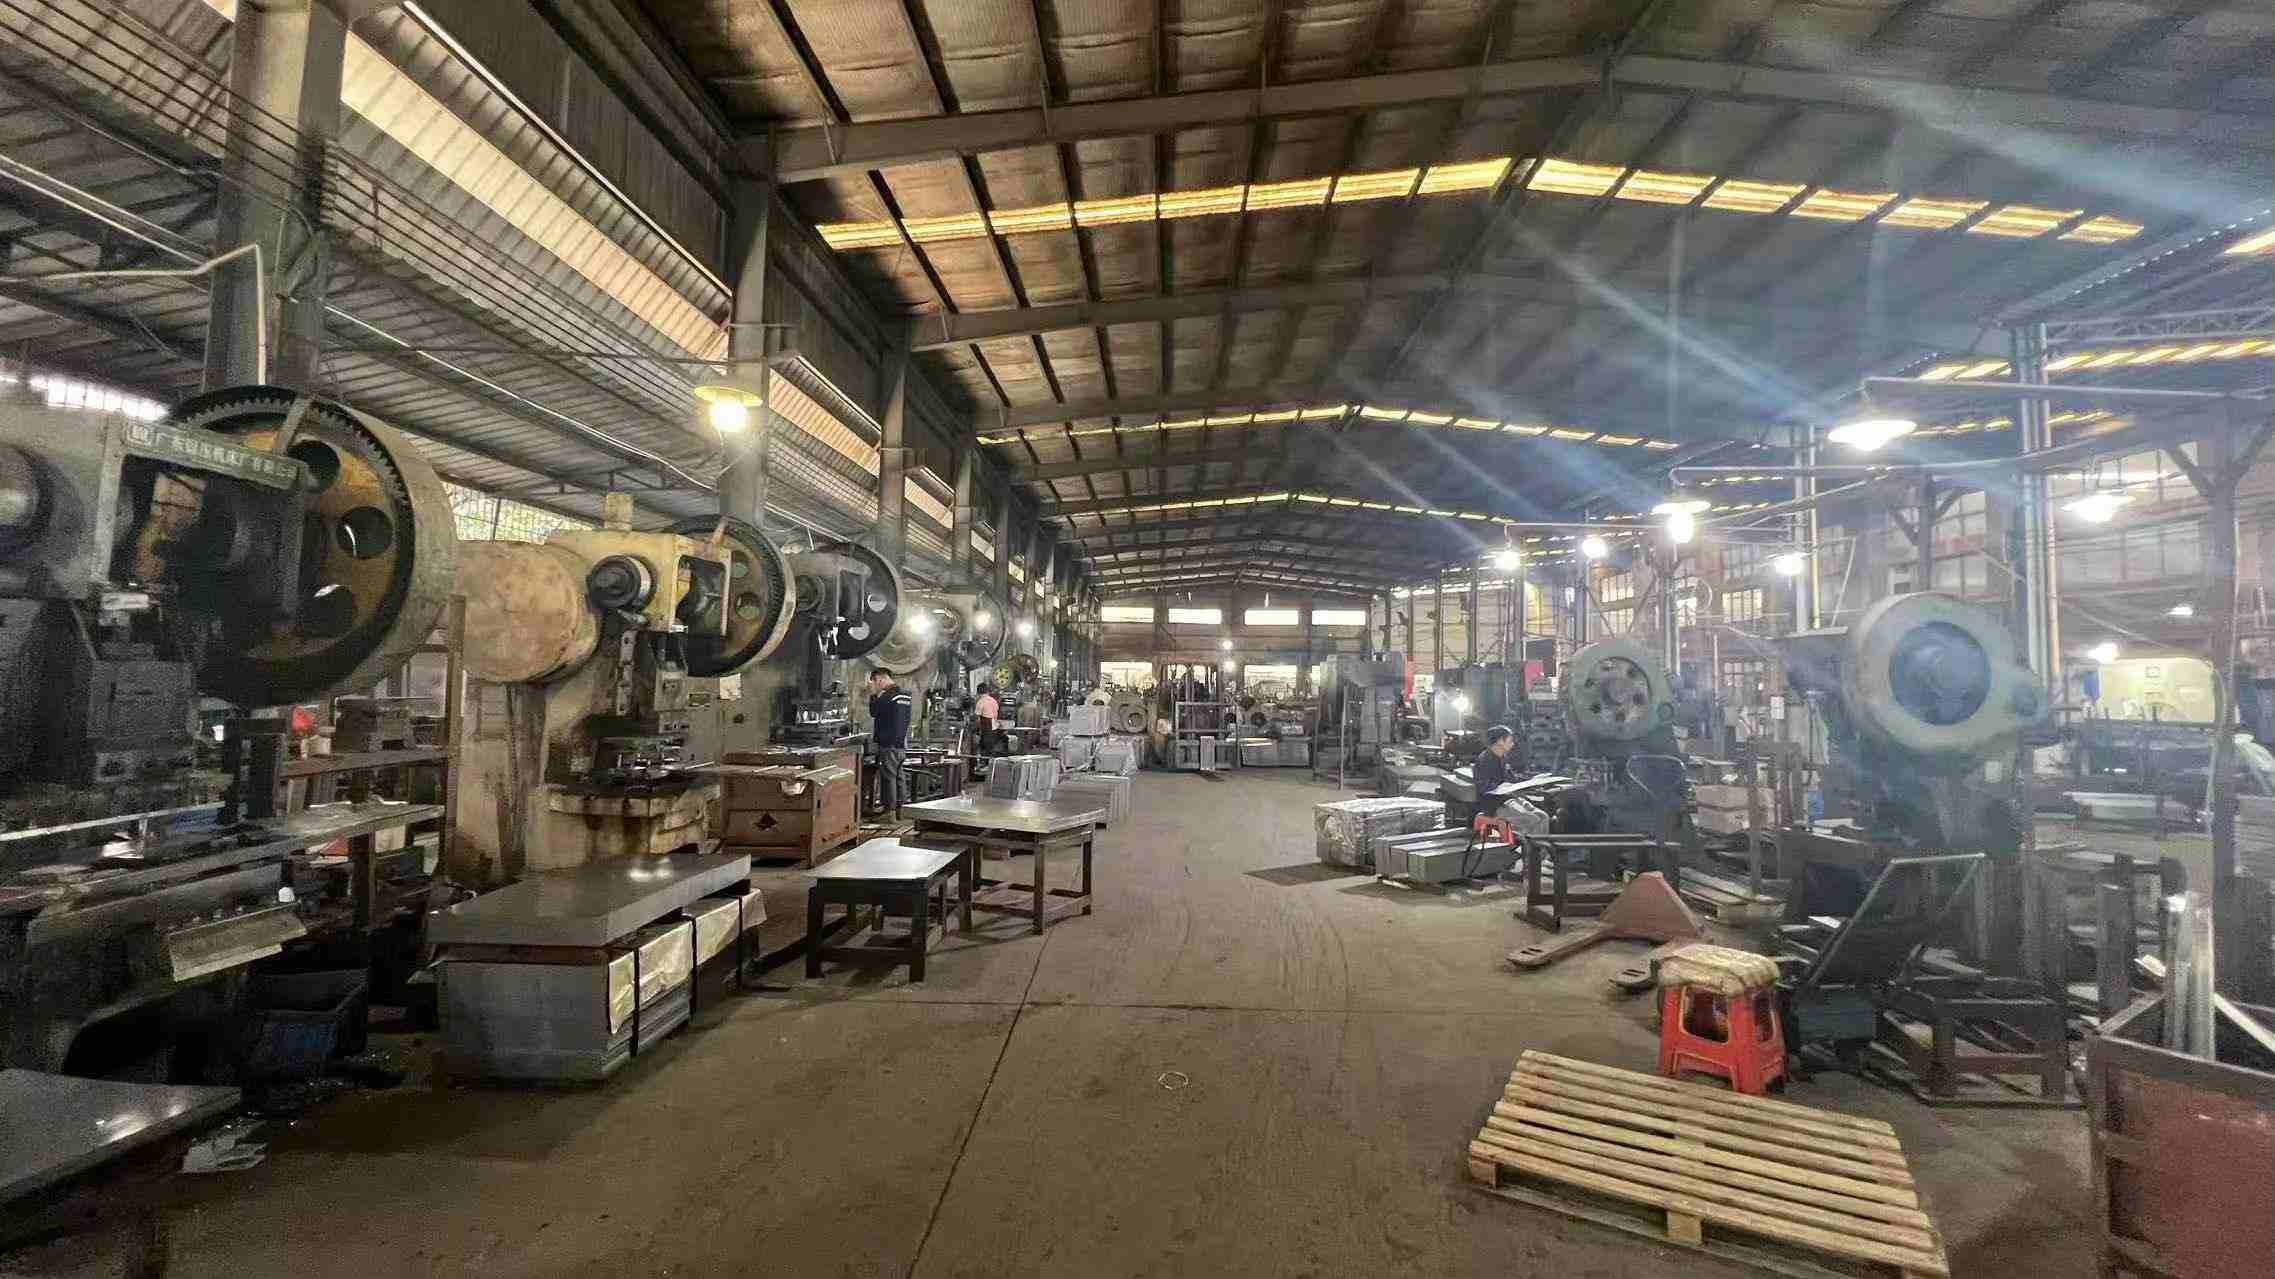
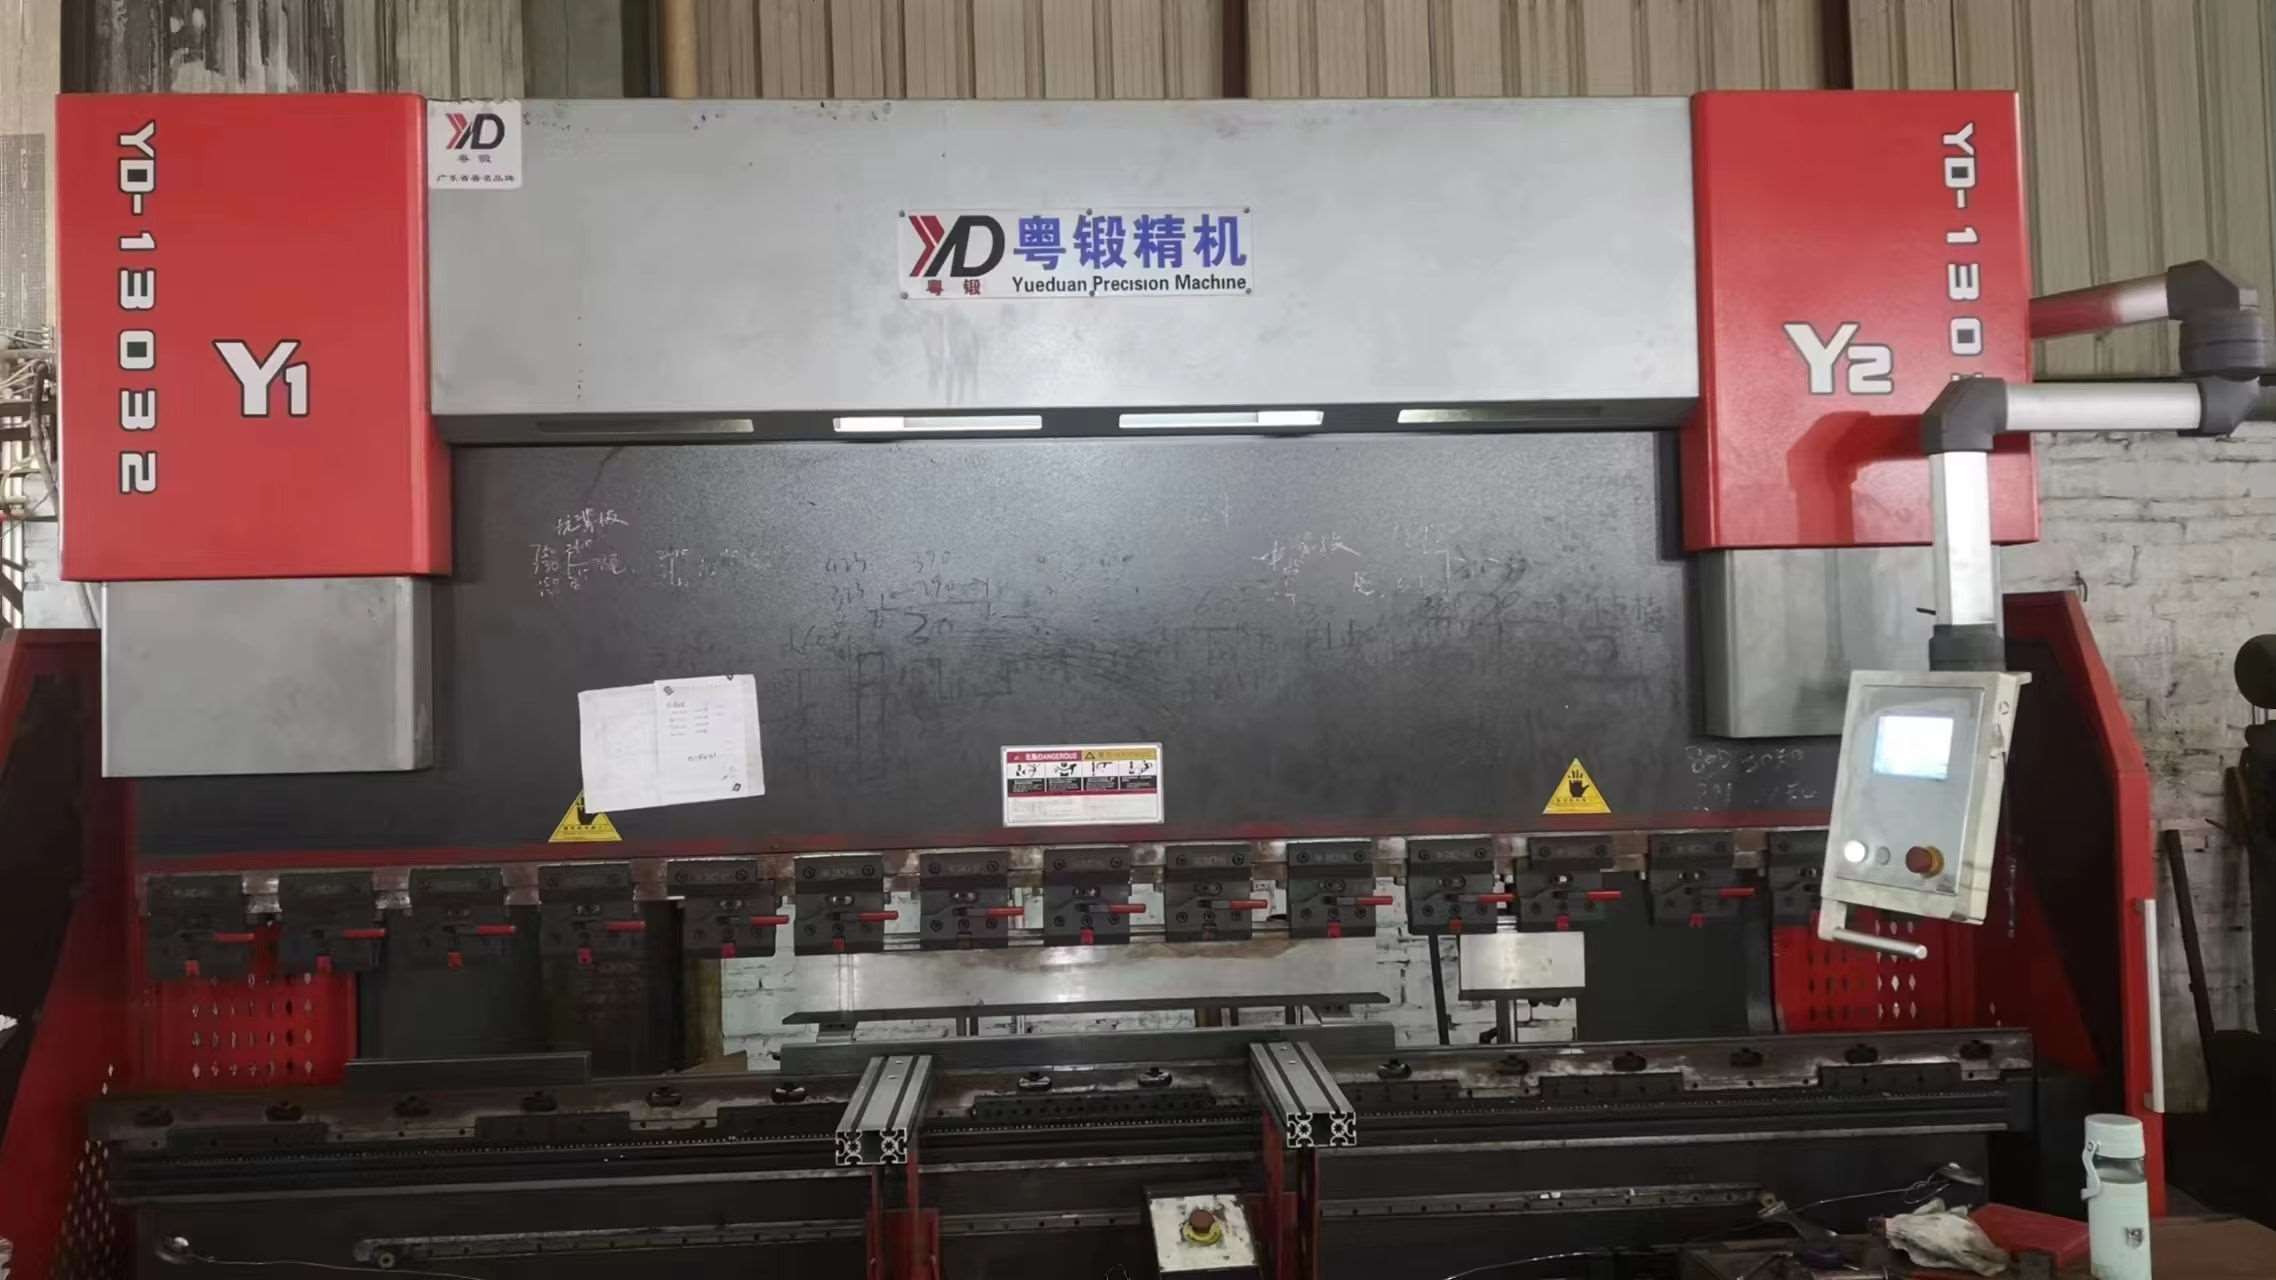
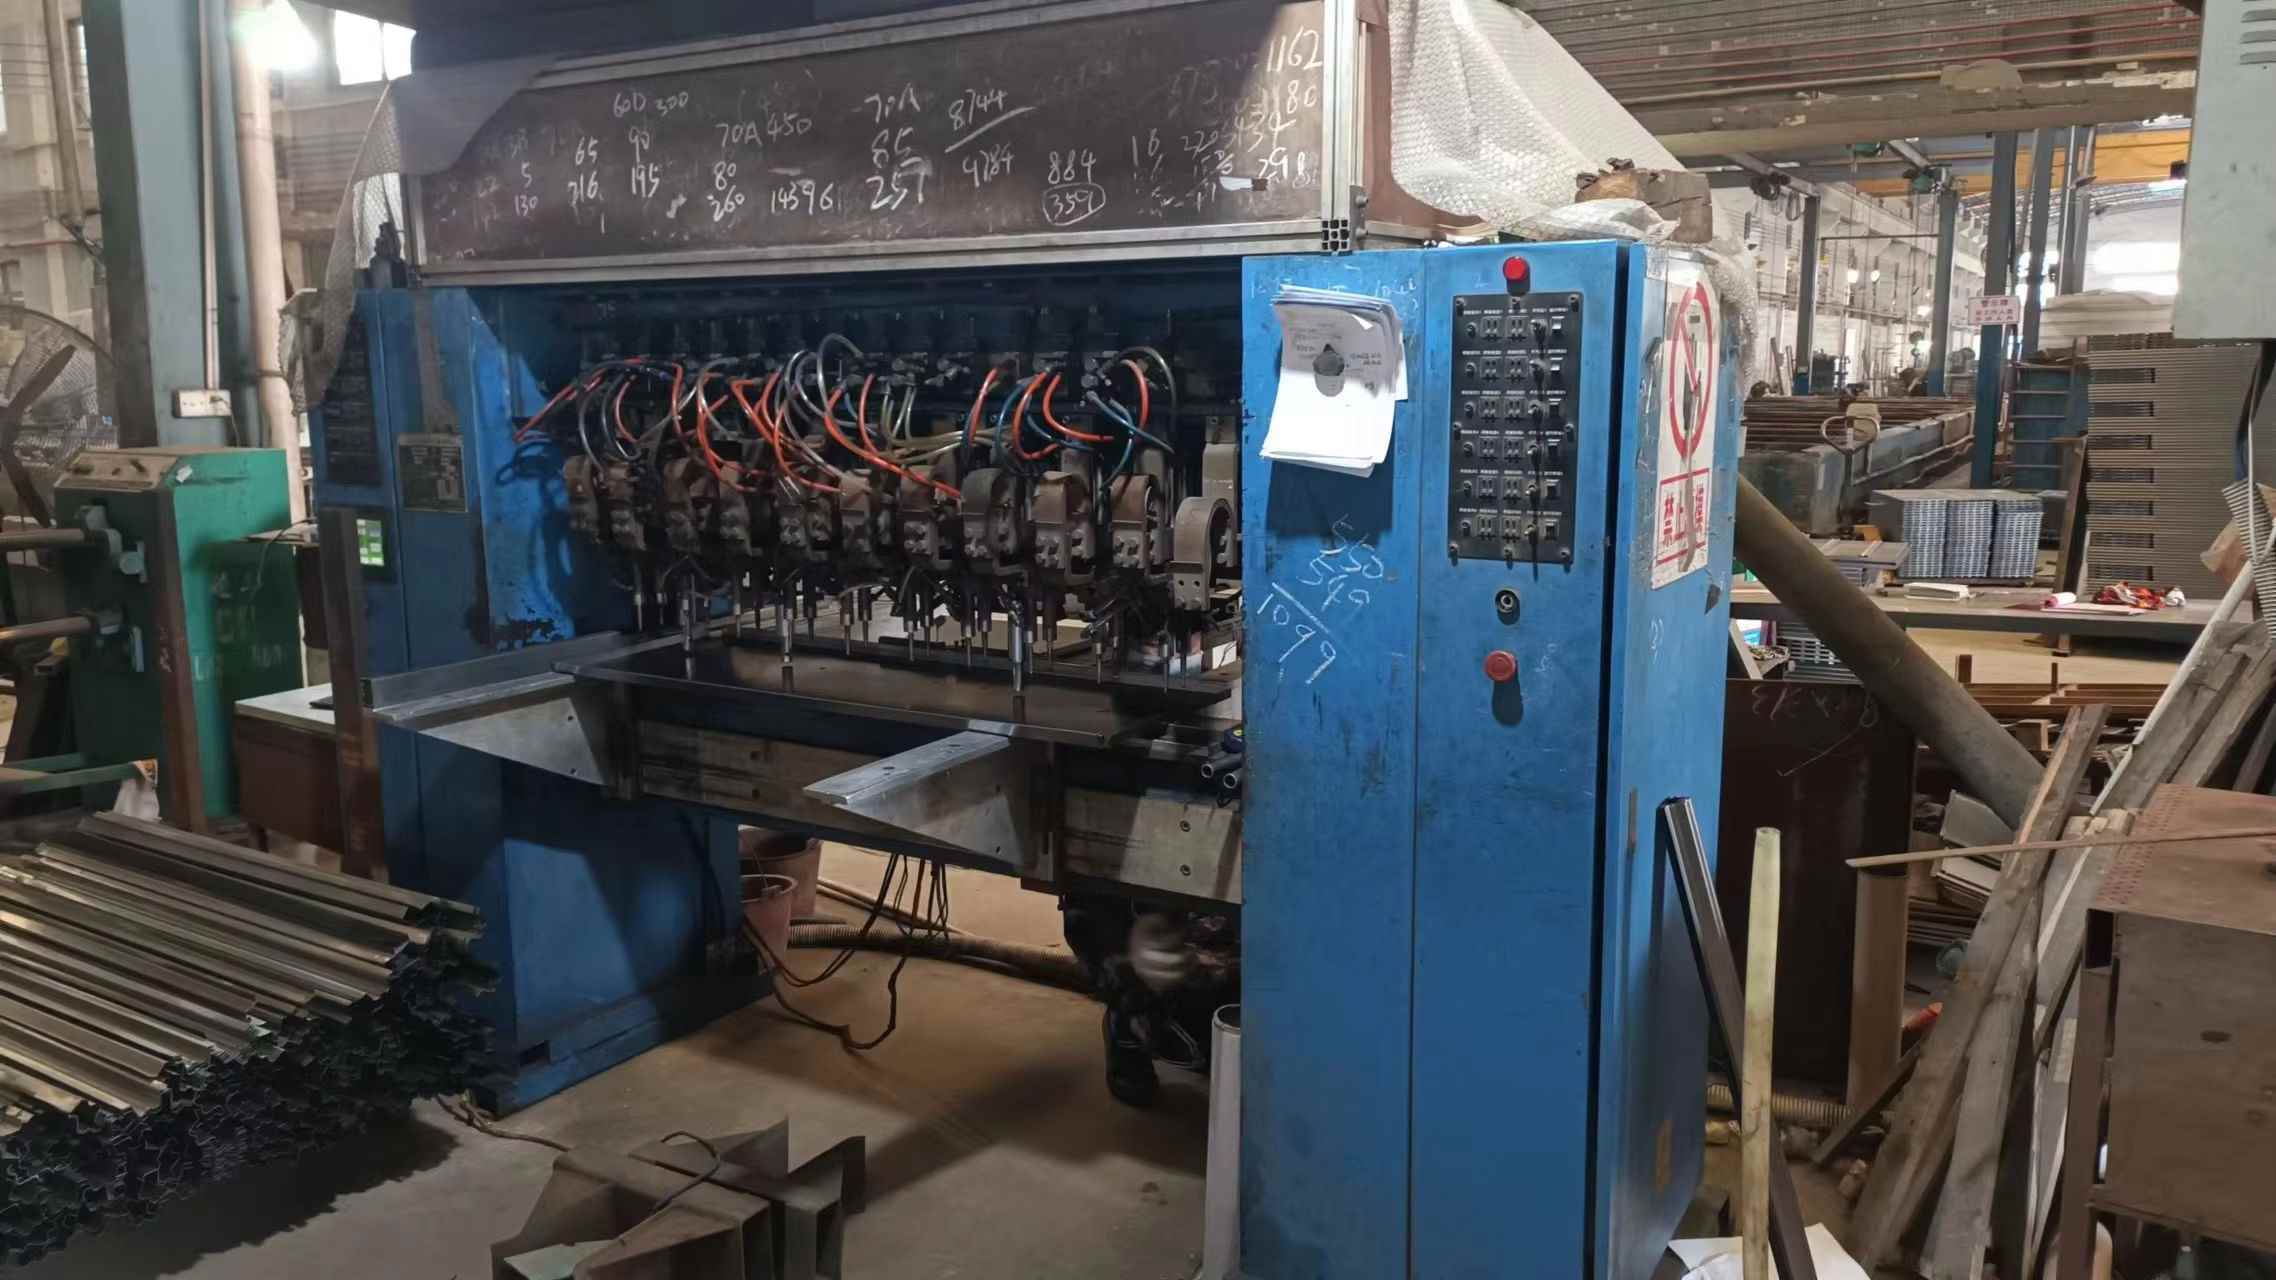
Our state-of-the-art production facility incorporates fully automated rolling mills, precise robotic welding cells, and eco-friendly powder coating lines to guarantee structural integrity and flawless finish.
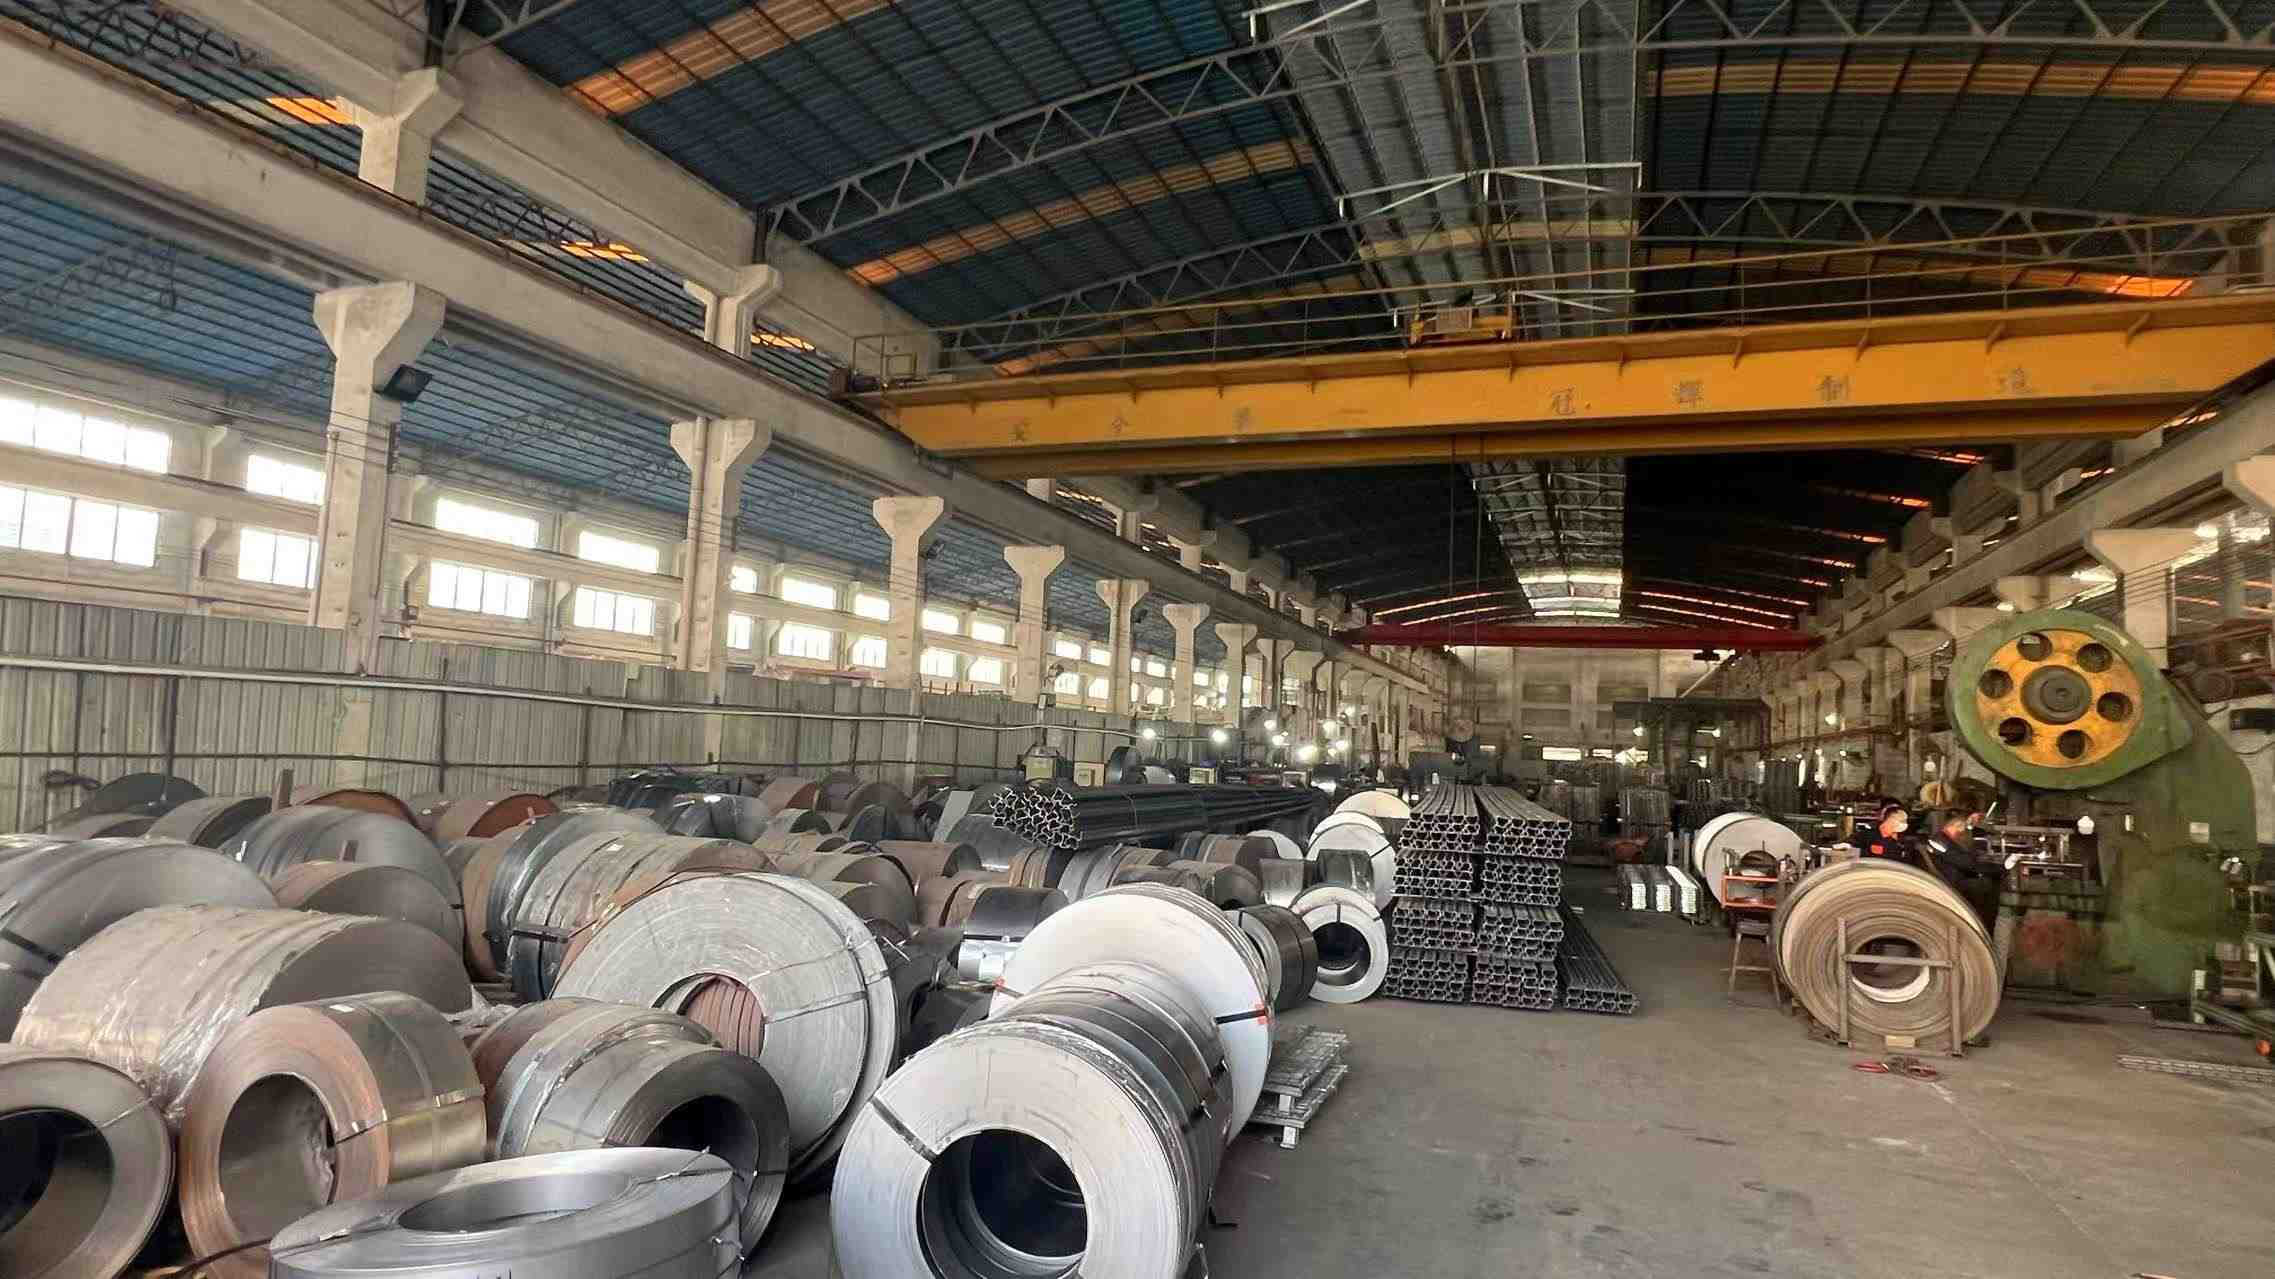
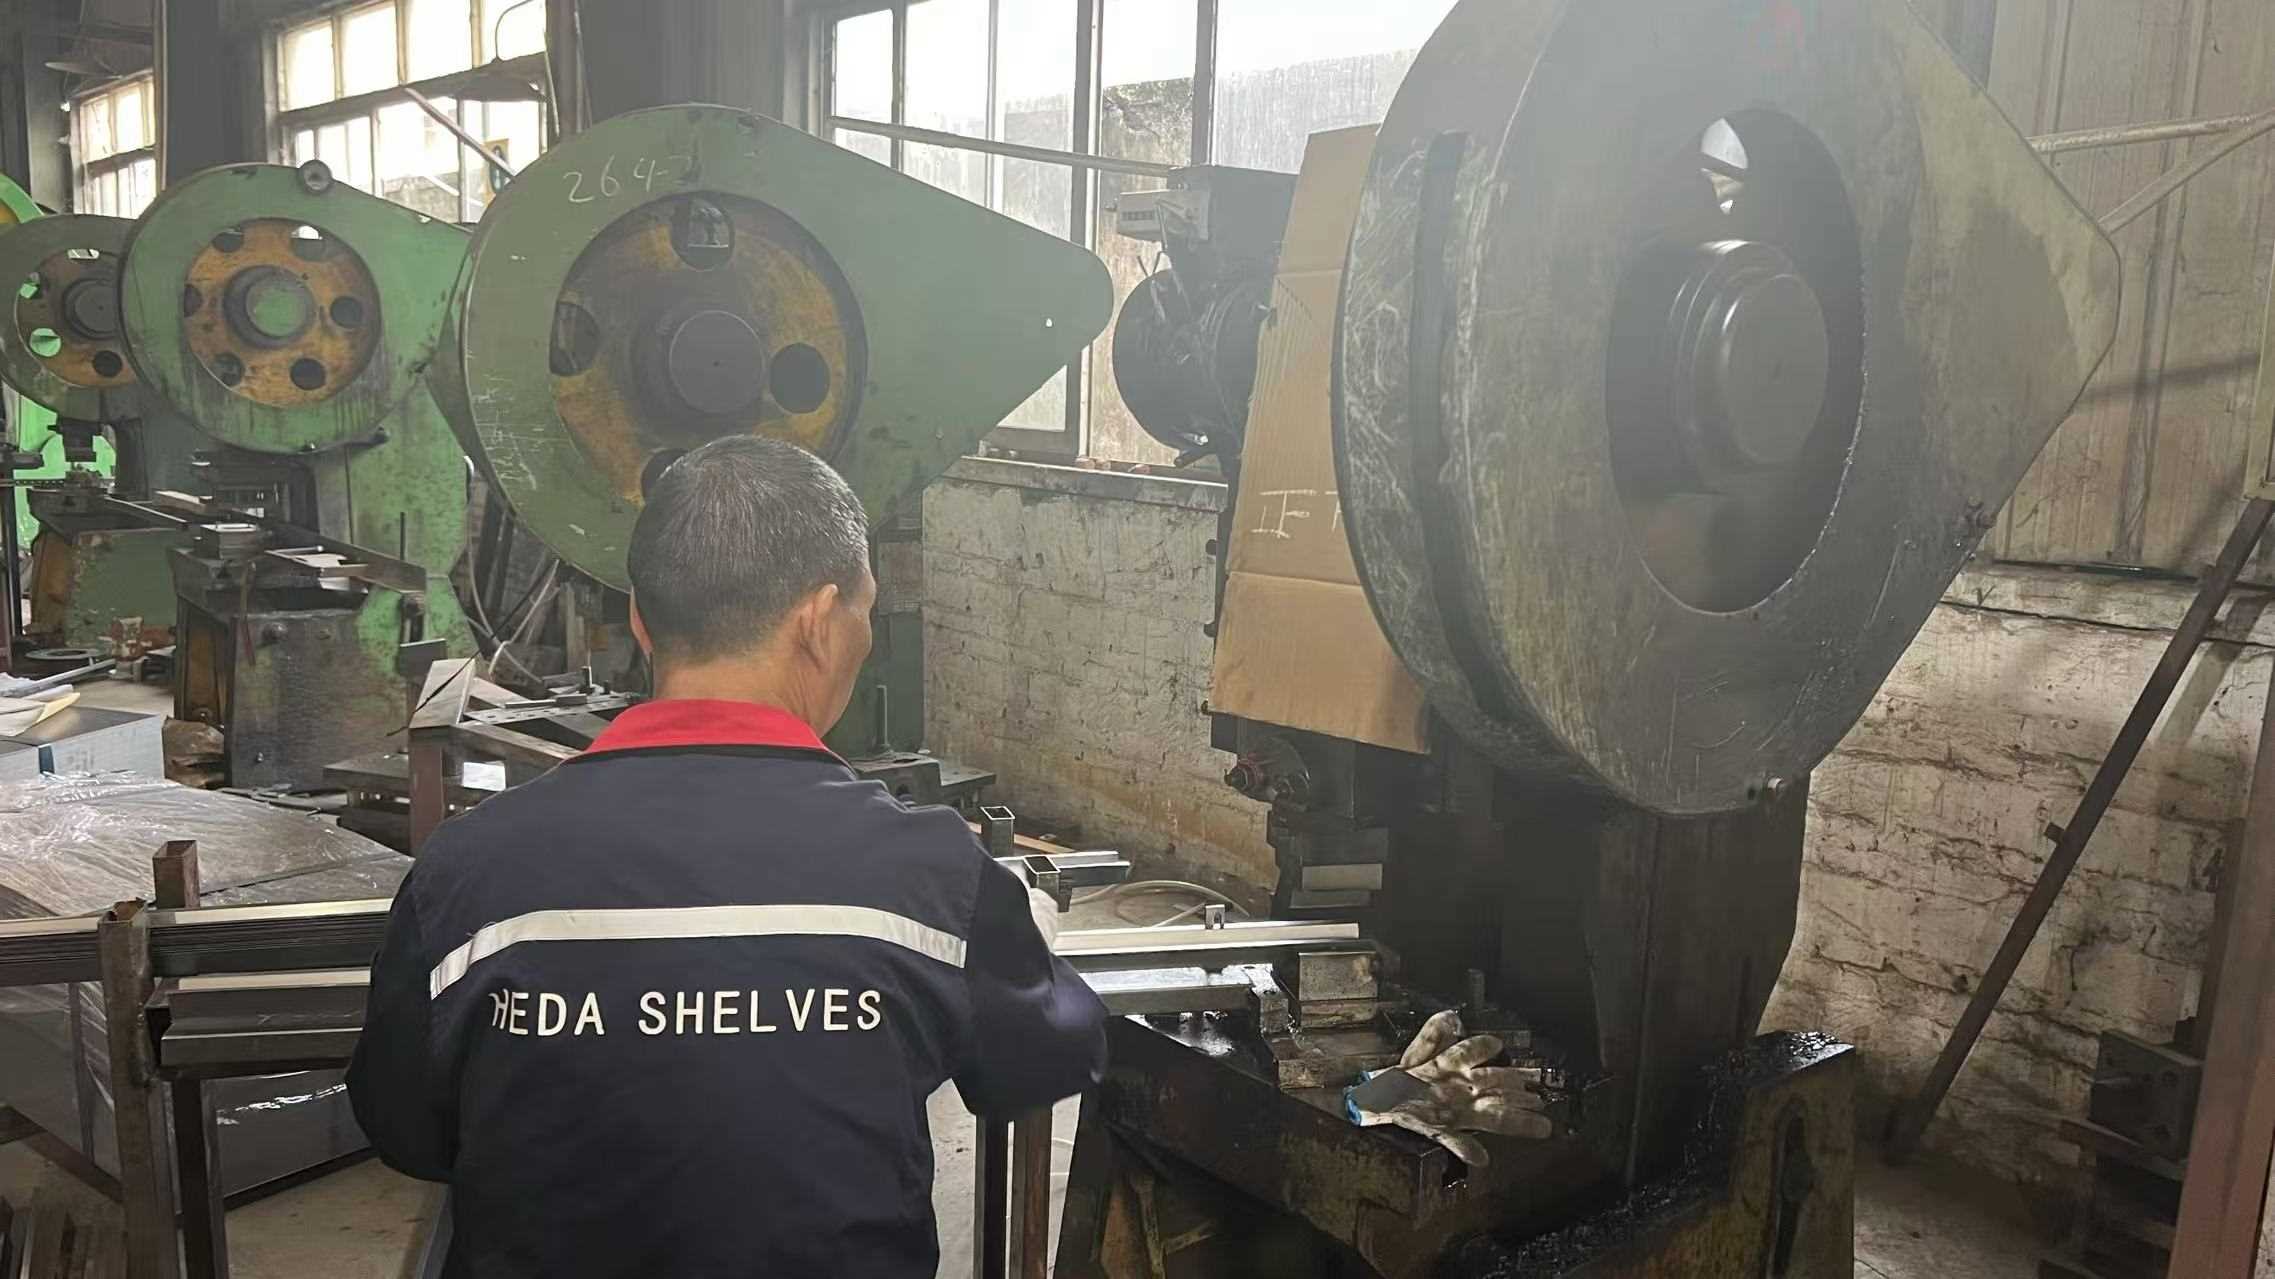
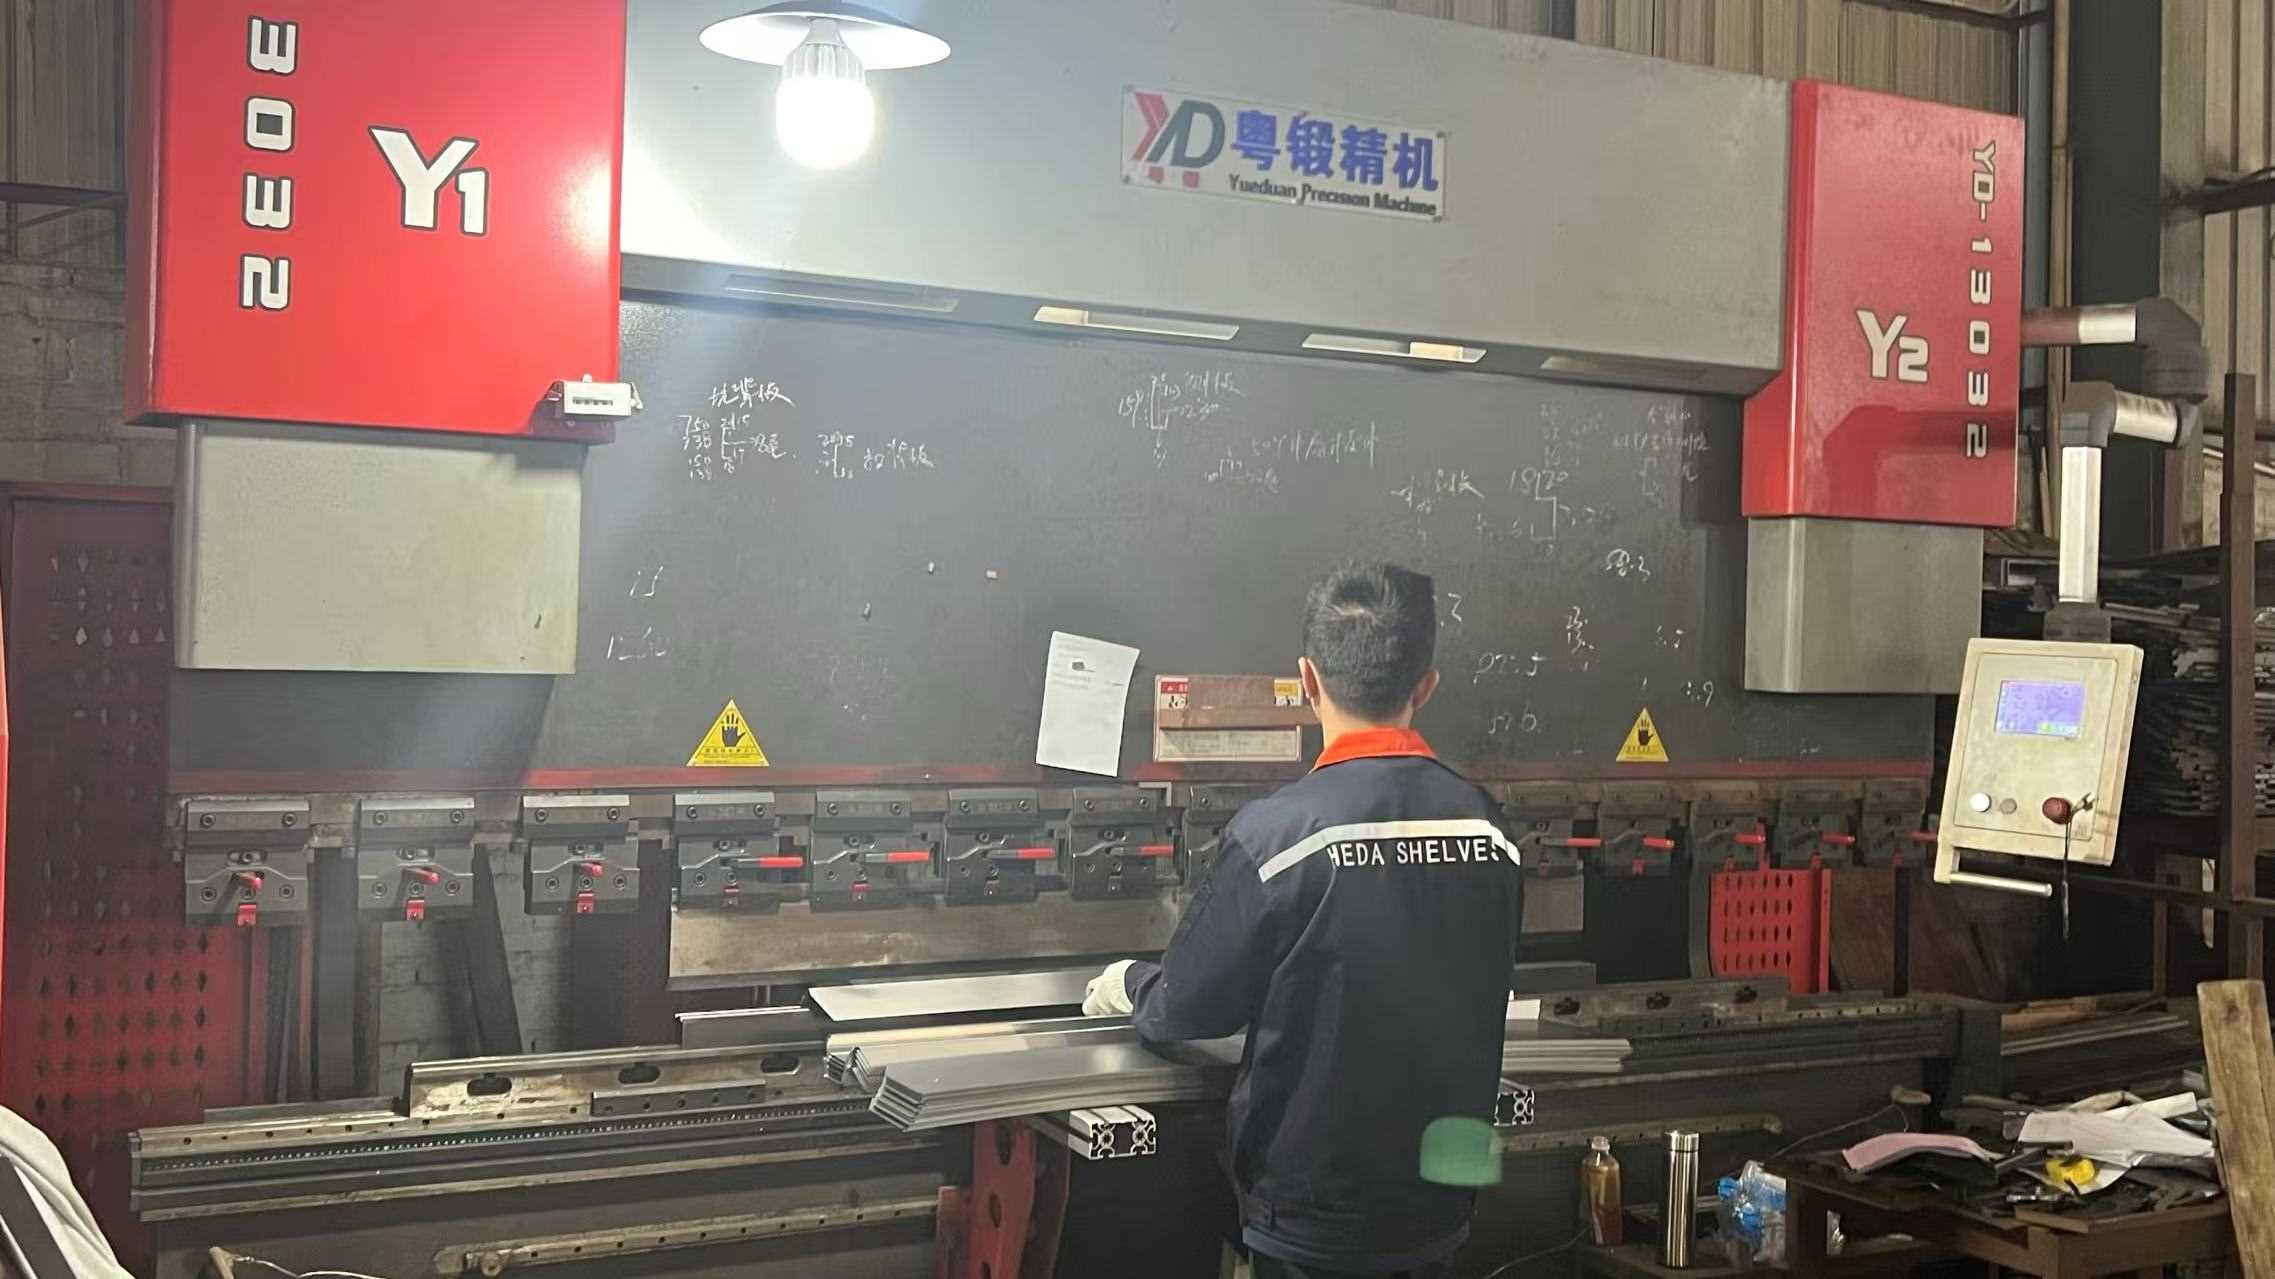
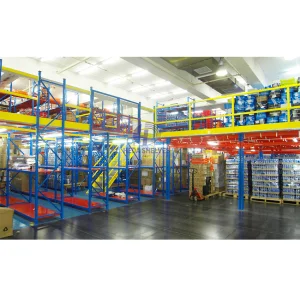
Explore our extended heavy-duty inventory, including high-capacity selective racks, multi-tier mezzanine floors, longspan shelving, and specialized cantilever storage structures.

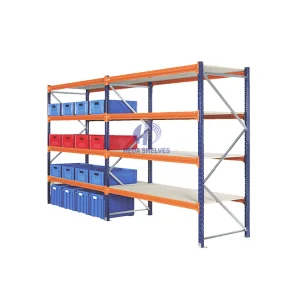
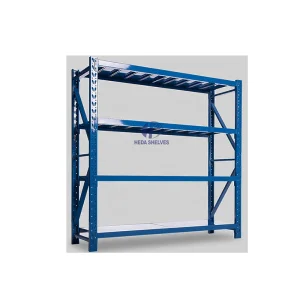
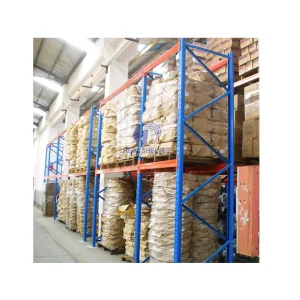
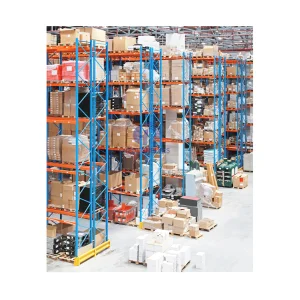
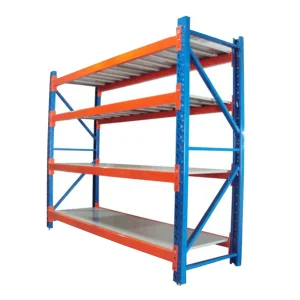
Navigating the complexities of worldwide supply chains requires highly adaptable, modular, and structurally certified warehouse storage solutions that adhere to international safety standards.
Modern third-party logistics operators demand rapid inventory turnover and ultra-high vertical space optimization. Our selective pallet racks and automated 4-way shuttle systems deliver unmatched pick efficiency and inventory control.
Industrial plants storing raw steel bars, heavy molds, and oversized components rely on our rugged cantilever systems and high-capacity structural steel racks capable of enduring extreme mechanical stress.
Temperature-controlled environments demand specialized anti-corrosion finishes and high-density deep-lane storage. Our cold storage shuttle systems maximize cubic capacity while minimizing energy consumption per pallet stored.
As smart warehousing, AI-driven inventory tracking, and autonomous robotics redefine industrial operations, Heda continues to spearhead technological advancements in modular storage engineering.
The convergence of Internet of Things (IoT) sensors with heavy-duty structural steel racking allows real-time load monitoring and structural health diagnostics. Our automated 4-way shuttle systems seamlessly interface with Warehouse Management Systems (WMS) to achieve lights-out inventory automation.
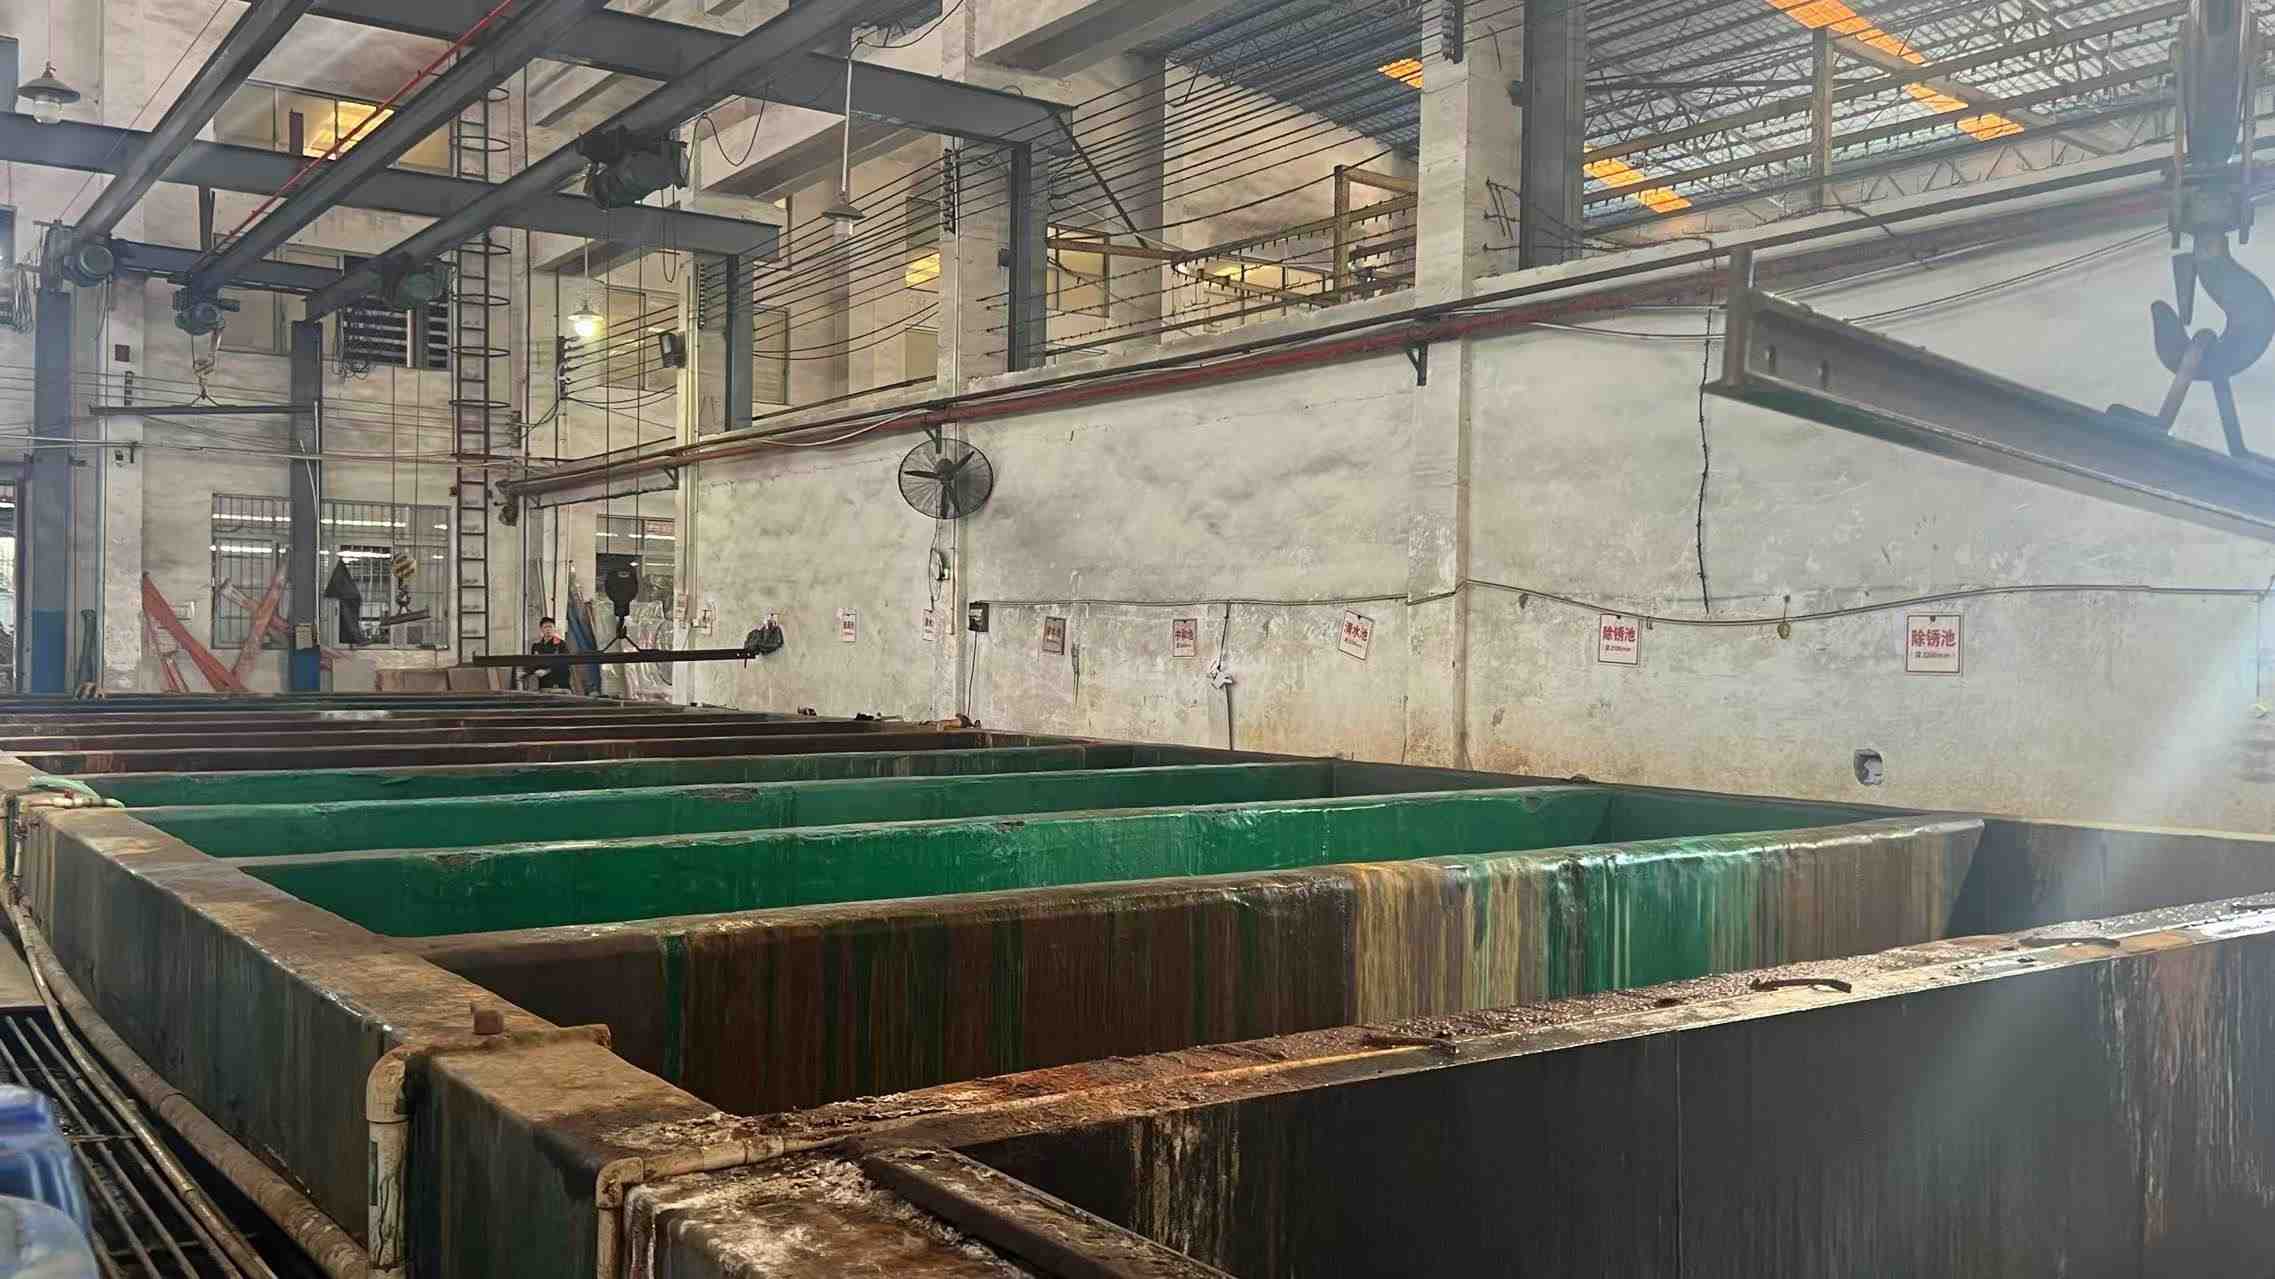
Committed to global carbon neutrality, our manufacturing facility utilizes energy-efficient rolling mills, closed-loop acid-washing water recycling systems, and solvent-free electrostatic powder coating lines, ensuring every exported rack meets strict international environmental benchmarks.
Exporting heavy industrial equipment across continents demands rigorous quality compliance, professional engineering documentation, and seamless logistical execution.
Our racking systems comply with RMI (Rack Manufacturers Institute) guidelines, FEM standards, and CE safety certifications, providing global buyers with absolute structural confidence.
Supported by 28 senior structural engineers, we deliver bespoke CAD layouts, load capacity calculations, and custom color coding tailored to specific warehouse blueprints.
With export experience spanning over 8 years, we offer secure container packaging, moisture-resistant bundling, and comprehensive customs clearance documentation for worry-free delivery.
Expert answers regarding our warehouse storage solutions, customization capabilities, and global export procedures.
 Hedaracking