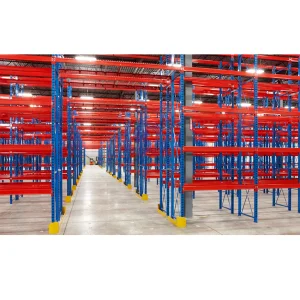
Established in 2014, Shenzhen Heda Warehouse Equipment Co., Ltd. is a premier manufacturer specializing in heavy-duty warehouse racking and industrial storage solutions. Spanning a modern manufacturing facility of 35,000 m², our enterprise integrates R&D, design, production, and international marketing to serve diverse storage needs worldwide. With 12 years of industry experience and 8 years of dedicated export expertise, we deliver high-caliber storage systems that generate over $28 million in annual export revenue.
At Heda, quality control and engineering innovation drive our core operations. Our robust QC department comprises 45 skilled inspectors utilizing rigorous testing methods, including raw material tensile testing, automated weld flaw detection, layer load-bearing stress analysis, and salt spray surface corrosion testing. Supported by a professional R&D team of 28 senior structural engineers, we maintain strong full-customization capabilities (OEM/ODM)—offering tailored rack dimensions, load capacities, surface coatings, and layout designs. Driven by continuous innovation, we launched over 120 new dynamic storage products and component upgrades last year.
Operating with a strong direct-factory and international trade background, we have built a resilient ecosystem supported by over 800 supply chain partners. Our products are exported to major global markets, including North America, Western Europe, Southeast Asia, and the Middle East. We proudly serve a diverse clientele ranging from third-party logistics (3PL) providers and large distribution centers to industrial manufacturers and wholesale equipment distributors.
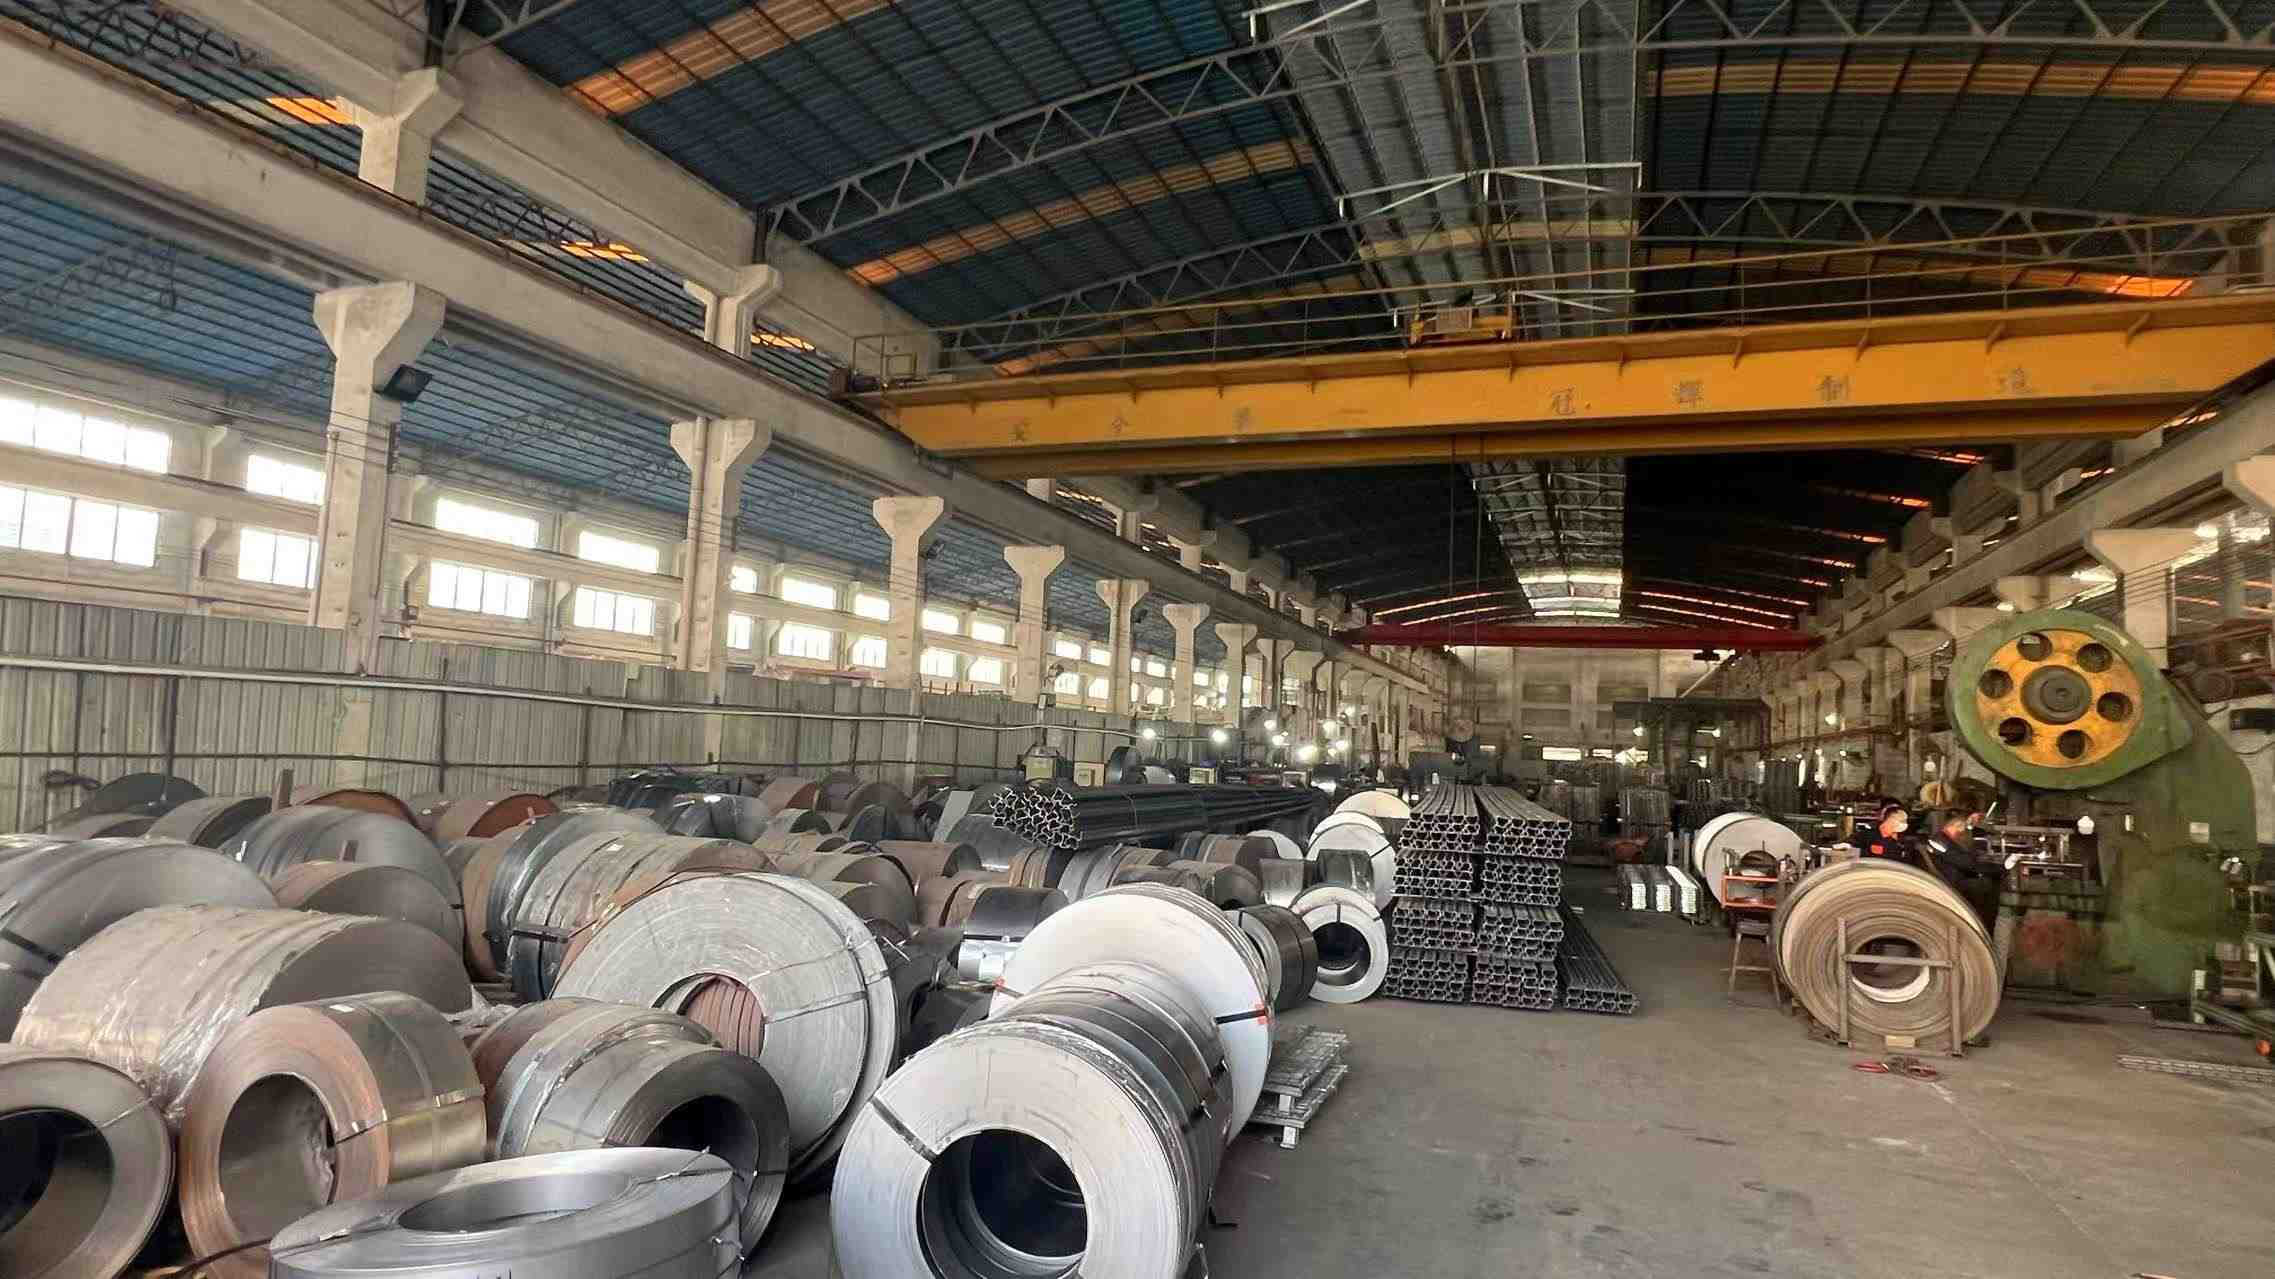
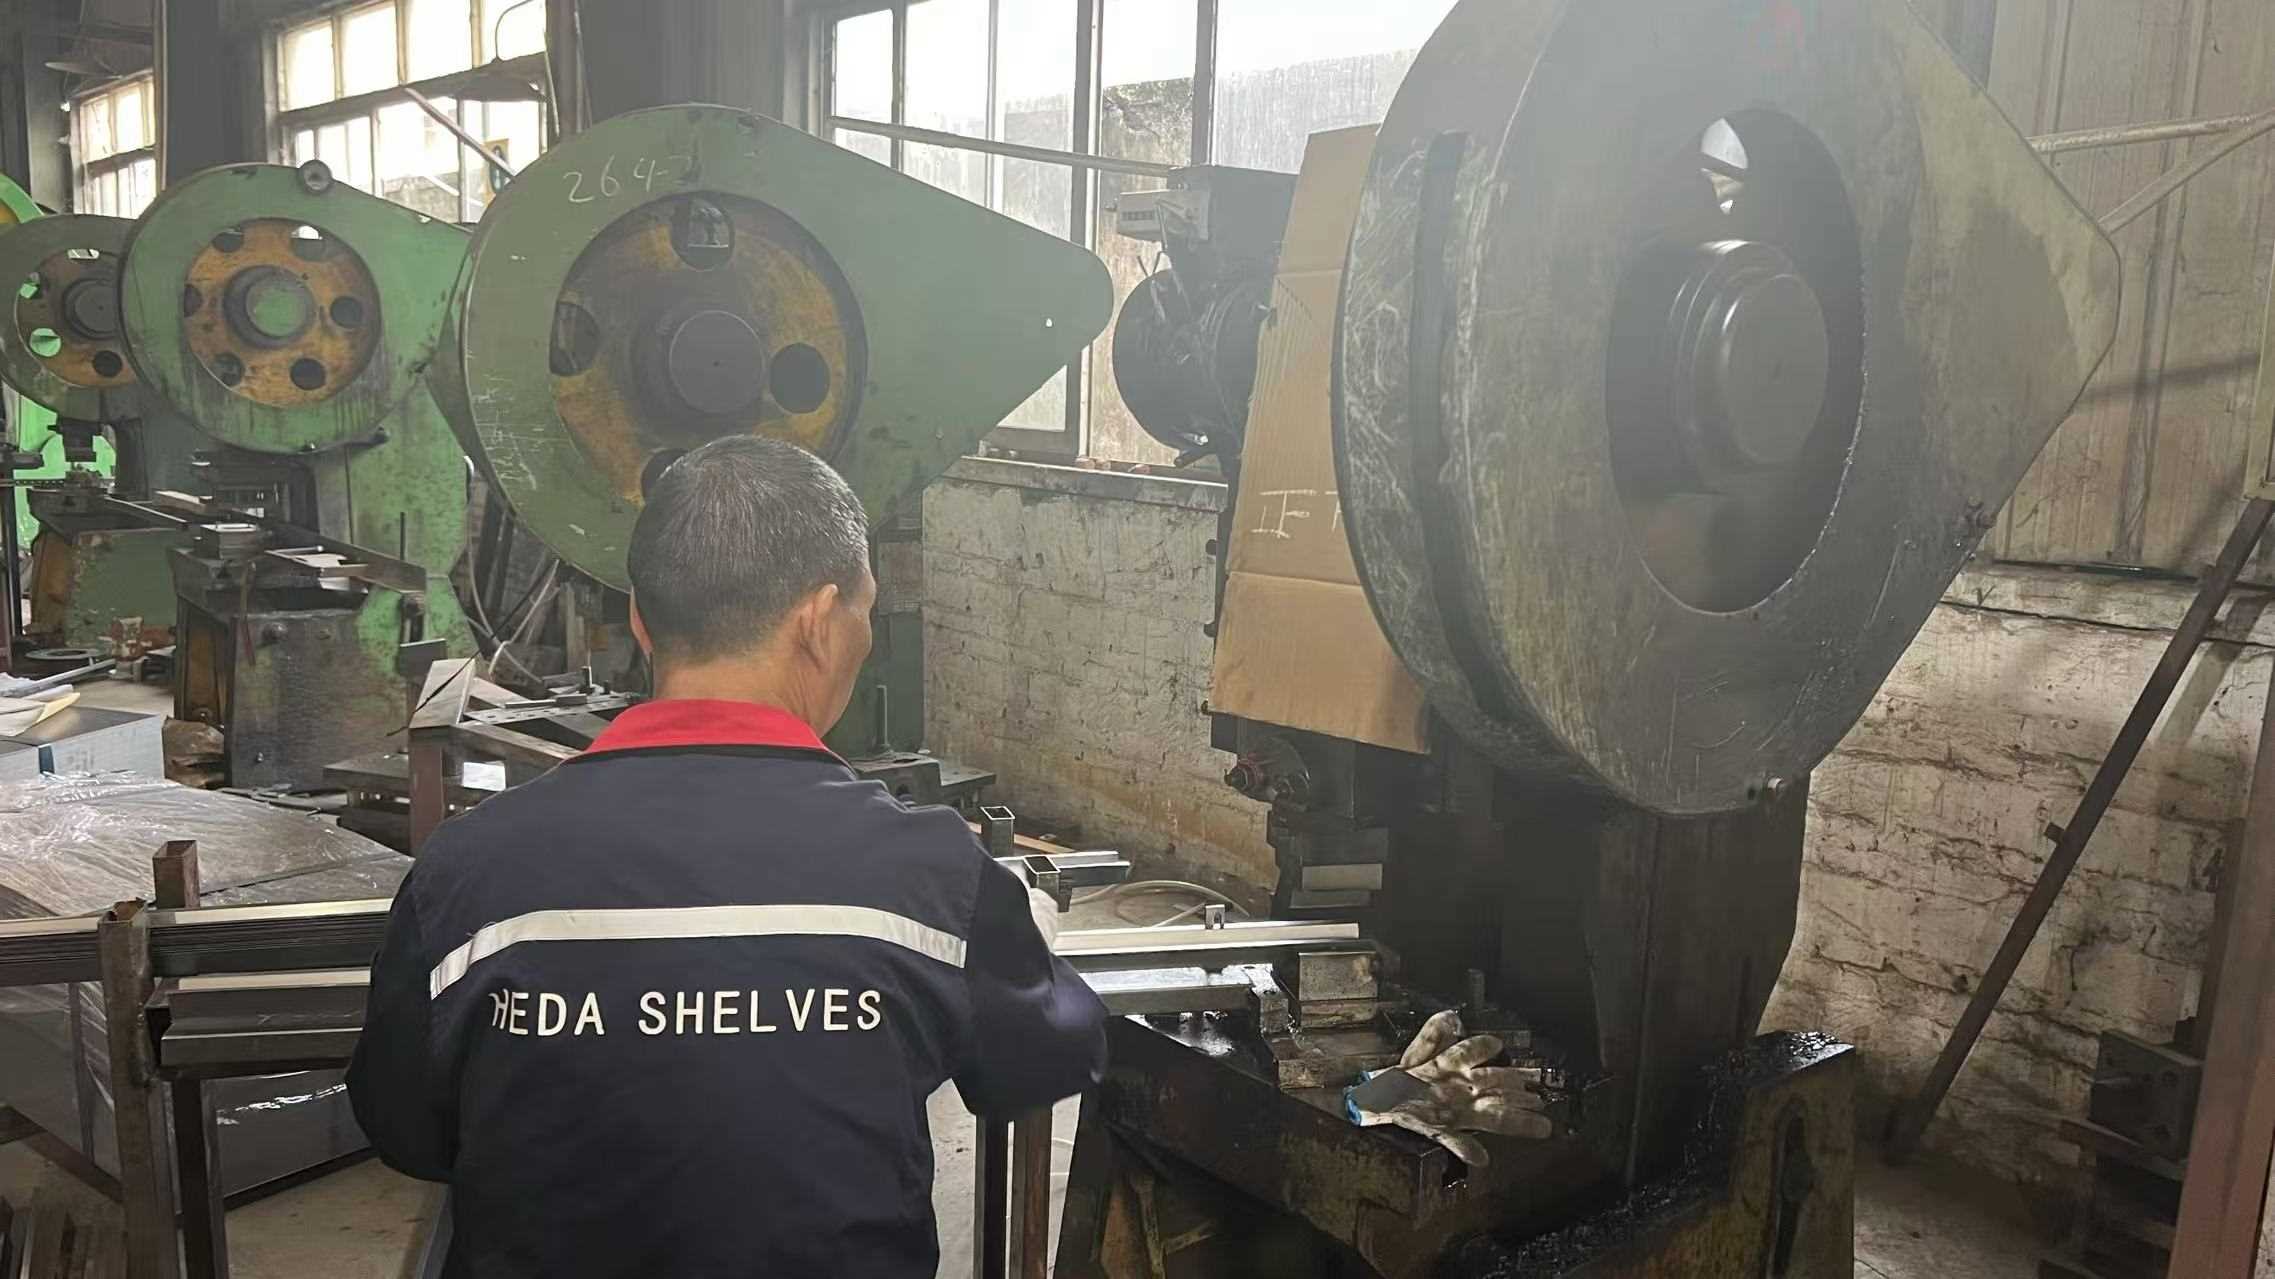
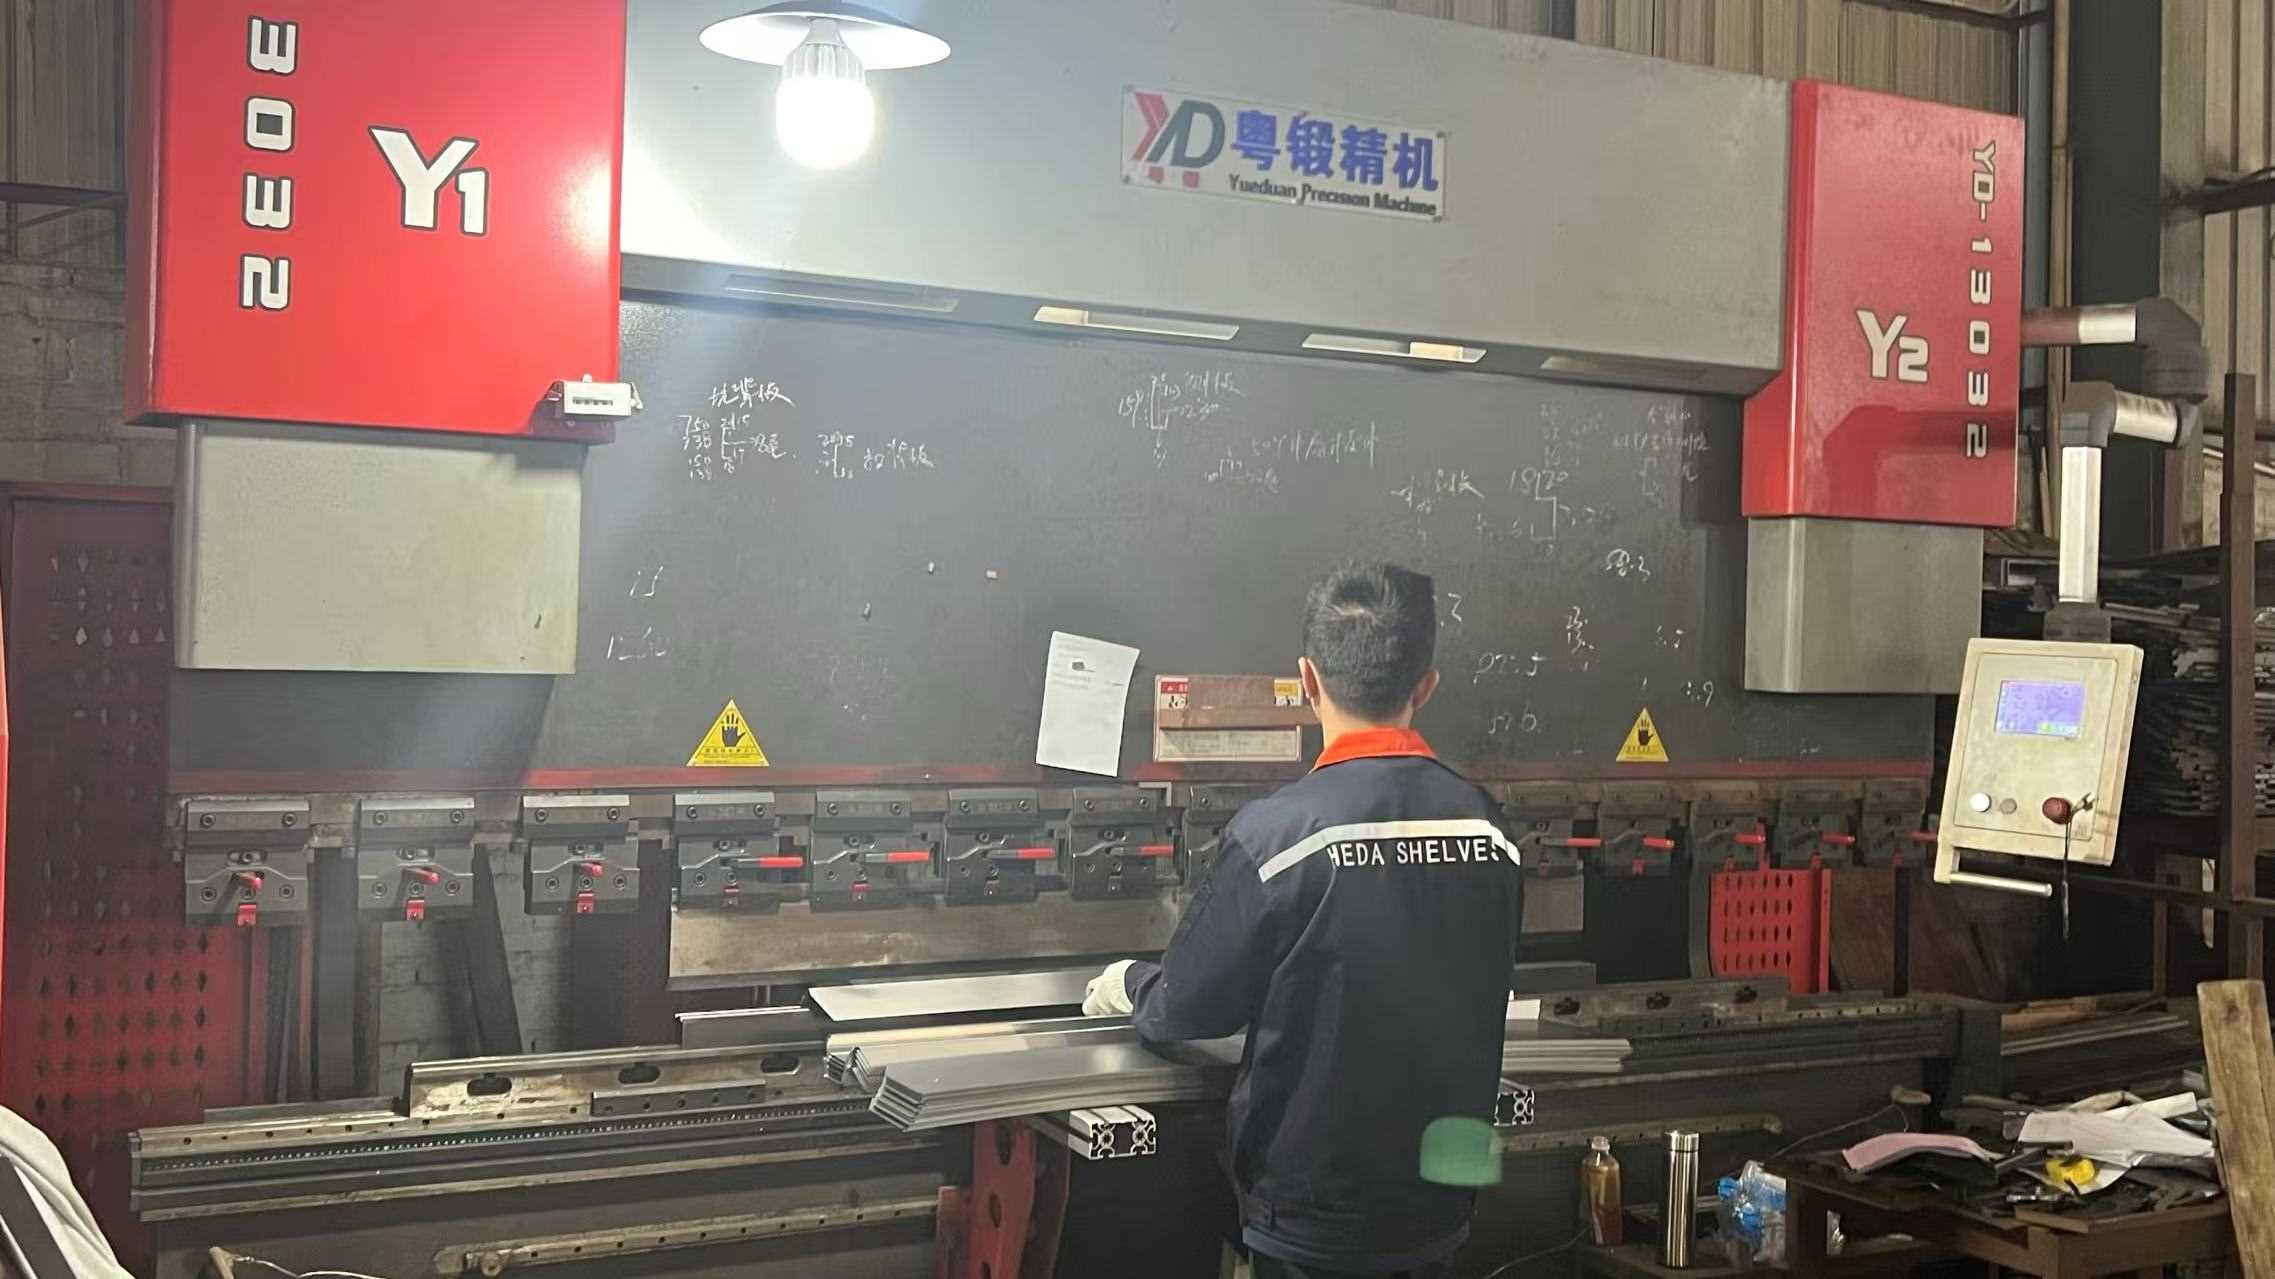
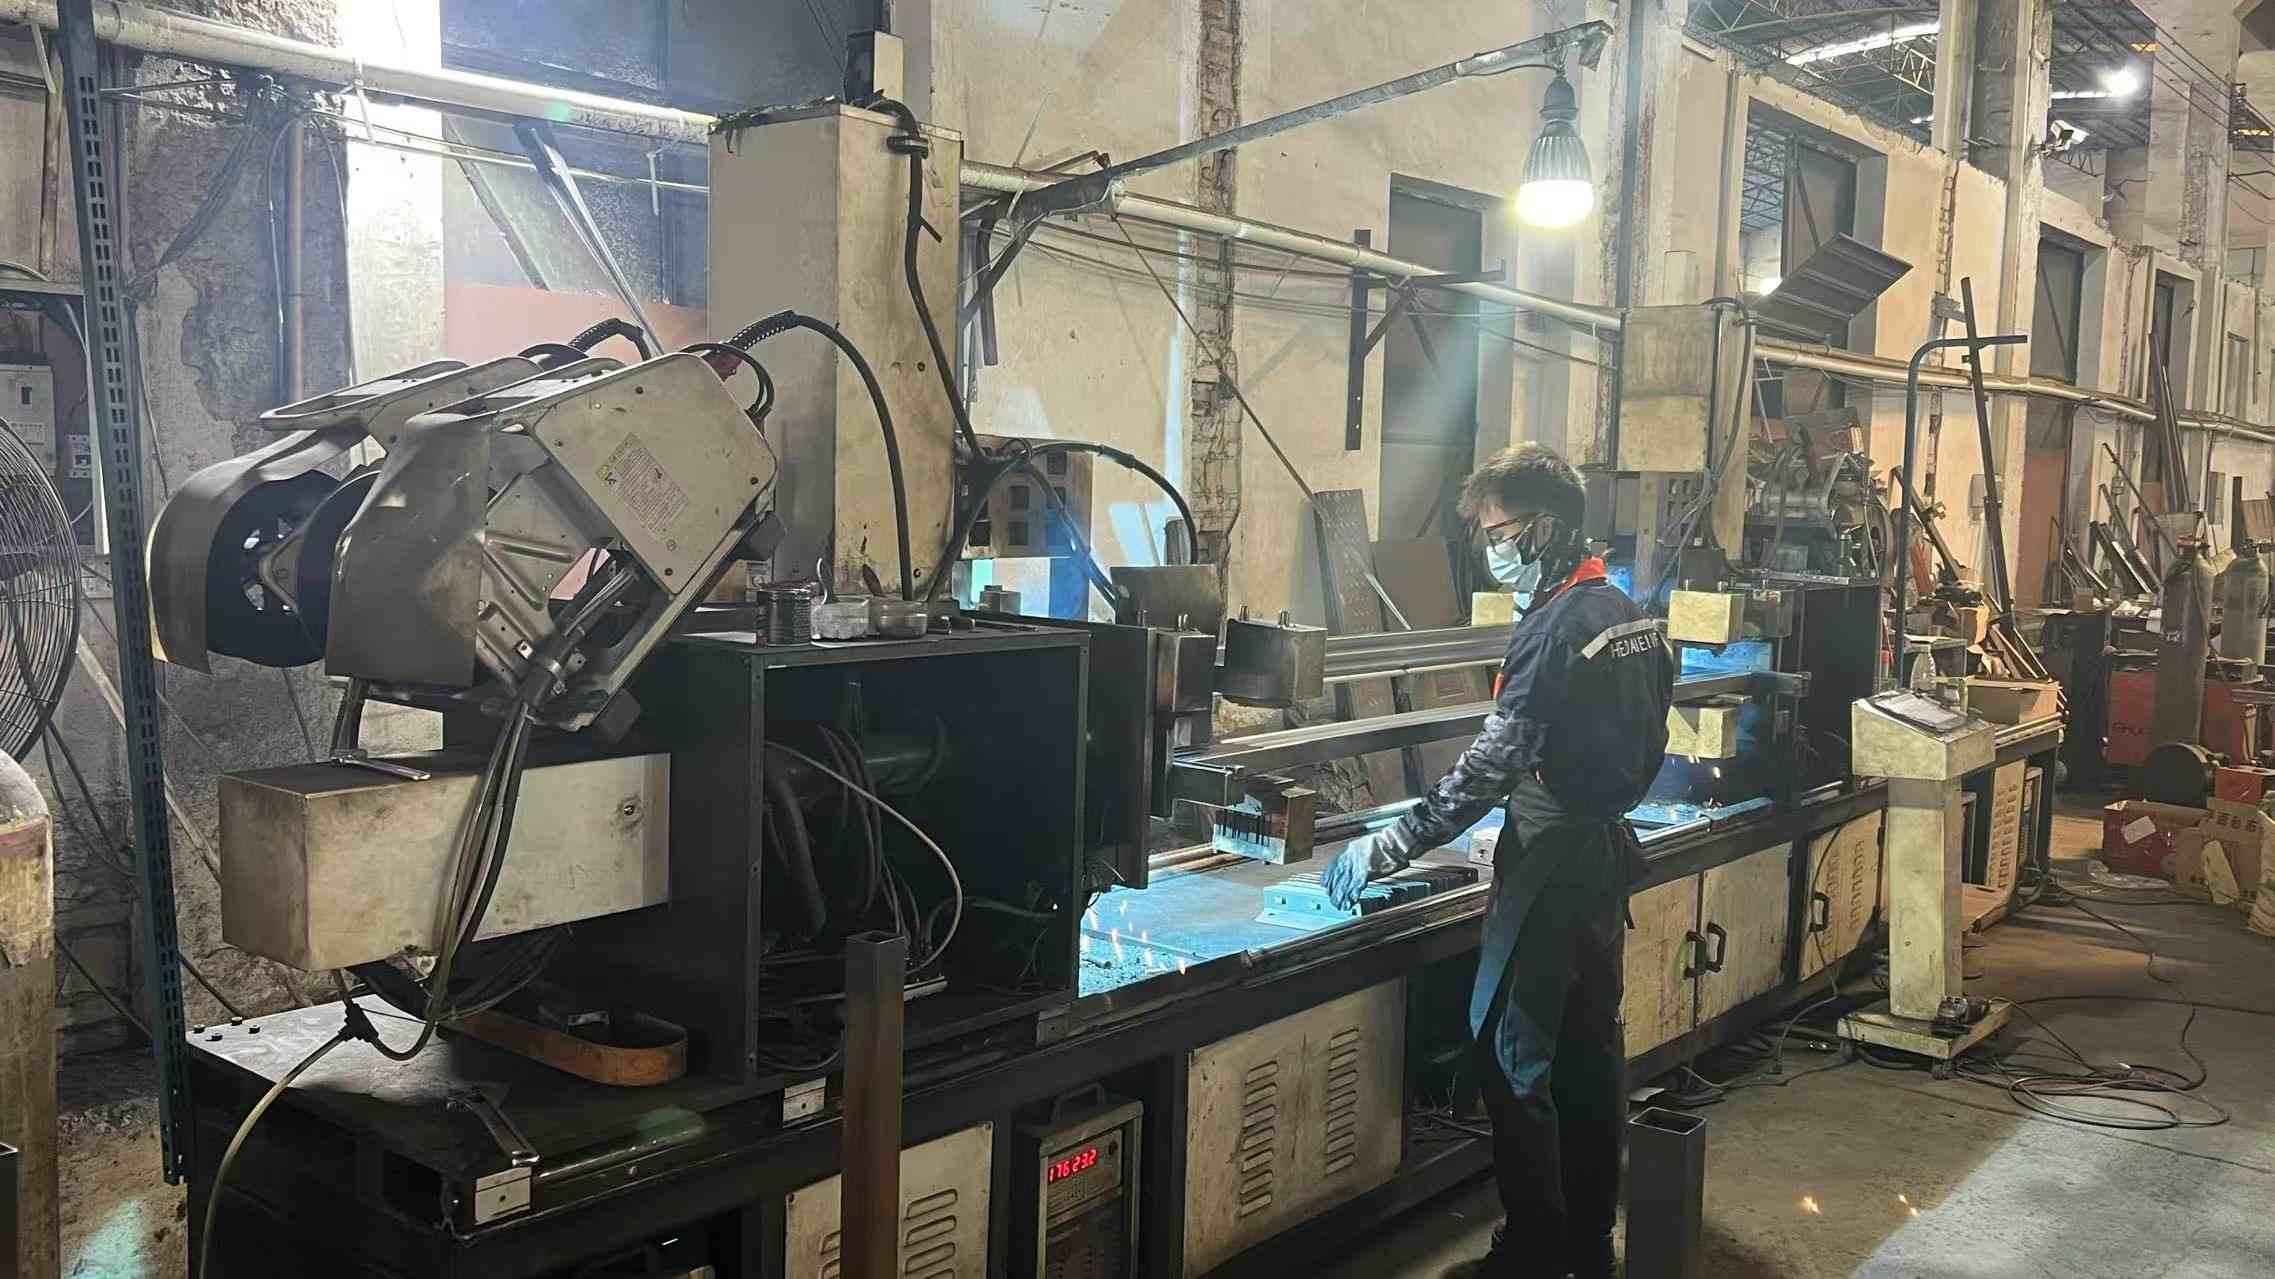
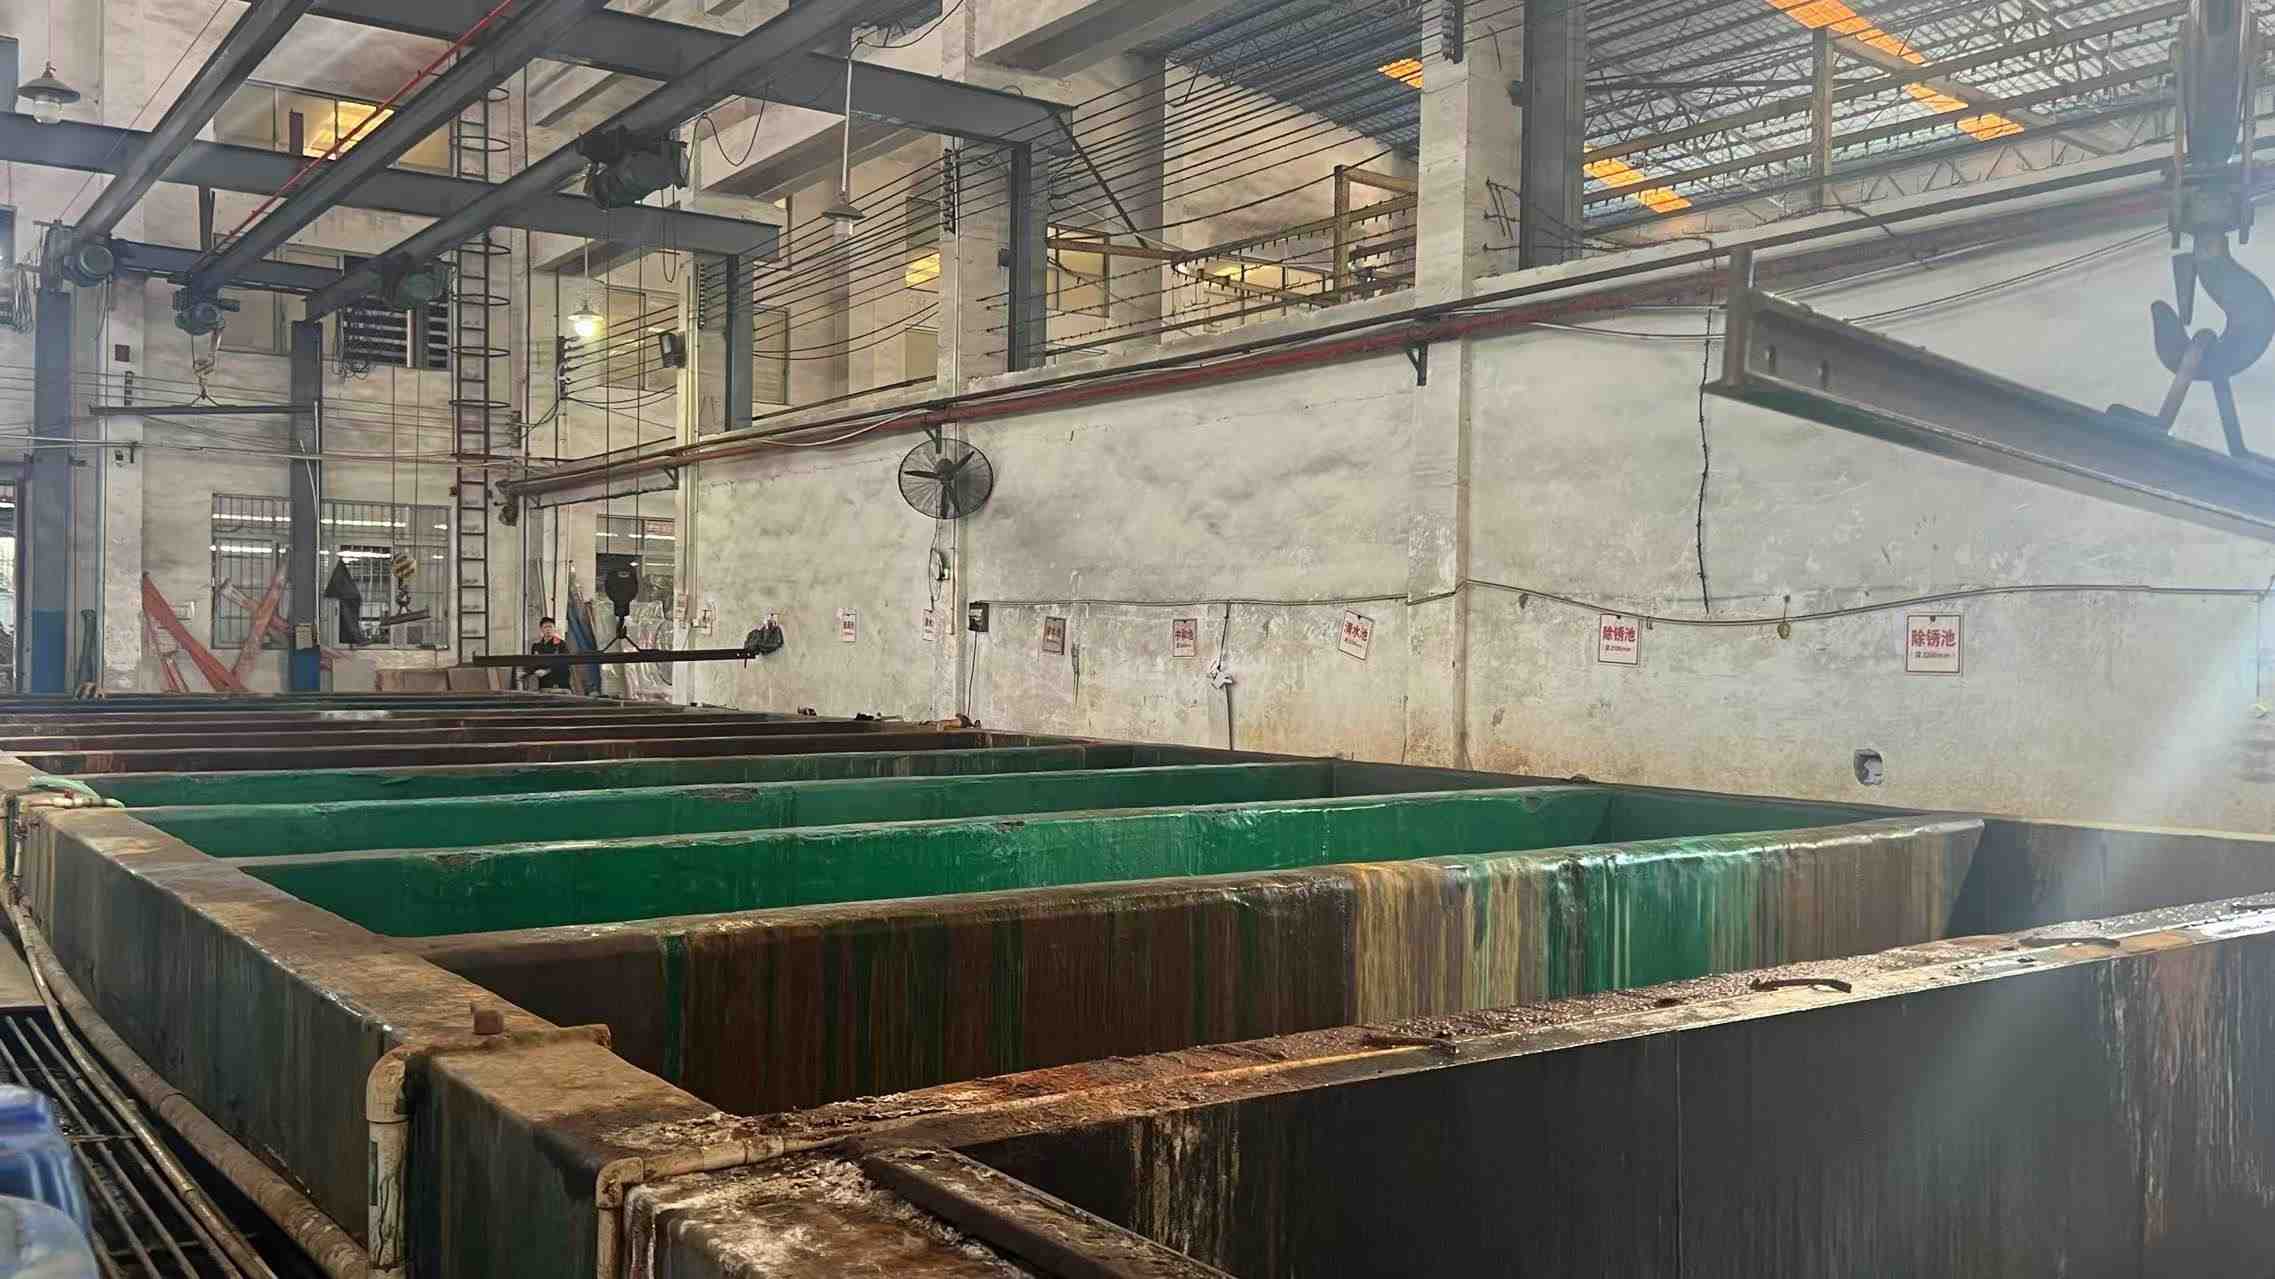
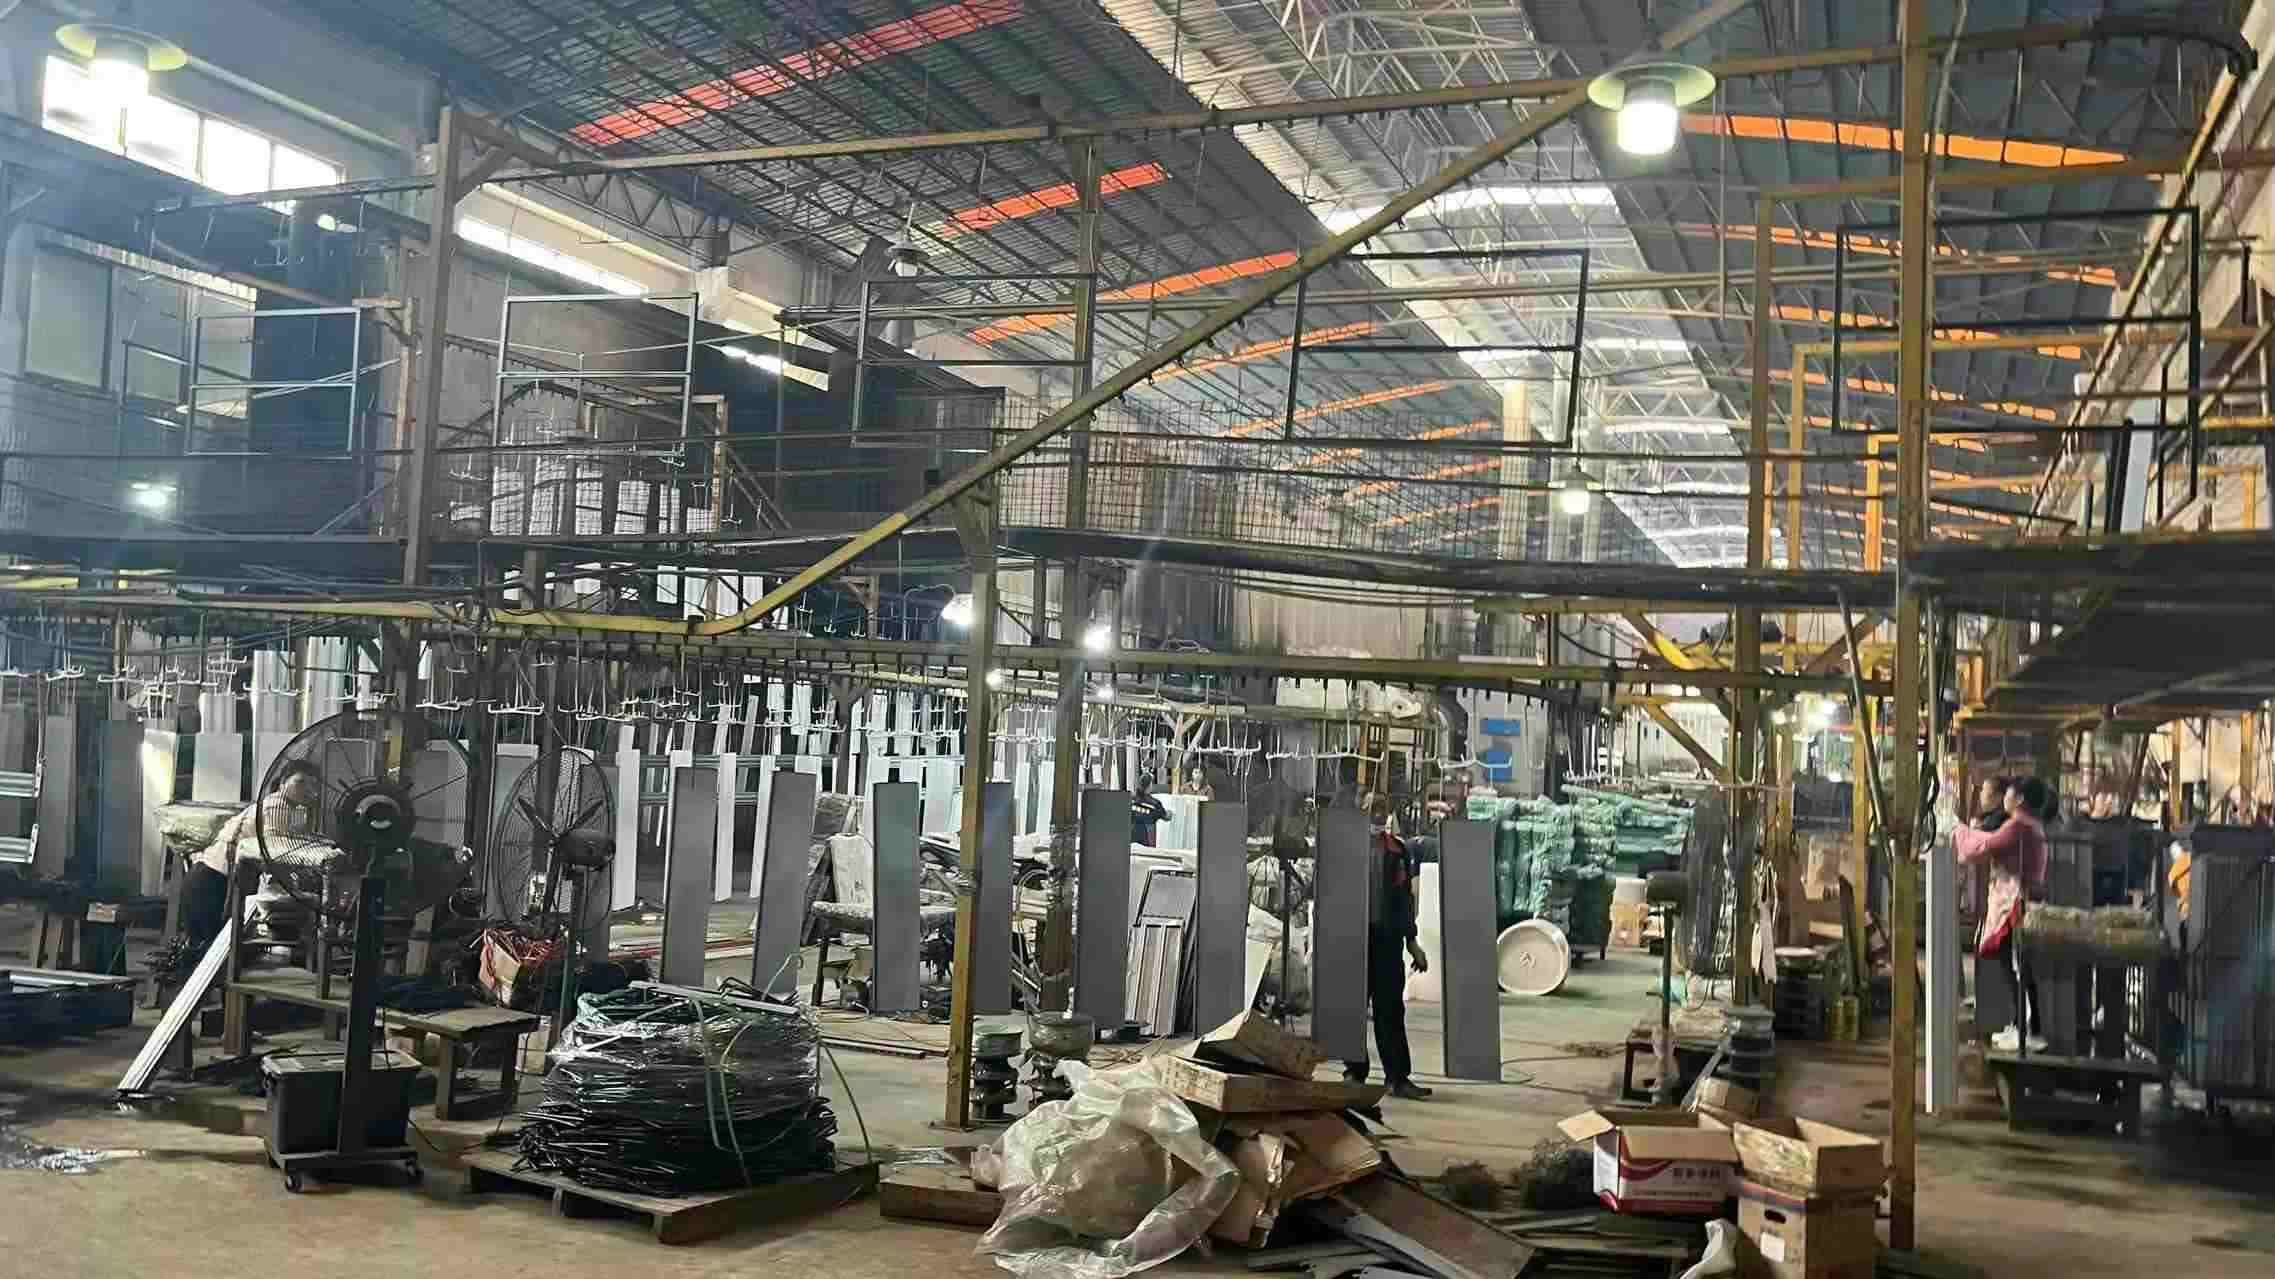
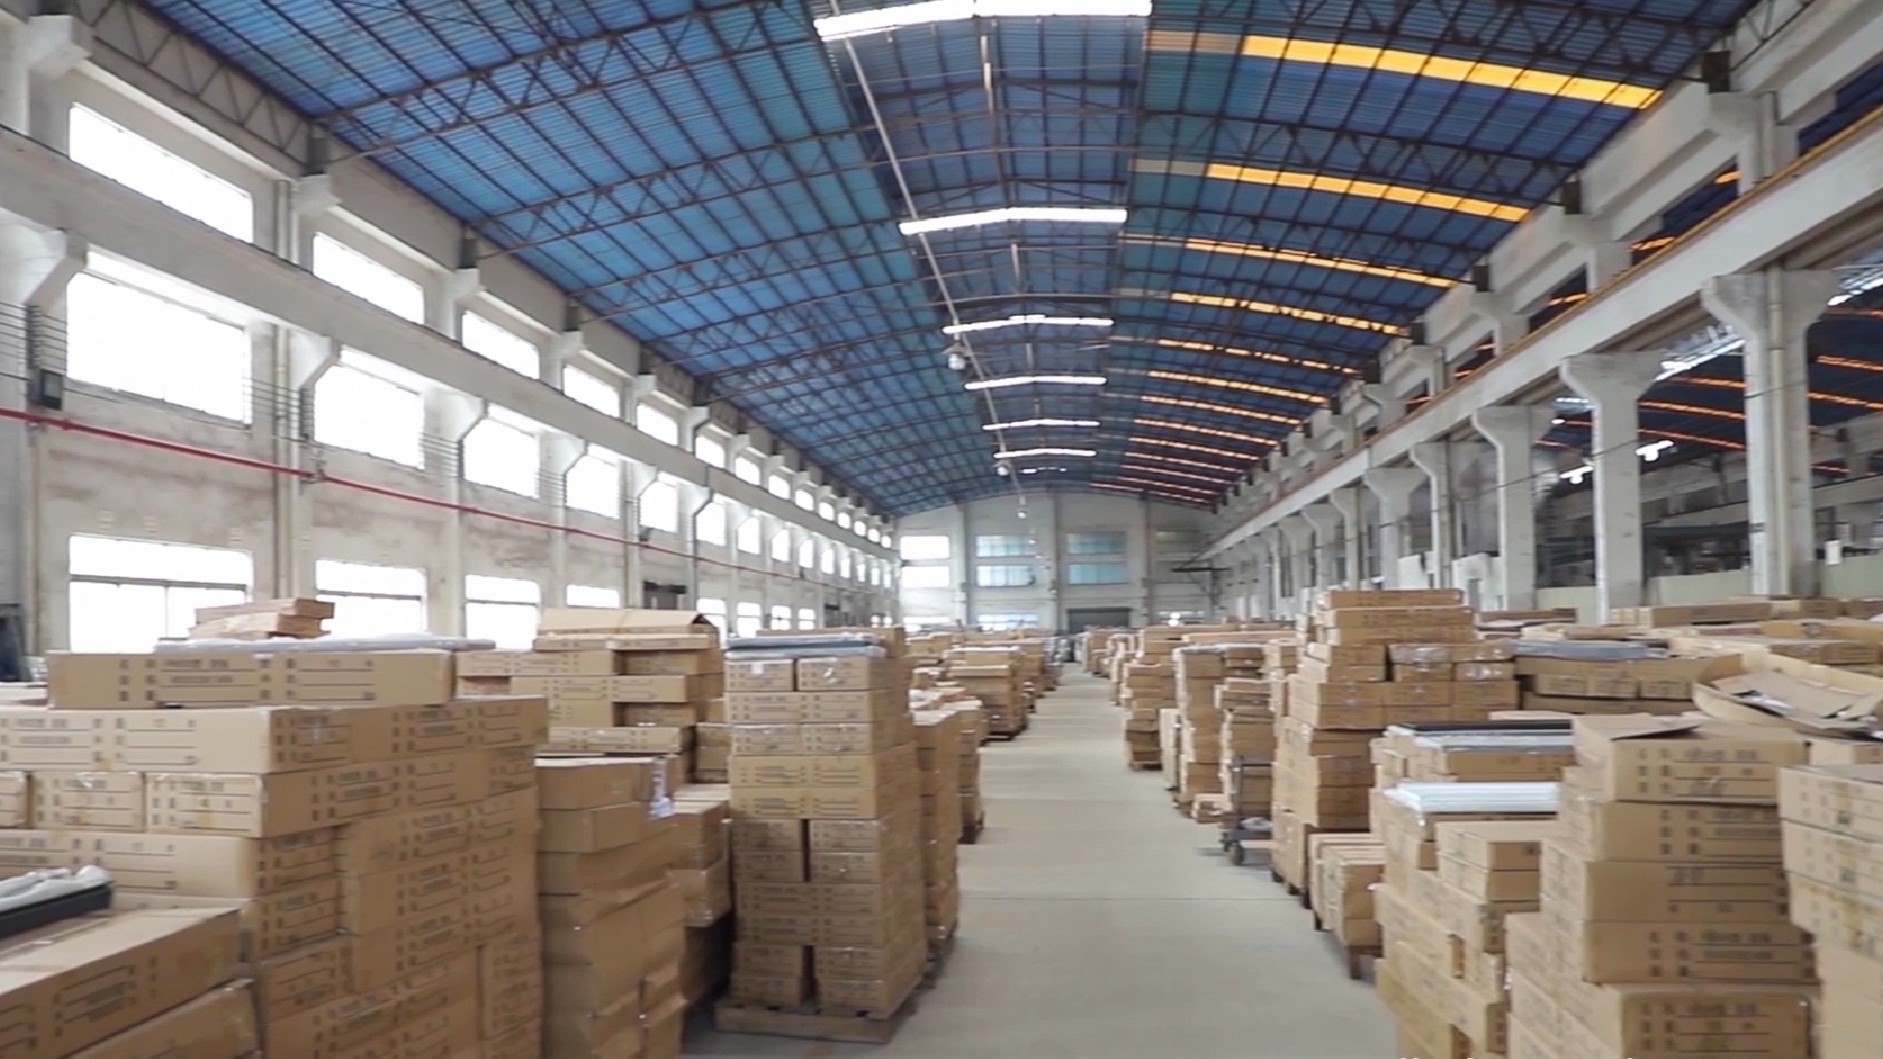
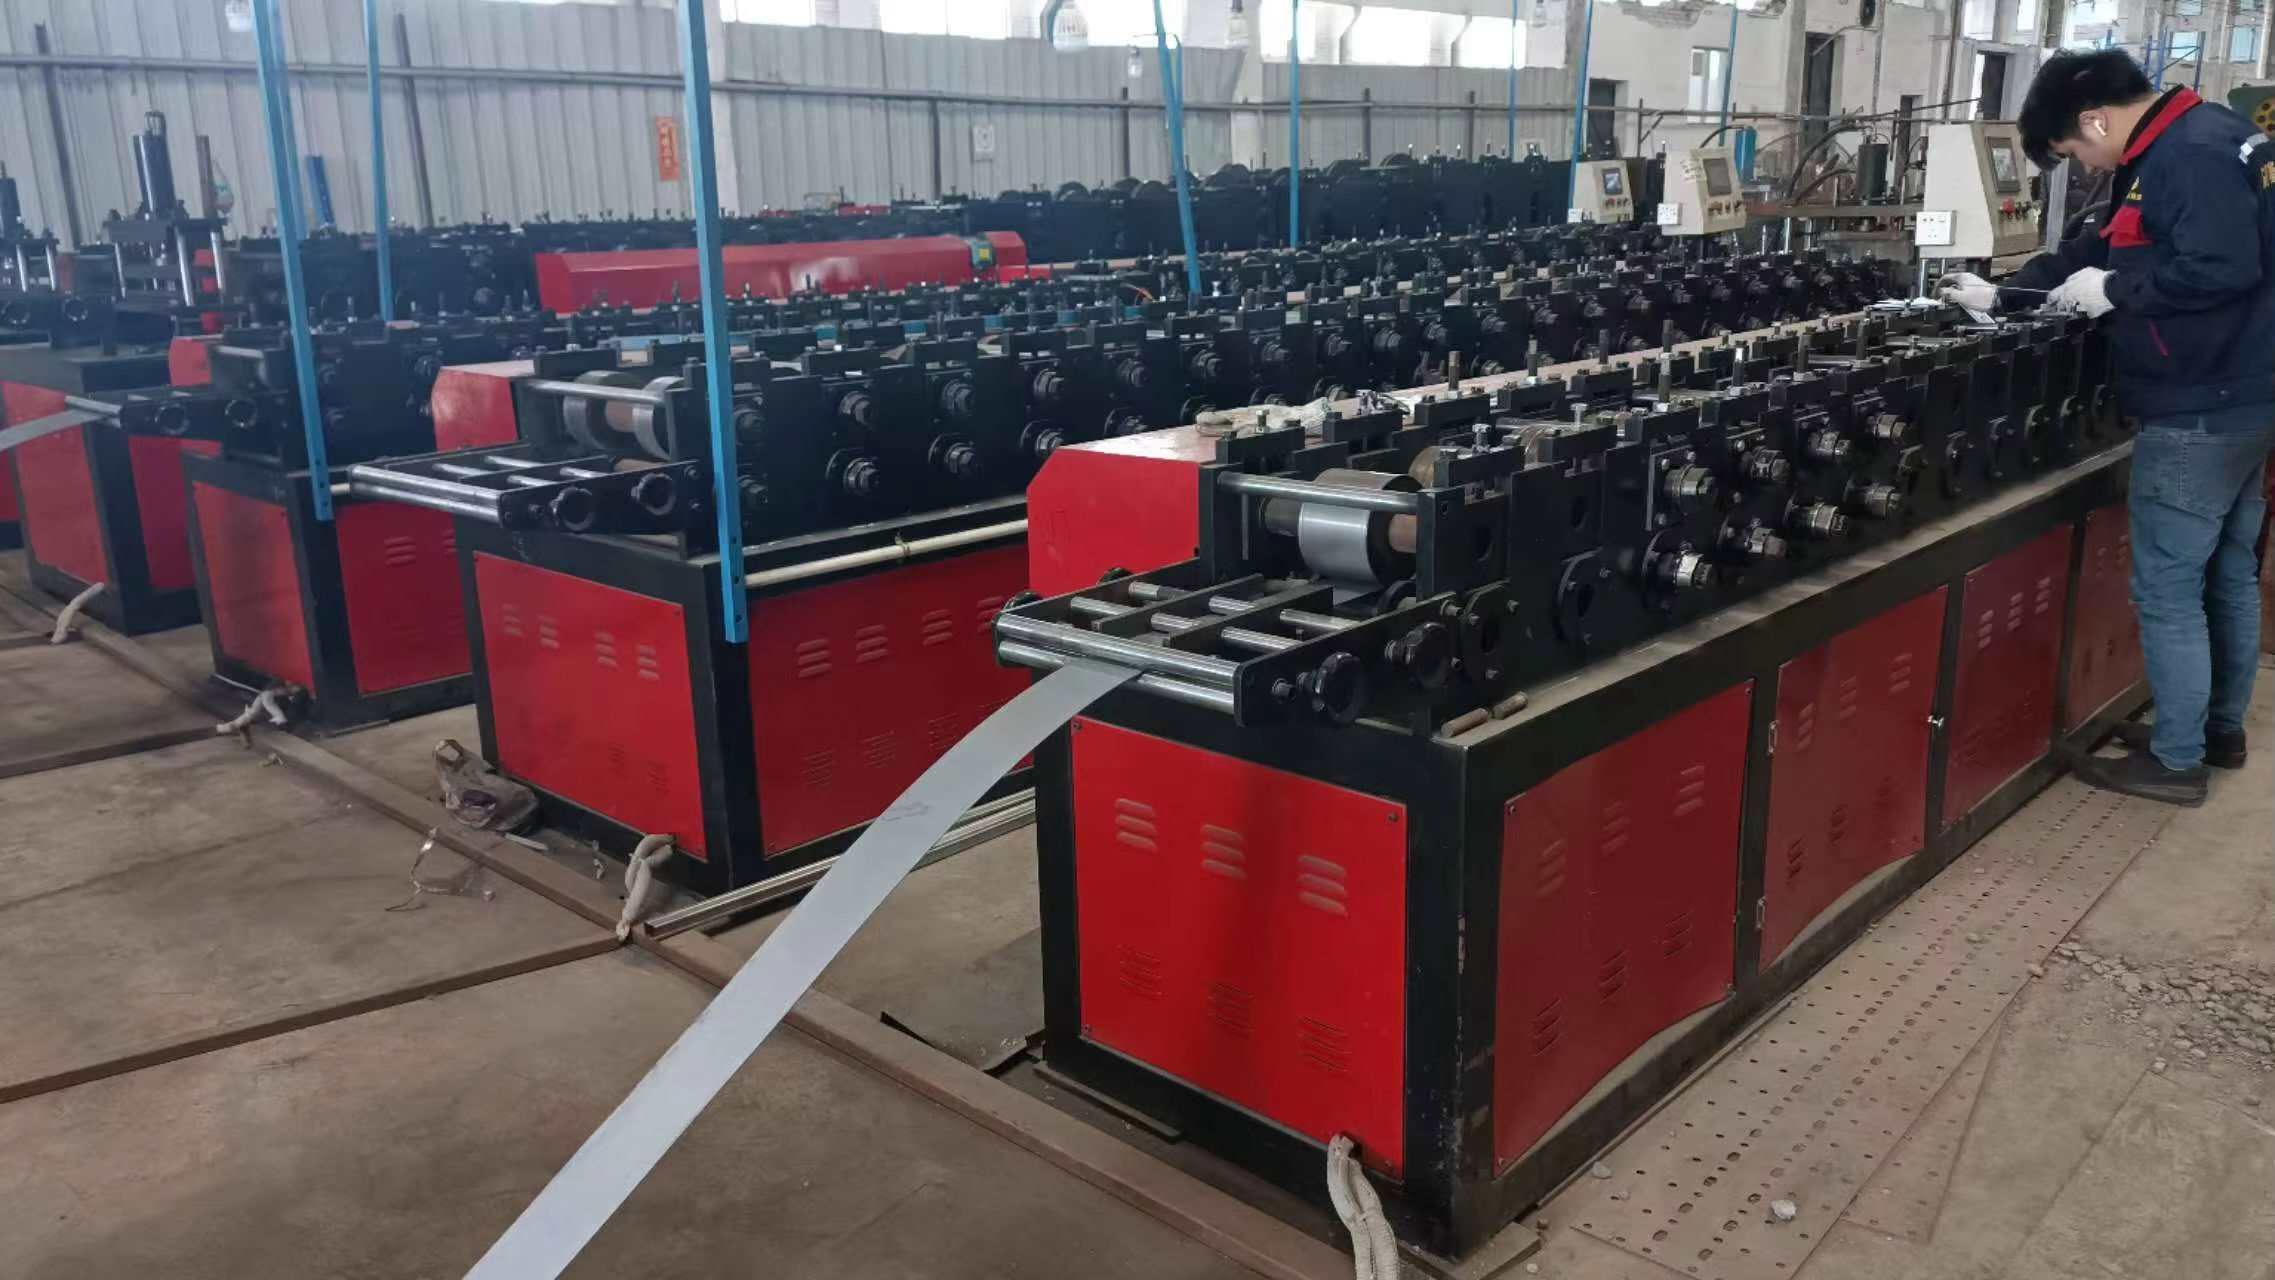
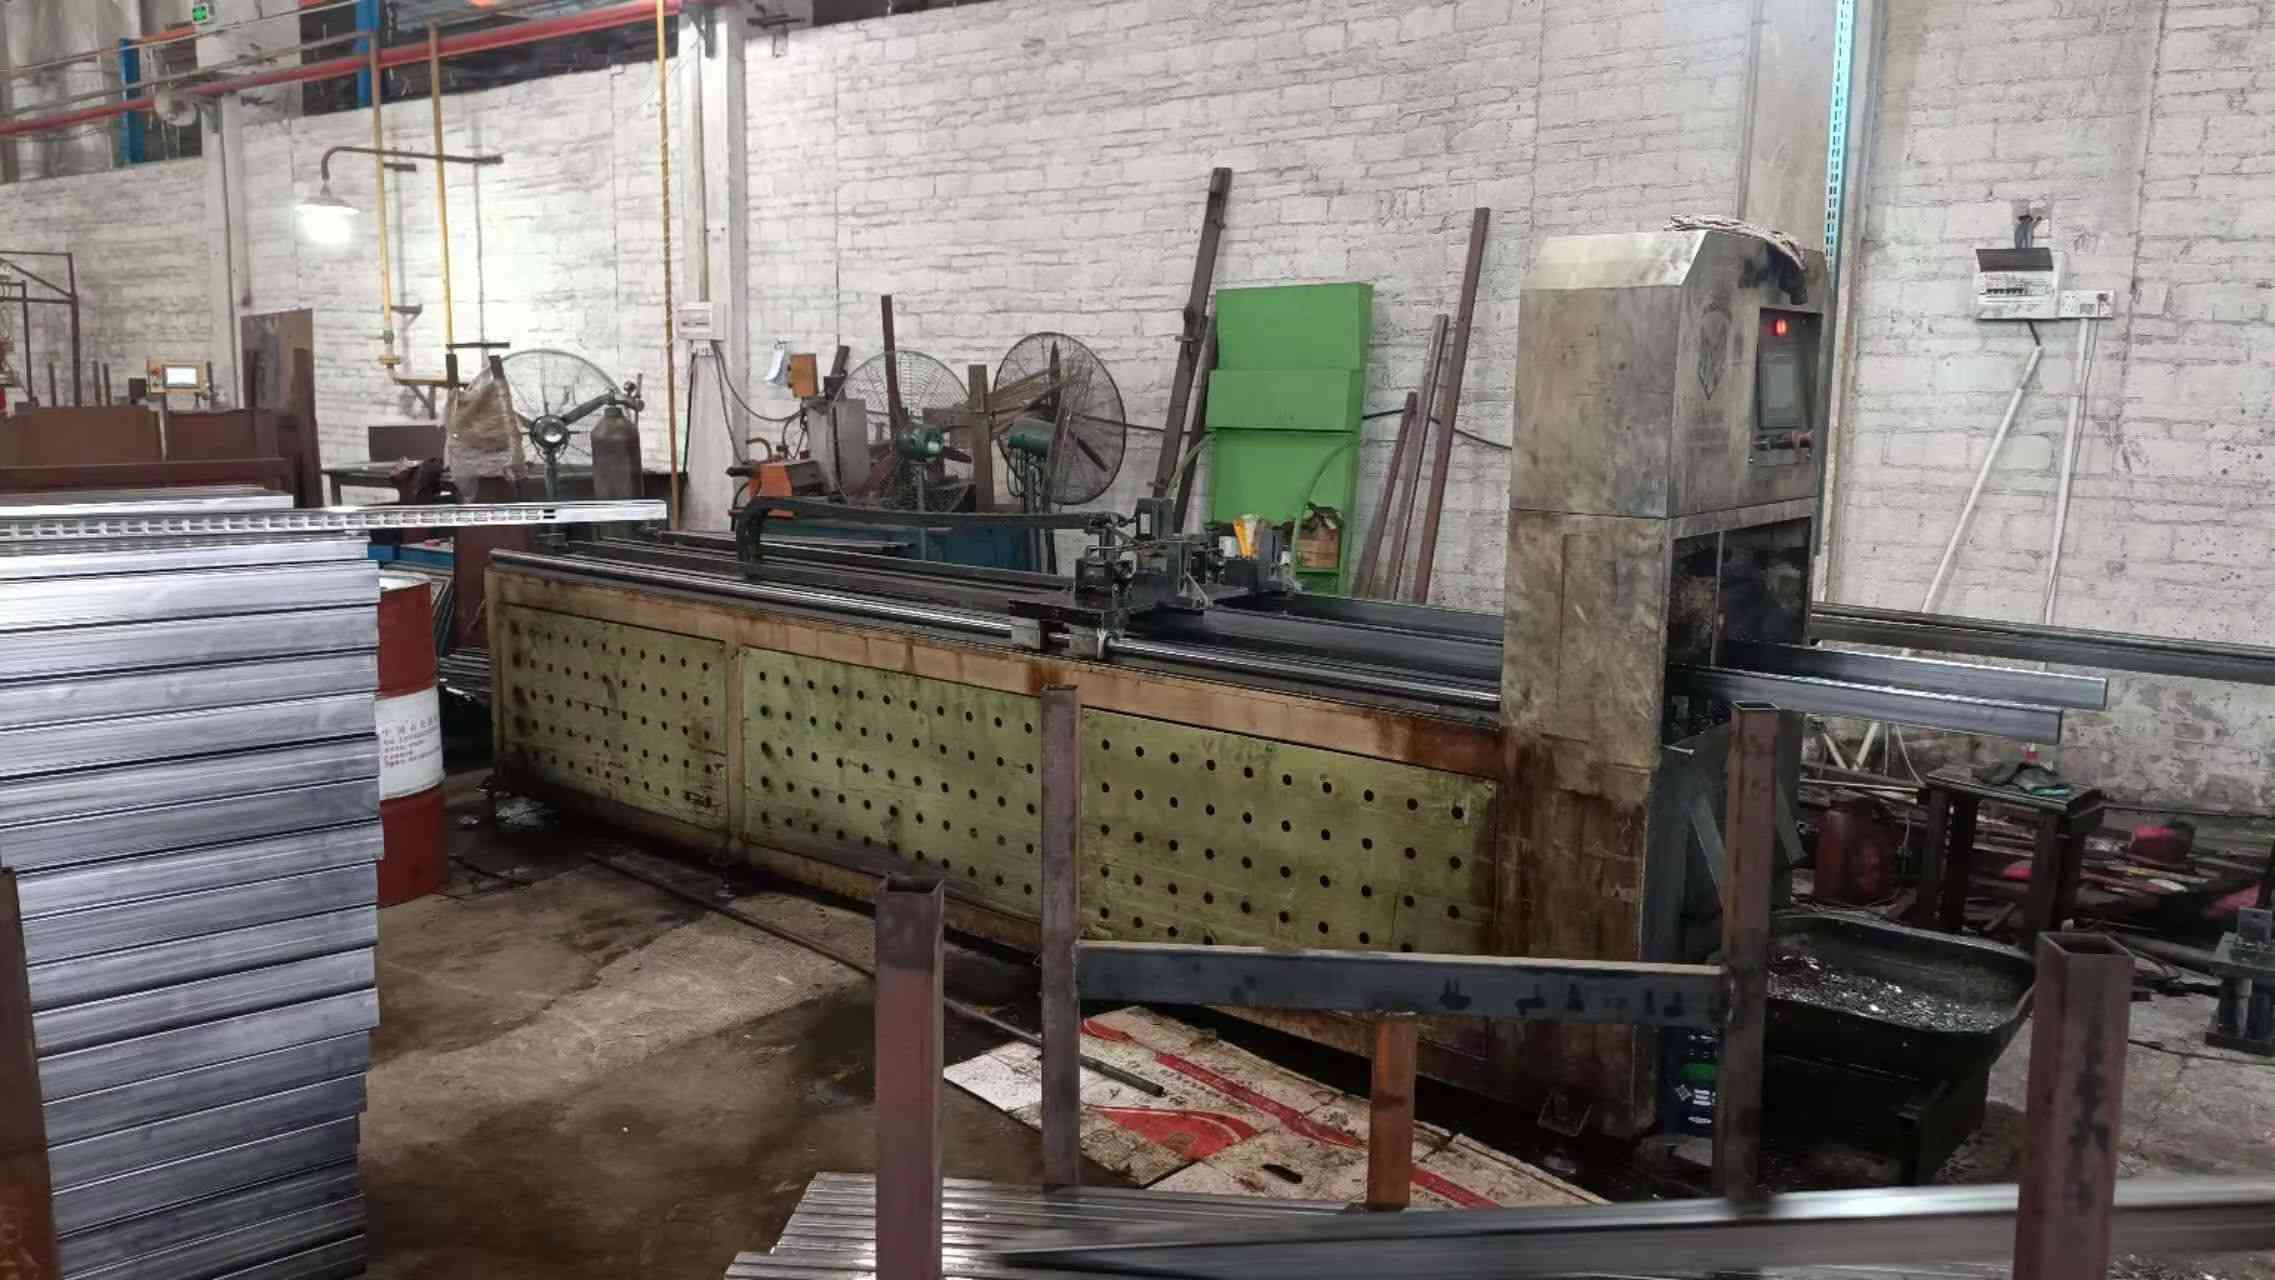
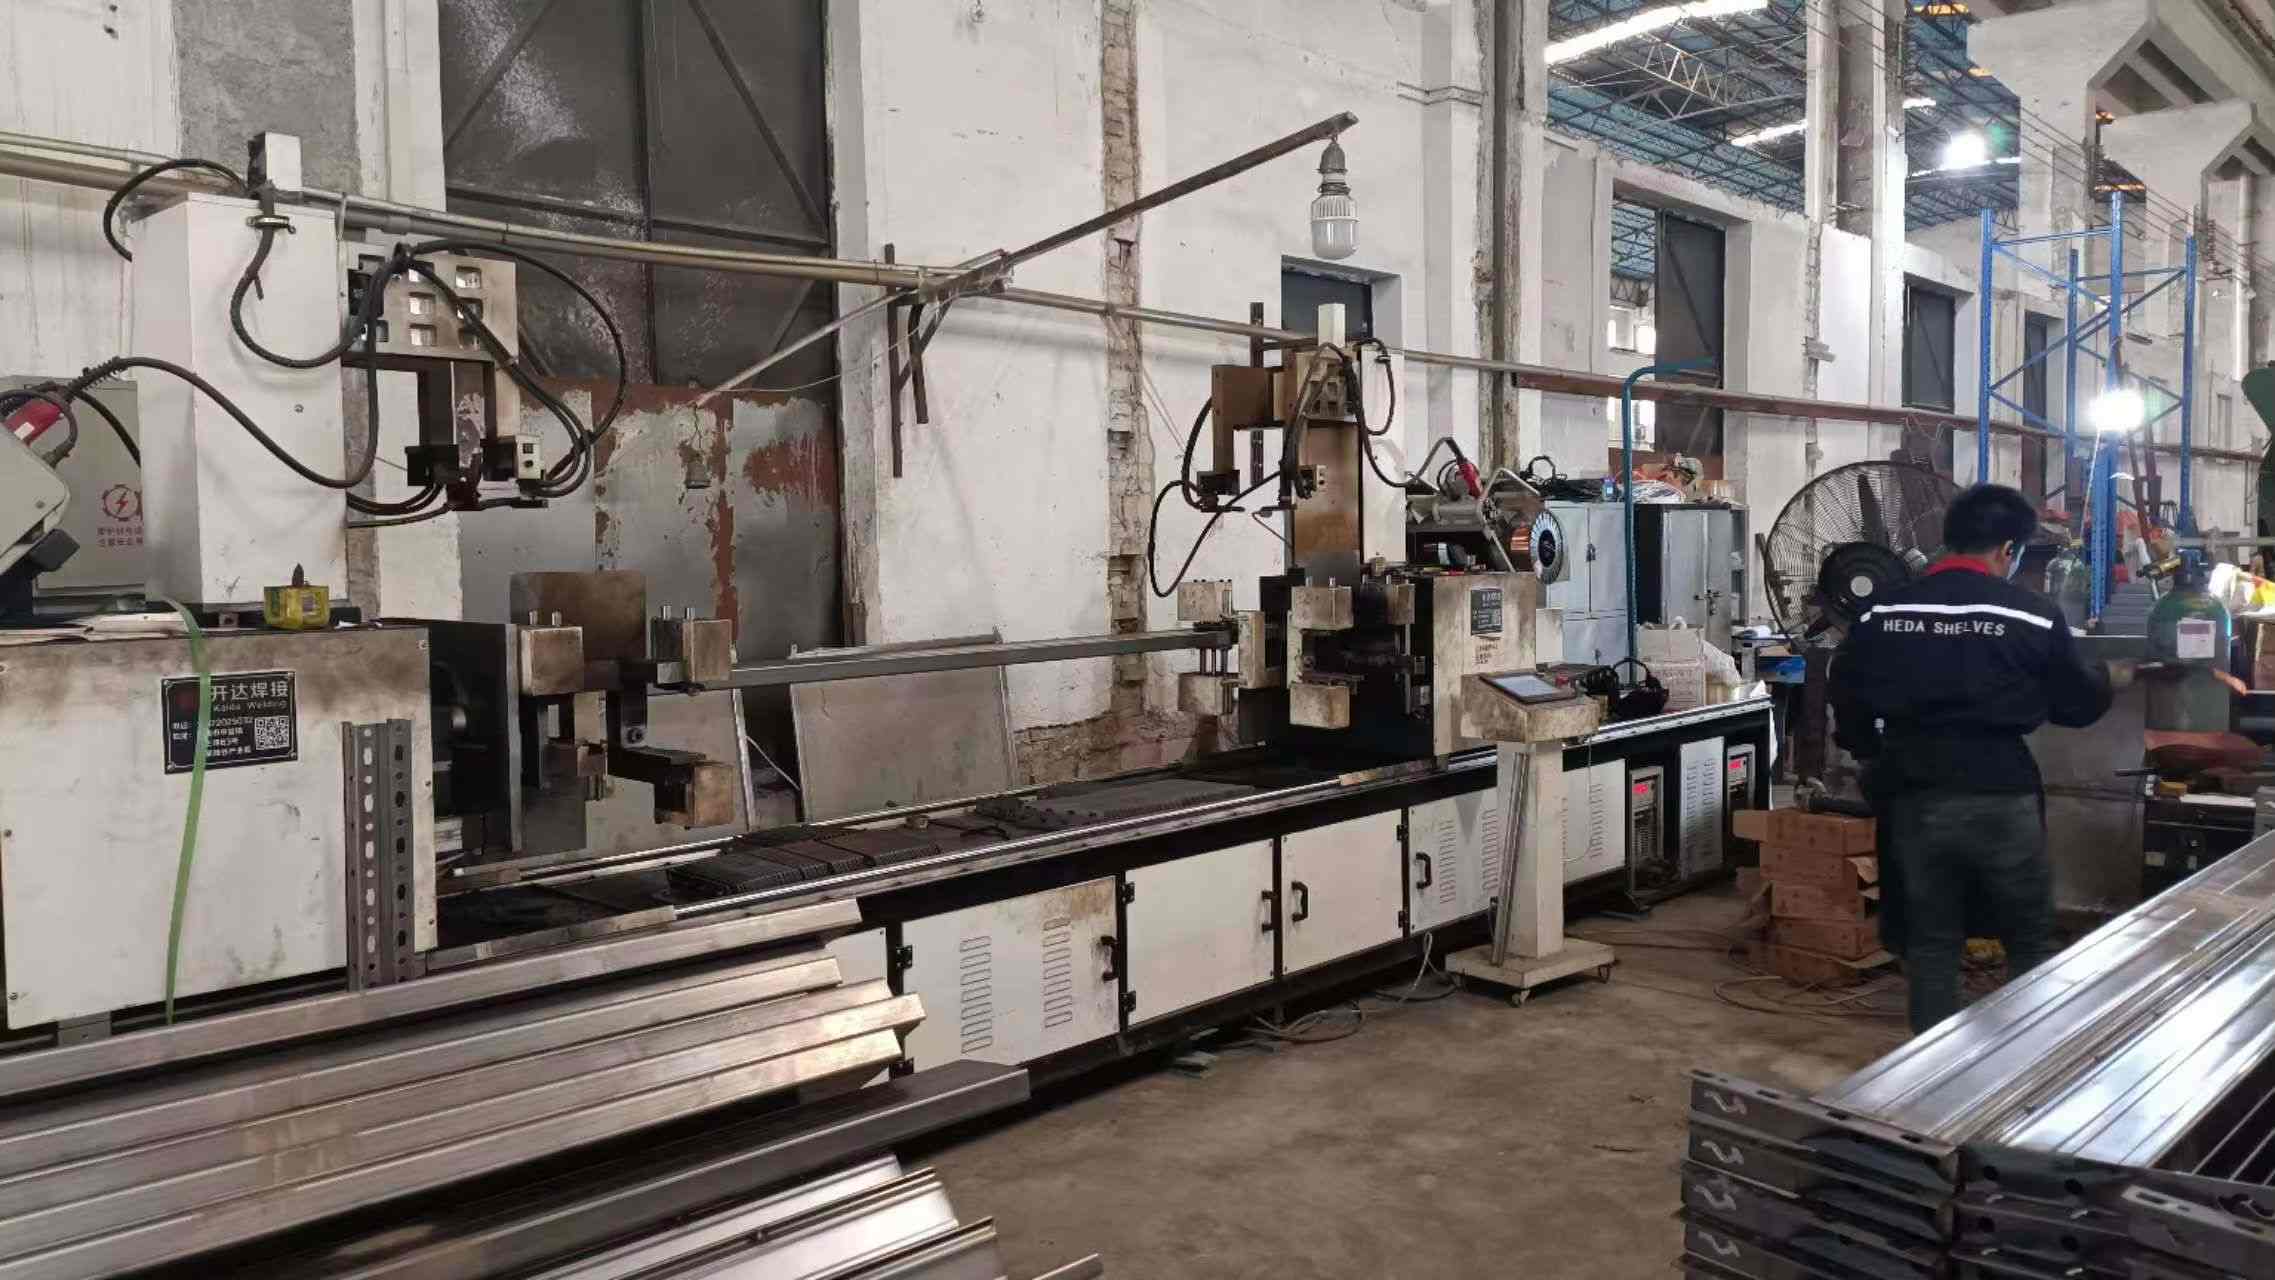
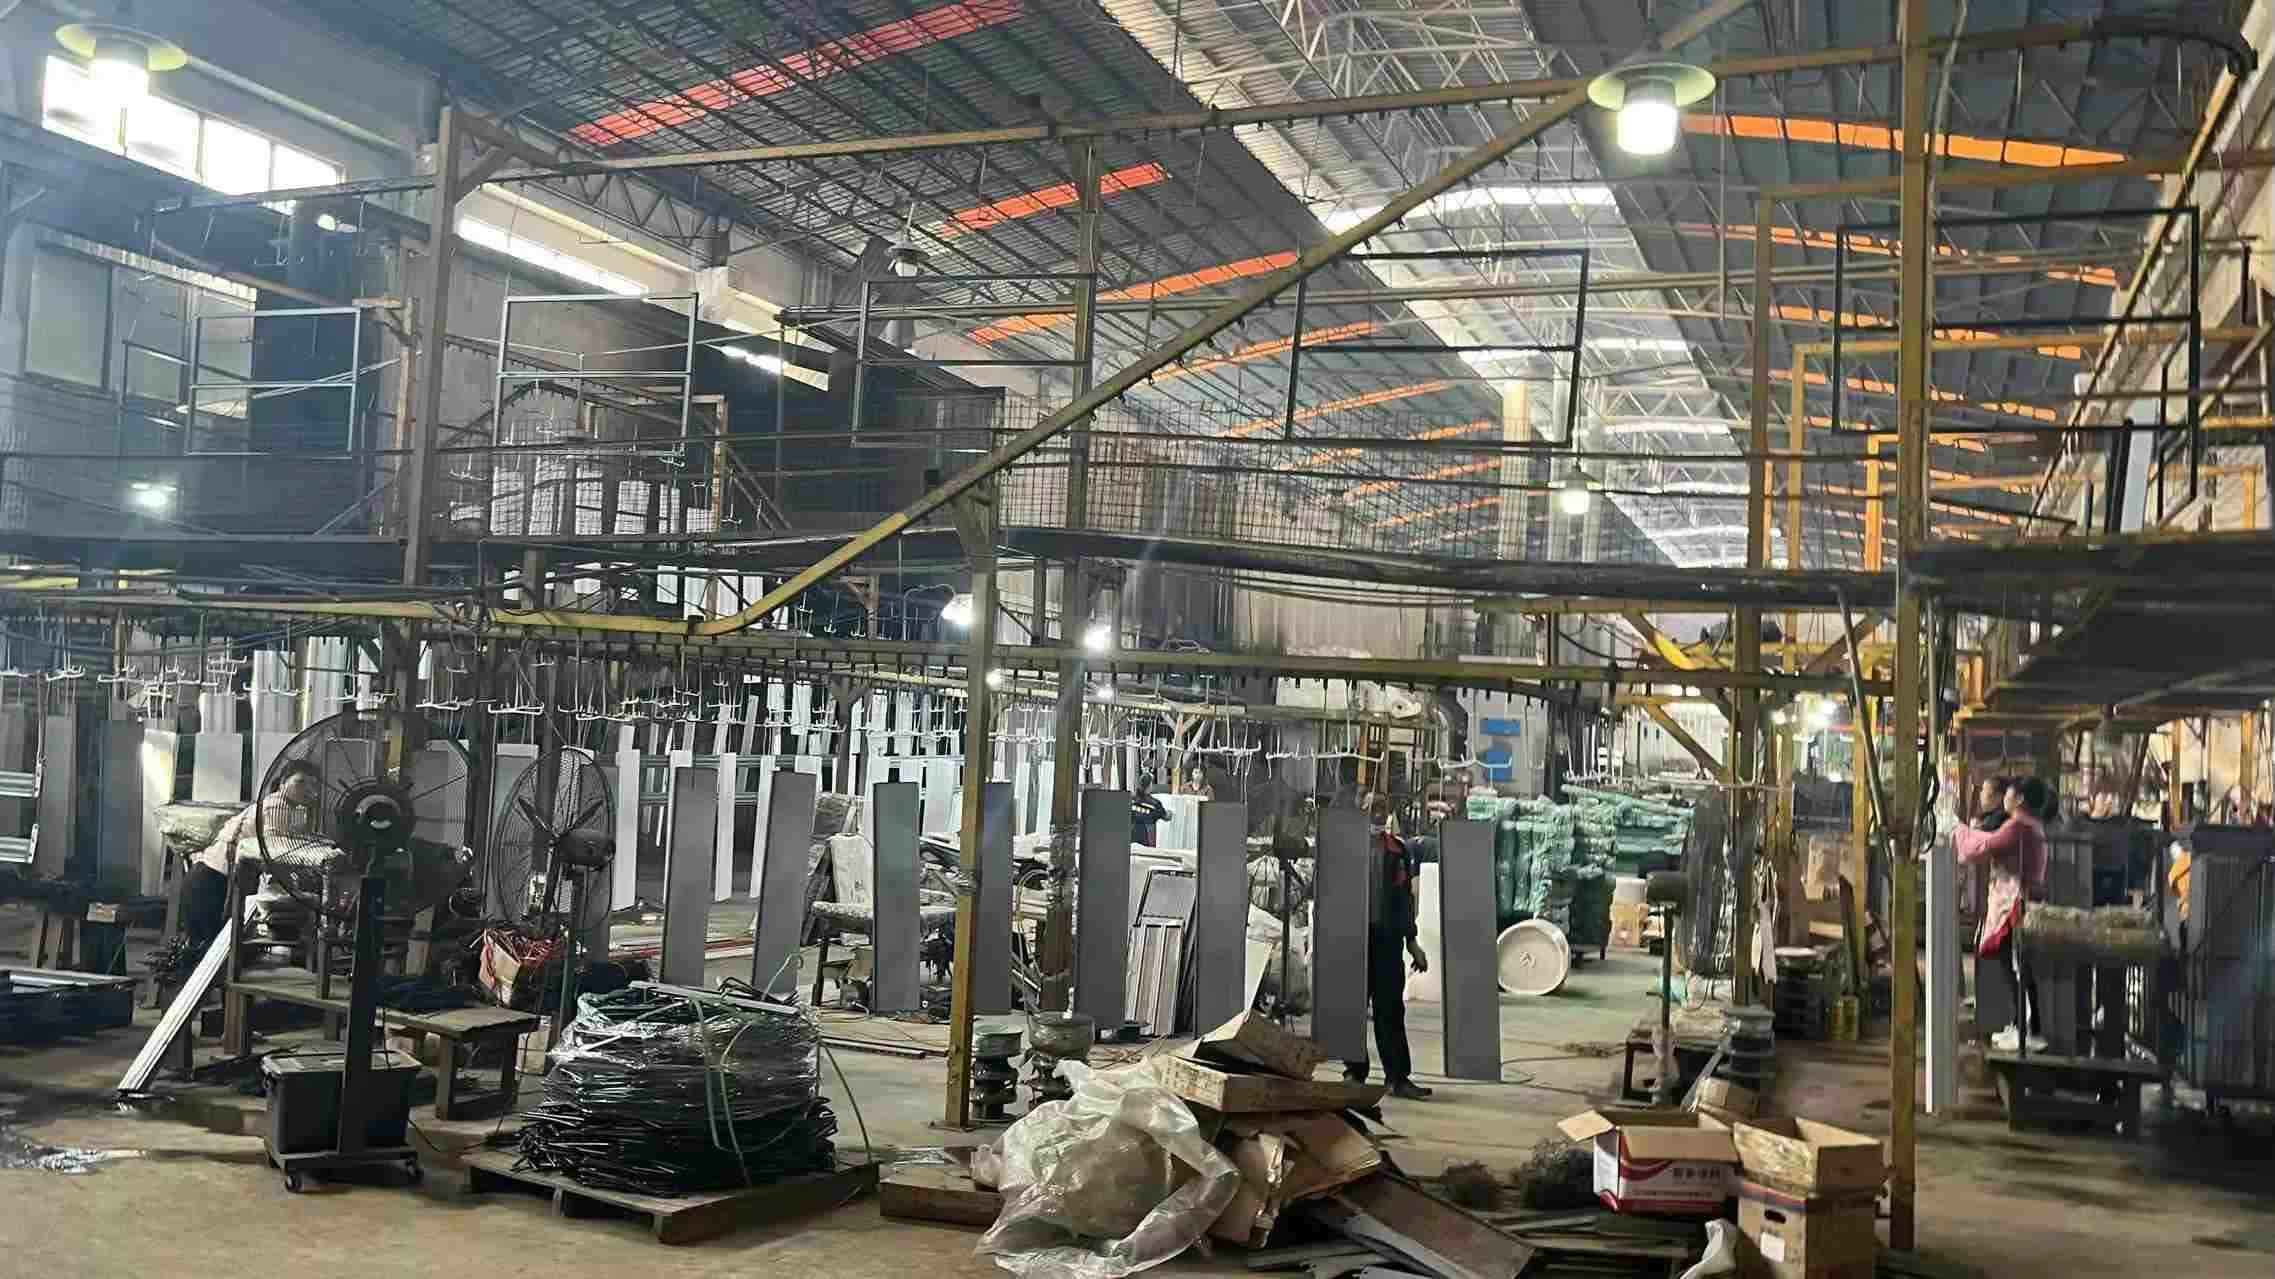
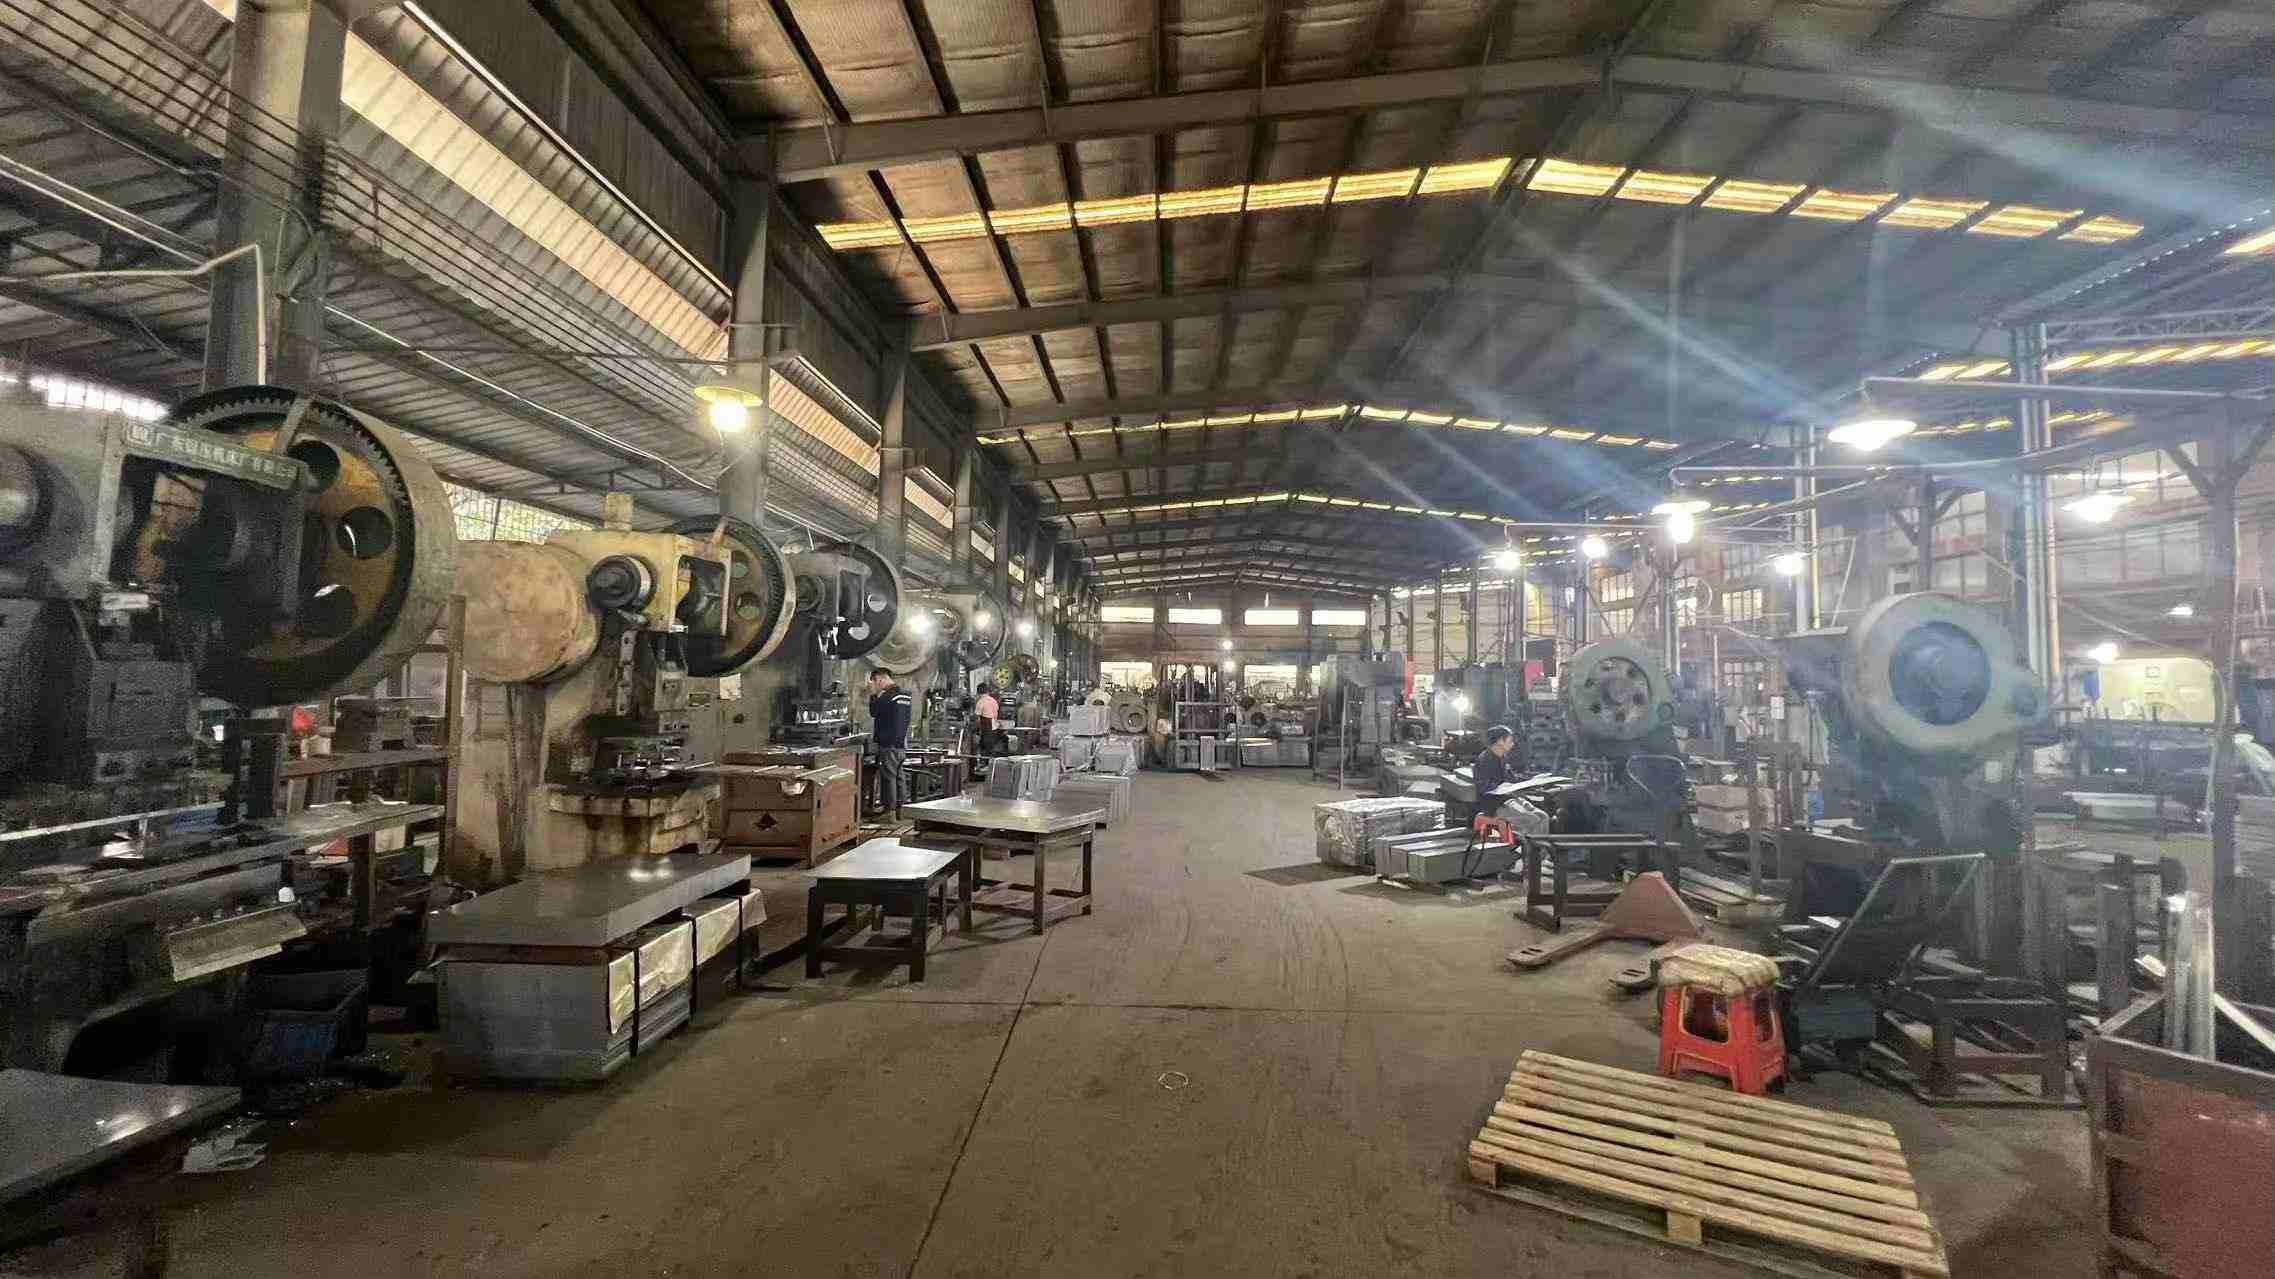
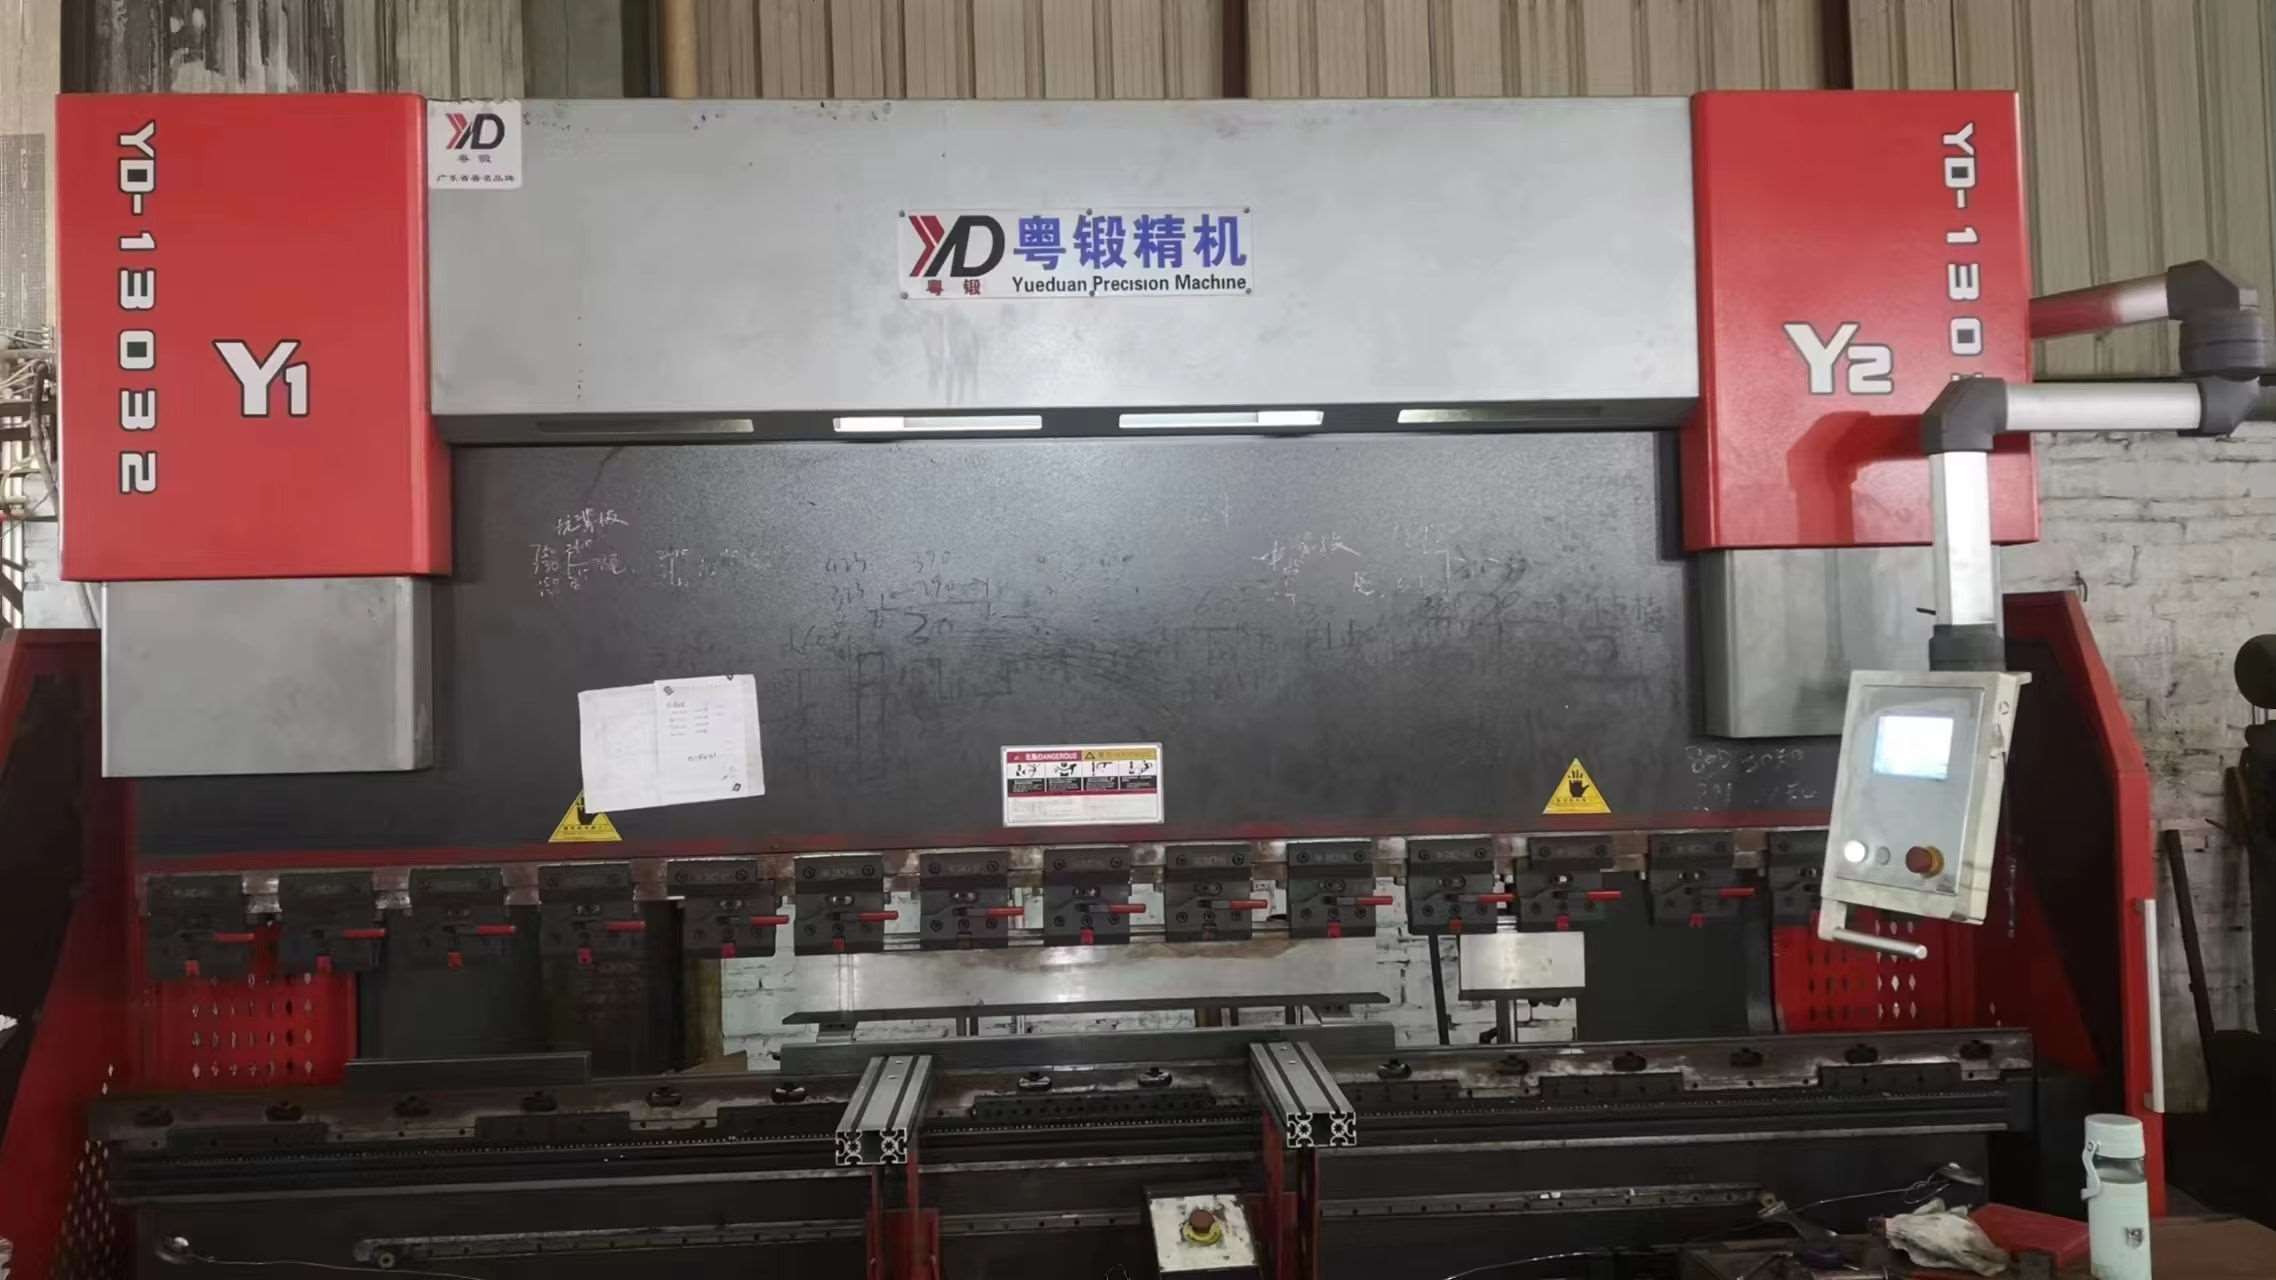
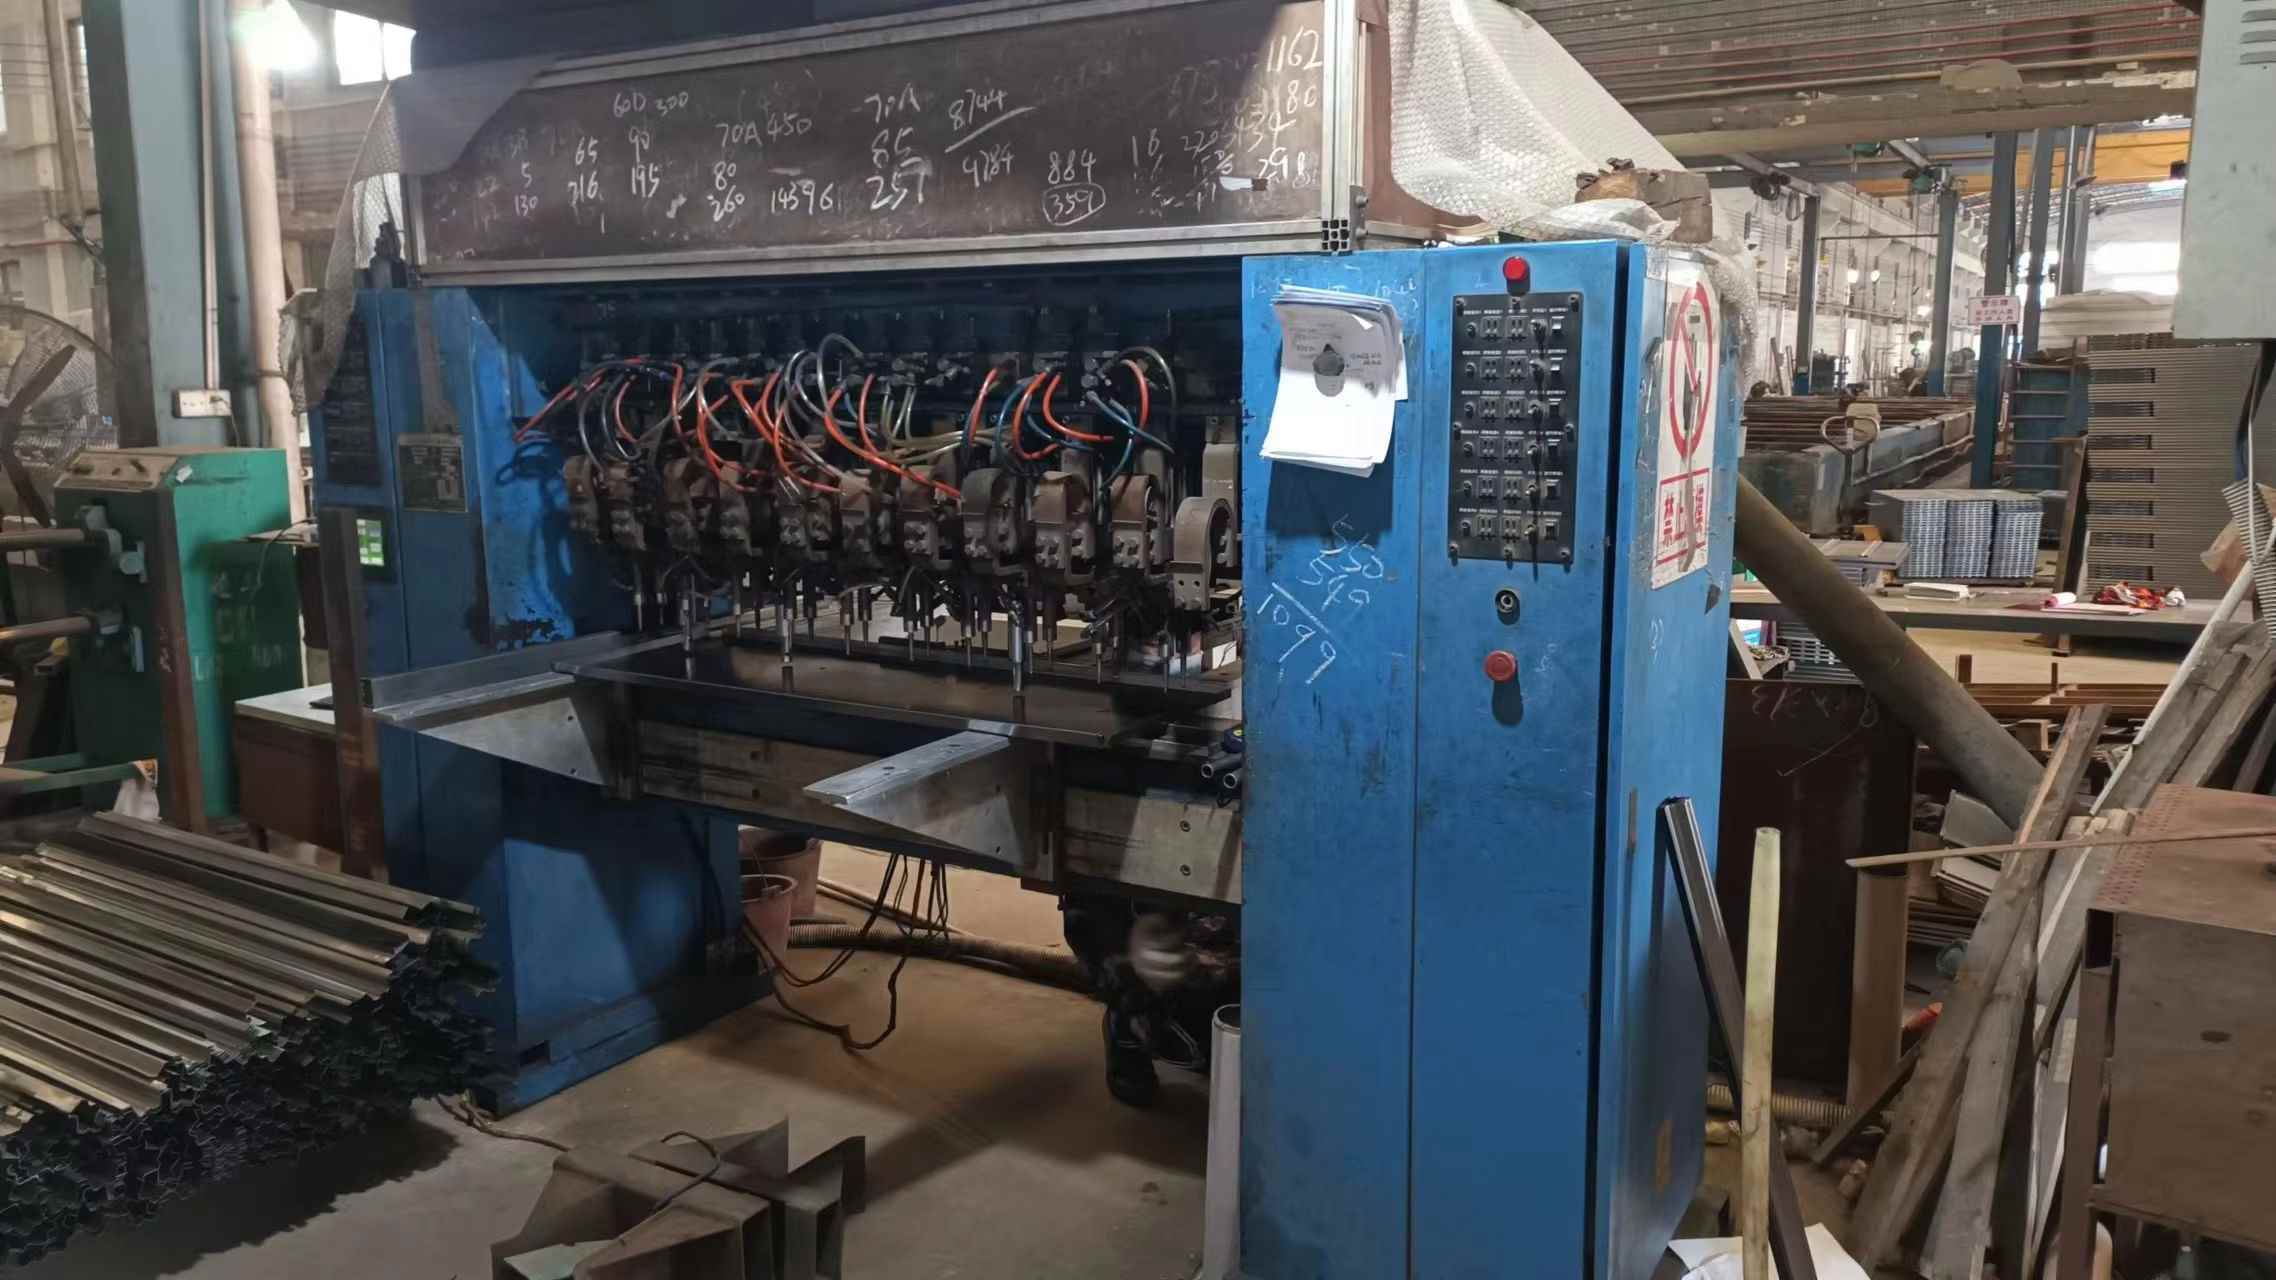
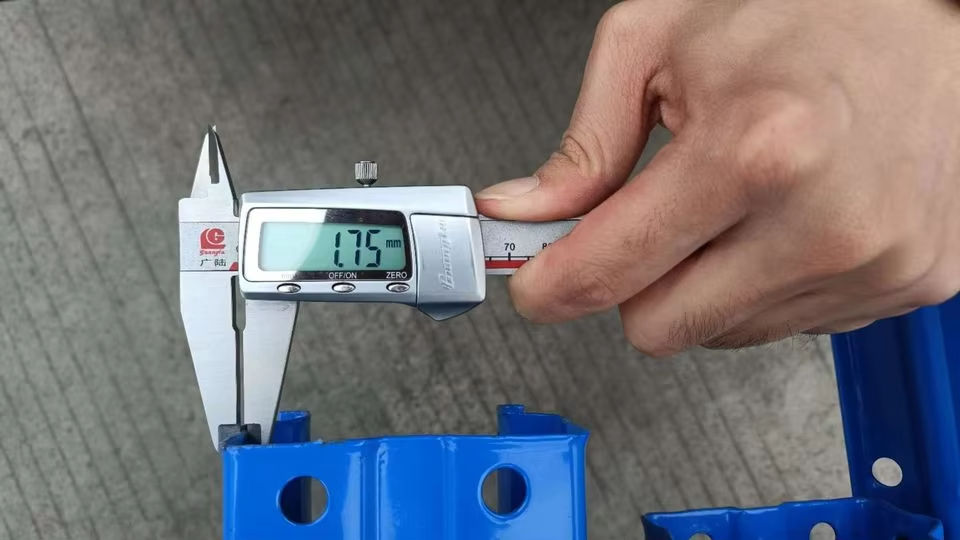
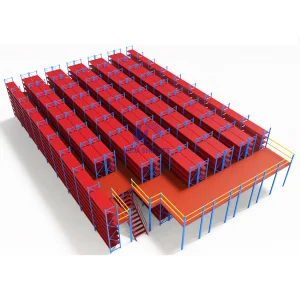
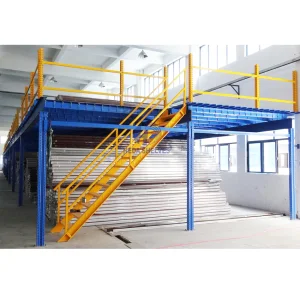
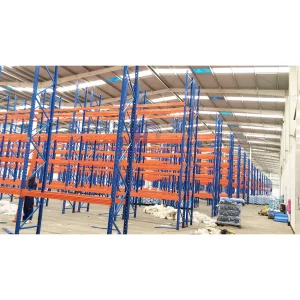
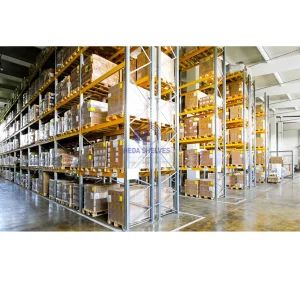
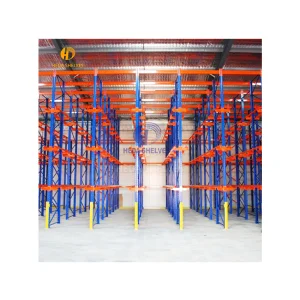
Our storage systems adhere rigorously to international safety and structural standards, including FEM, RMI, ASMS, and CE certifications. Every batch undergoes rigorous load testing to guarantee seismic stability, structural integrity, and long-term workplace safety across North American, European, and Asia-Pacific markets.
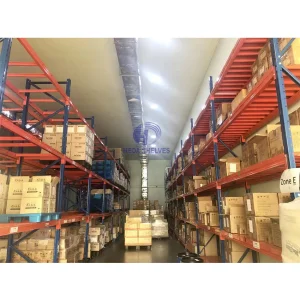
Tailored for fast-paced e-commerce fulfillment, cold storage facilities, automotive distribution, and multi-tier retail warehouses. Our solutions accommodate diverse environmental demands, featuring anti-corrosion finishes for humid maritime regions and heavy-load capacities for industrial manufacturing.
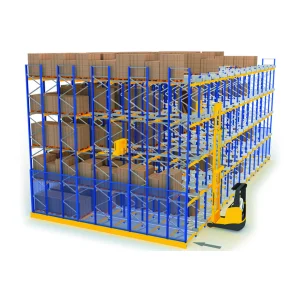
Pioneering the future of warehousing through automated 4-way shuttle systems, IoT-enabled inventory tracking, and seamless integration with Automated Storage and Retrieval Systems (ASRS). We help enterprises transition smoothly into fully autonomous, lights-out fulfillment centers.
 Hedaracking