Engineered for intense retail foot-traffic, heavy structural load capacities, and maximum spatial utilization across supermarket and wholesale operations.
An authoritative whitepaper report on commercial display dynamics, coastal microclimate engineering, and logistics optimization in the Grenville market.
The commercial retail infrastructure in Grenville is experiencing a rapid structural pivot toward high-density superstores, hypermarket formats, and cash-and-carry retail hubs. As consumer purchasing patterns demand wider stock variety and frictionless shelf accessibility, supermarket operators are moving away from traditional light-duty shelving toward heavy-duty, modular steel gondola systems and back-of-house high-bay pallet racking.
Furthermore, urban real estate constraints in Grenville have escalated floor space costs per square meter. Retailers must maximize vertical air-cube utilization without compromising aisle maneuverability, customer safety, or aesthetic visual merchandising standards. This requires precise steel shelf engineering with load ratings engineered specifically for dense inventory stacking.
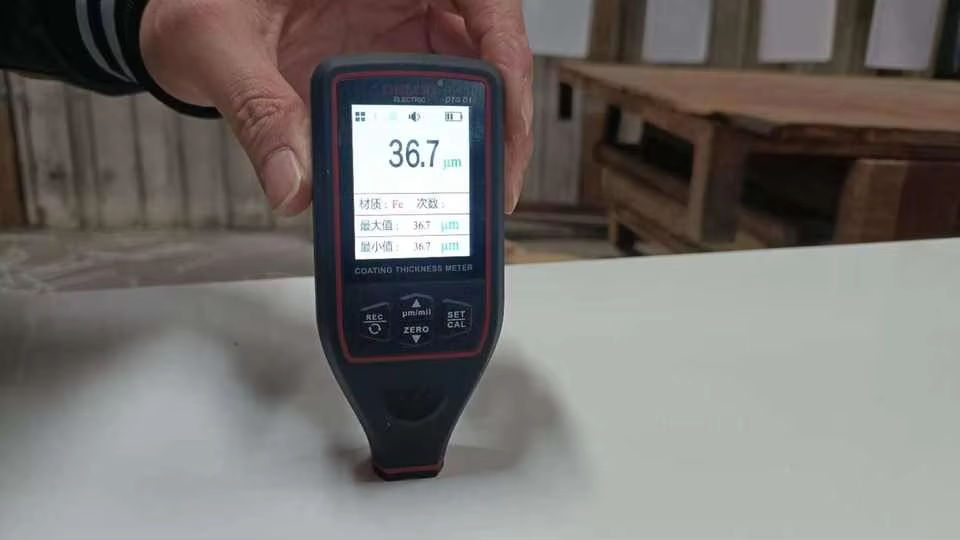
SEO Information Gain Insight: Standard supermarket shelves often fail under sustained high-load capacity in coastal commercial corridors due to environmental humidity. HEDA’s structural Q235B cold-rolled steel design integrates an advanced multi-stage electro-powder coating, delivering 500+ hours of ASTM B117 salt spray protection specifically customized for Grenville's atmospheric conditions.
Commercial store managers and warehouse directors across Grenville face distinct physical and operational pressures:
Tailored shelf and racking architectures optimized for diverse commercial end-uses in the Grenville regional ecosystem.
Double-sided central gondolas and single-sided wall shelving units engineered for high aesthetic appeal. Feature clean powder-coated steel finishes, optional LED shelf-edge lighting channels, dynamic price tags, and heavy-load support columns for premium FMCG merchandising in Grenville retail stores.
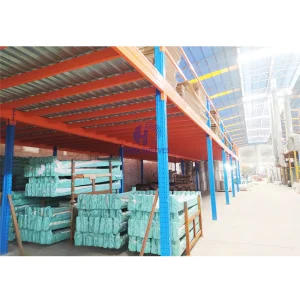
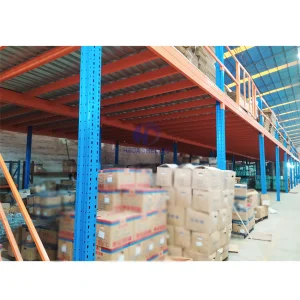
Hybrid storage-display systems that combine lower-tier retail display shelves with upper-tier heavy pallet beam storage. Designed for Grenville wholesale clubs where floor inventory replenishment occurs directly above customer shopping zones.
Corrosion-proof wire shelving and stainless steel rack assemblies customized for Grenville grocery cold-chain storage. Features open-wire ventilation to promote uniform air circulation, anti-bacterial coating options, and resistance to sub-zero freezer condensation.
Integrating R&D, structural engineering, direct-factory production, and international logistics execution for the Grenville market.
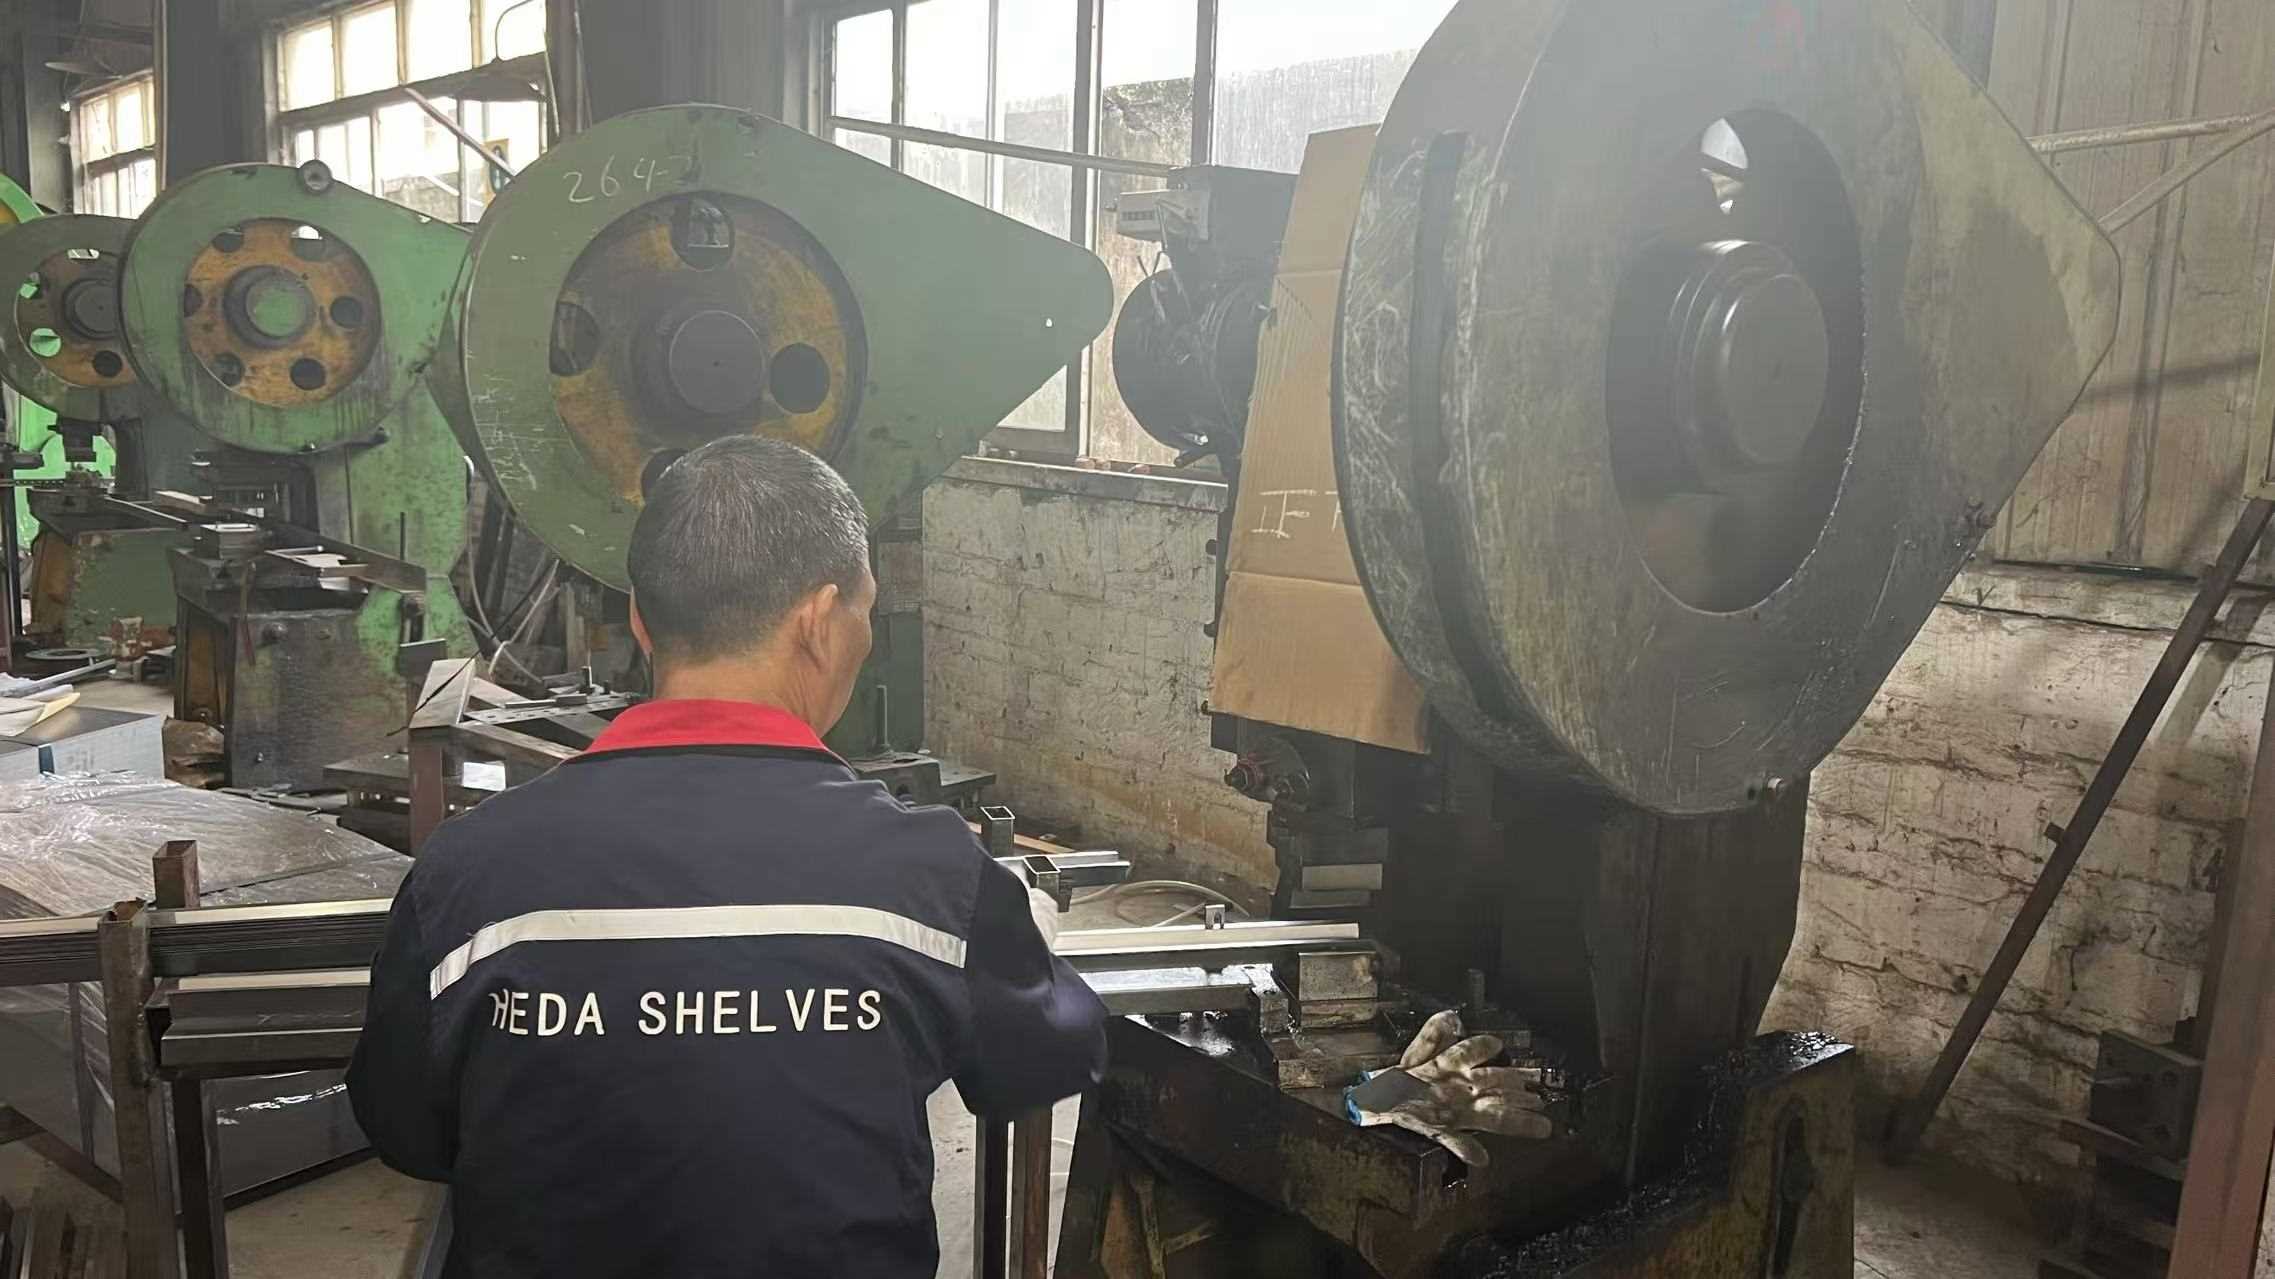
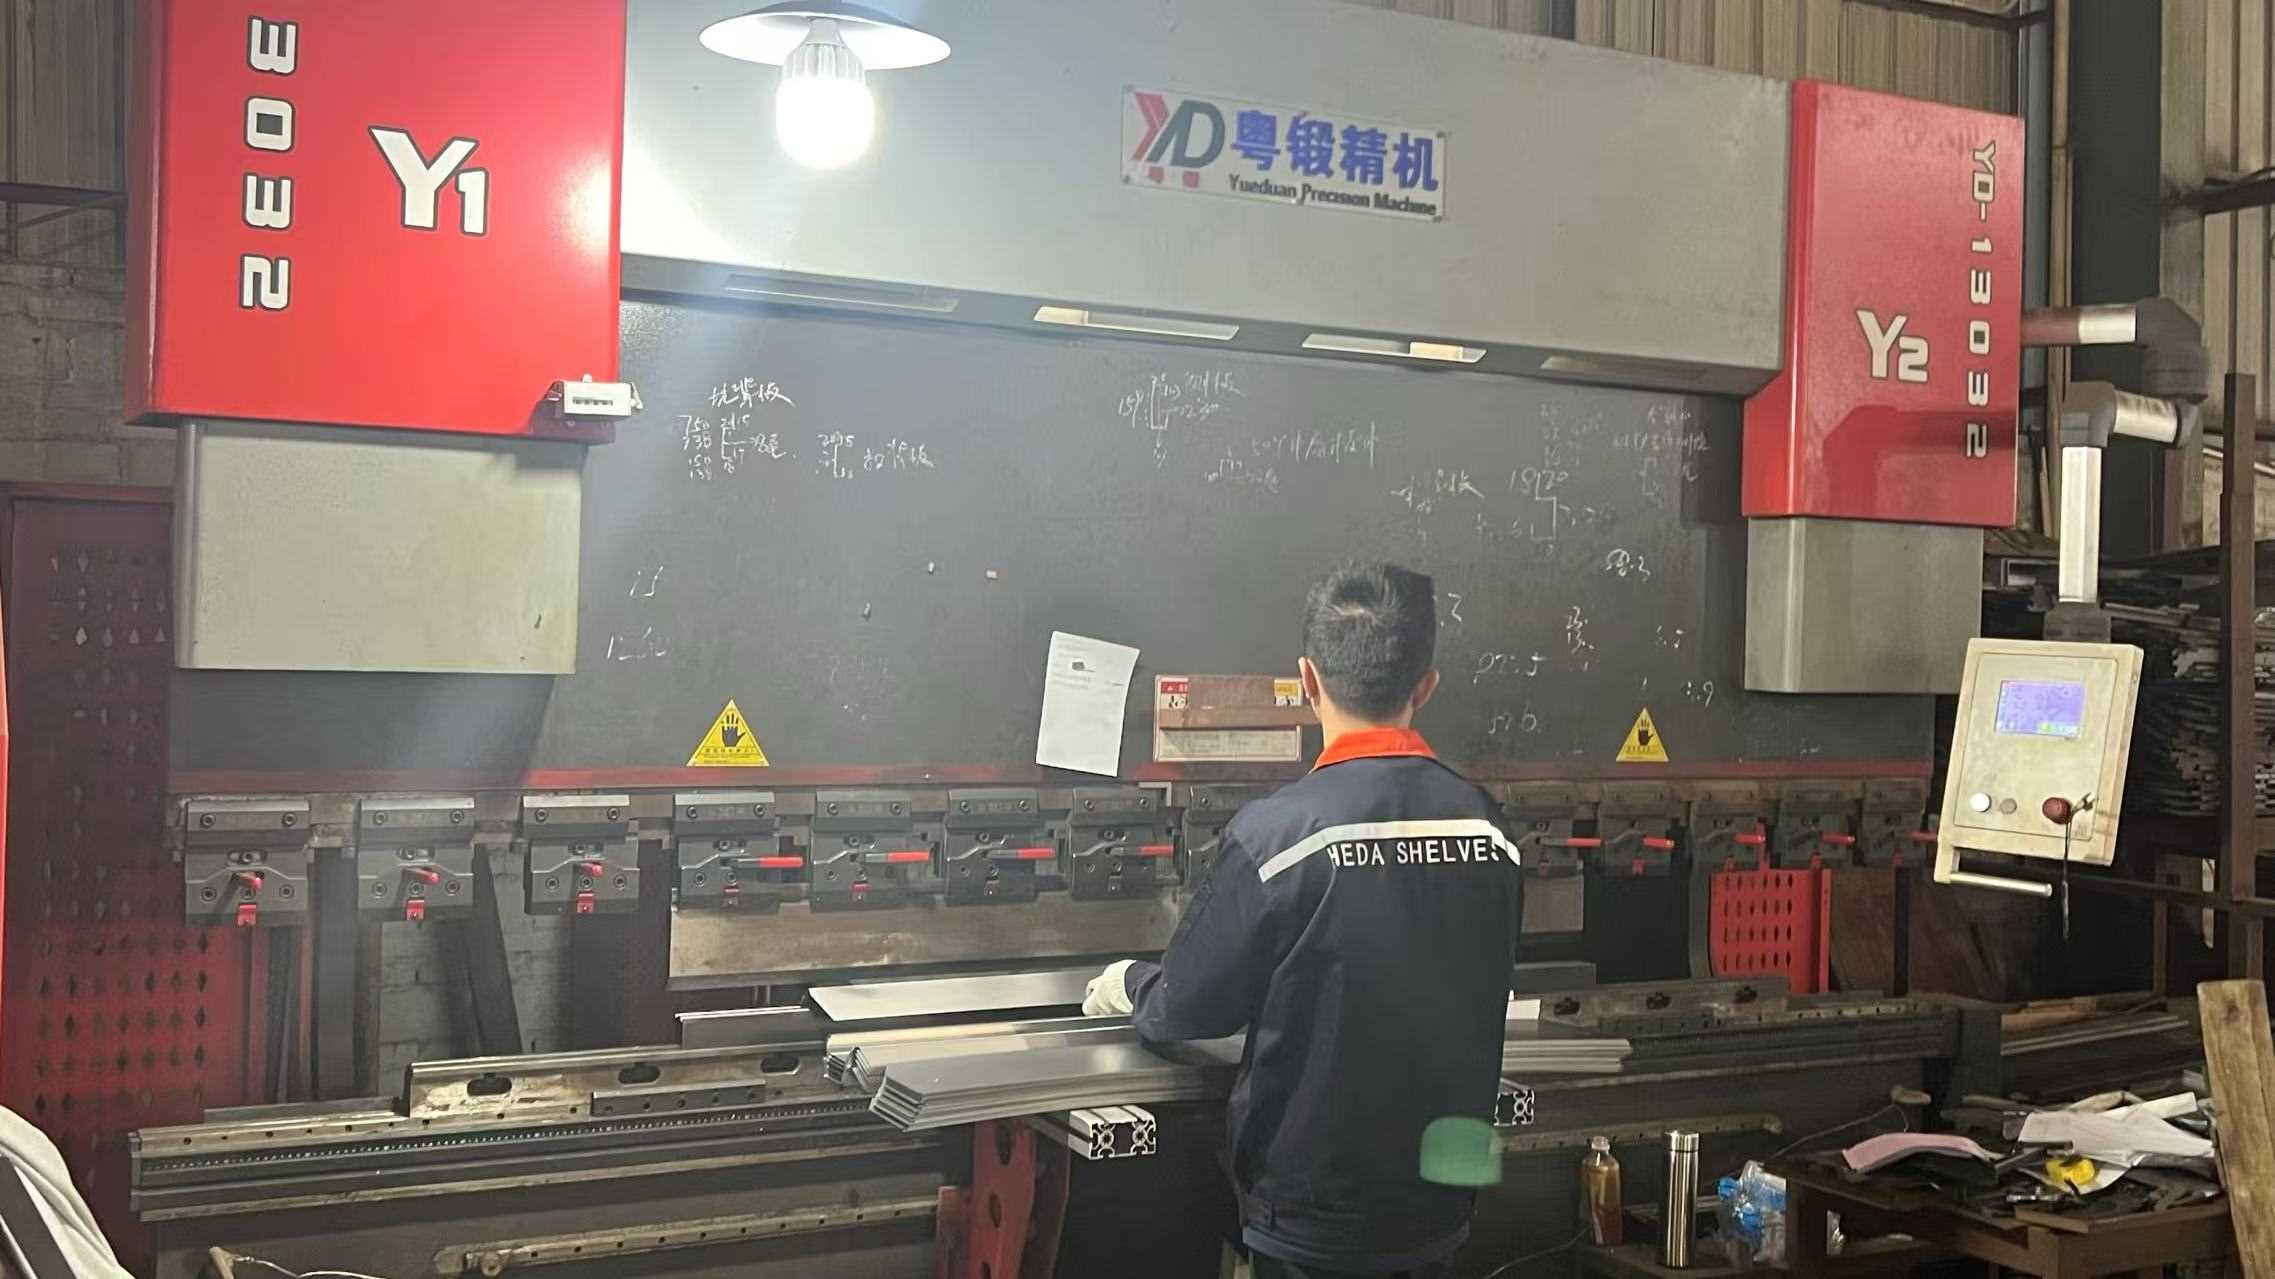
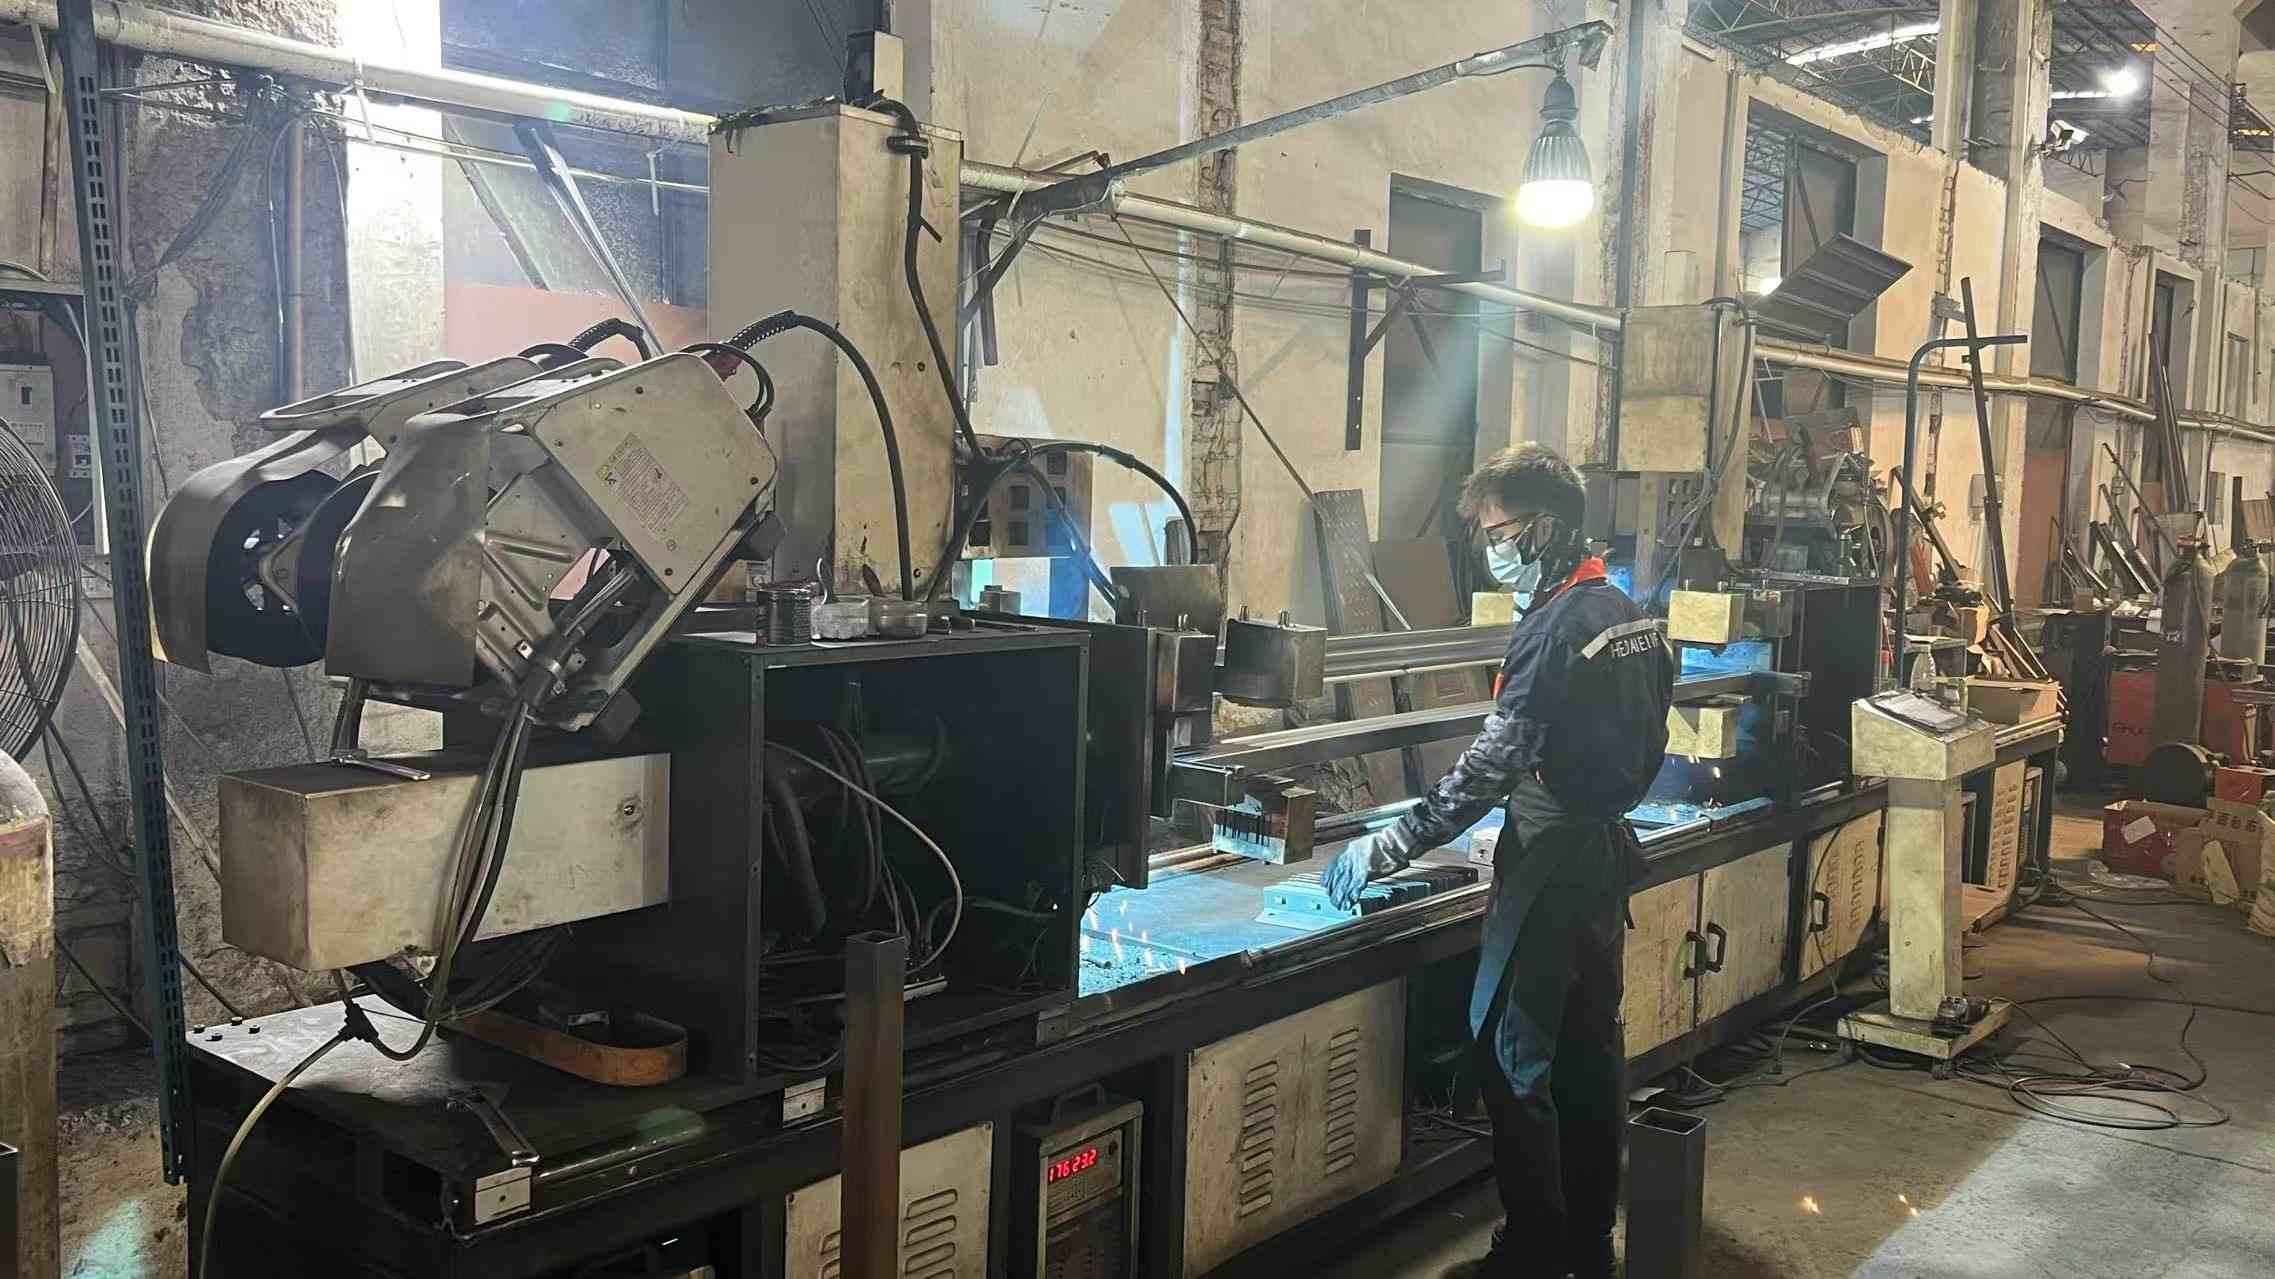
Established in 2014, Shenzhen Heda Warehouse Equipment Co., Ltd. is a premier manufacturer specializing in heavy-duty warehouse racking and industrial storage solutions. Spanning a modern manufacturing facility of 35,000 m², our enterprise integrates R&D, design, production, and international marketing to serve diverse storage needs worldwide. With 12 years of industry experience and 8 years of dedicated export expertise, we deliver high-caliber storage systems that generate over $28 million in annual export revenue.
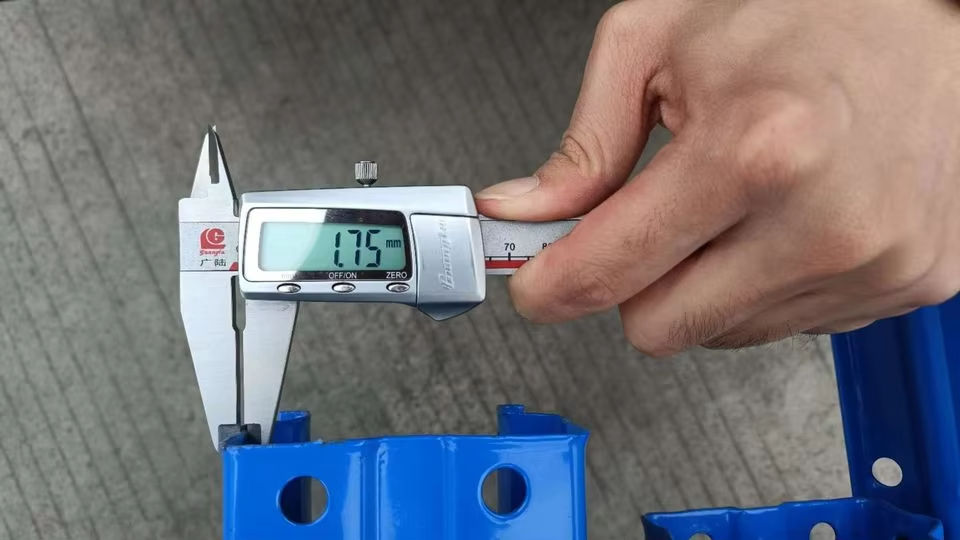
At Heda, quality control and engineering innovation drive our core operations. Our robust QC department comprises 45 skilled inspectors utilizing rigorous testing methods, including raw material tensile testing, automated weld flaw detection, layer load-bearing stress analysis, and salt spray surface corrosion testing. Supported by a professional R&D team of 28 senior structural engineers, we maintain strong full-customization capabilities (OEM/ODM)—offering tailored rack dimensions, load capacities, surface coatings, and layout designs. Driven by continuous innovation, we launched over 120 new dynamic storage products and component upgrades last year.
Operating with a strong direct-factory and international trade background, we have built a resilient ecosystem supported by over 800 supply chain partners. Our products are exported to major global markets, including North America, Western Europe, Southeast Asia, and the Middle East. We proudly serve a diverse clientele ranging from third-party logistics (3PL) providers and large distribution centers to industrial manufacturers and wholesale equipment distributors in Grenville.
Send Inquiry Now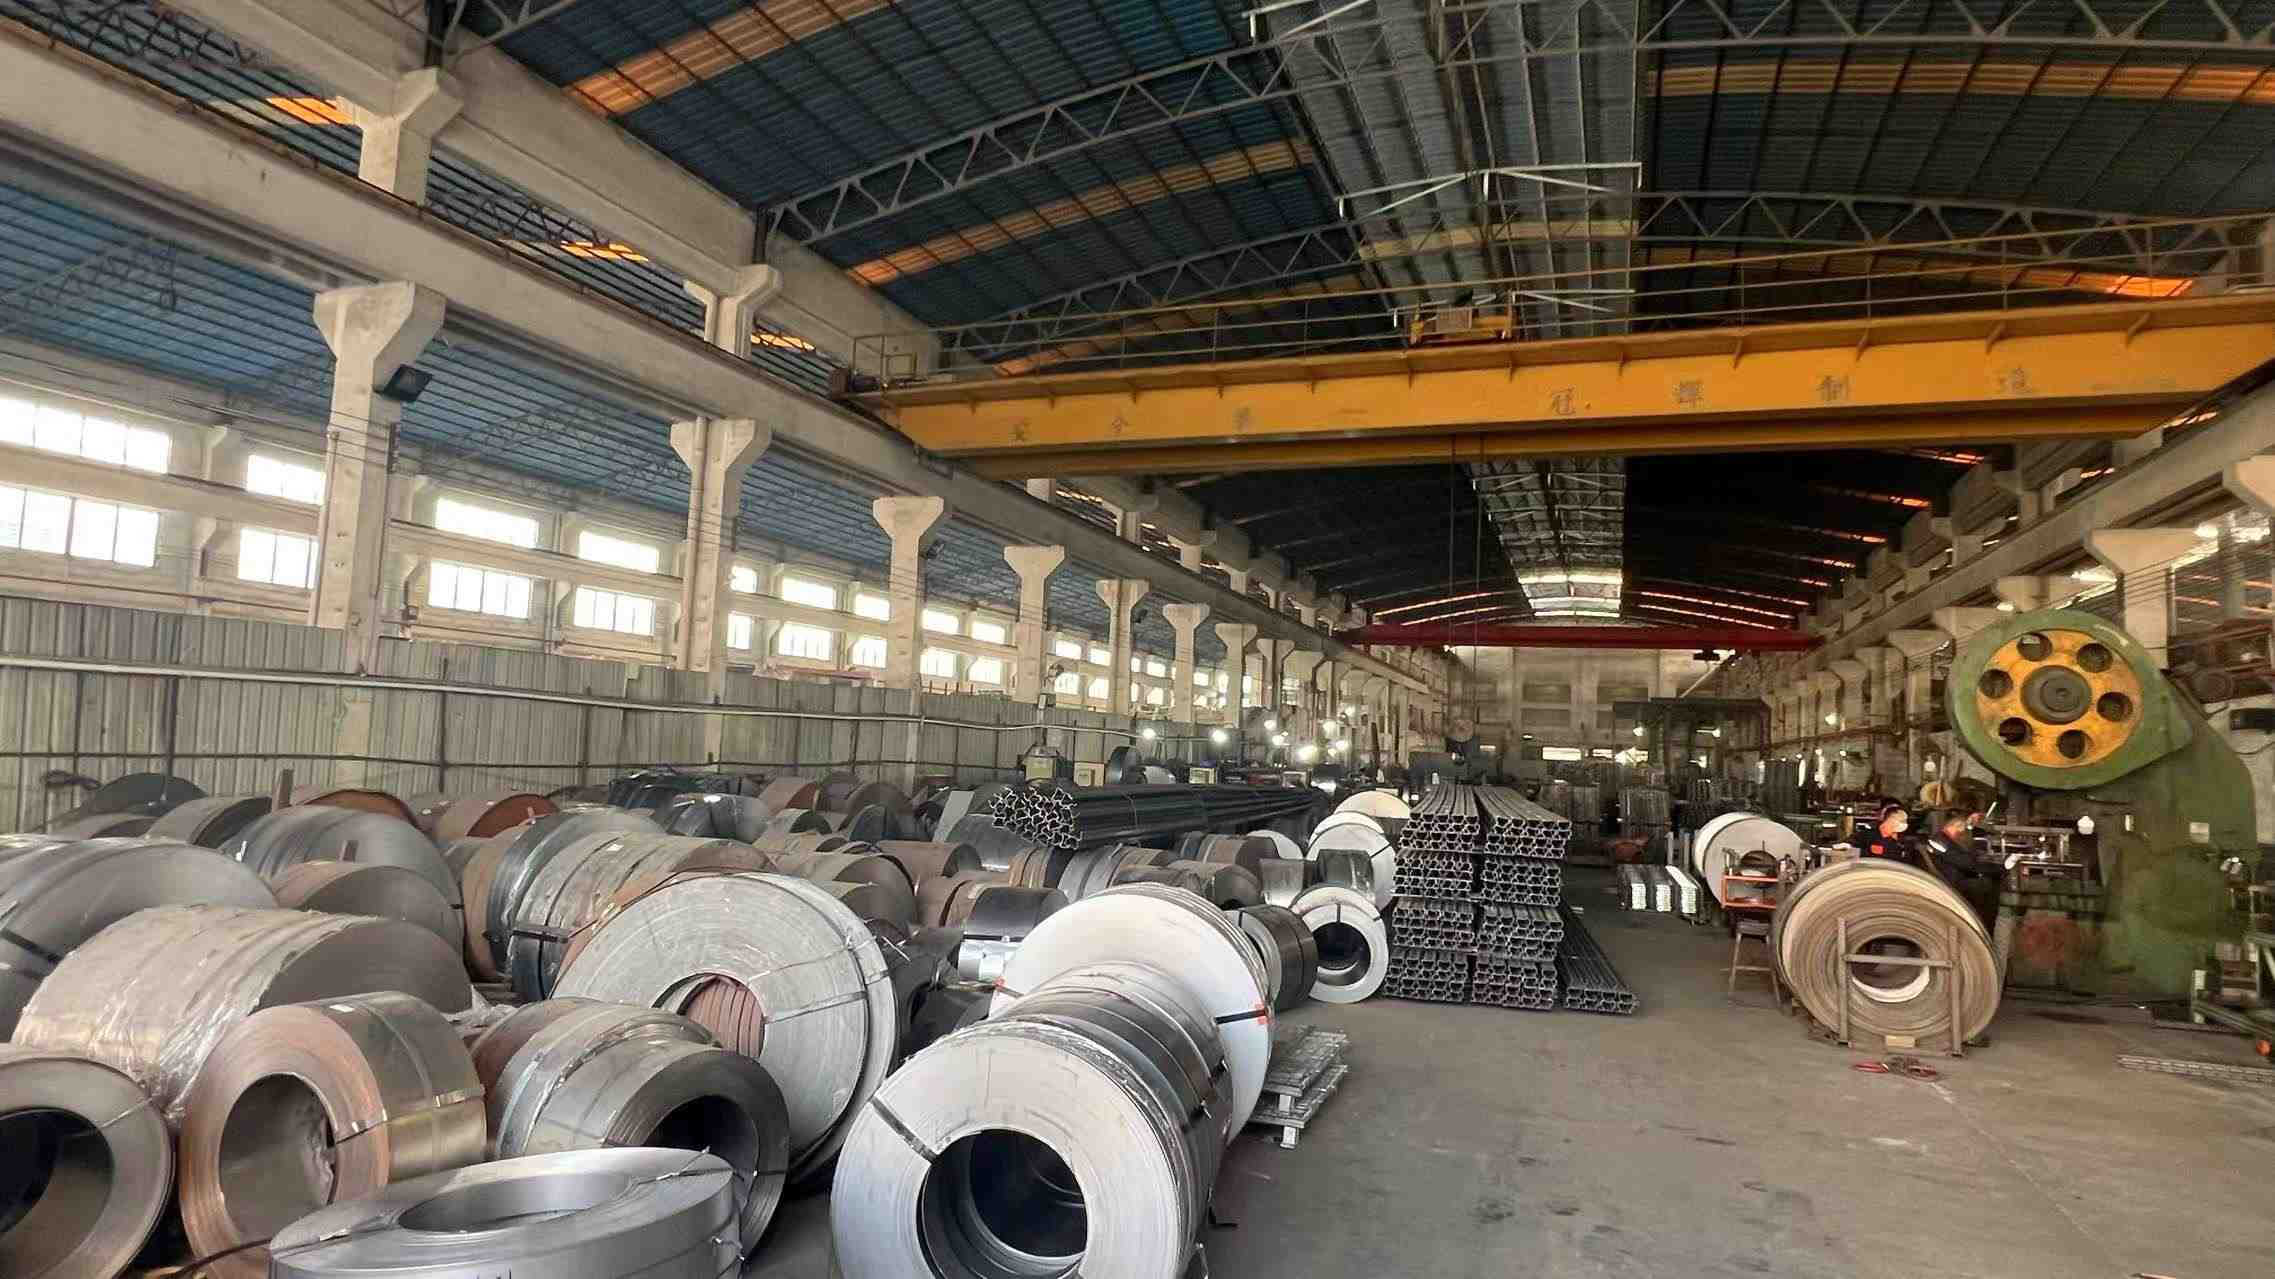
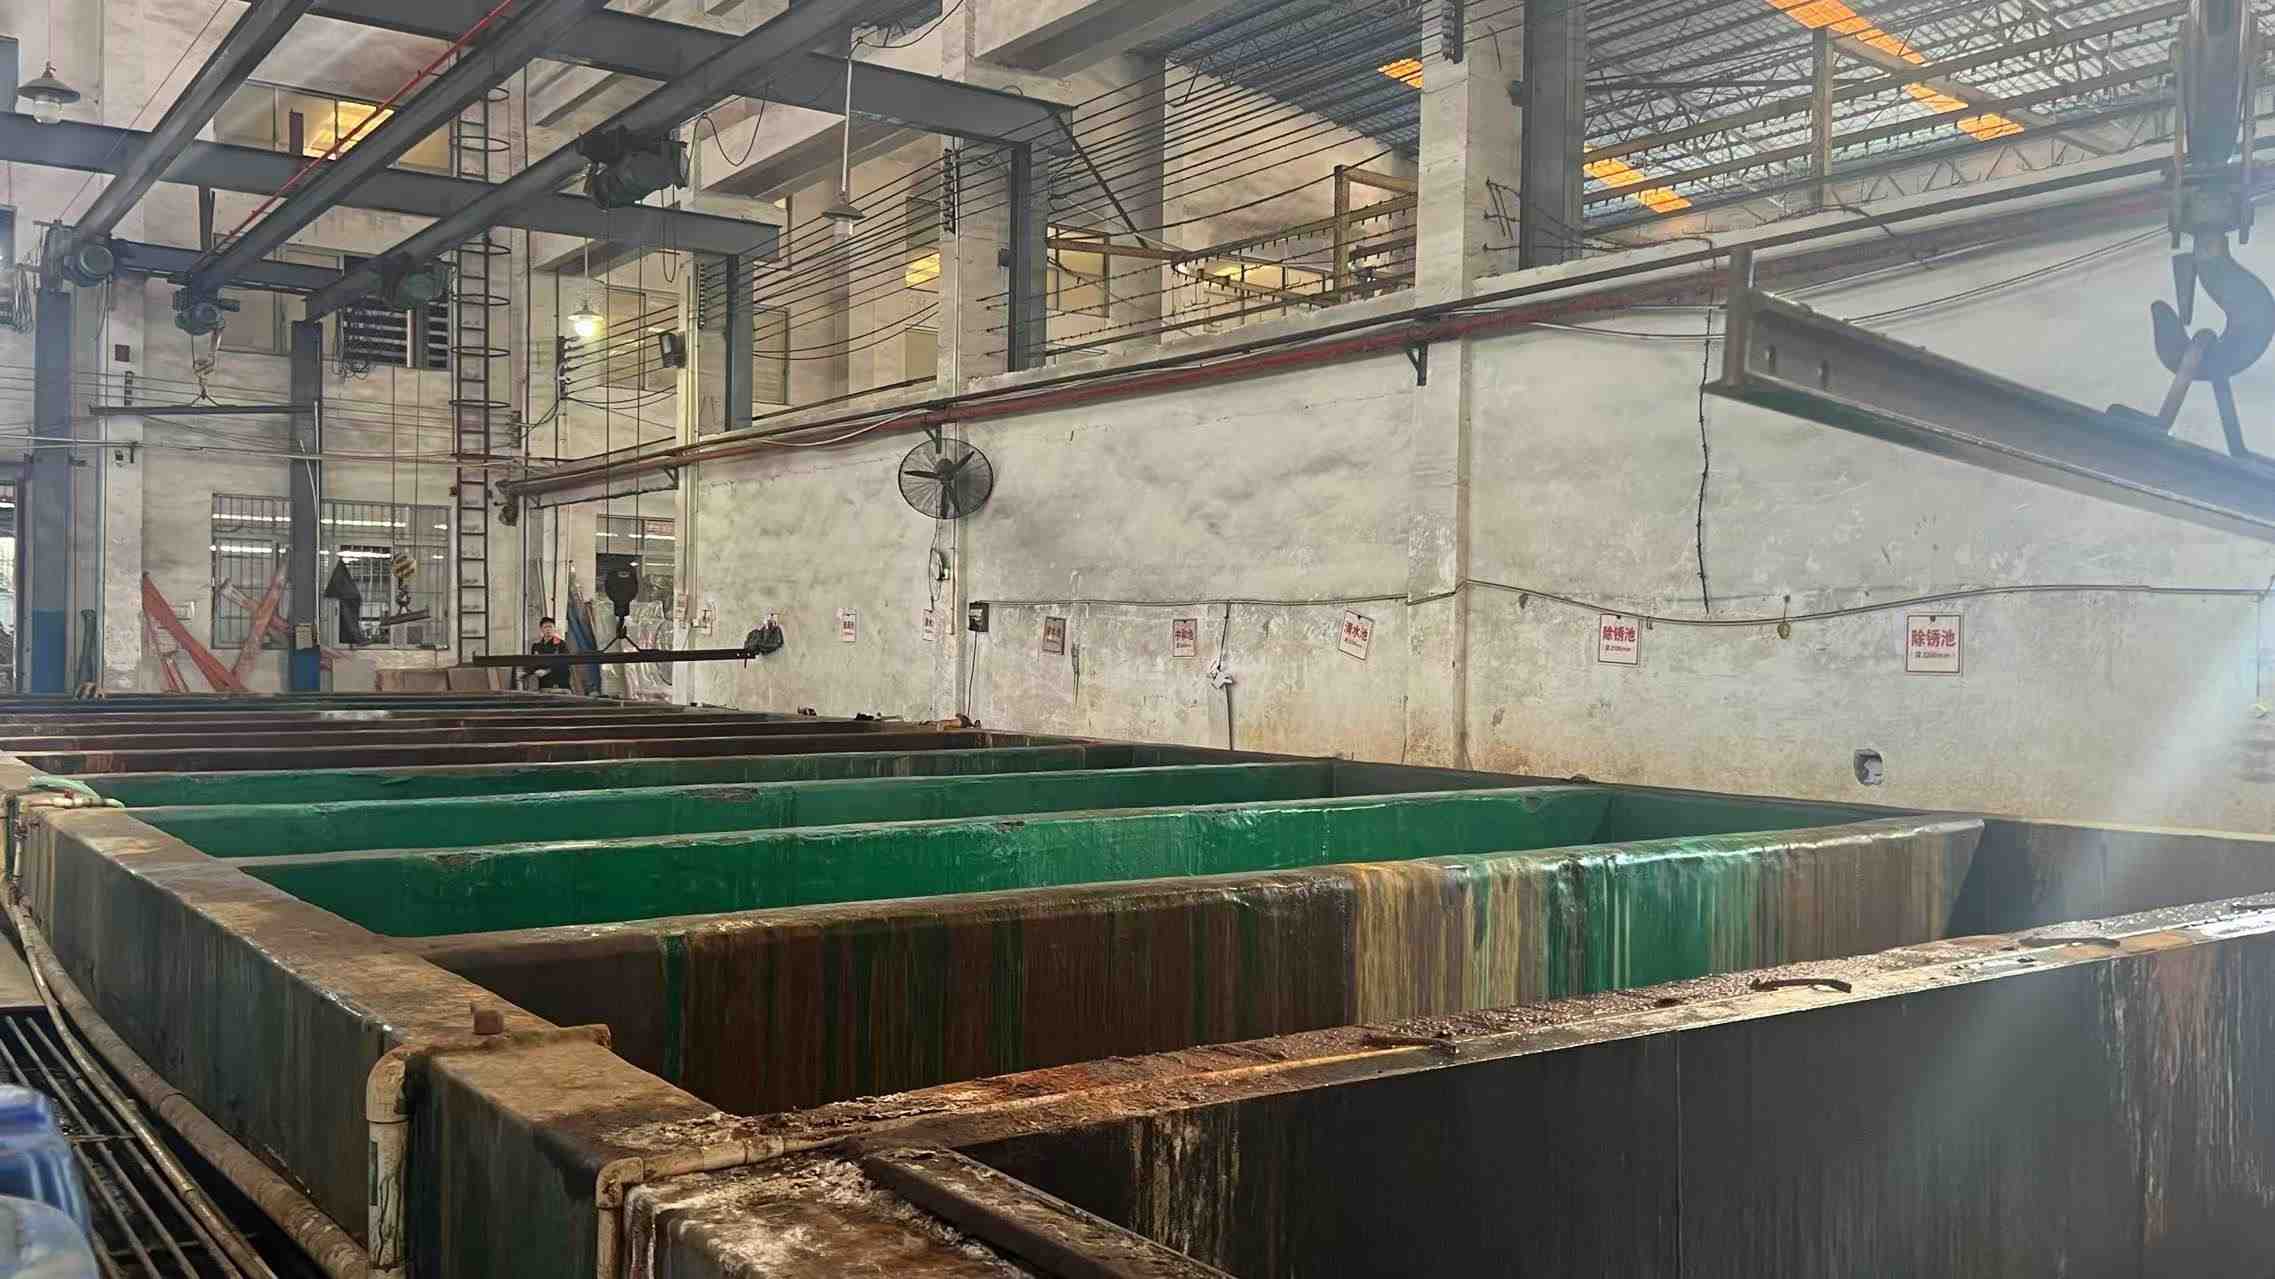
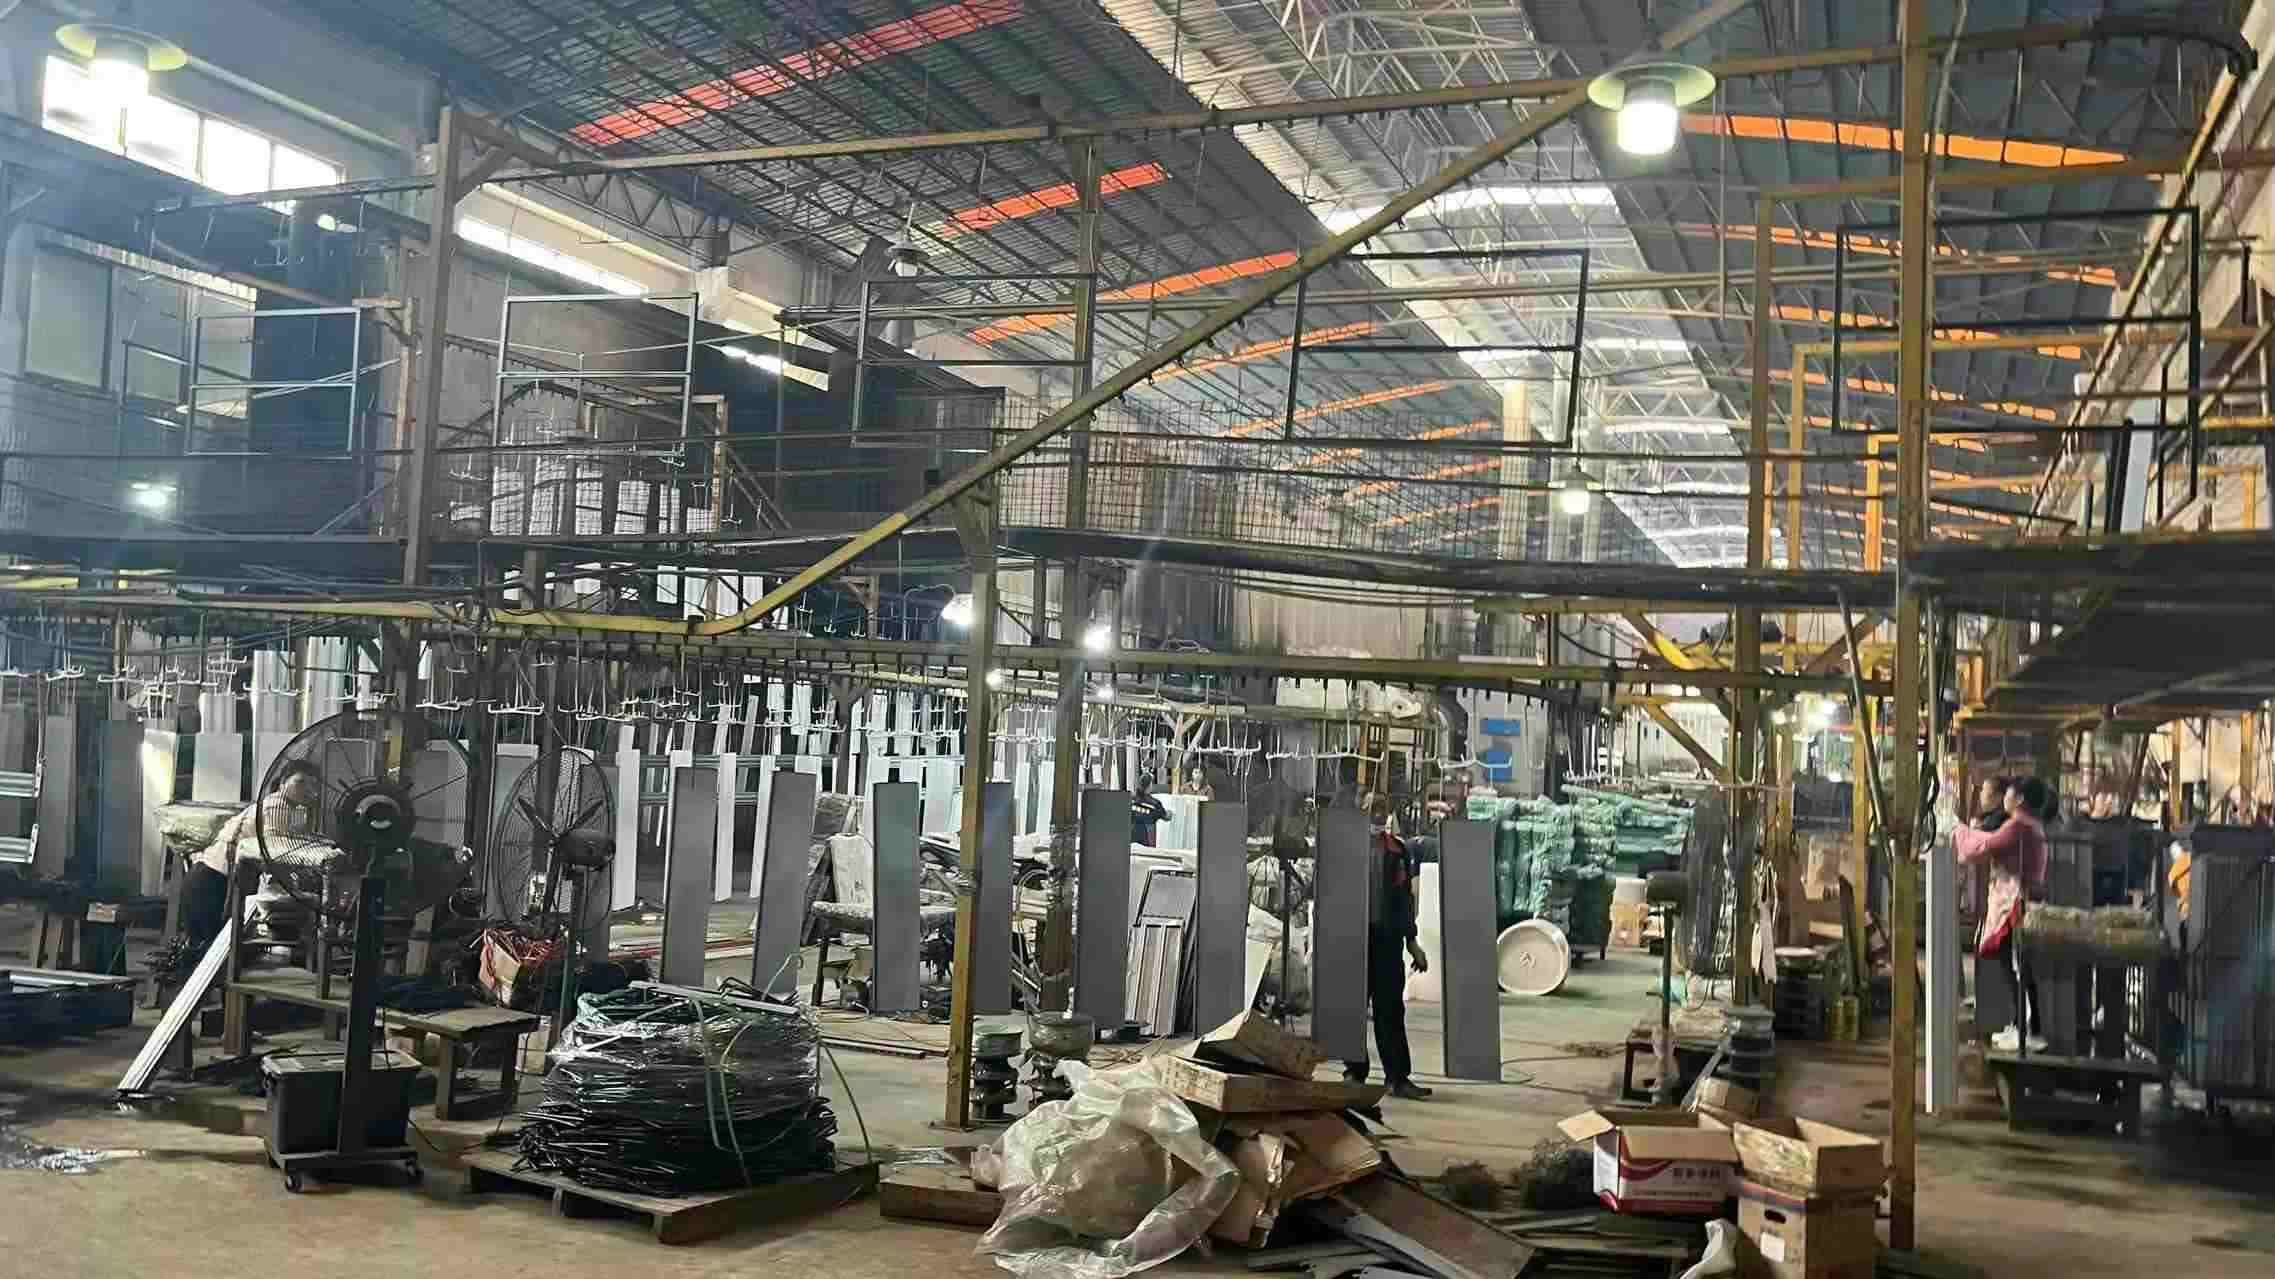
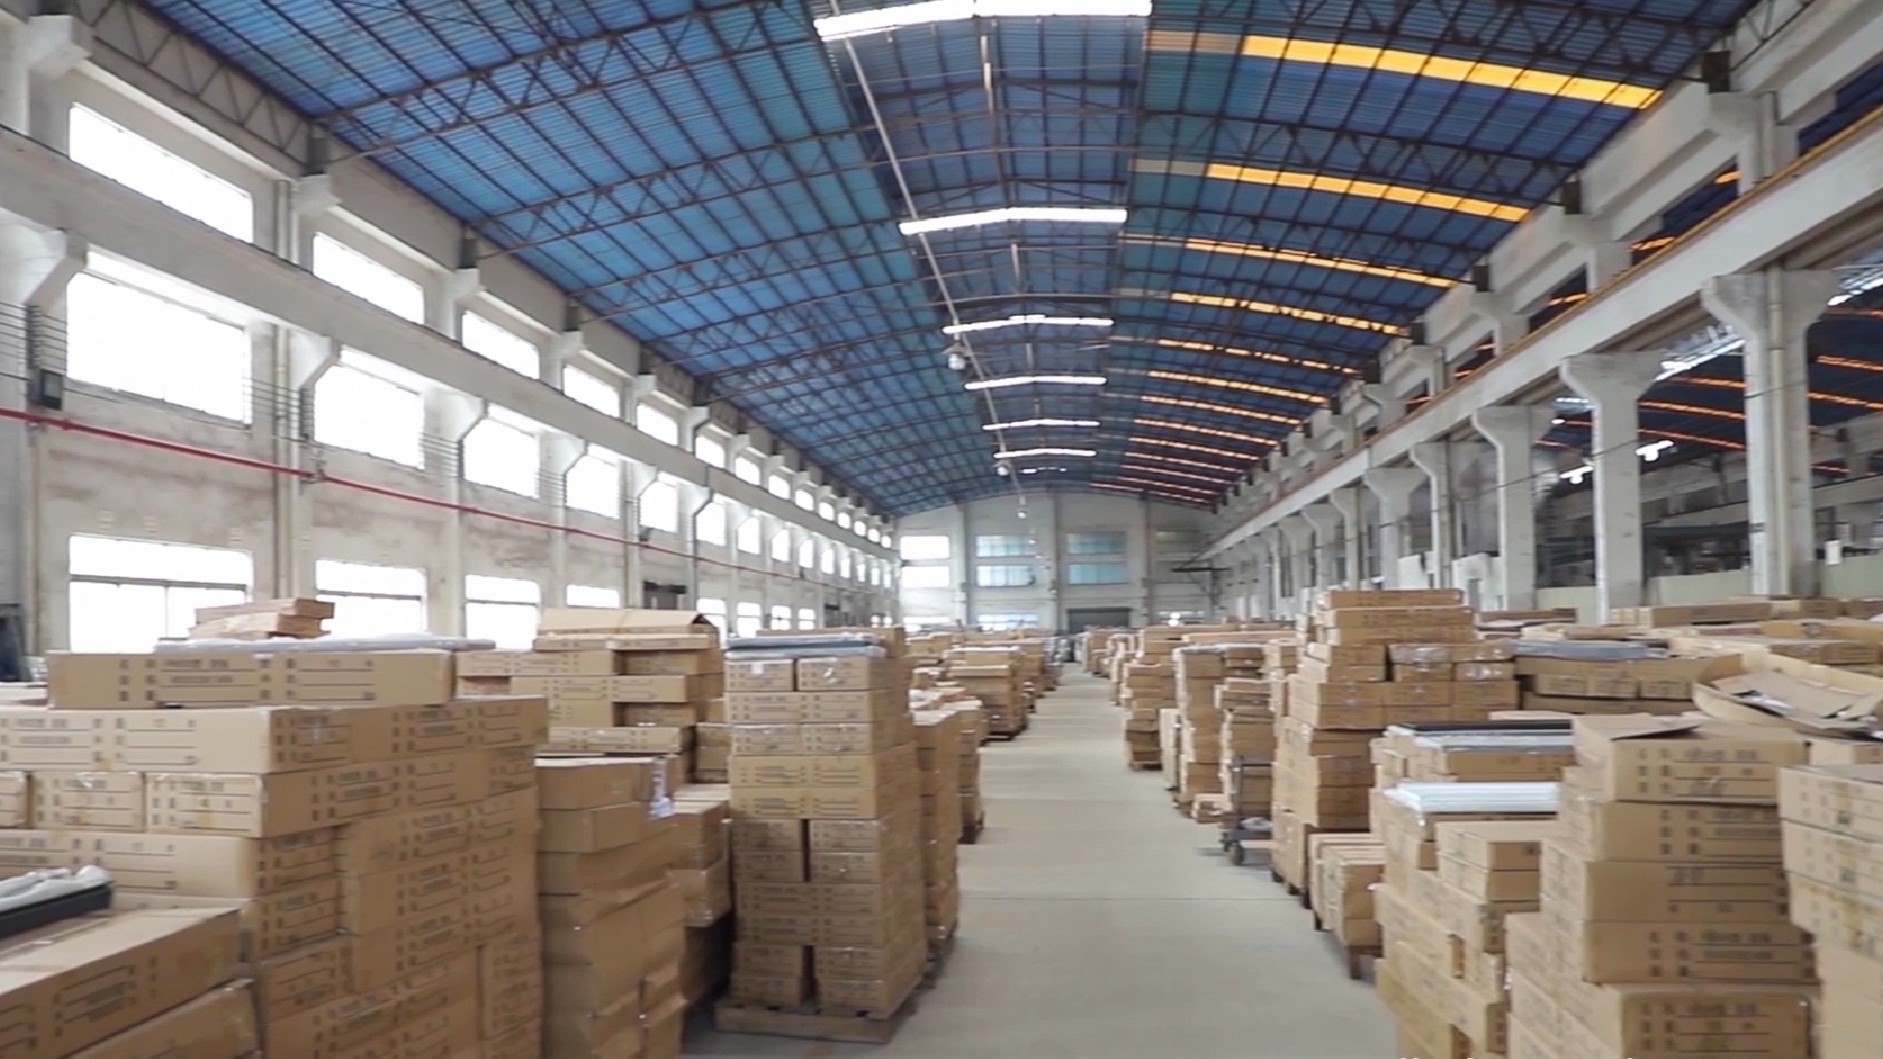
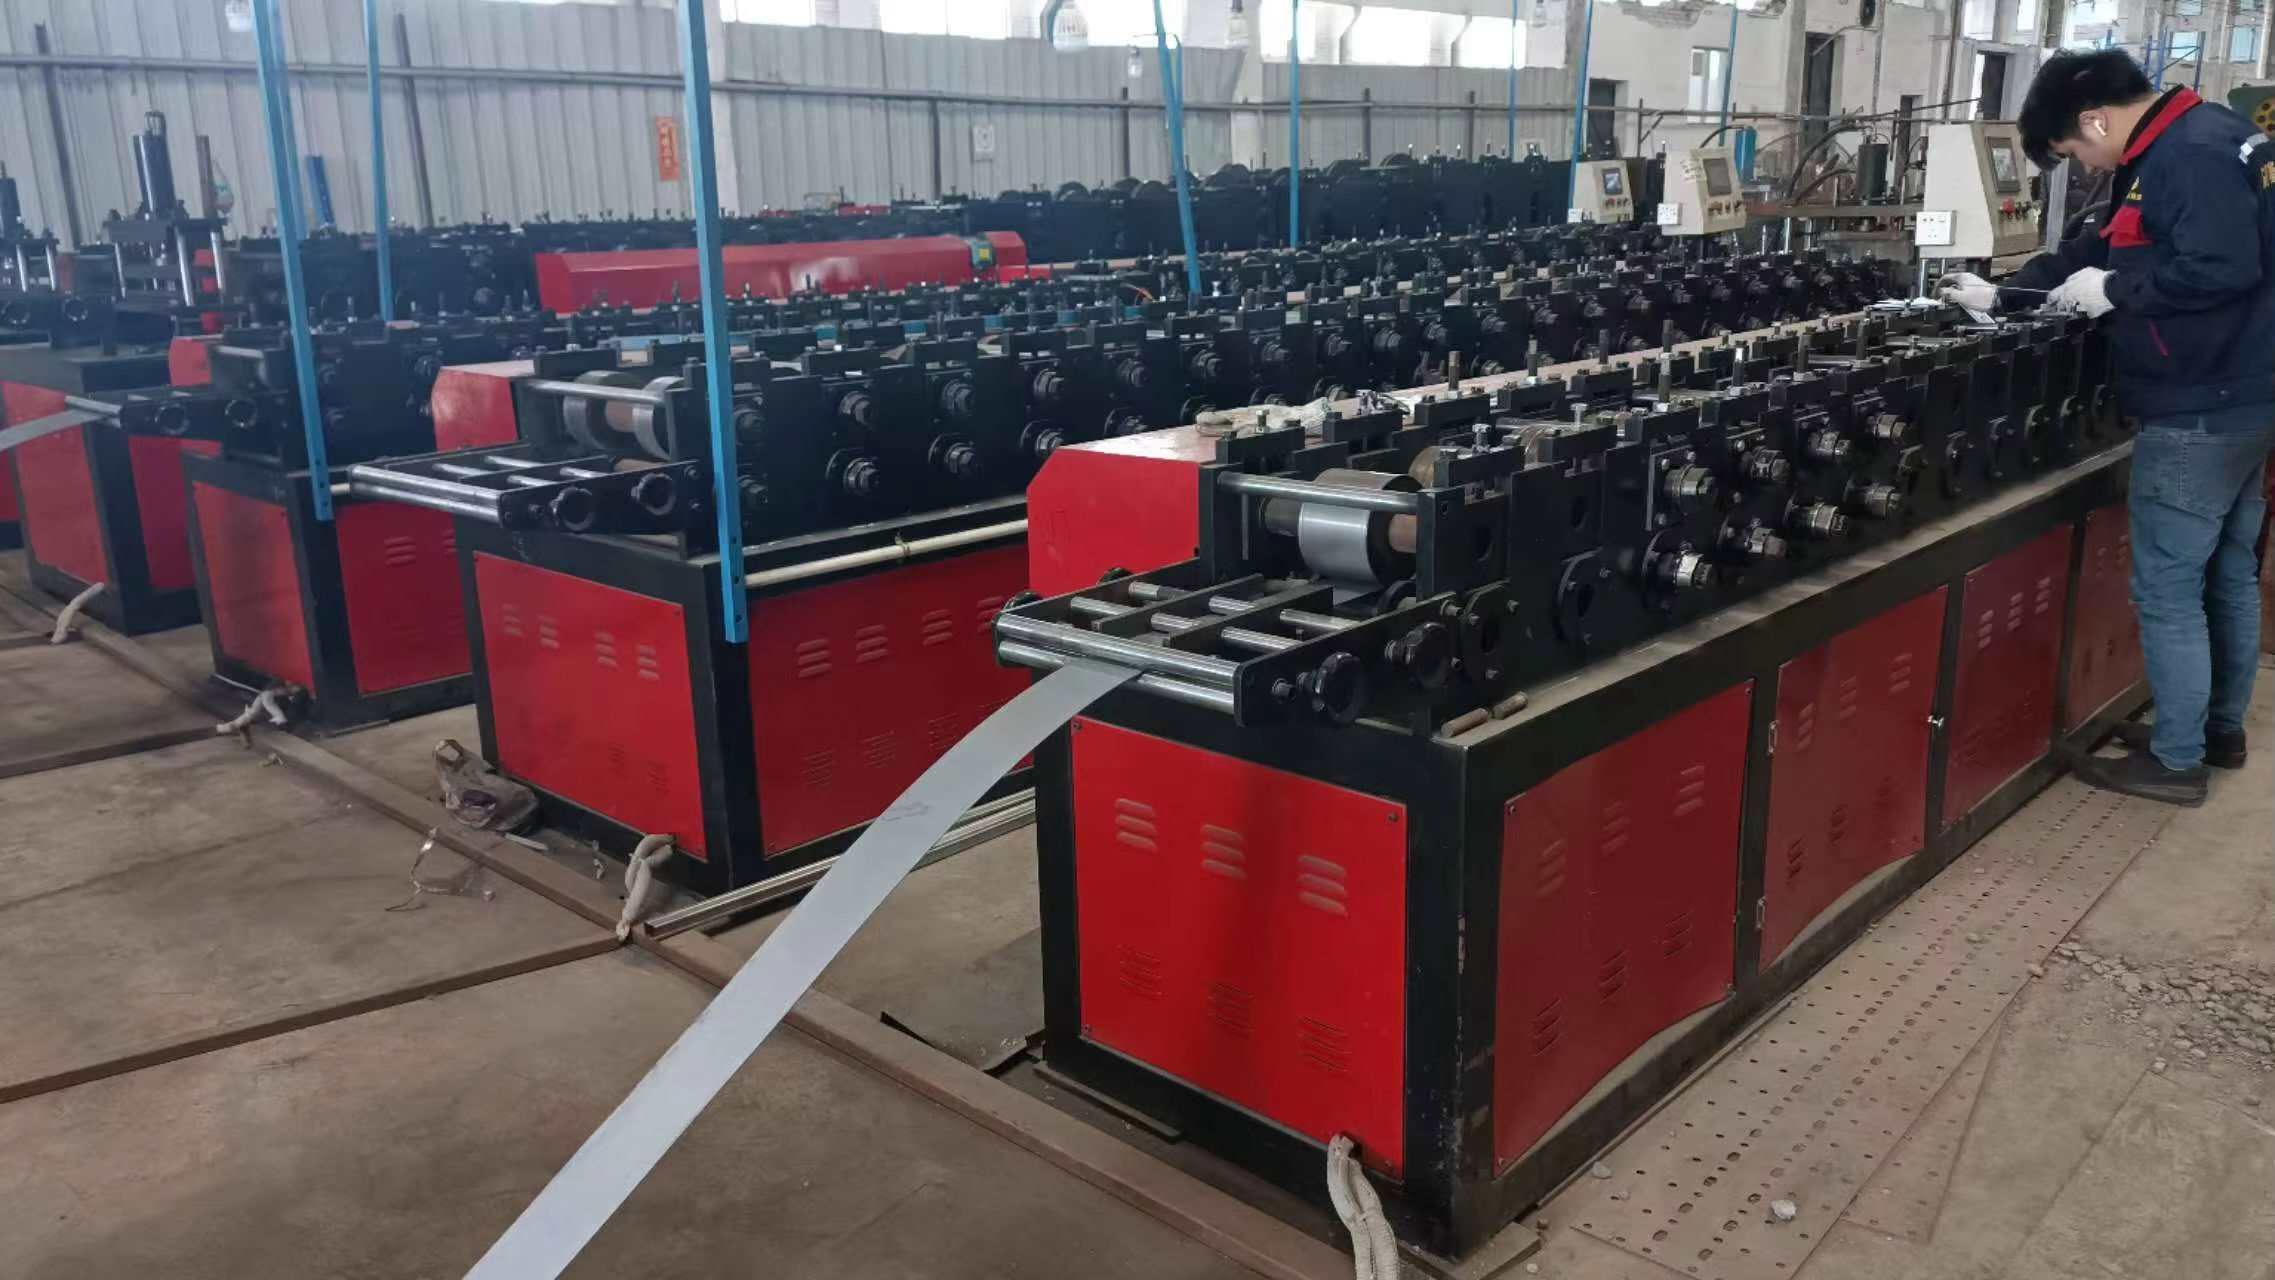
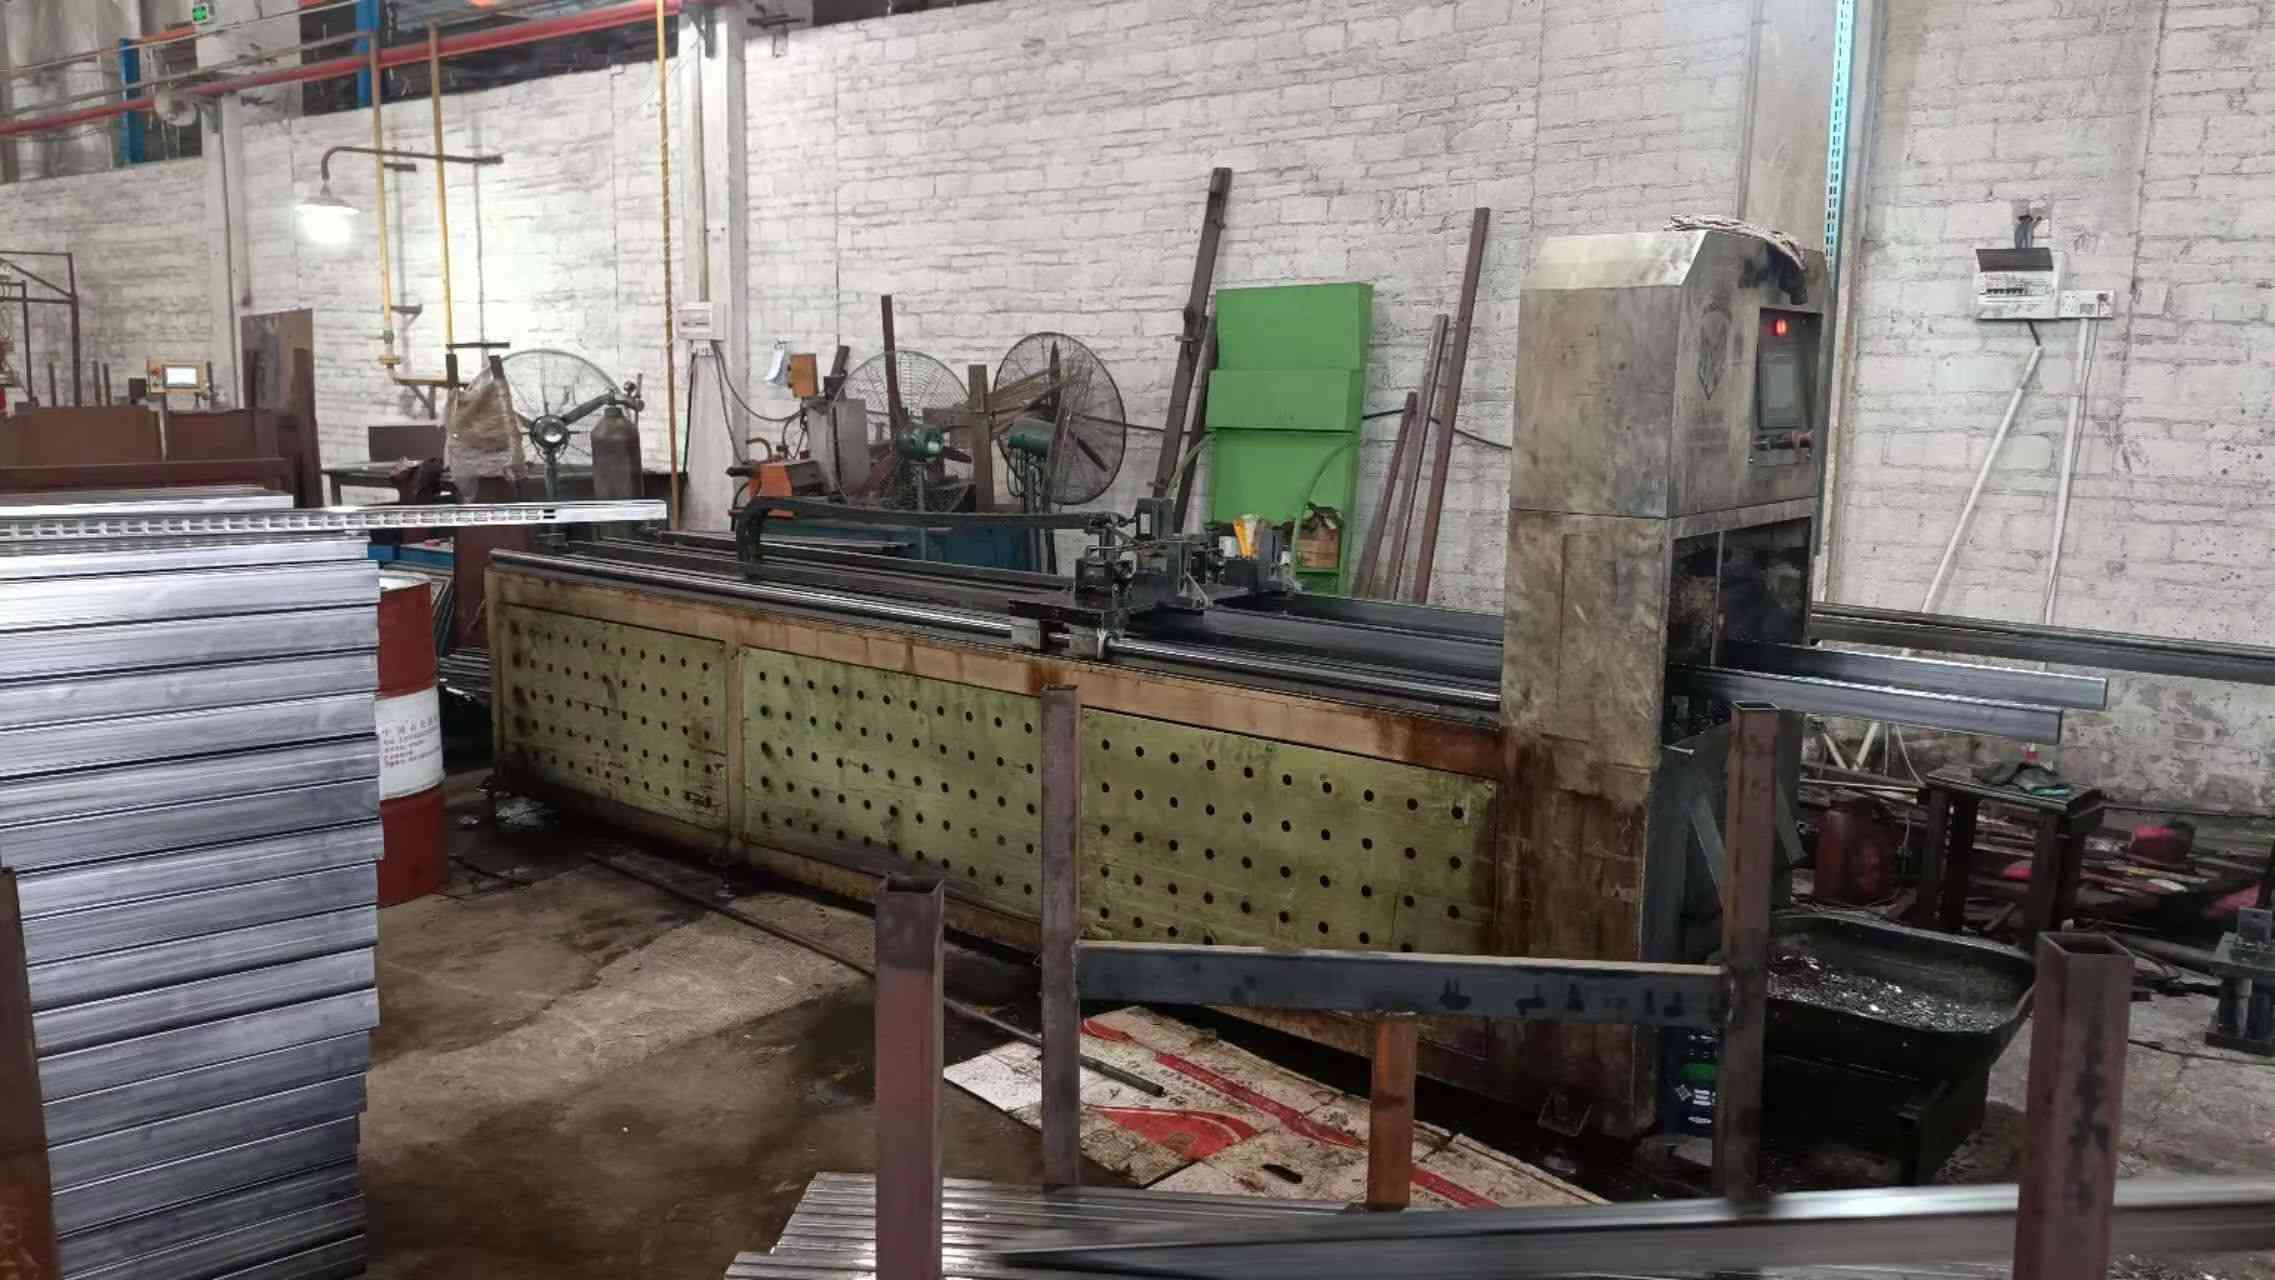
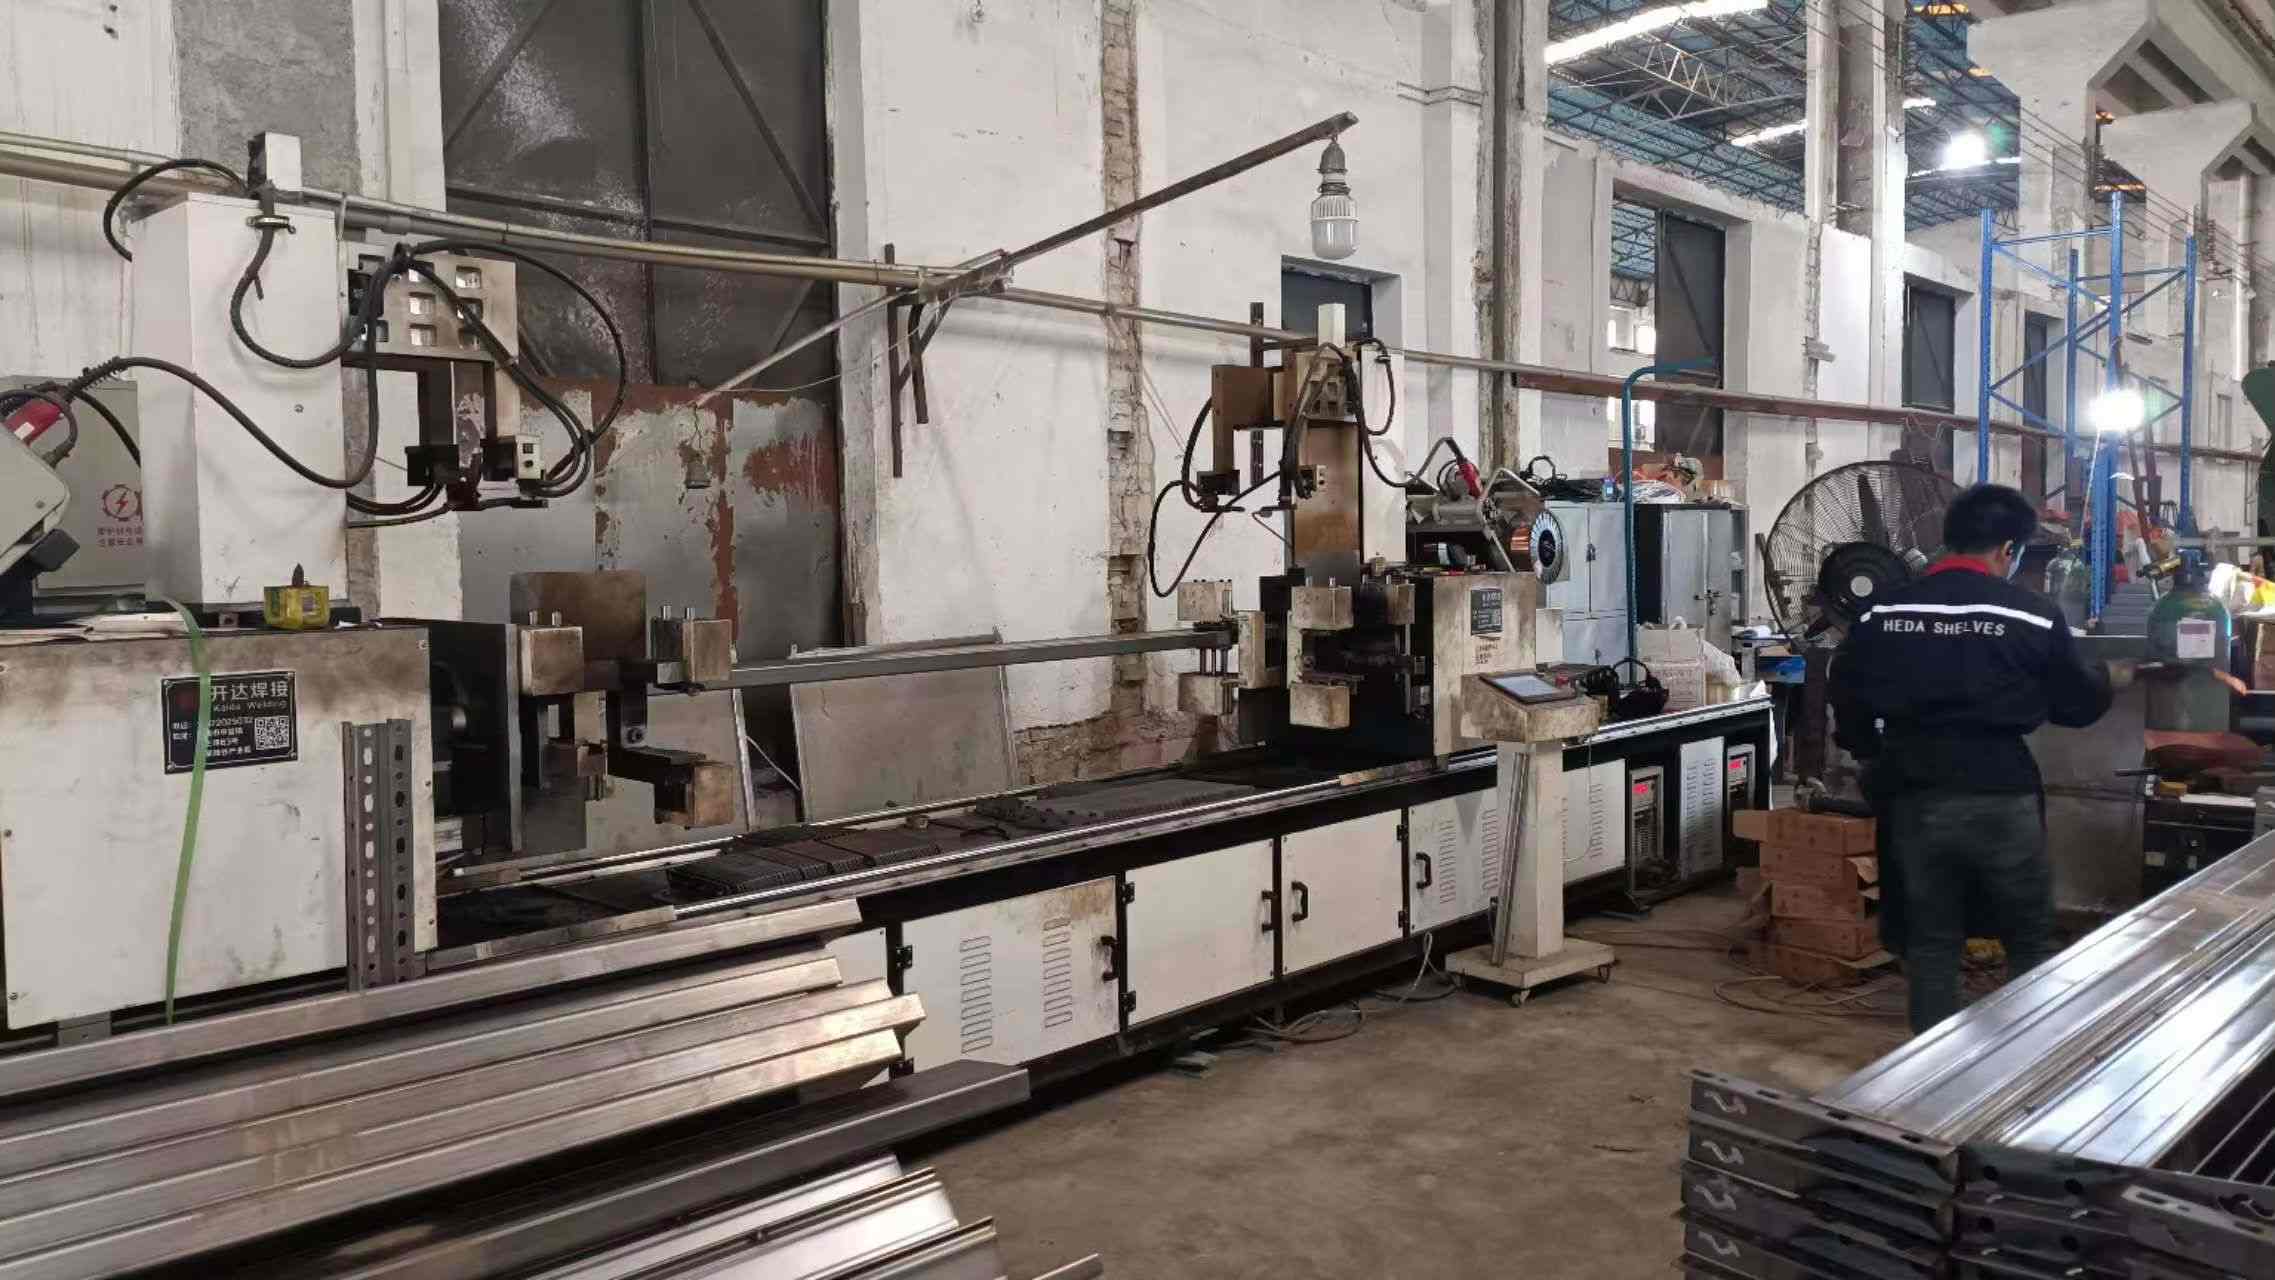
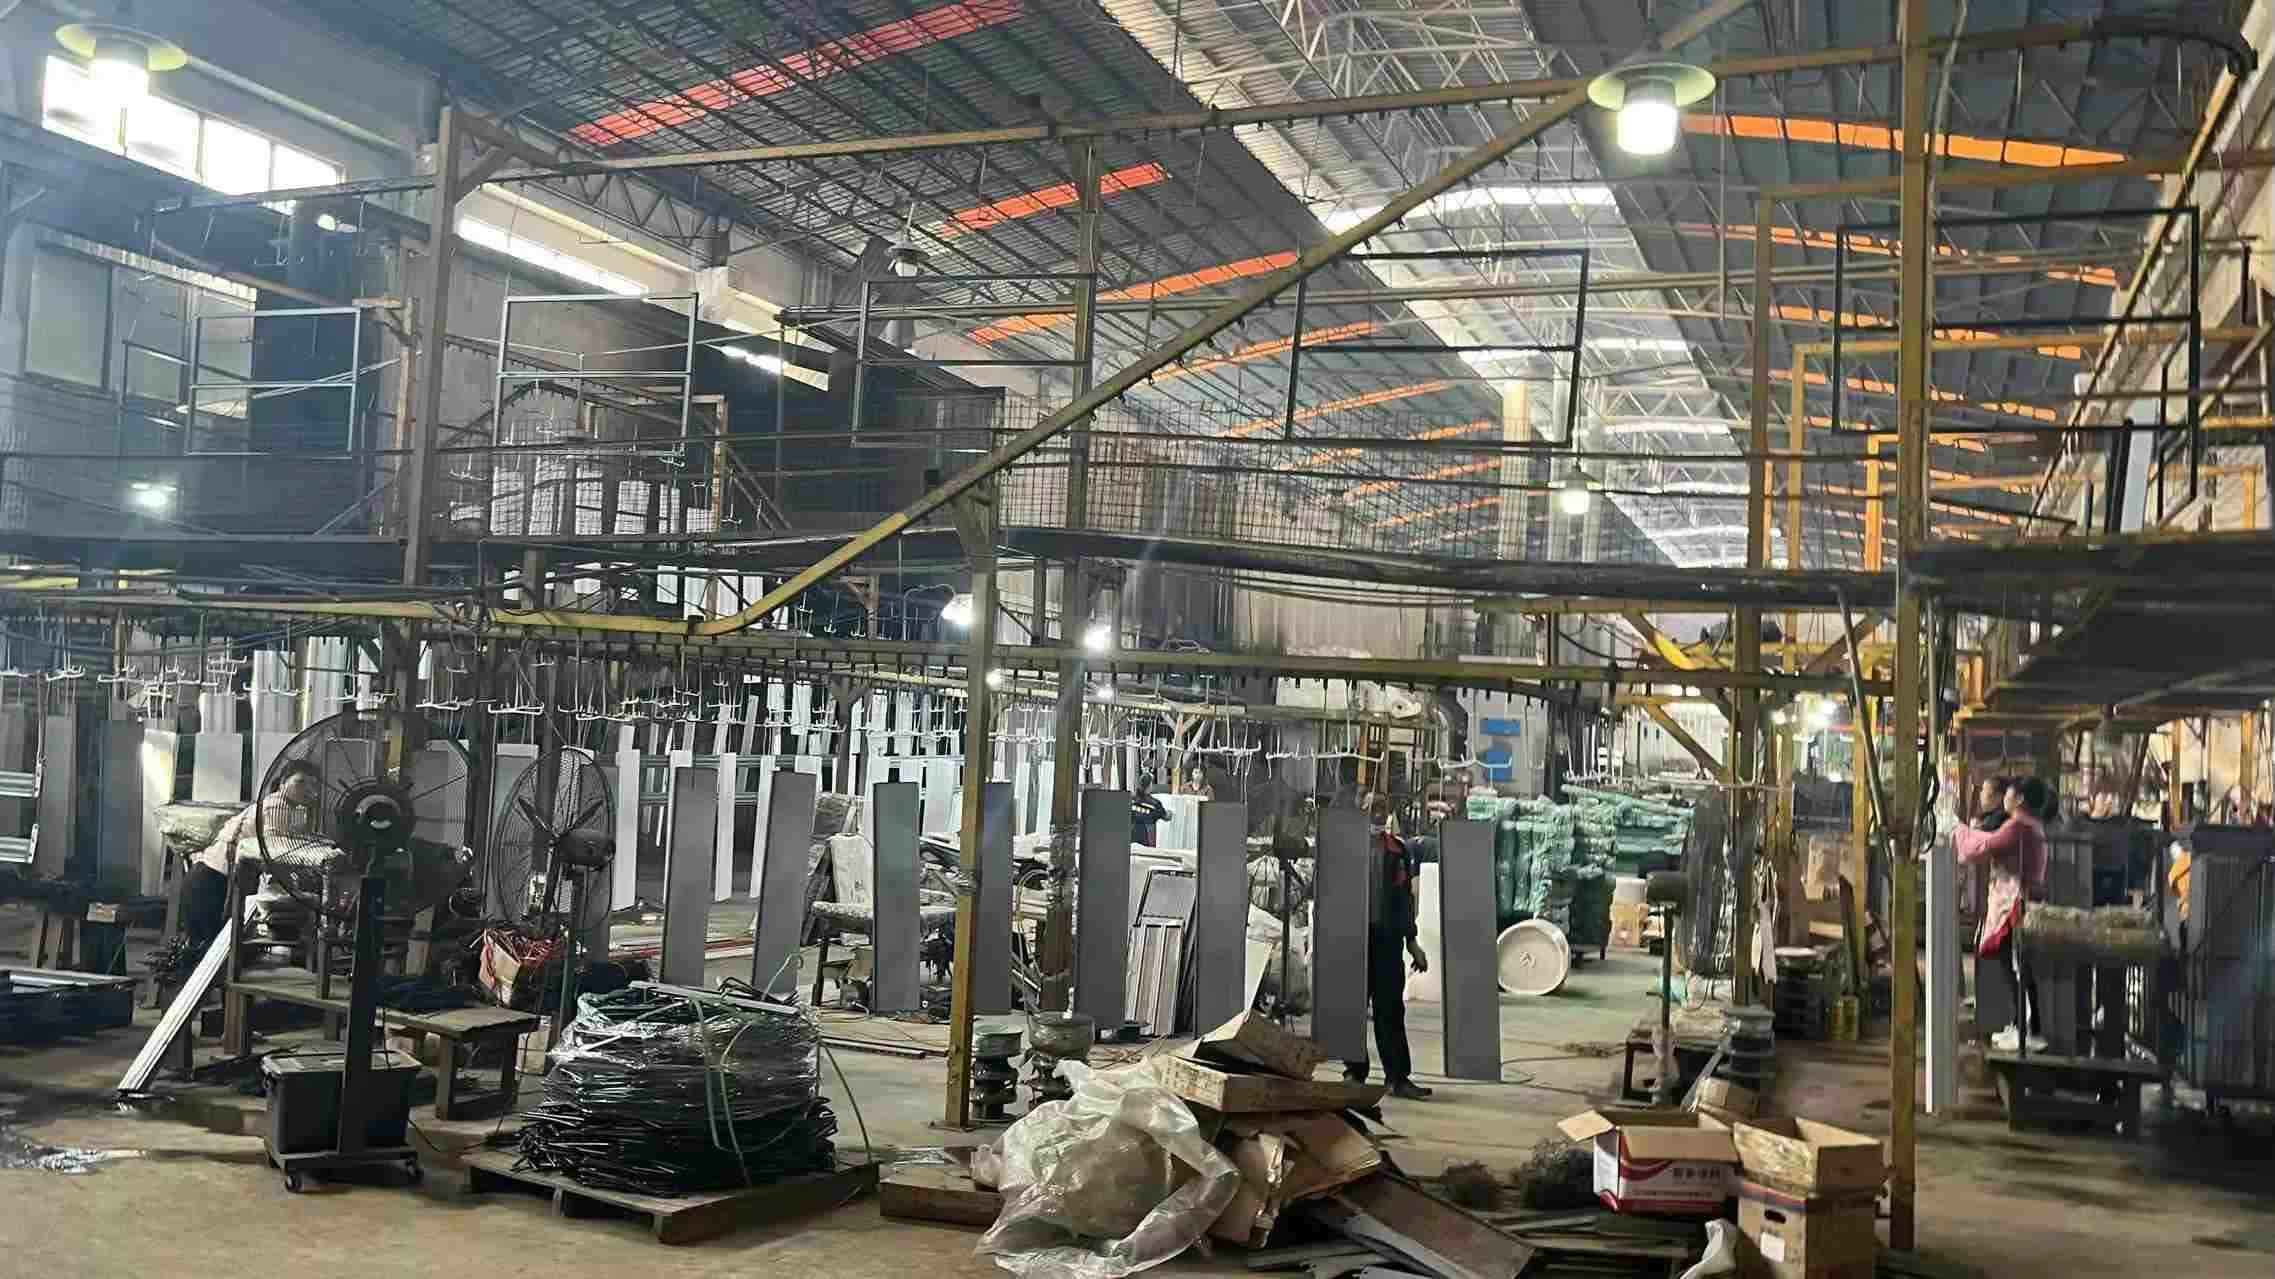
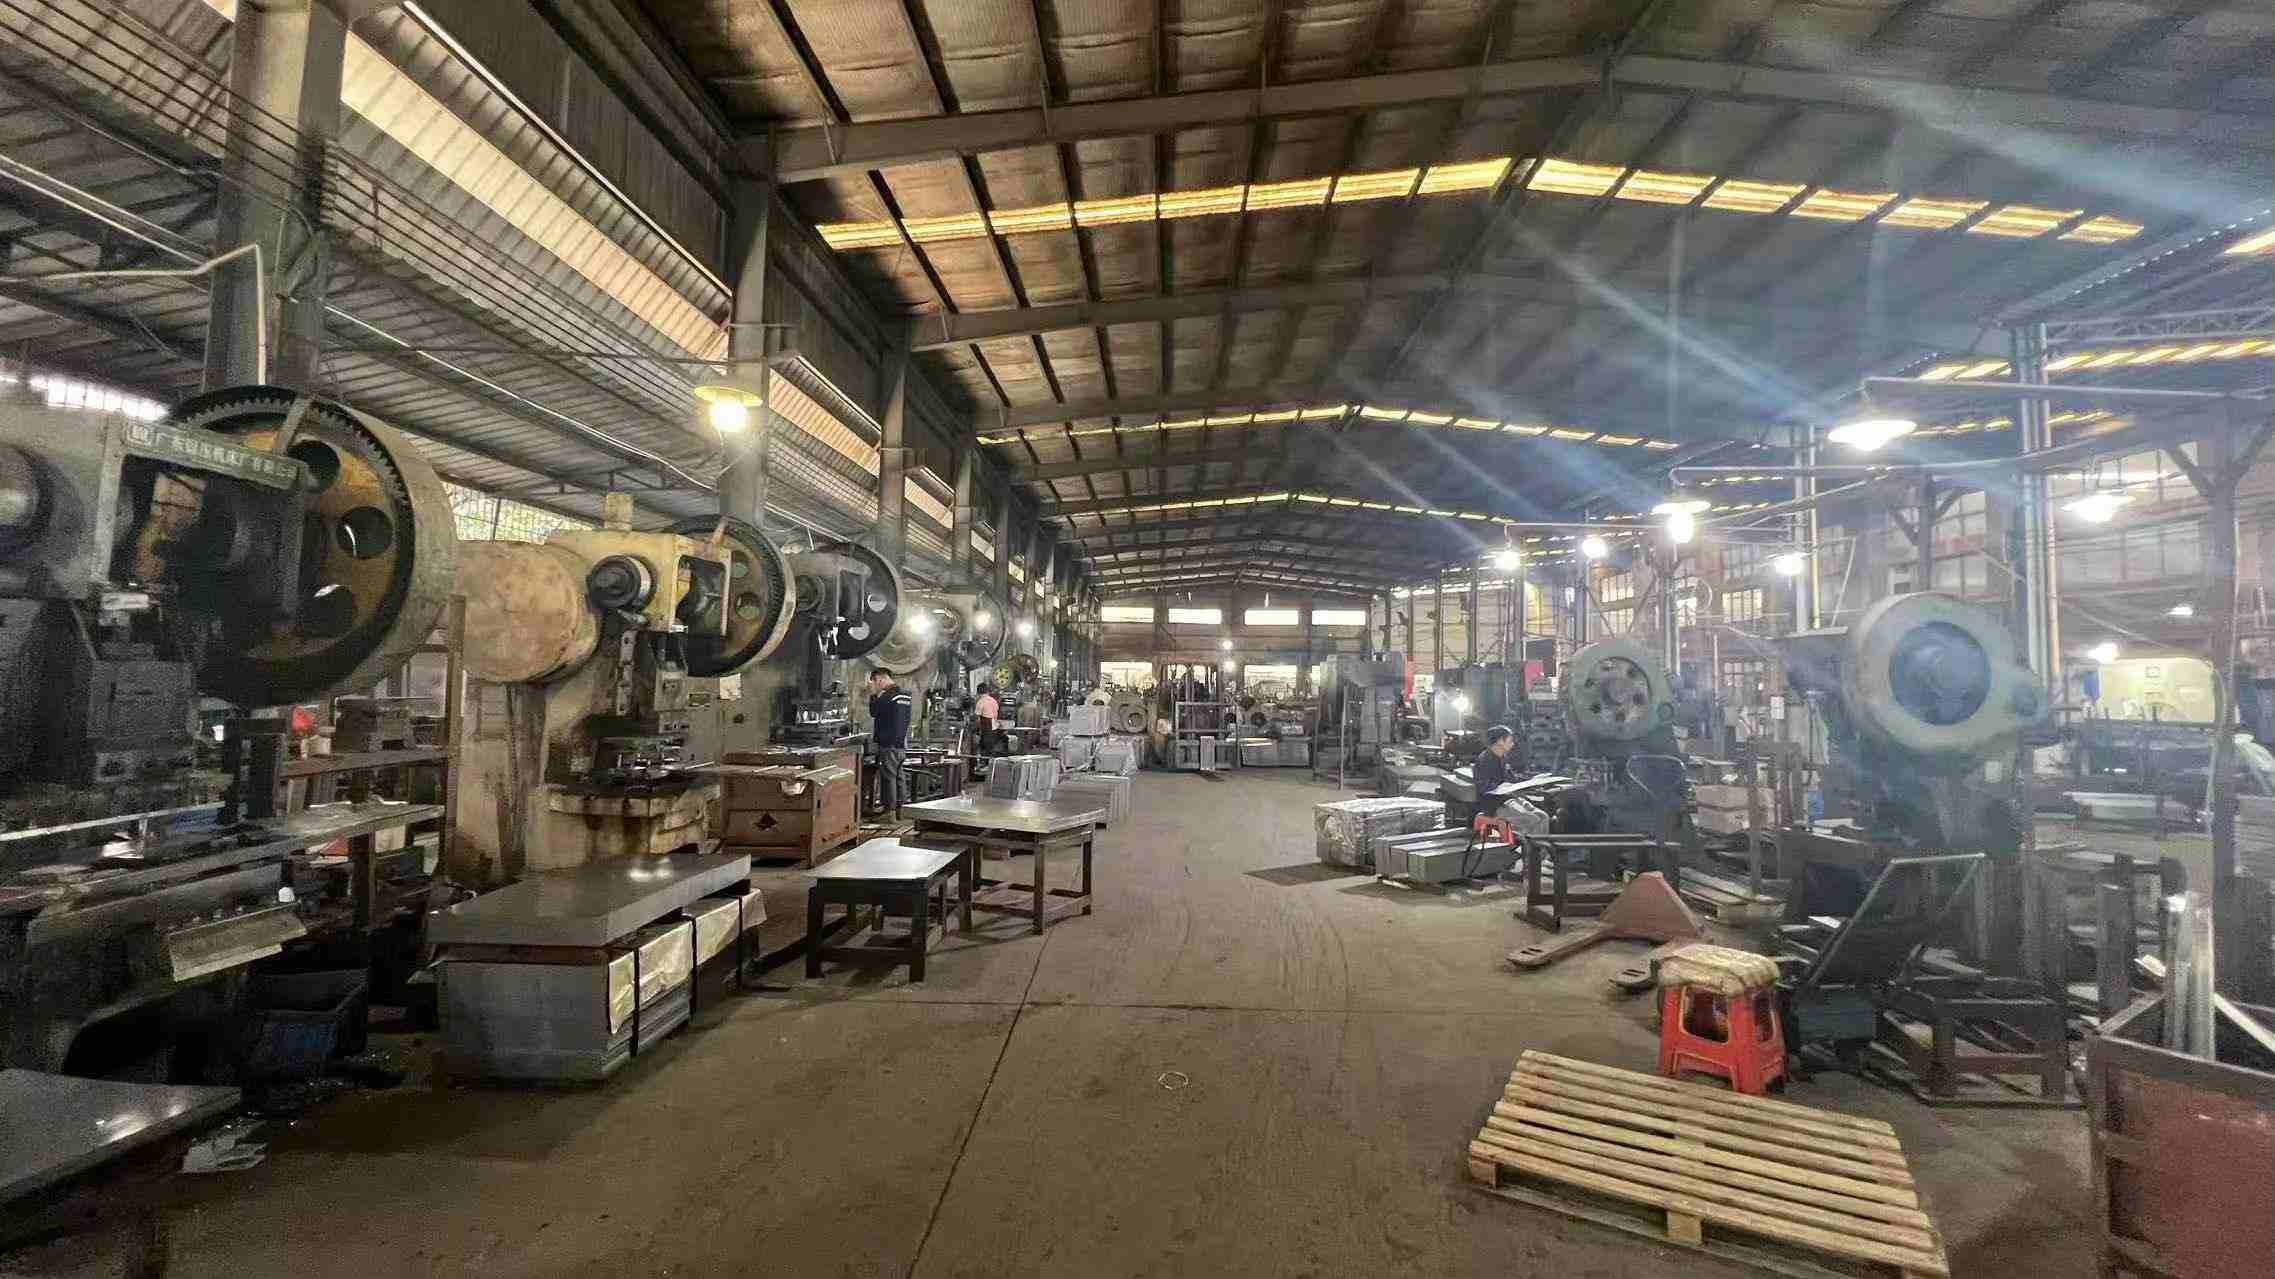
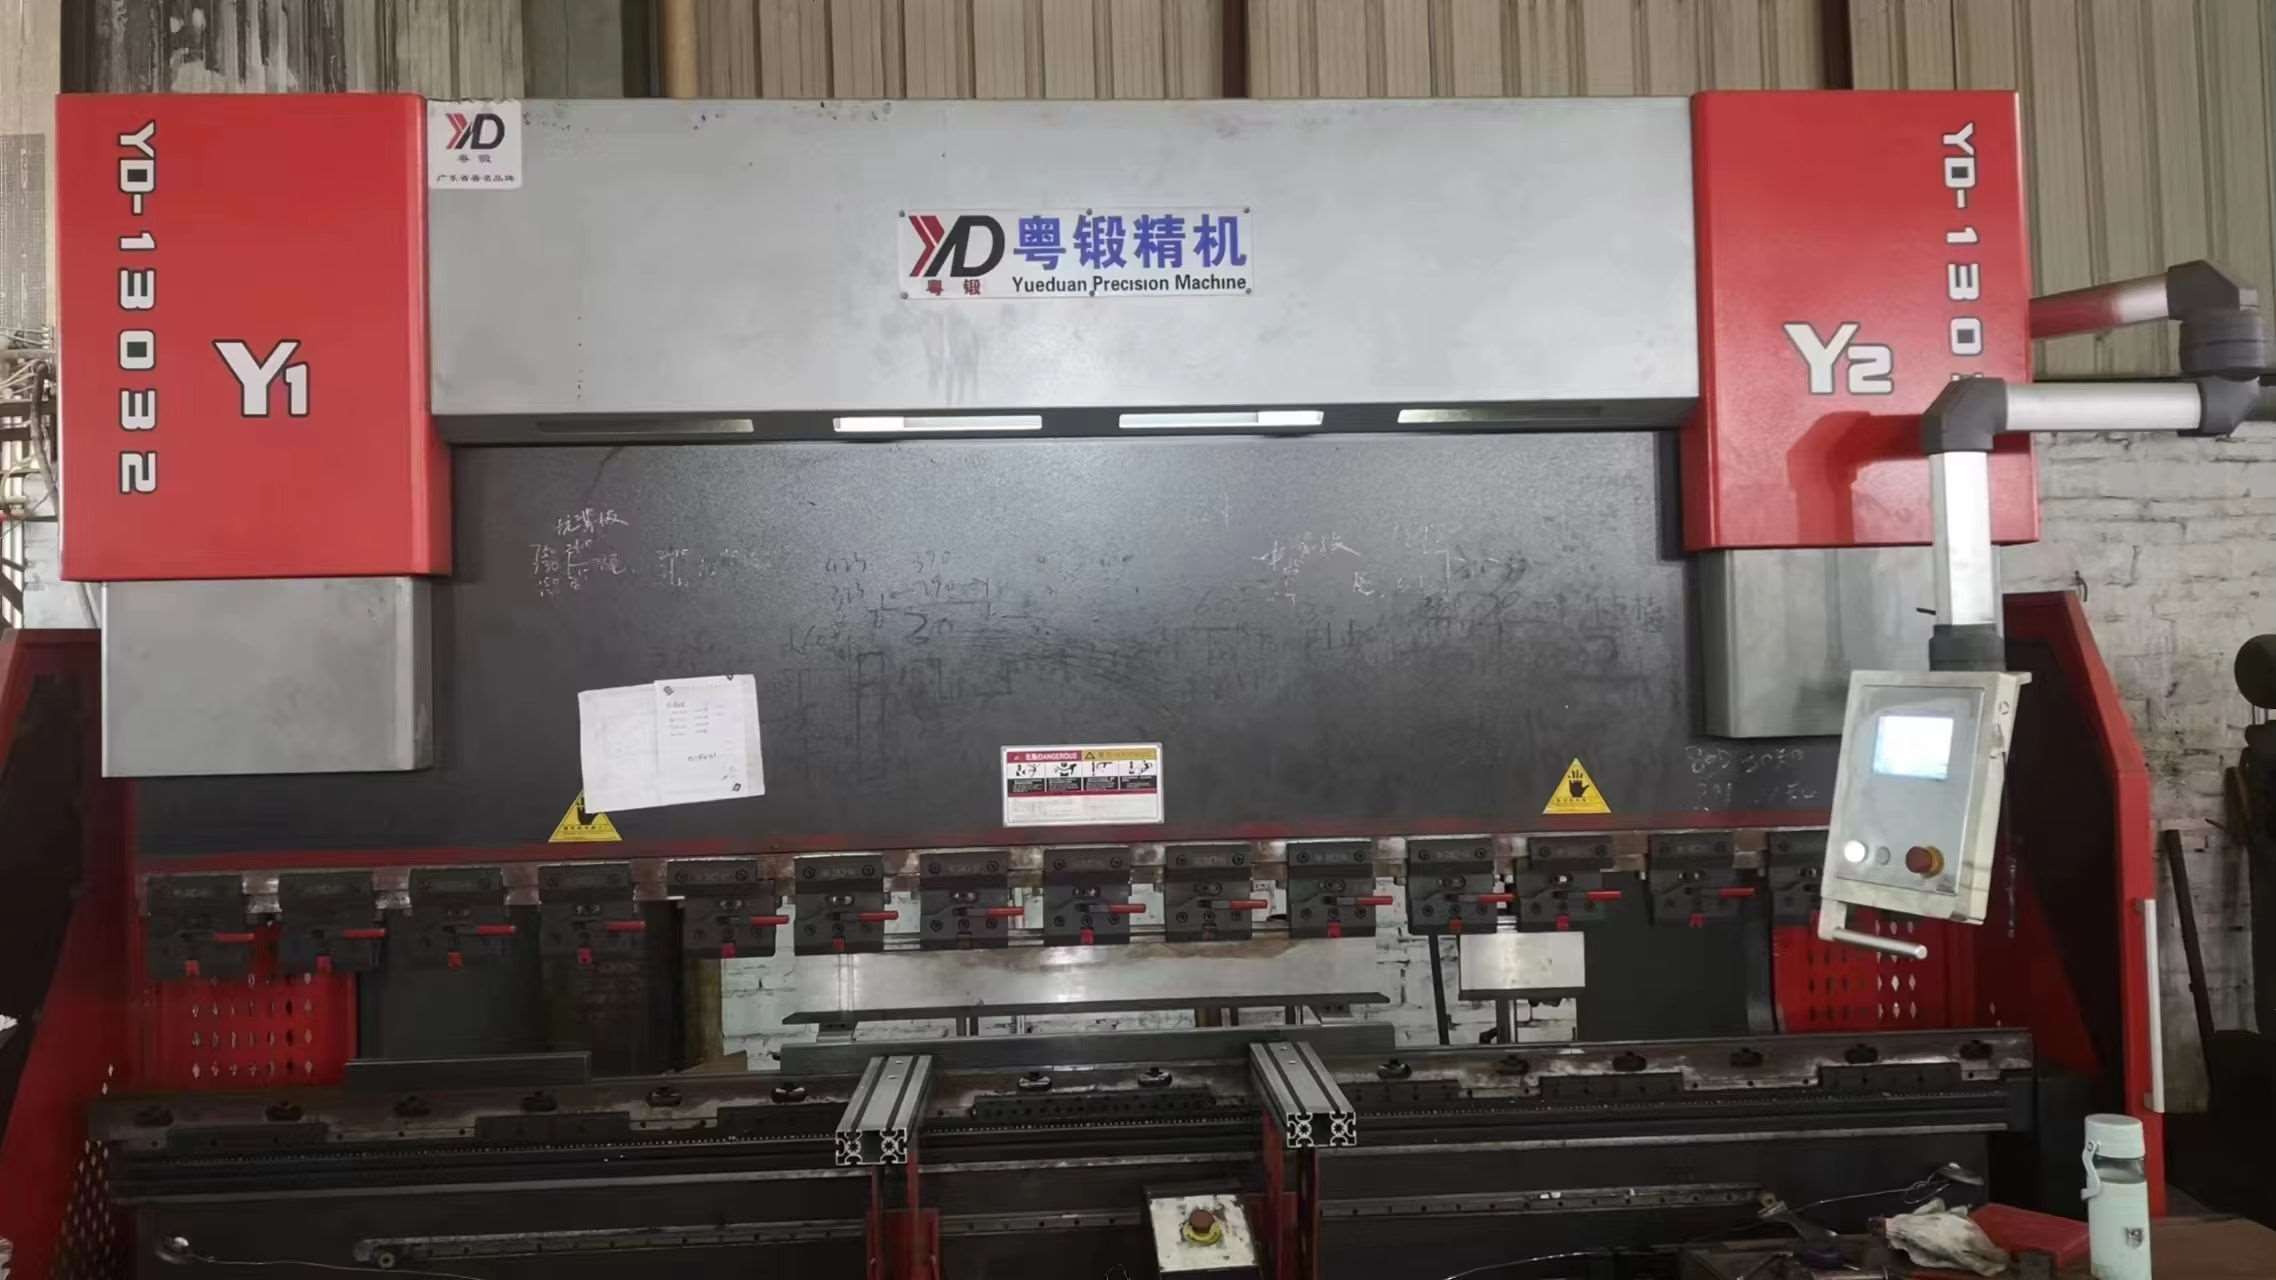
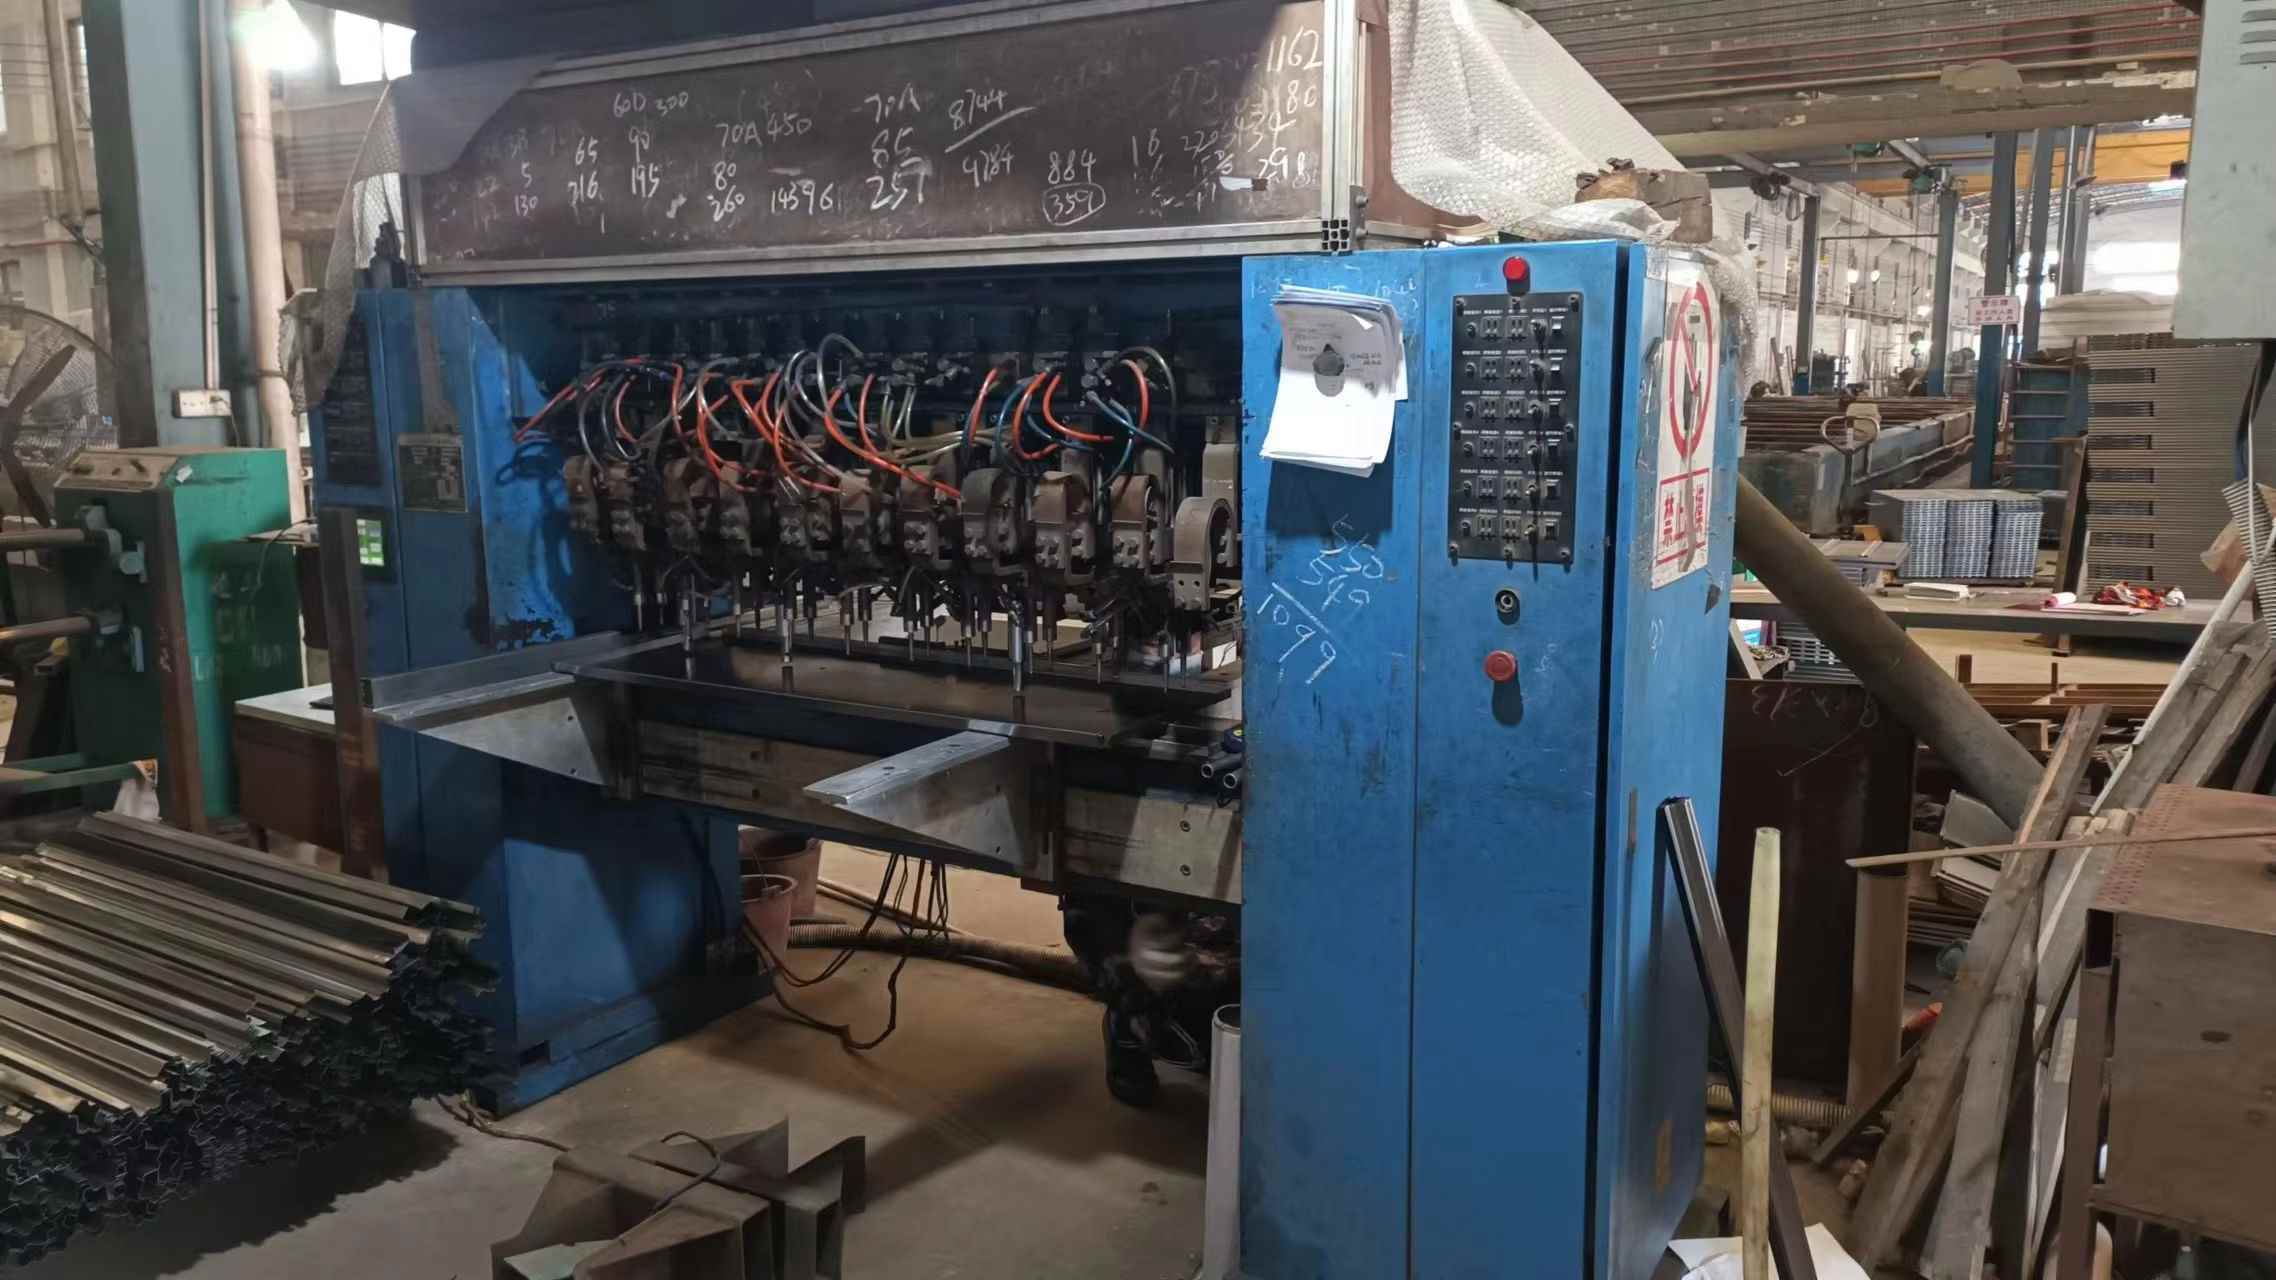
Leveraging Guangzhou/Shenzhen automated manufacturing scale to lower total landed costs and accelerate project completion timetables.
By eliminating middle-tier brokers and trading markups, HEDA provides direct factory-gate pricing. Grenville importers benefit from 20%-35% cost savings on major commercial racking procurement projects.
Our integrated raw material procurement network guarantees continuous access to premium cold-rolled steel coils, custom hardware fittings, wire mesh decking, and acrylic retail accessories without supply bottleneck delays.
Engineered flat-pack packaging protocols ensure maximum container volumetric filling (CBM optimization), minimizing ocean freight shipping costs per unit directly to Grenville port destinations.
Integrating IoT intelligence, lightweight structural alloys, and micro-fulfillment mechanics into retail shelf infrastructure.
HEDA is actively prototyping smart shelf systems equipped with sub-shelf load cells and RFID tracking channels. This enables real-time inventory monitoring, automated stock-out alerts, and loss prevention tracking for high-value supermarket items in modern retail hubs.
Transitioning to zero-VOC, heavy-metal-free thermosetting powder coatings with enhanced scratch resistance. Our latest formulation dramatically reduces friction wear during heavy pallet insertion while enhancing rust defense in humid environments like Grenville.
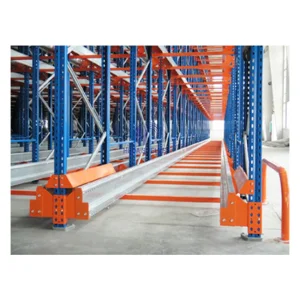
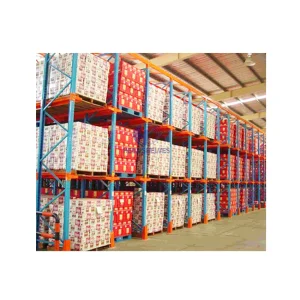
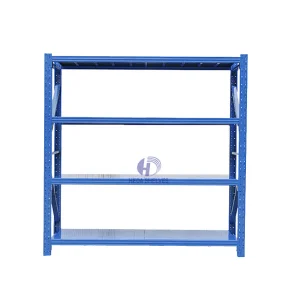
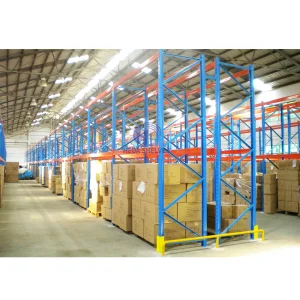
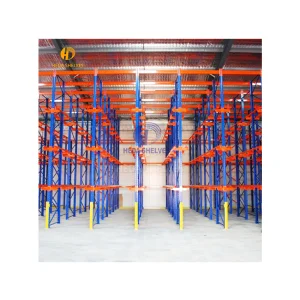
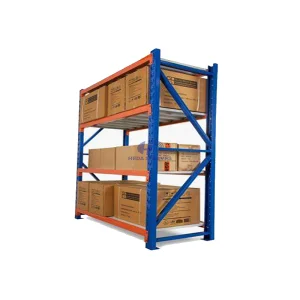
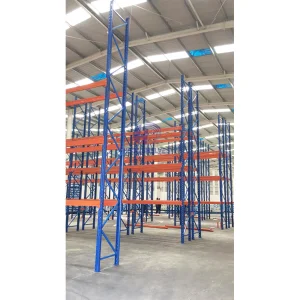
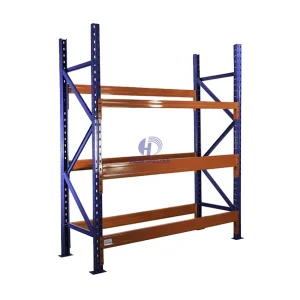
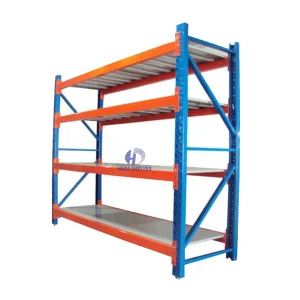
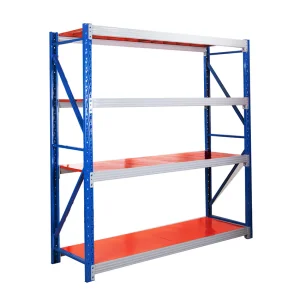
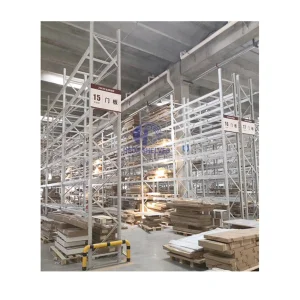
Select from our comprehensive line of heavy-duty pallet racks, drive-in systems, longspan shelving, and mezzanine platforms.
Get expert insights on customization options, ocean freight delivery timetables, load certifications, and installation support.
Our engineering team provides full OEM/ODM layout services. We utilize CAD and 3D BIM software to tailor rack height, shelf depth, bay width, pitch adjustment spacing, and color schemes based on your exact store floor blueprints and traffic flow analysis in Grenville.
Our medium-duty gondola display shelves support between 80kg to 150kg per level, while our heavy-duty beam pallet rack systems support from 1,000kg up to 3,000kg (1-3 Tons) per beam level under uniform static load conditions, fully certified via Finite Element Analysis (FEA).
Standard factory production takes 15 to 20 business days following technical drawing approval. Ocean freight transit to Grenville ports generally ranges from 25 to 35 days depending on maritime carrier schedules. Express sample production can be completed within 7 days.
Yes. All structural steel members undergo a 9-stage pre-treatment process including pickling, acid-washing, parkerising, and high-temperature electrostatic powder coating. This provides robust corrosion resistance compliant with salt-spray exposure requirements for coastal regions like Grenville.
Every order is shipped with detailed 3D step-by-step assembly manuals, exploded component diagrams, and video walkthroughs. For large mezzanine or high-bay warehouse projects in Grenville, our engineering team offers remote technical supervision and structural safety compliance sign-offs.
Contact our engineering sales department today for direct factory quotes, complimentary 3D layout designs, and complete technical specifications.
Send Inquiry Now Hedaracking