Architecting Next-Generation Industrial Bin Storage Systems & Dynamic Warehouse Racking Infrastructure for Global Supply Chain Excellence.
Explore our engineered inventory of heavy-duty pallet systems, dynamic shuttle racking, and modular boltless bin shelves designed for maximum volumetric utilization.
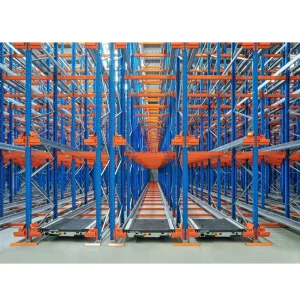
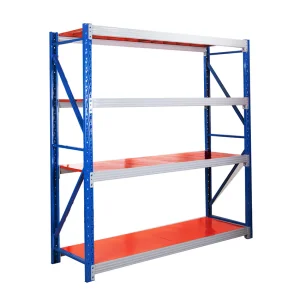
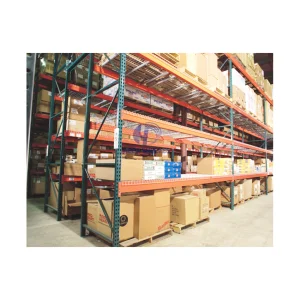
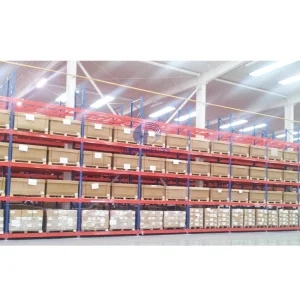
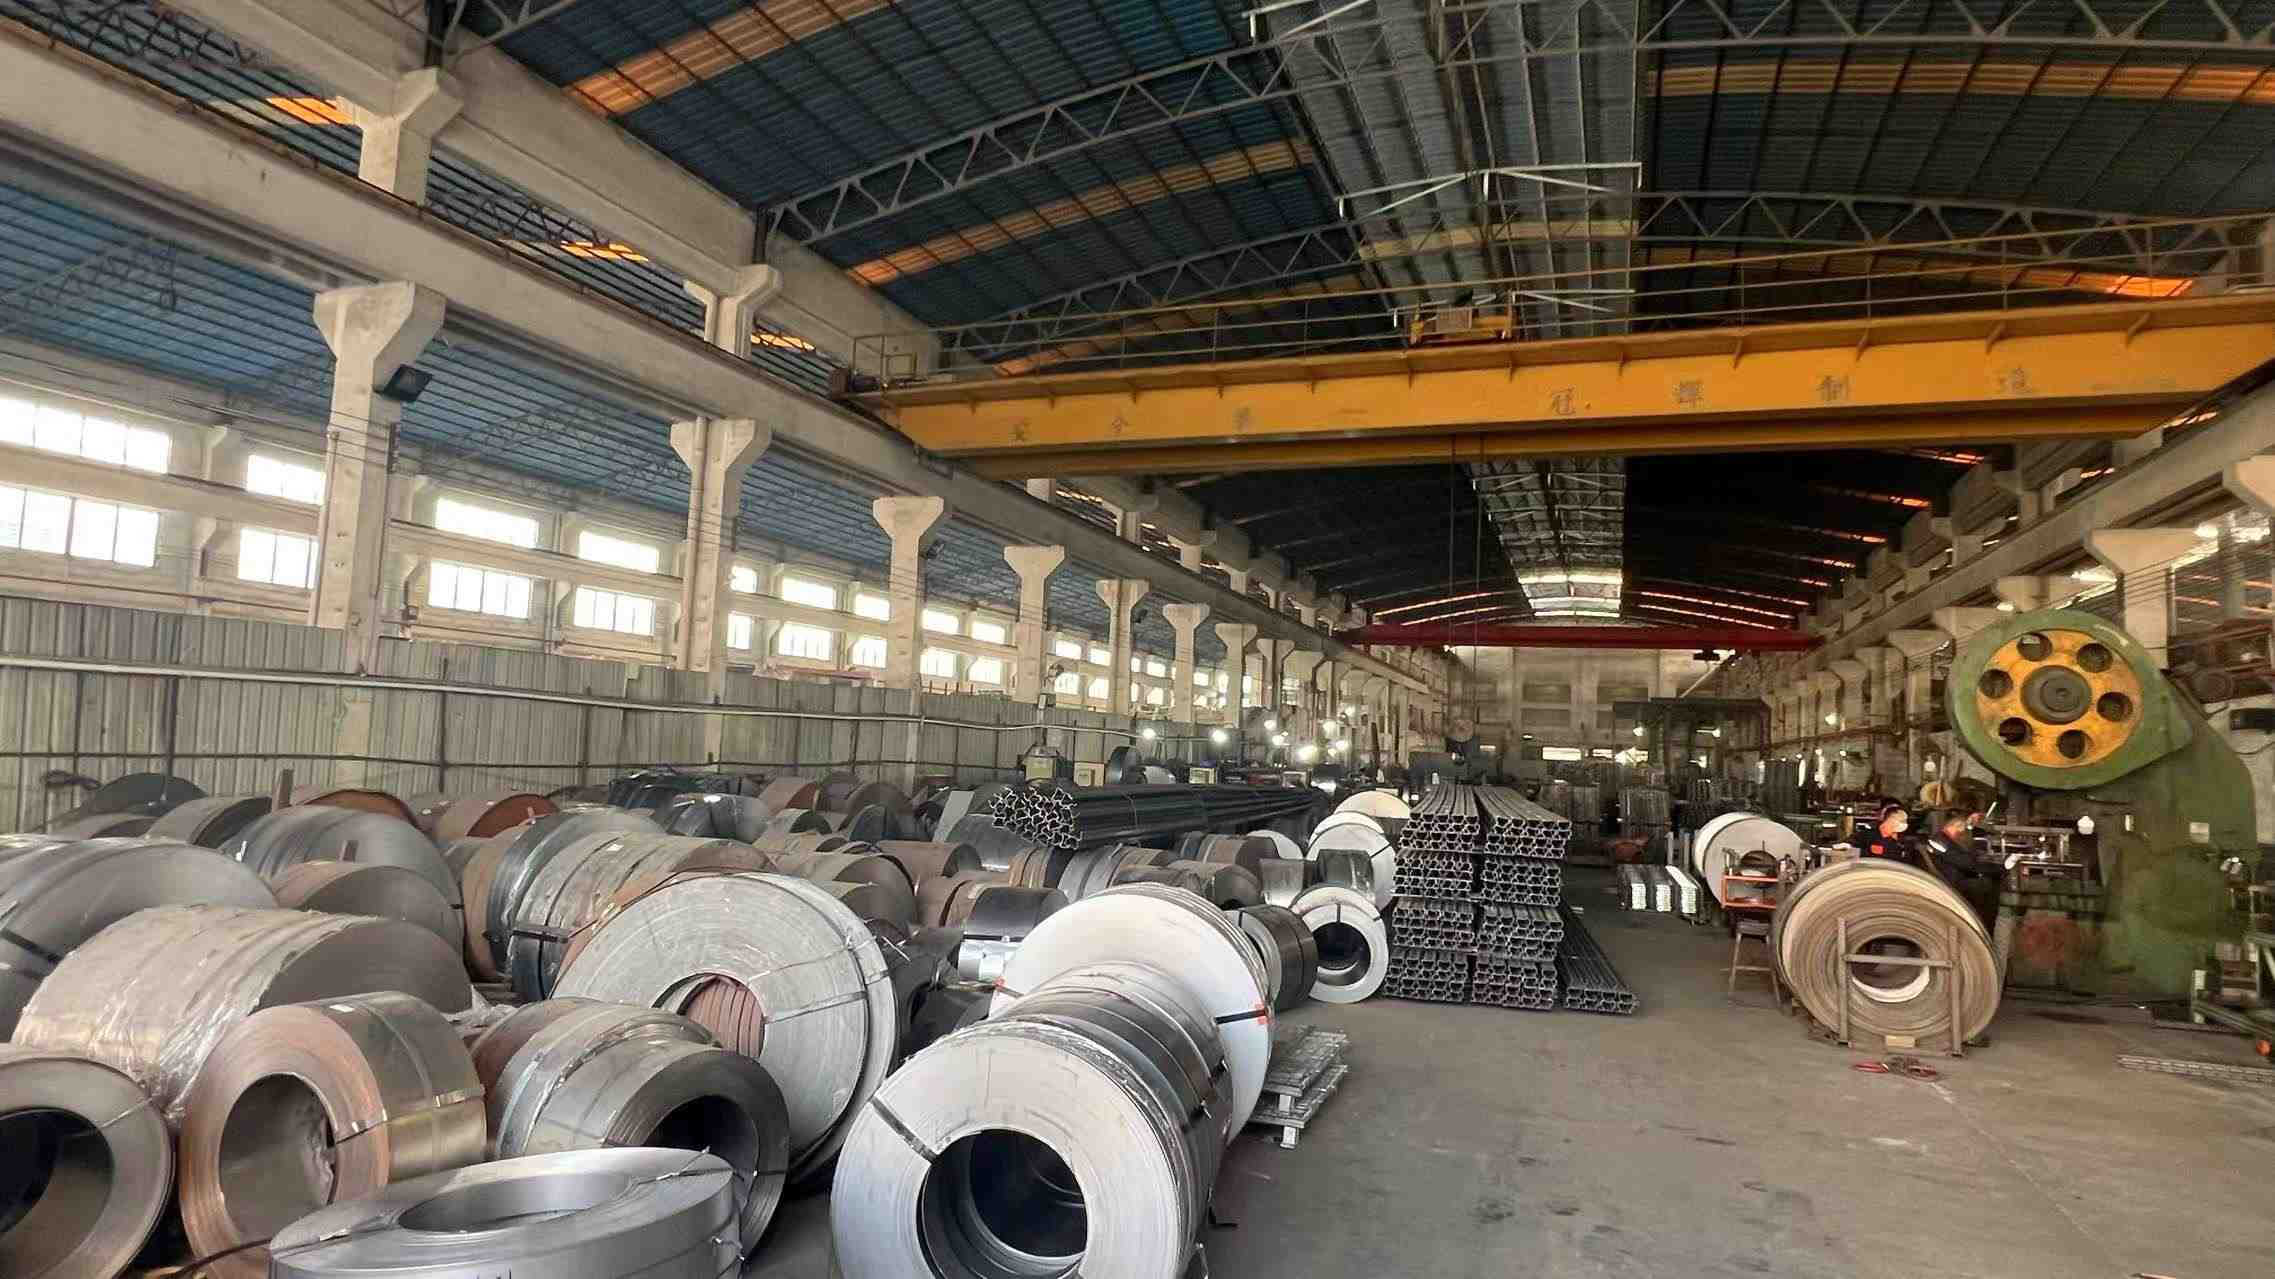
Established in 2014, Shenzhen Heda Warehouse Equipment Co., Ltd. has consolidated its position as a world-class premier manufacturer specializing in engineered heavy-duty warehouse racking, dynamic bin shelves, and integrated automated storage solutions. Operating from a state-of-the-art manufacturing hub spanning over 35,000 m², our enterprise seamlessly merges advanced structural R&D, 3D spatial design, precision robotic manufacturing, and global commercial trade logistics. Over 12 years of deep industry experience combined with 8 years of dedicated export execution enable us to generate over $28 million in annual export revenue, driving supply chain efficiency for global enterprises across 100+ countries.
E-E-A-T Quality Commitment: Rigorous quality assurance is the bedrock of our manufacturing methodology. Our robust Quality Control (QC) department comprises 45 skilled inspectors deploying strict testing standards—including raw material tensile strength verification, ultrasonic weld flaw analysis, deflection load stress evaluations, and salt-spray surface anti-corrosion testing. Backed by an R&D team of 28 senior structural engineers, we introduced over 120 dynamic storage products and patented modular component upgrades last year alone.
Through a resilient ecosystem supported by over 800 trusted supply chain partners, Shenzhen Heda exports structural storage solutions to key industrial sectors across North America, Western Europe, Southeast Asia, and the Middle East. Our clients range from global Third-Party Logistics (3PL) integrators and cold-chain distribution centers to high-tech manufacturing plants and commercial equipment distribution hubs.
The global material handling and warehousing sector is undergoing a profound paradigm shift. Accelerating e-commerce penetration, micro-fulfillment dynamics, and escalating commercial real estate costs have elevated warehouse density from a operational metric to a core strategic advantage. Modern enterprises no longer view bin shelves and pallet racks merely as passive structural storage; they are critical nodes in high-speed, data-driven fulfillment networks.
Traditional static shelving is rapidly giving way to high-density modular bin systems and vertical storage racks. Bin shelves engineered with micro-adjustable shelf steps (50mm pitch) allow operators to optimize vertical air space, increasing SKU density per square meter by up to 65% while maintaining rapid manual or automated picking access.
Modern manufacturing in China has aligned structural bin rack designs with autonomous mobile robots (AMRs) and 4-Way Radio Shuttle AS/RS units. Precision-punched uprights and strict dimensional tolerances ensure zero-jam operation during high-speed robotic bin extraction and high-rack shuttle transit.
Cold storage facilities operating down to -30°C require structural steel grades (such as Q355 cold-rolled steel) with enhanced impact toughness. Multi-stage chemical Parkerising and epoxy electrostatic powder coatings prevent micro-fissuring, moisture rust, and thermal stress degradation over decades of continuous operation.
When global procurement directors, warehouse operations leads, and B2B supply chain architects source bin shelves and racking from China manufacturers, their evaluation extends beyond unit cost. The total cost of ownership (TCO), dynamic load safety coefficients, modular scalability, and regulatory compliance dictate sourcing decisions.
Professional buyers prioritize raw material integrity. High-tensile cold-rolled steel (SS400, Q235B, Q355B) ensures structural rigidity. Heavy-duty pallet racks and bin shelves must adhere to strict deflection ratios (e.g., L/200 maximum beam deflection under nominal rating) to eliminate catastrophic rack failure under fully loaded operational stresses.
Labor overhead during warehouse commissioning represents a significant capital outlay. Advanced boltless metal shelving systems utilizing drop-in beam locks, teardrop patterns, and interlocking bin dividers enable fast, tool-free installation, reducing total warehouse integration time by over 40%.
Industrial storage equipment must withstand severe friction, impact, and chemical exposure. Pre-treatment chemical washing (degreasing, acid-pickling, Parkerising phosphating) followed by thermosetting epoxy-polyester powder coating guarantees coating adhesion exceeding 5B standards and salt-spray corrosion resistance up to 500 hours.
Enterprise facilities require customized footprint engineering. Top Chinese manufacturers supply complete BIM models, 3D CAD stress simulations, and tailored height-to-depth rack configurations designed around exact forklift turning radiuses, aisle clearances, and overhead sprinkler system clearances.
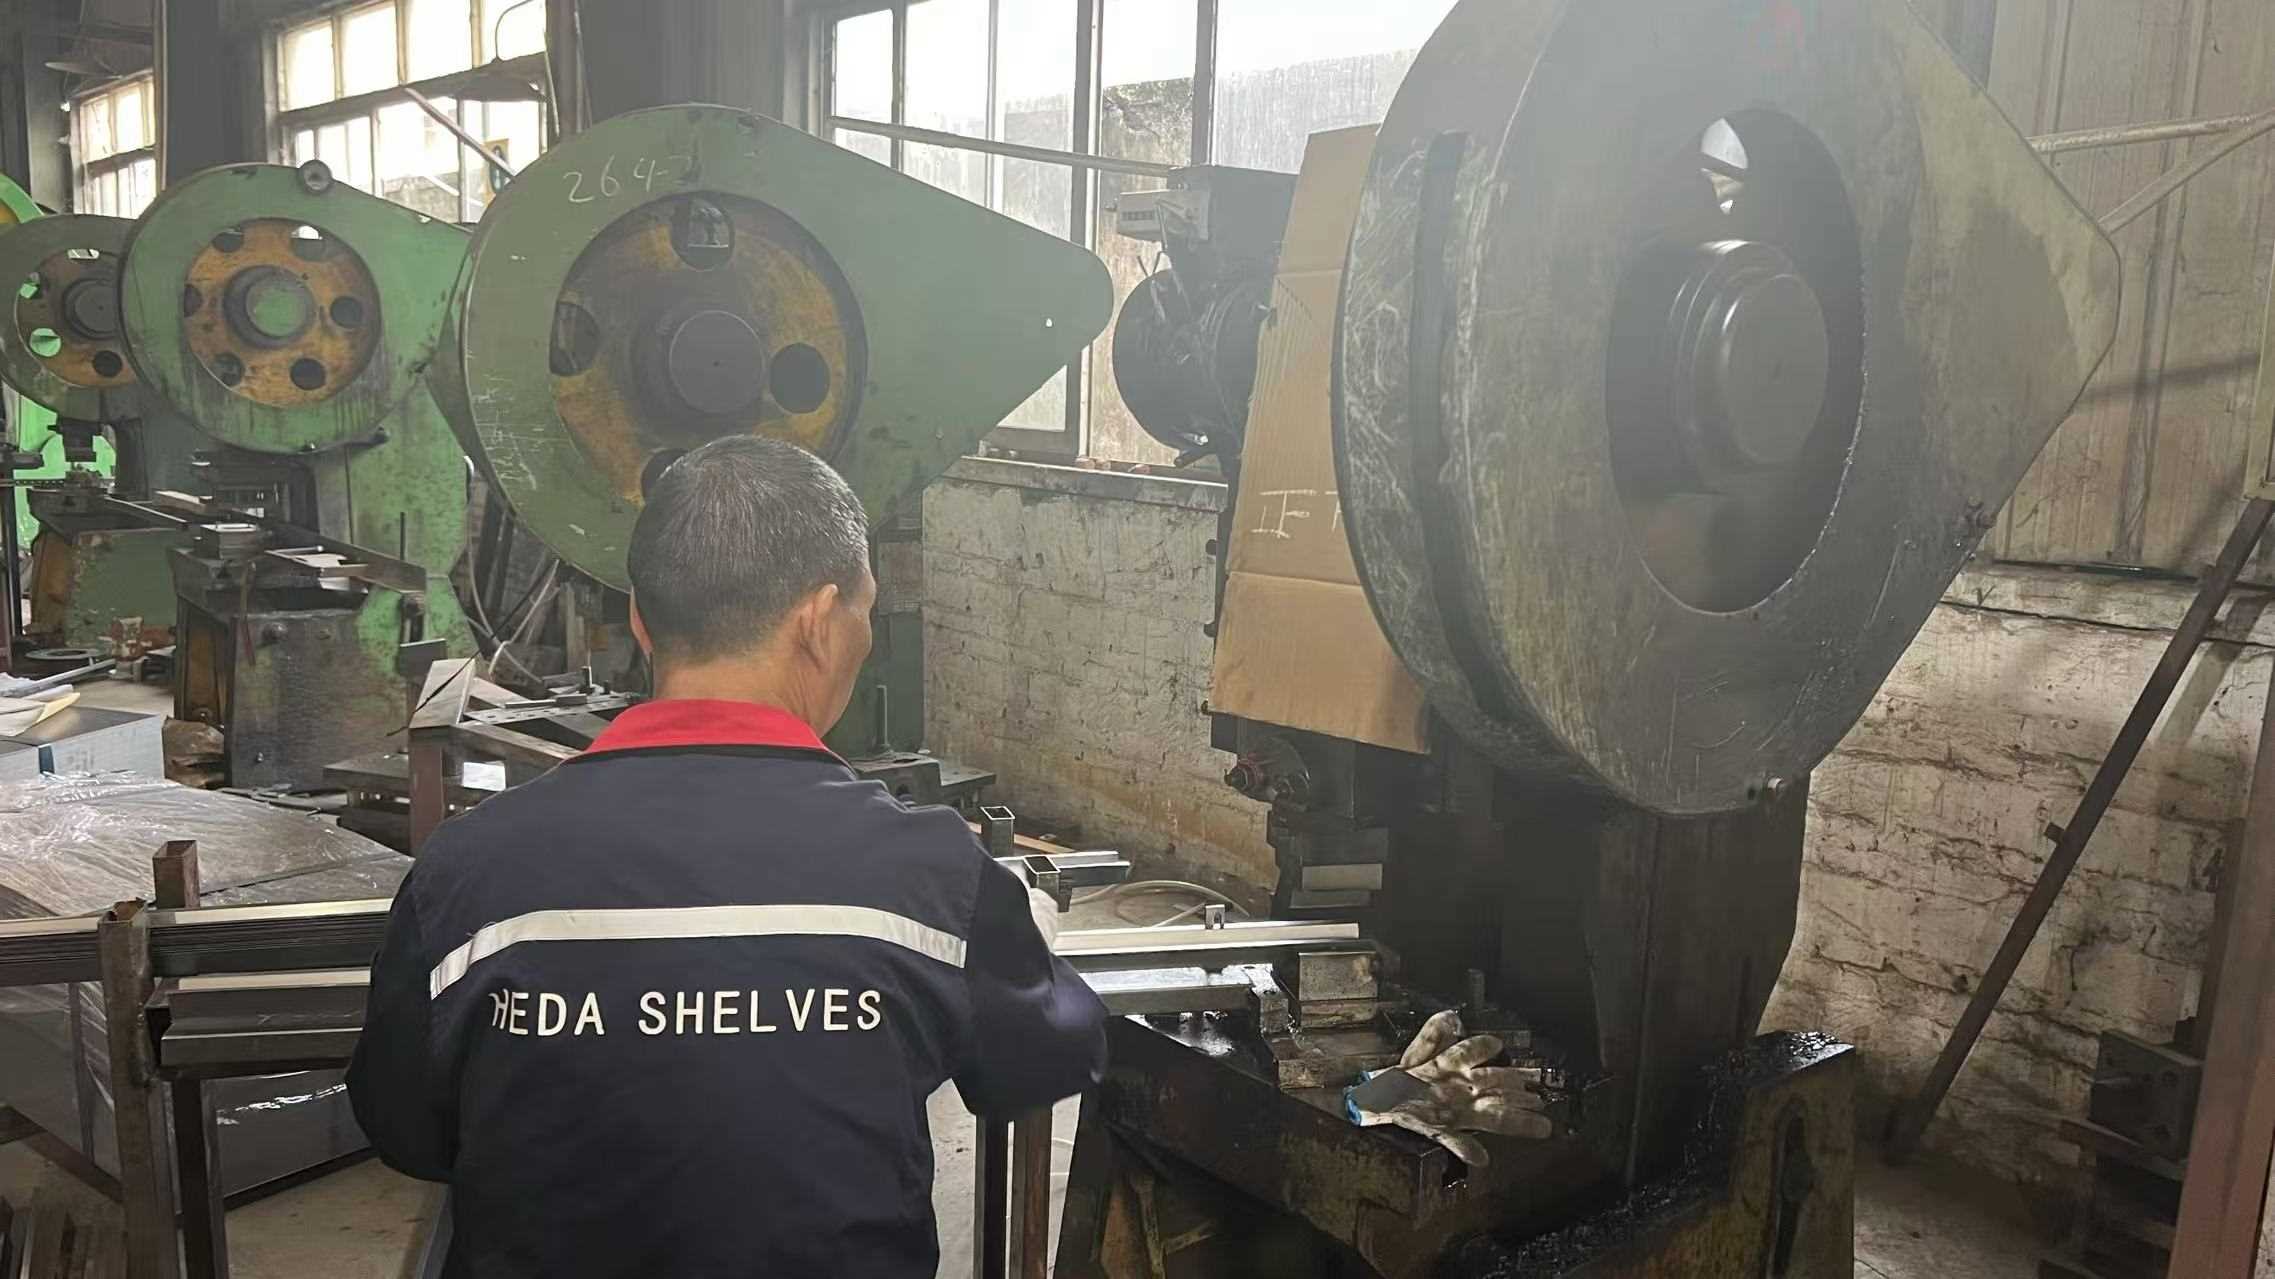
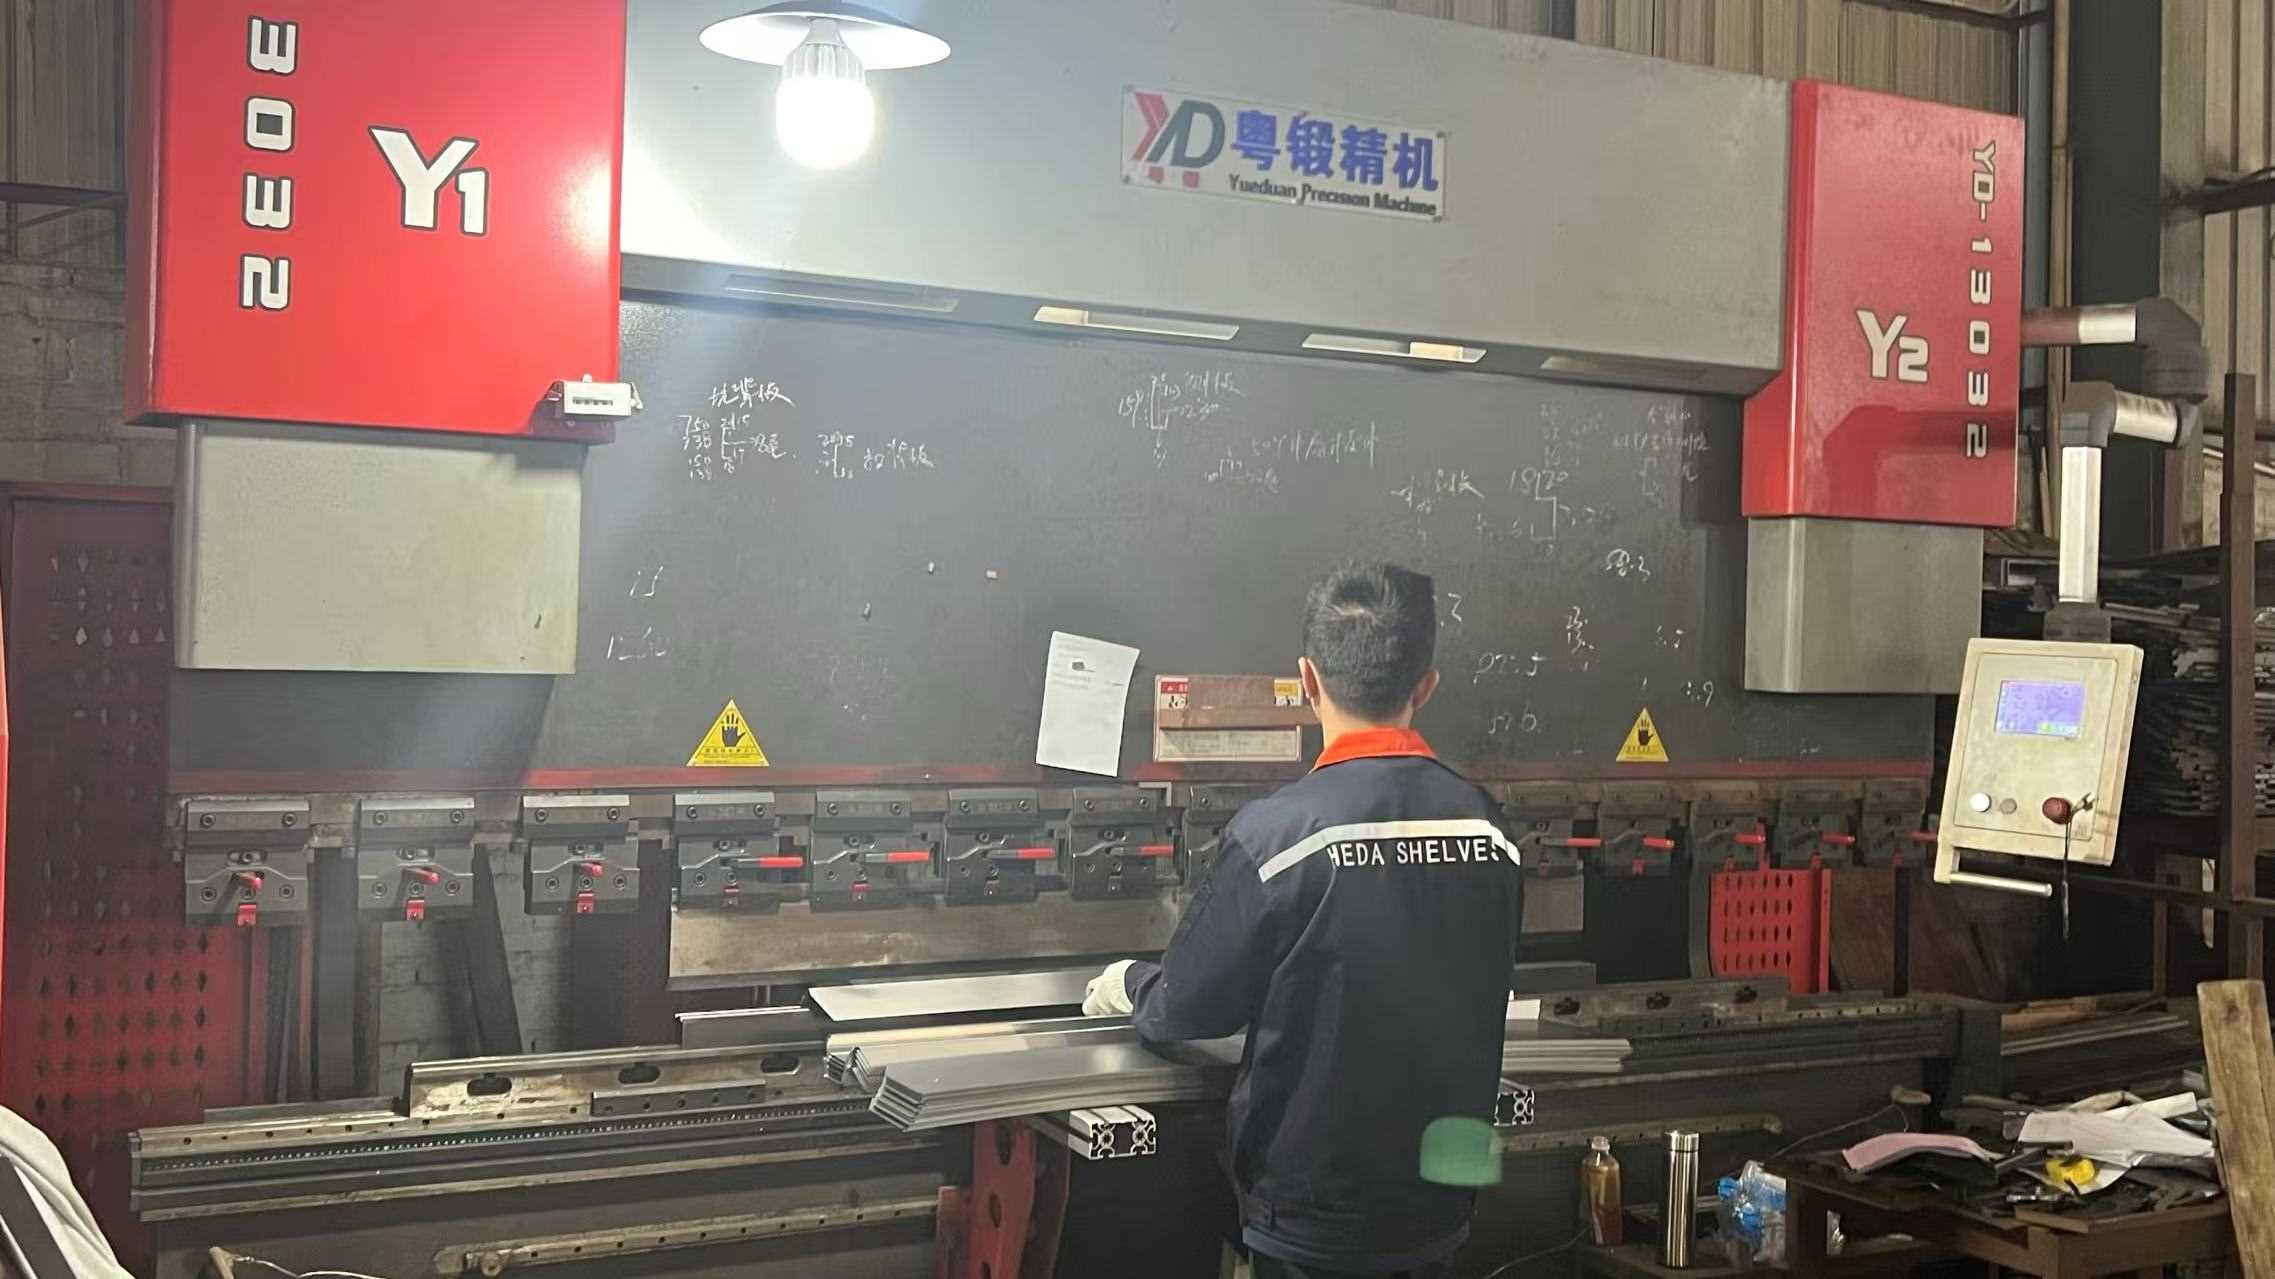
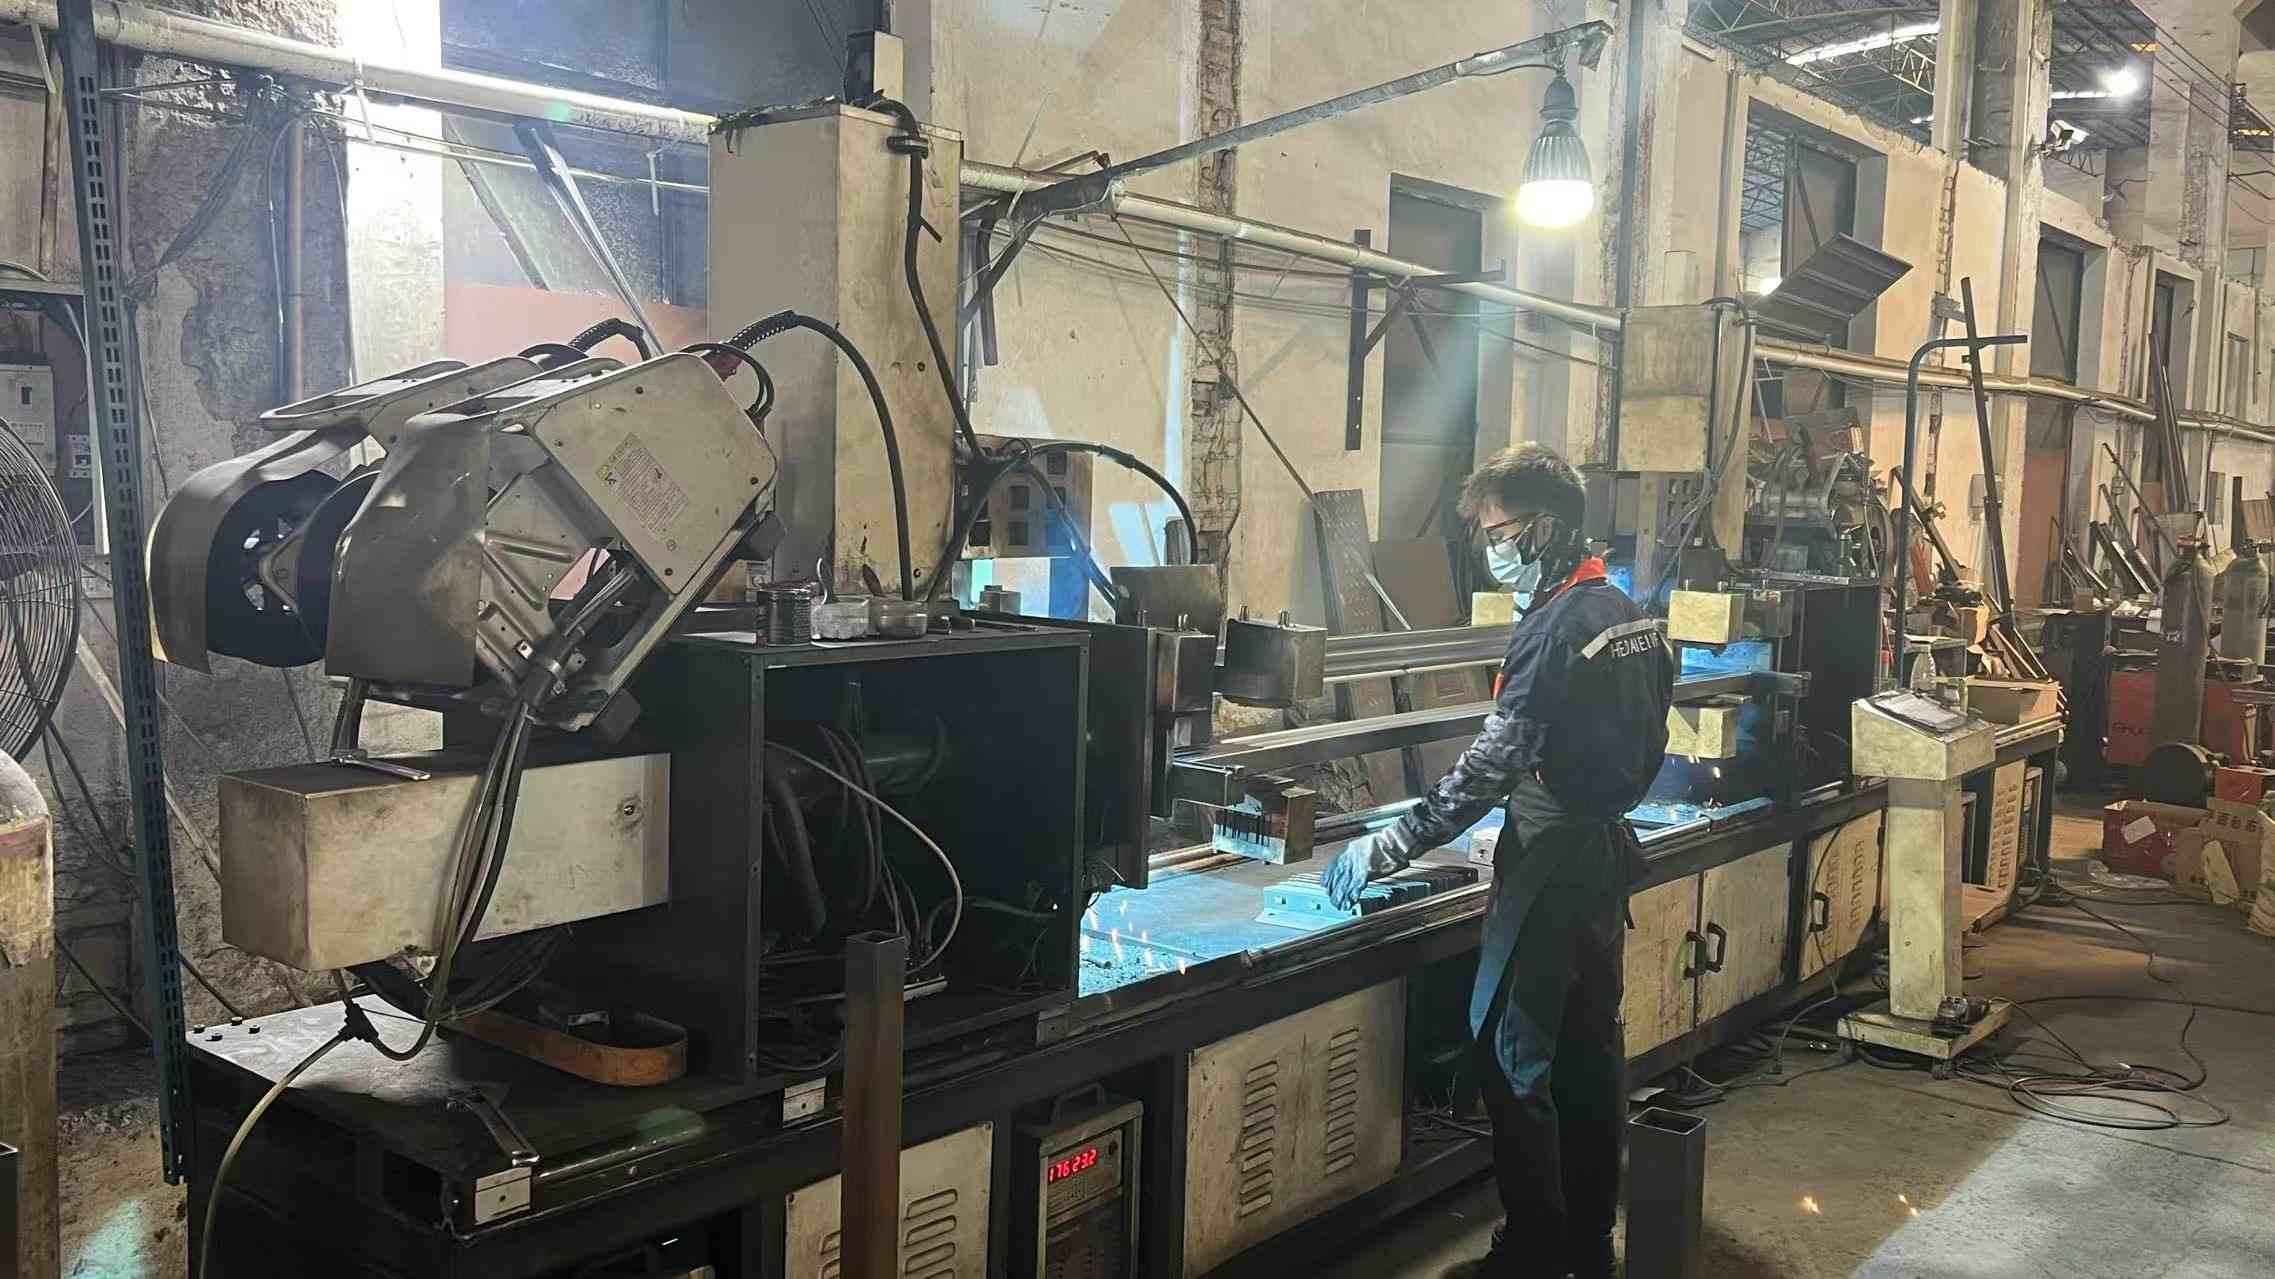
Every industrial bin rack and structural component engineered by Shenzhen Heda undergoes a rigorous, fully automated 14-stage manufacturing and inspection workflow to guarantee exact mechanical compliance and zero-defect delivery.
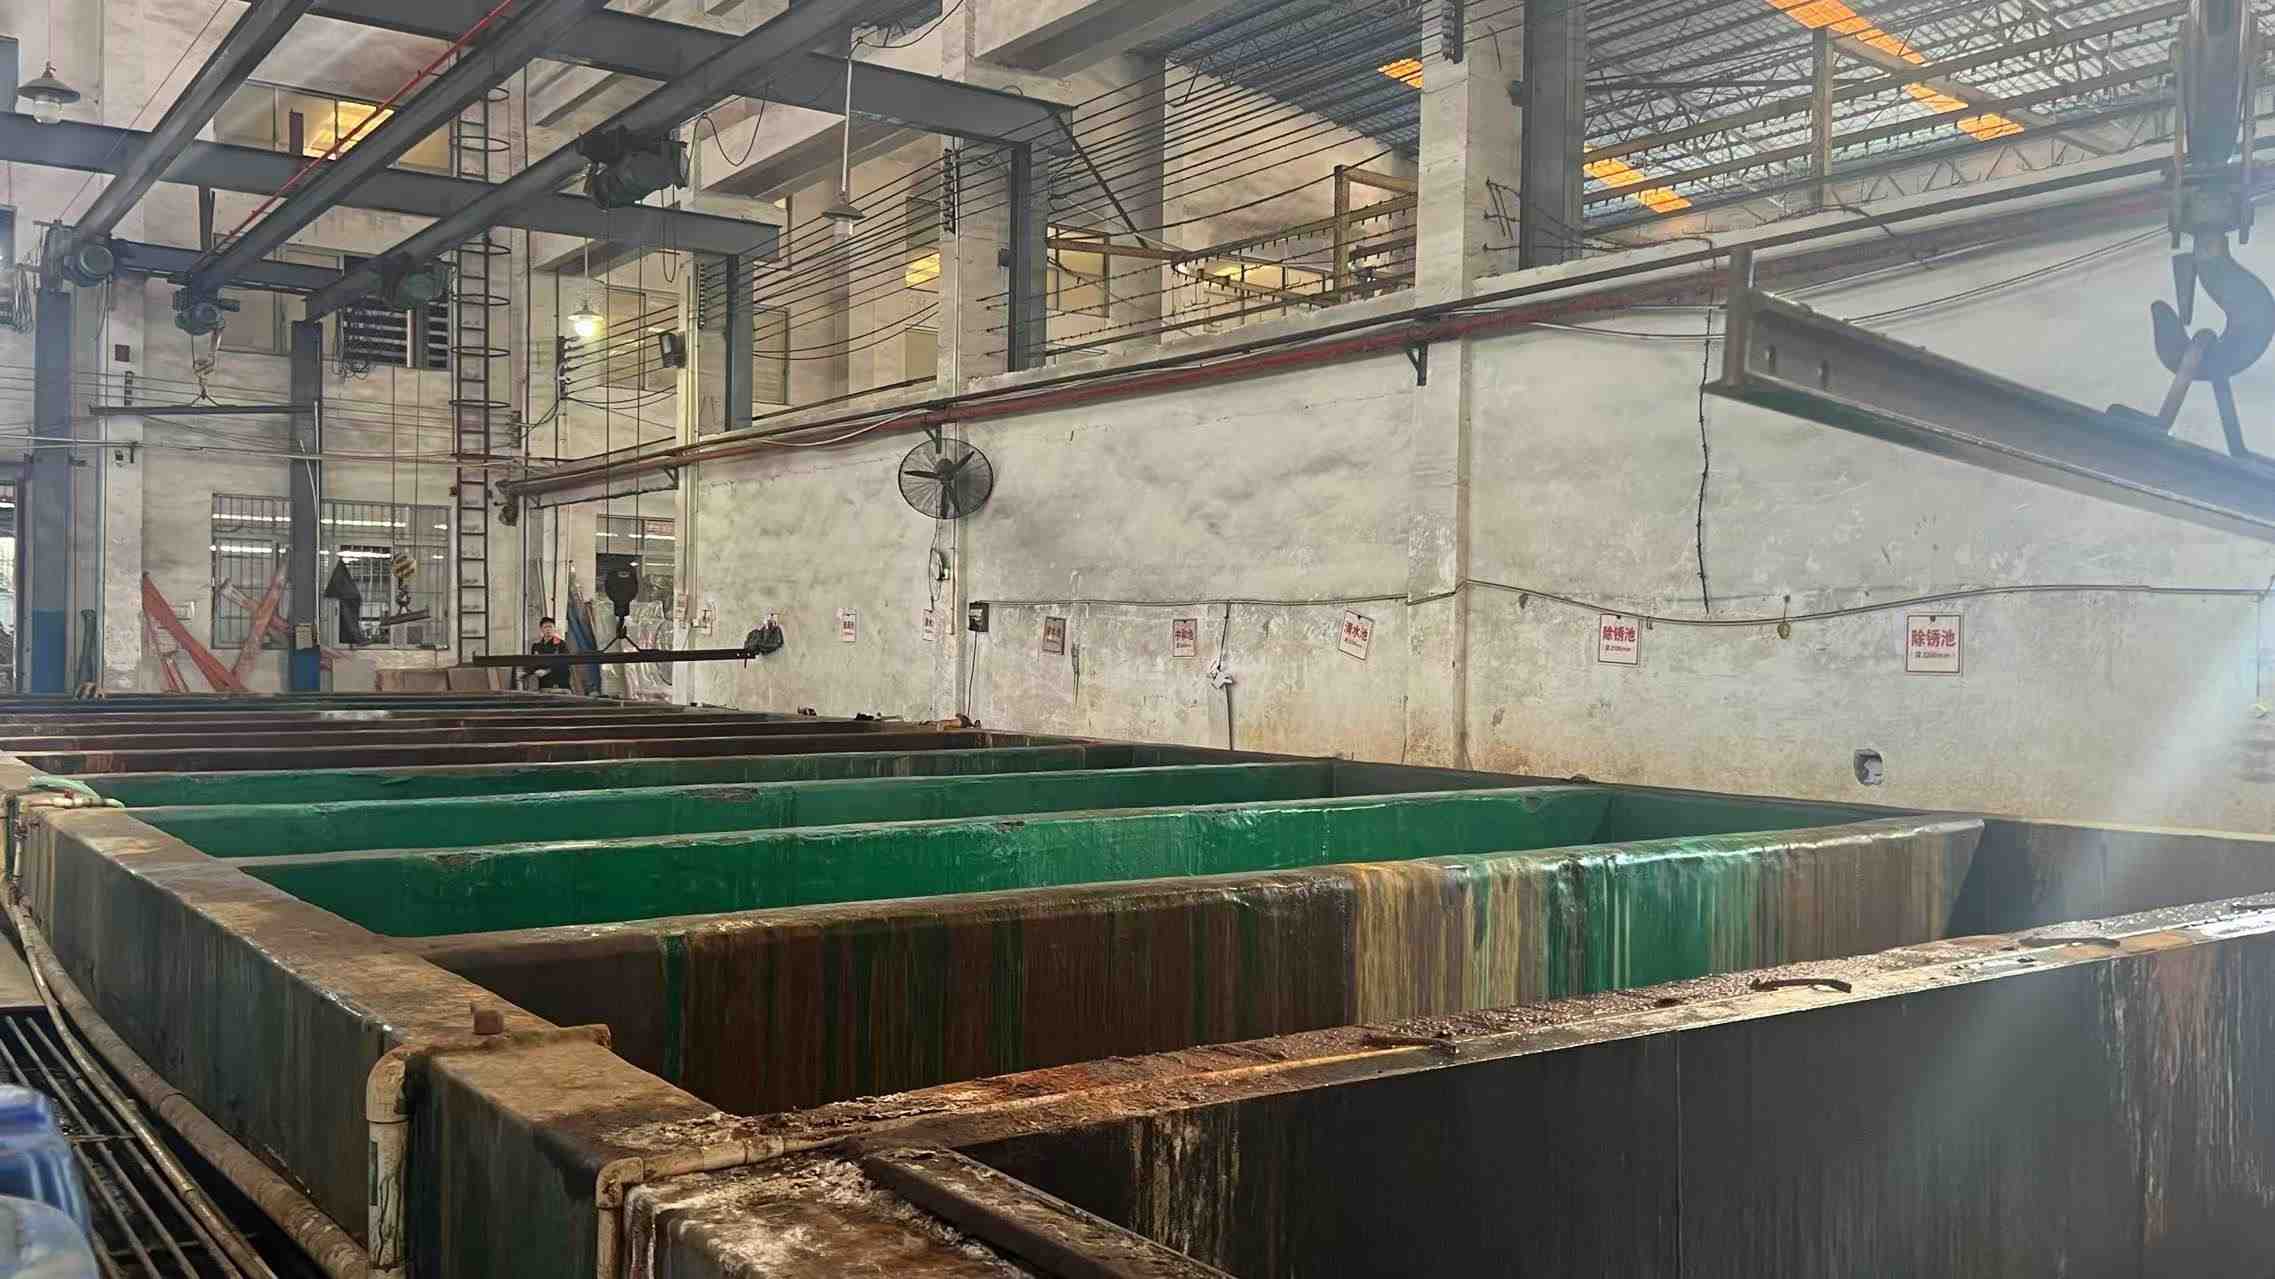
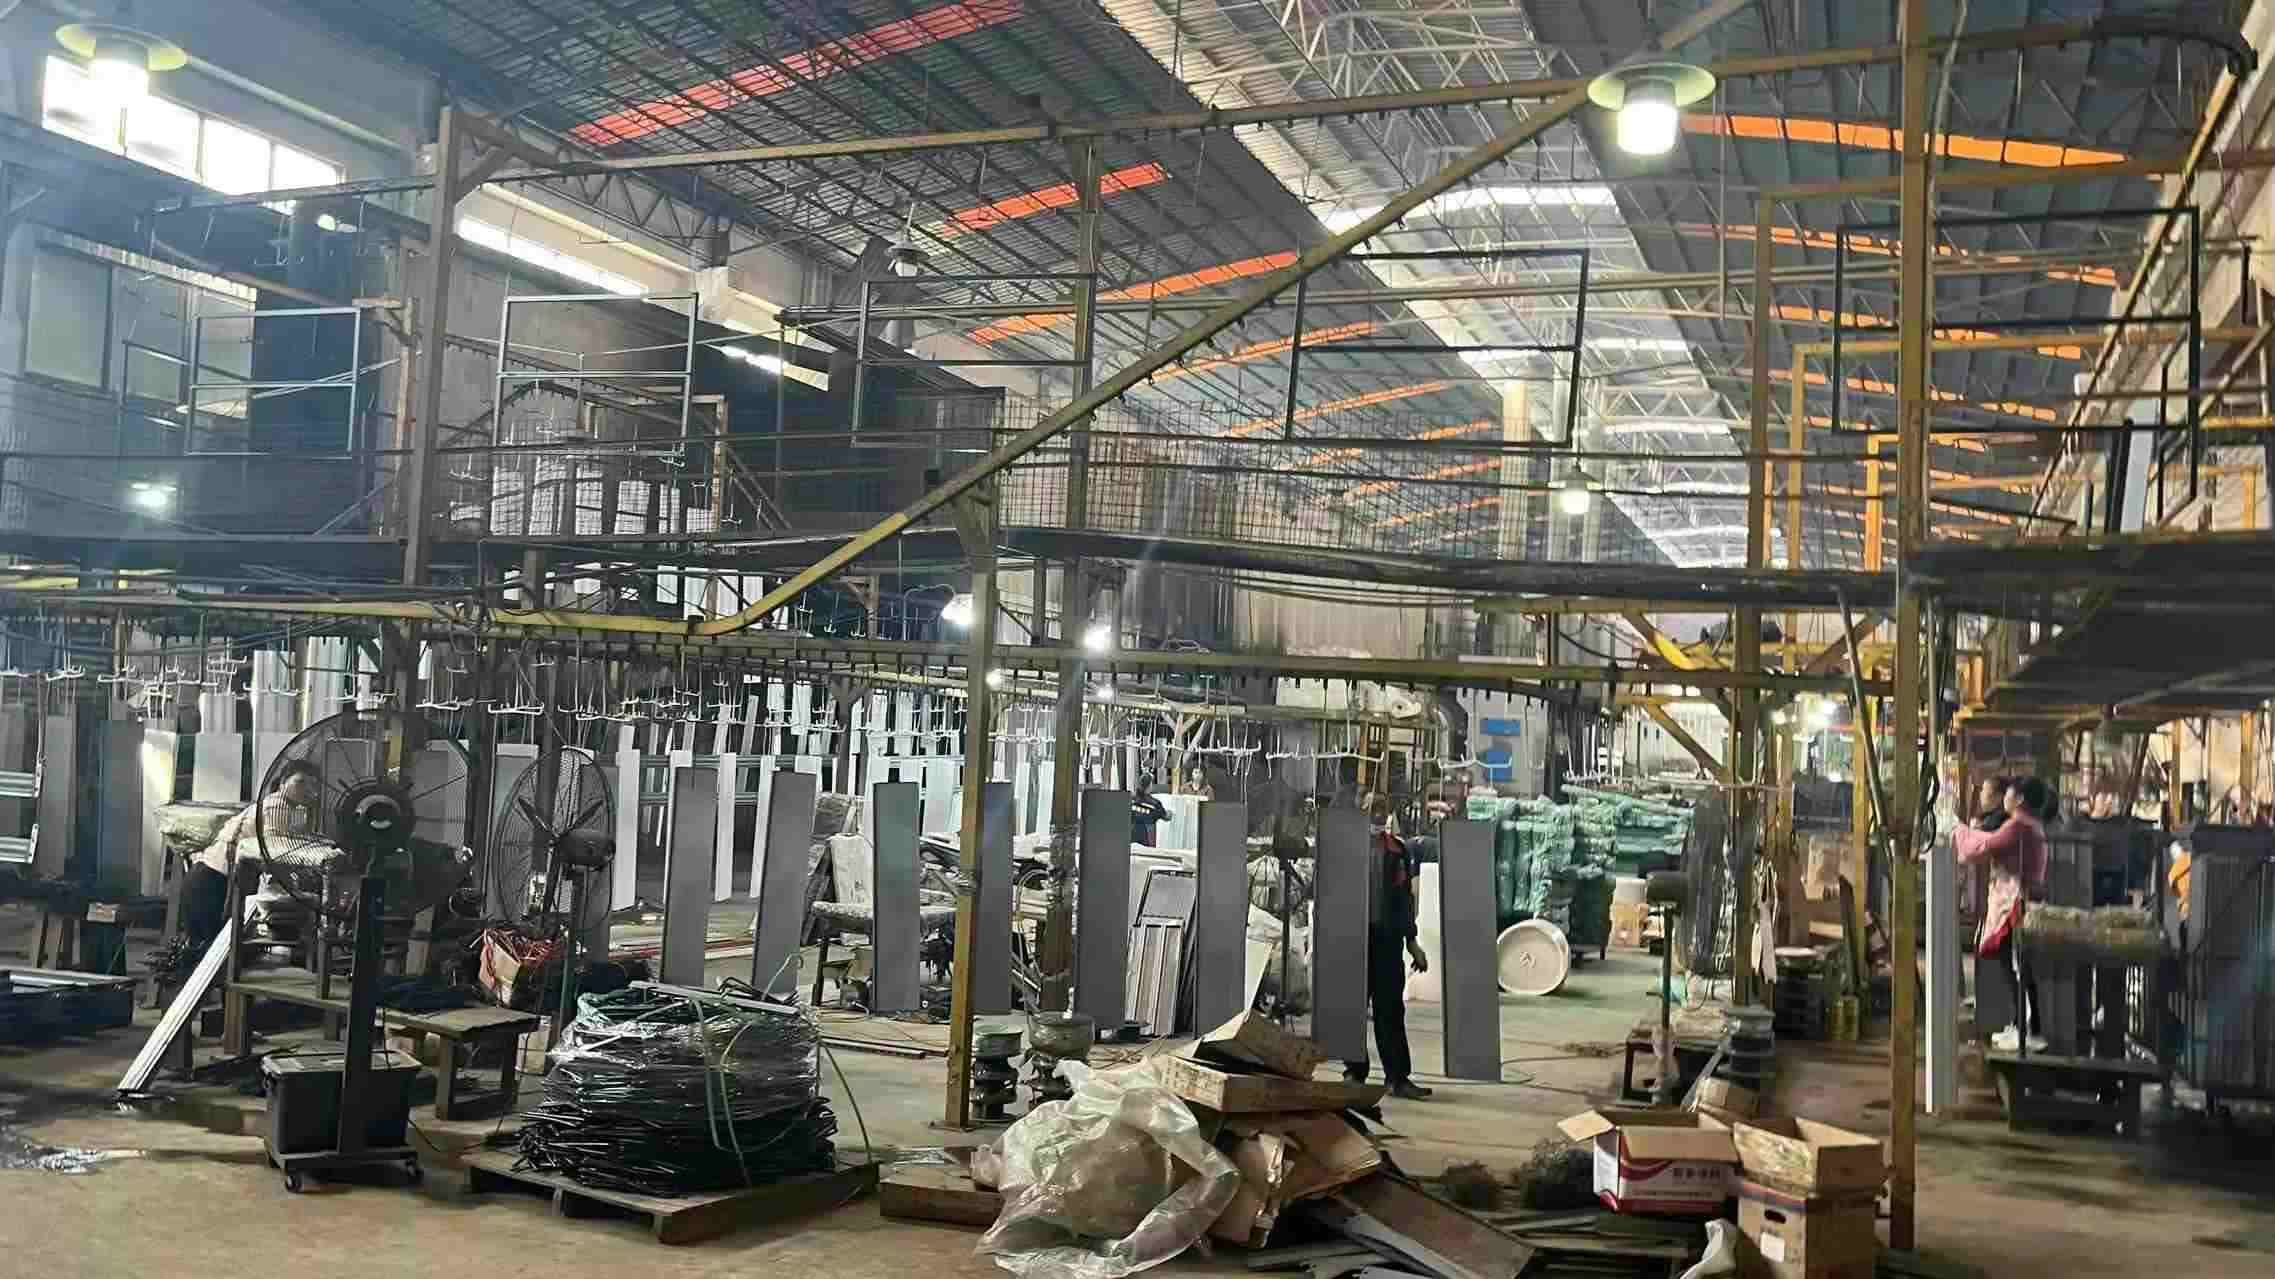
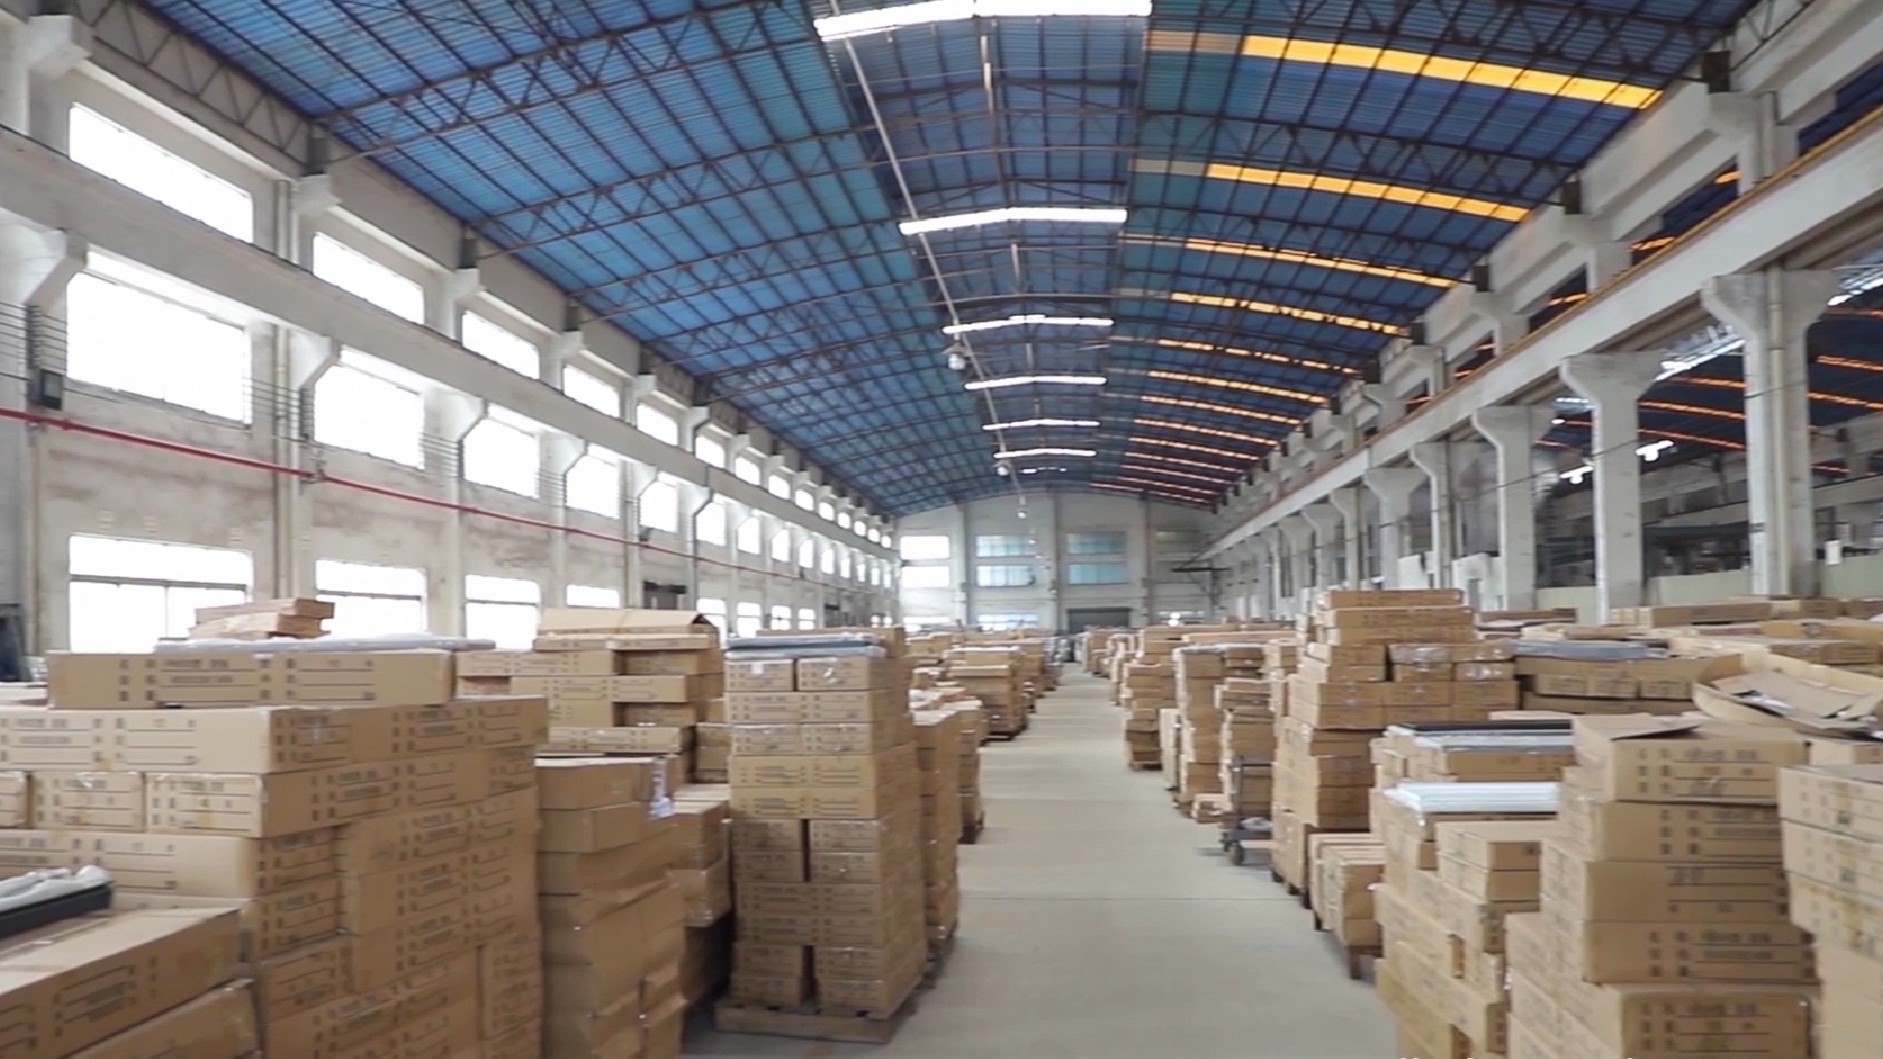
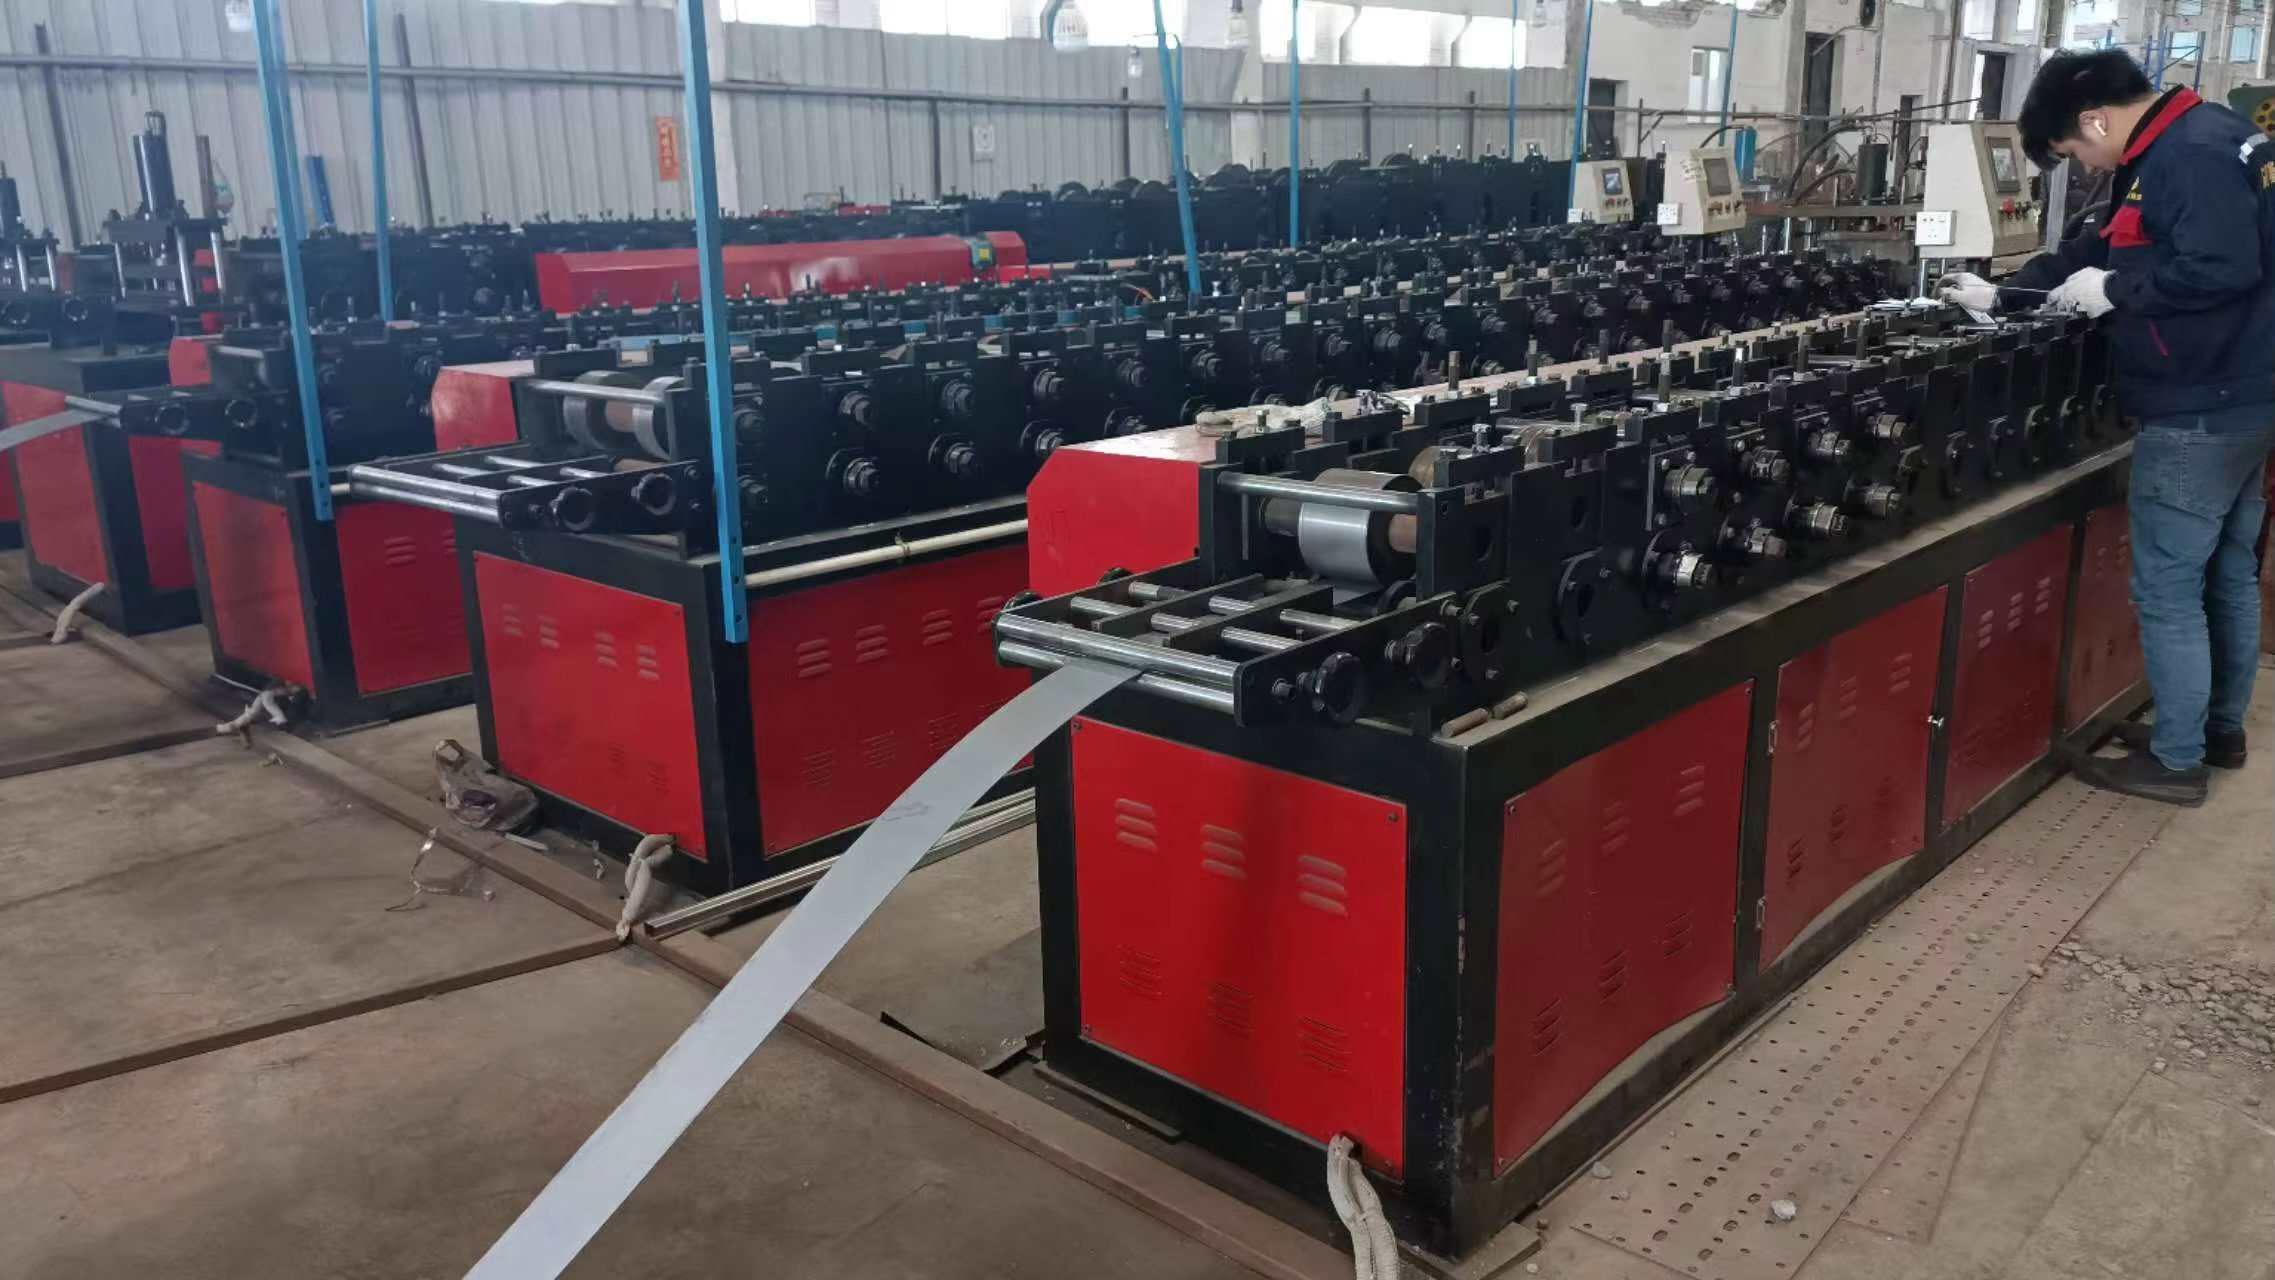
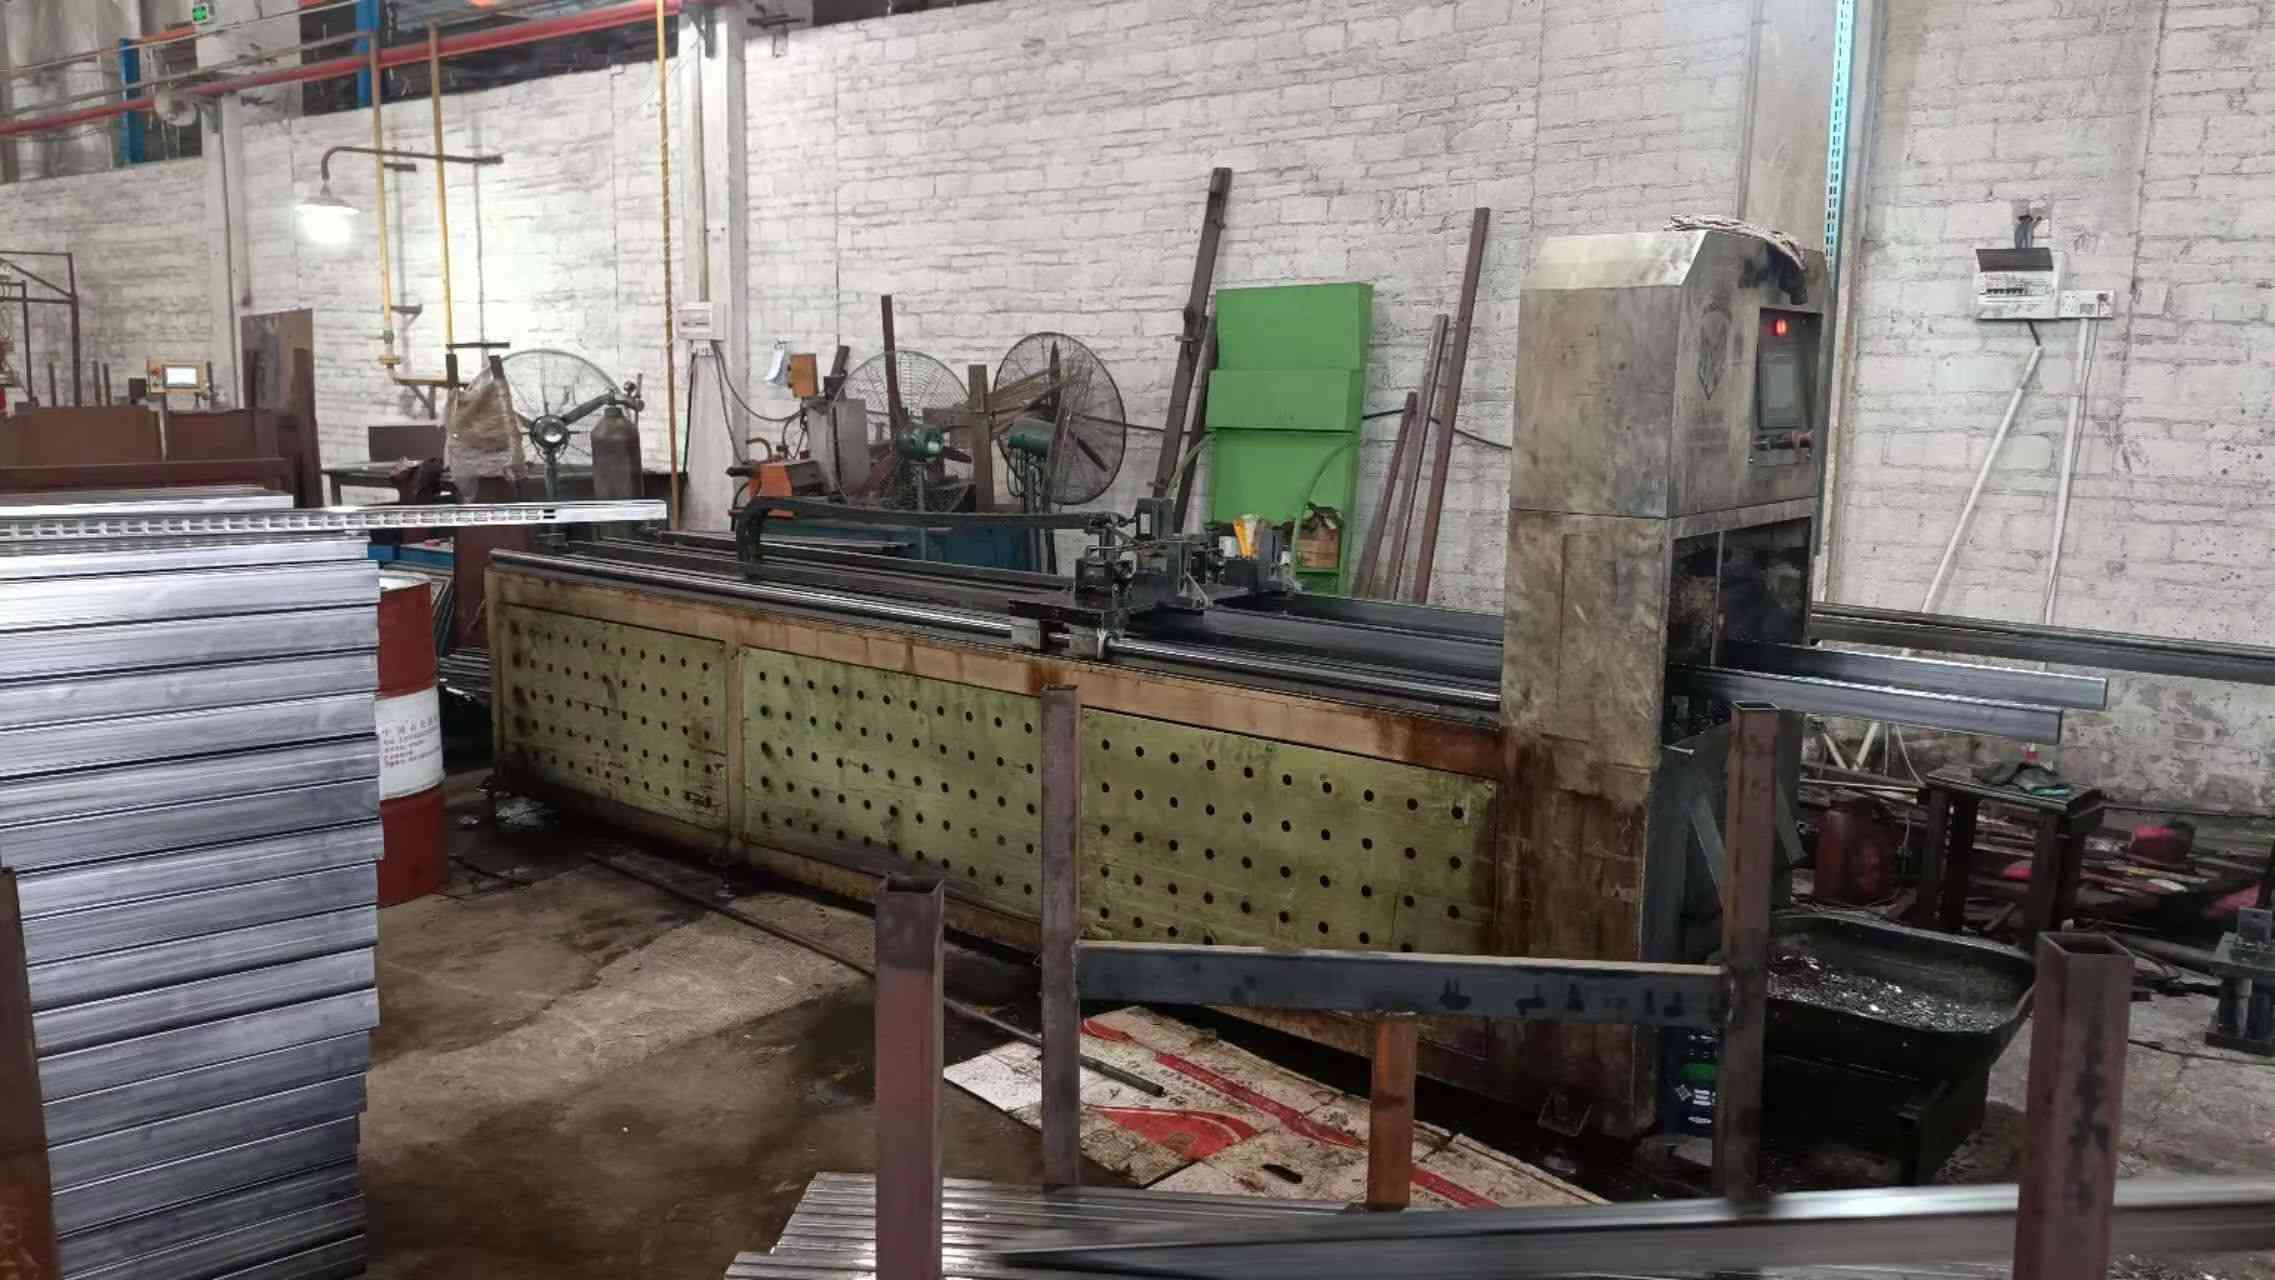
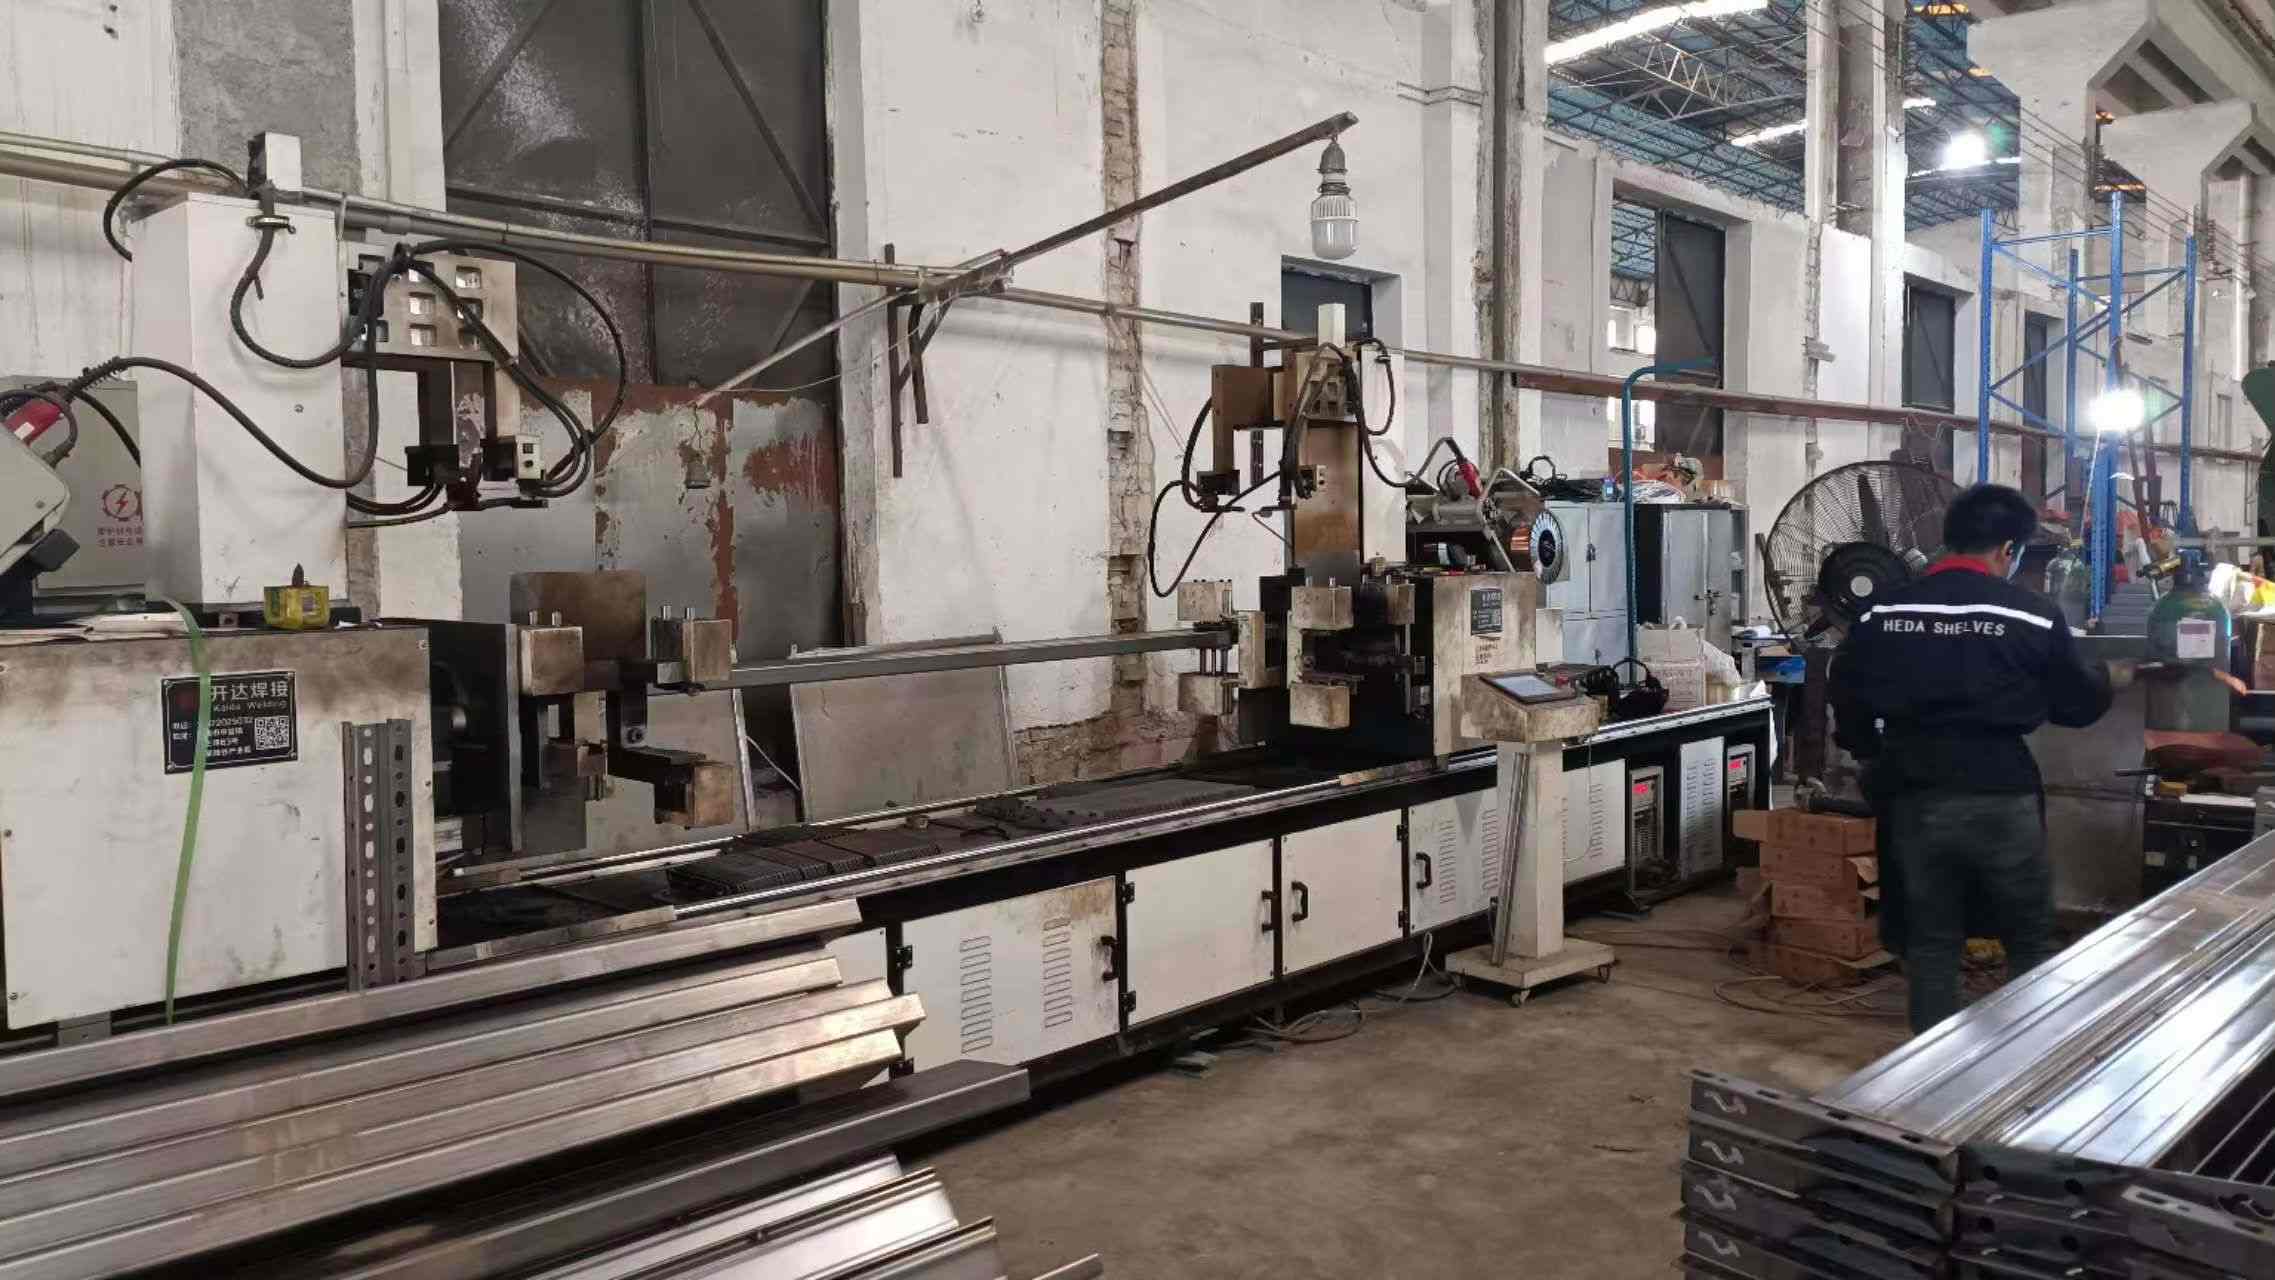
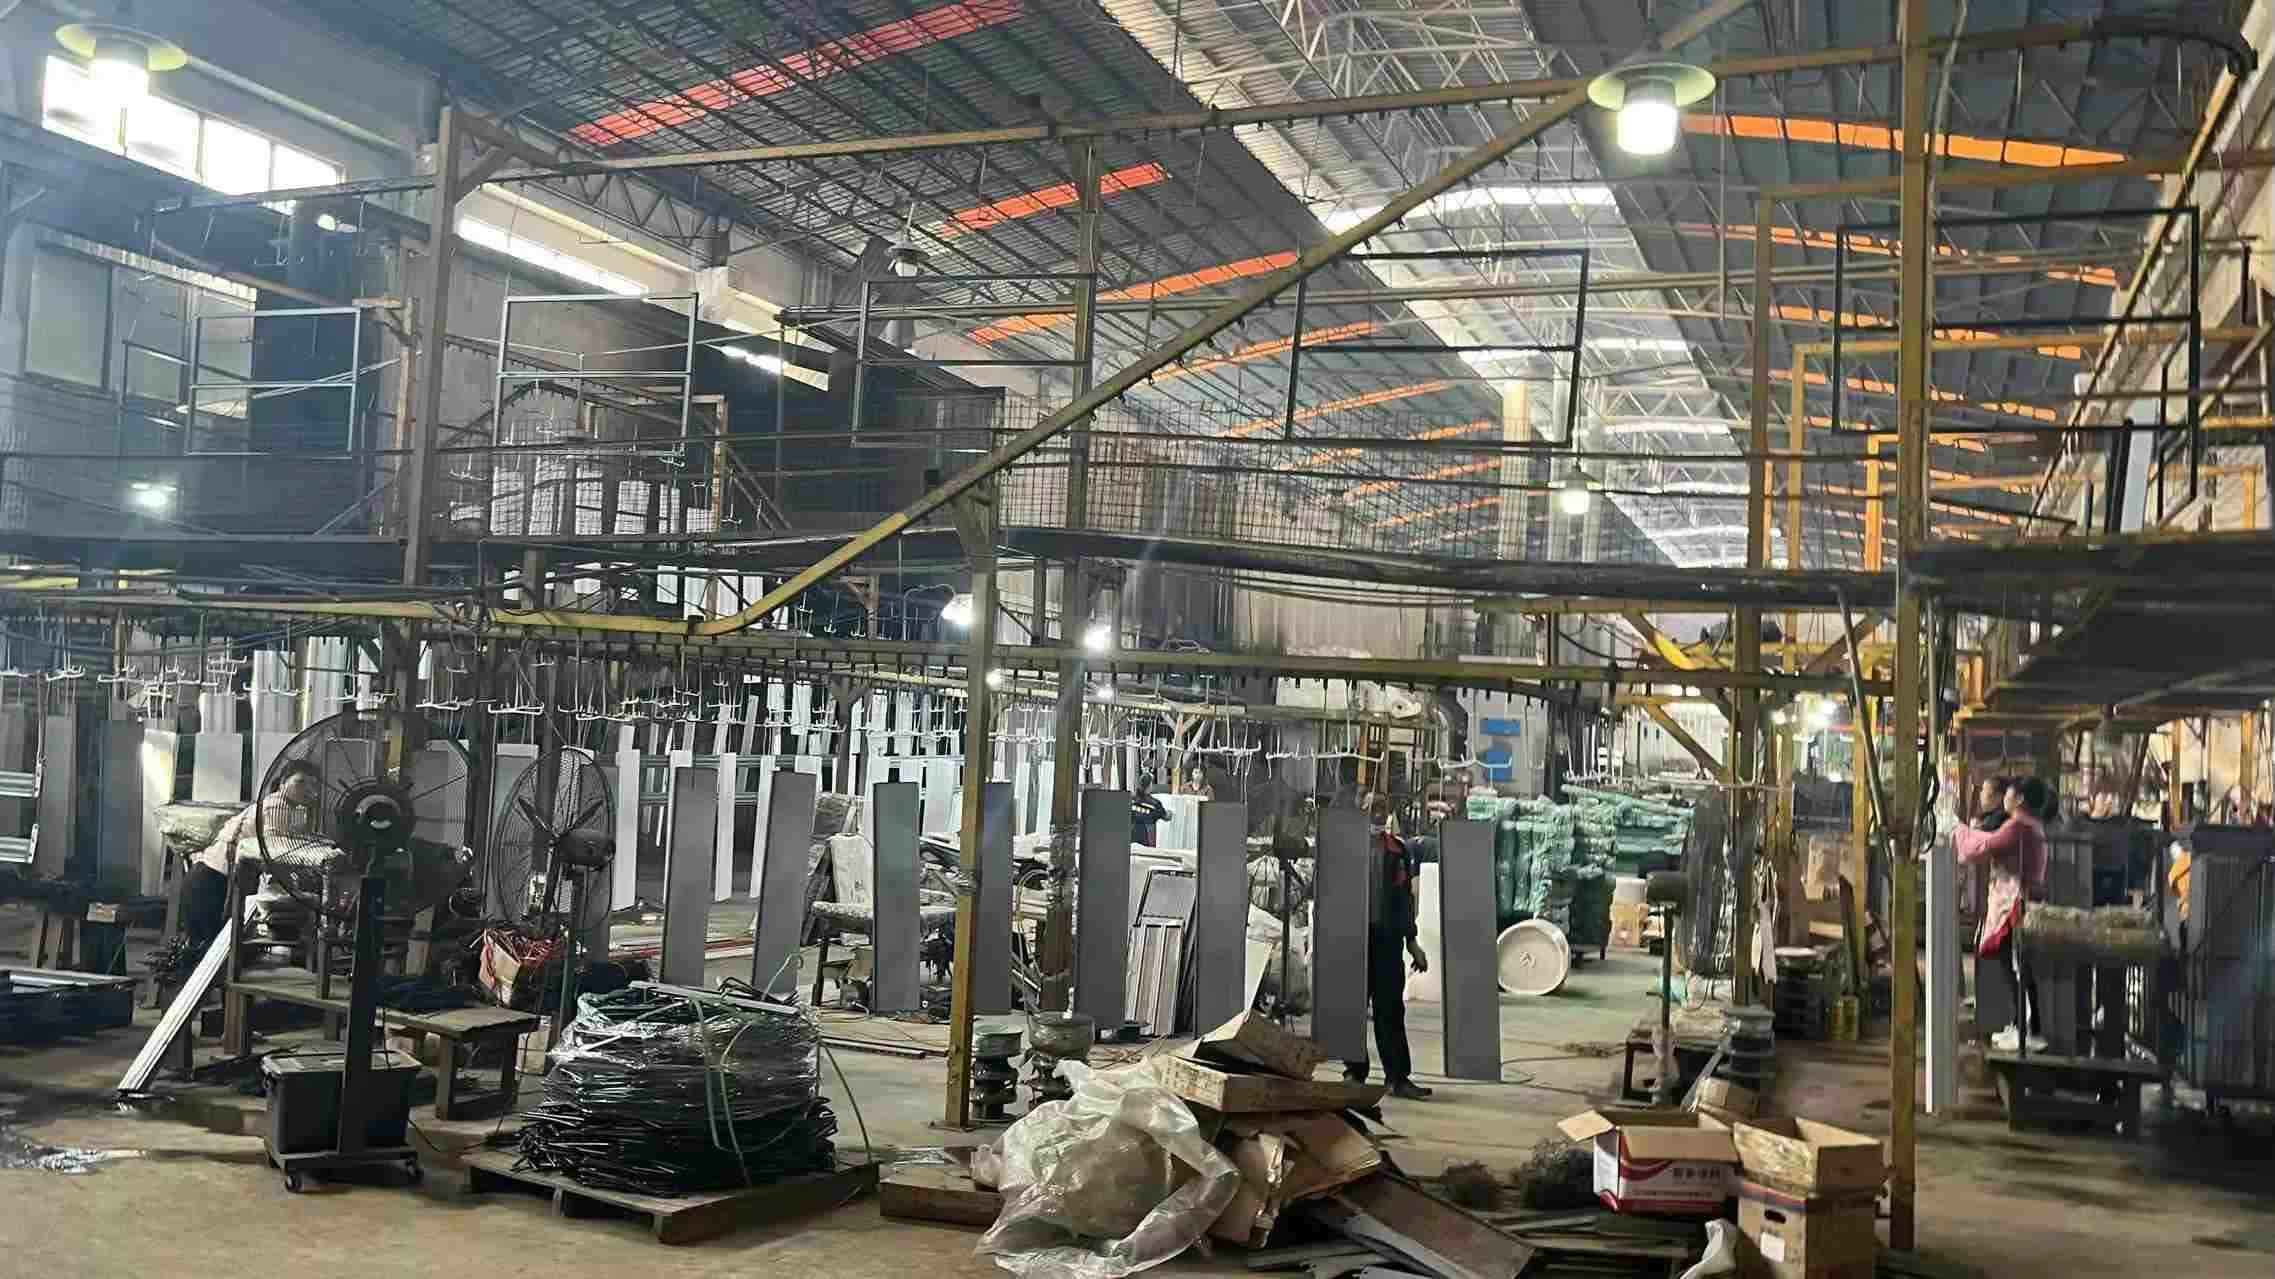
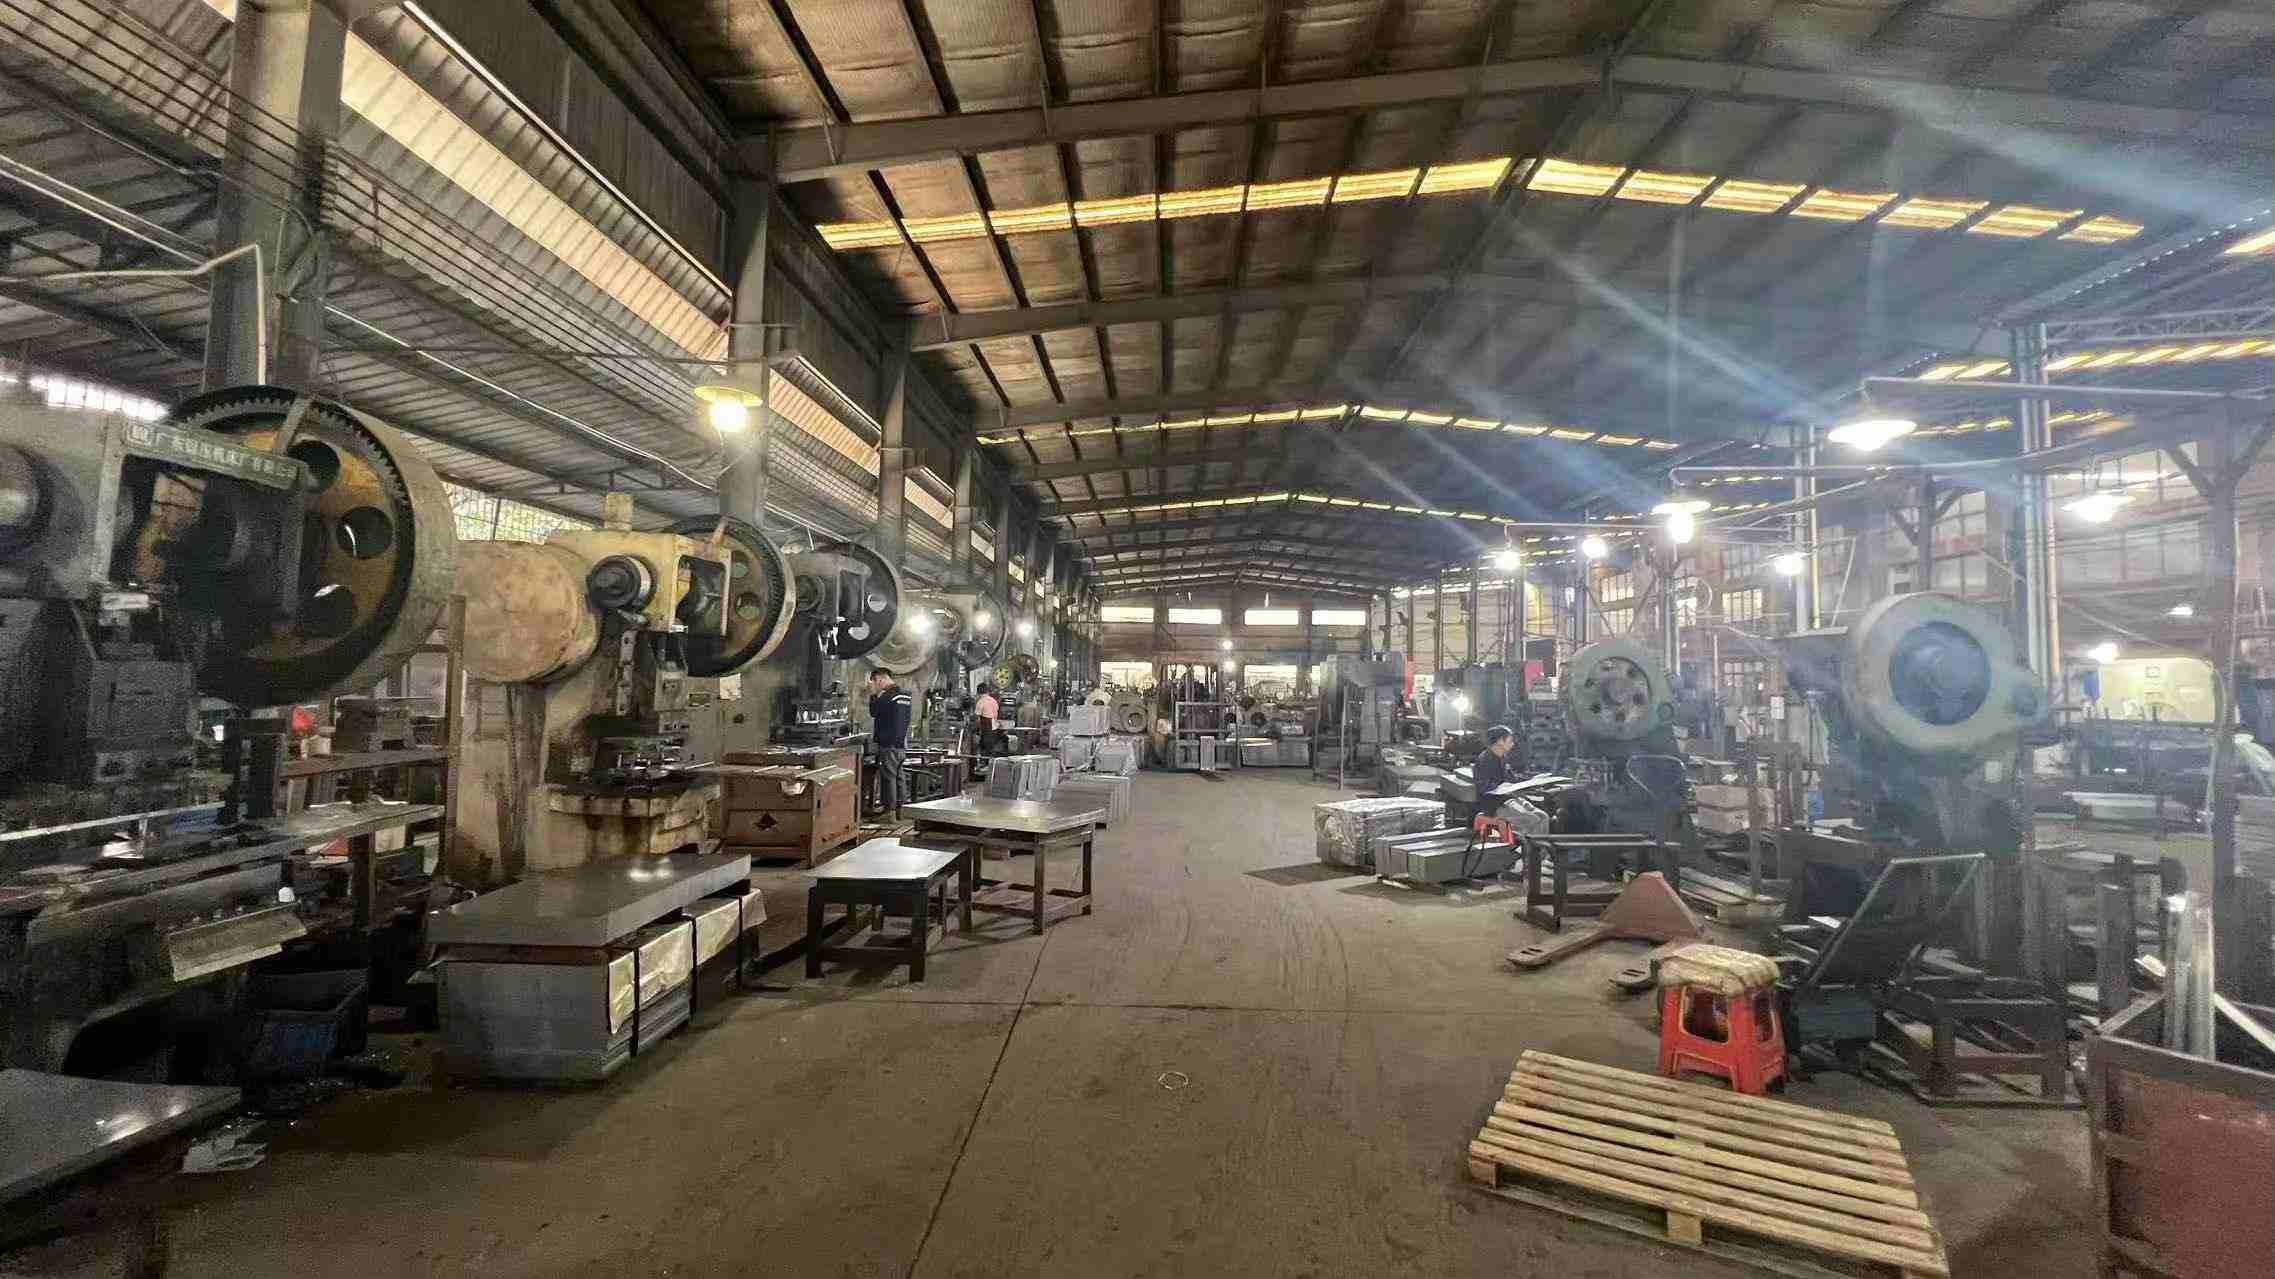
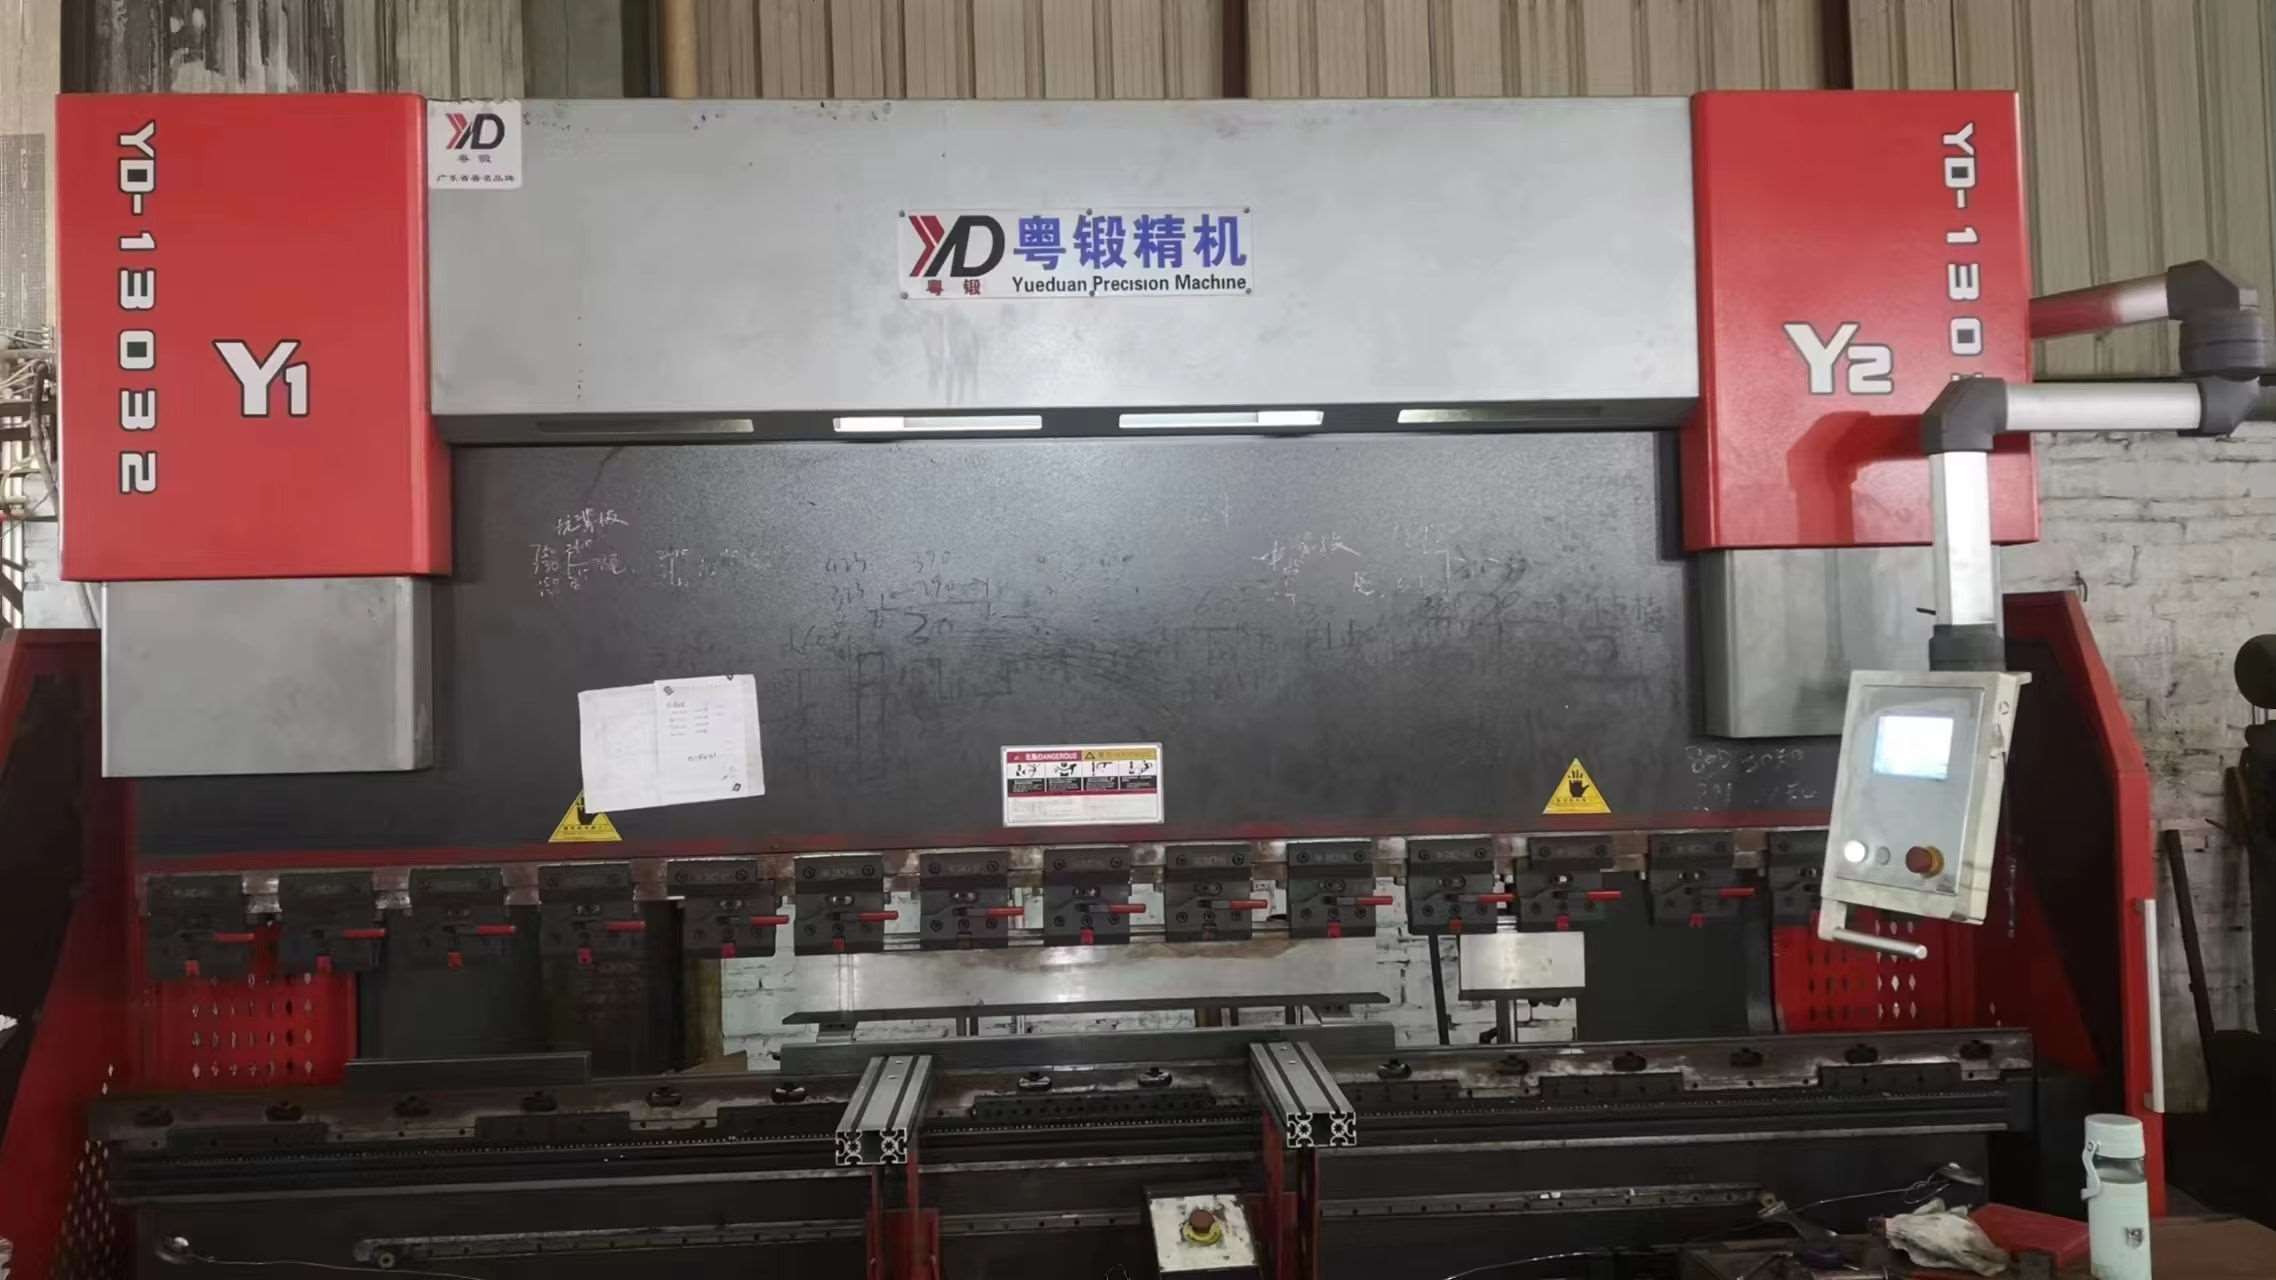
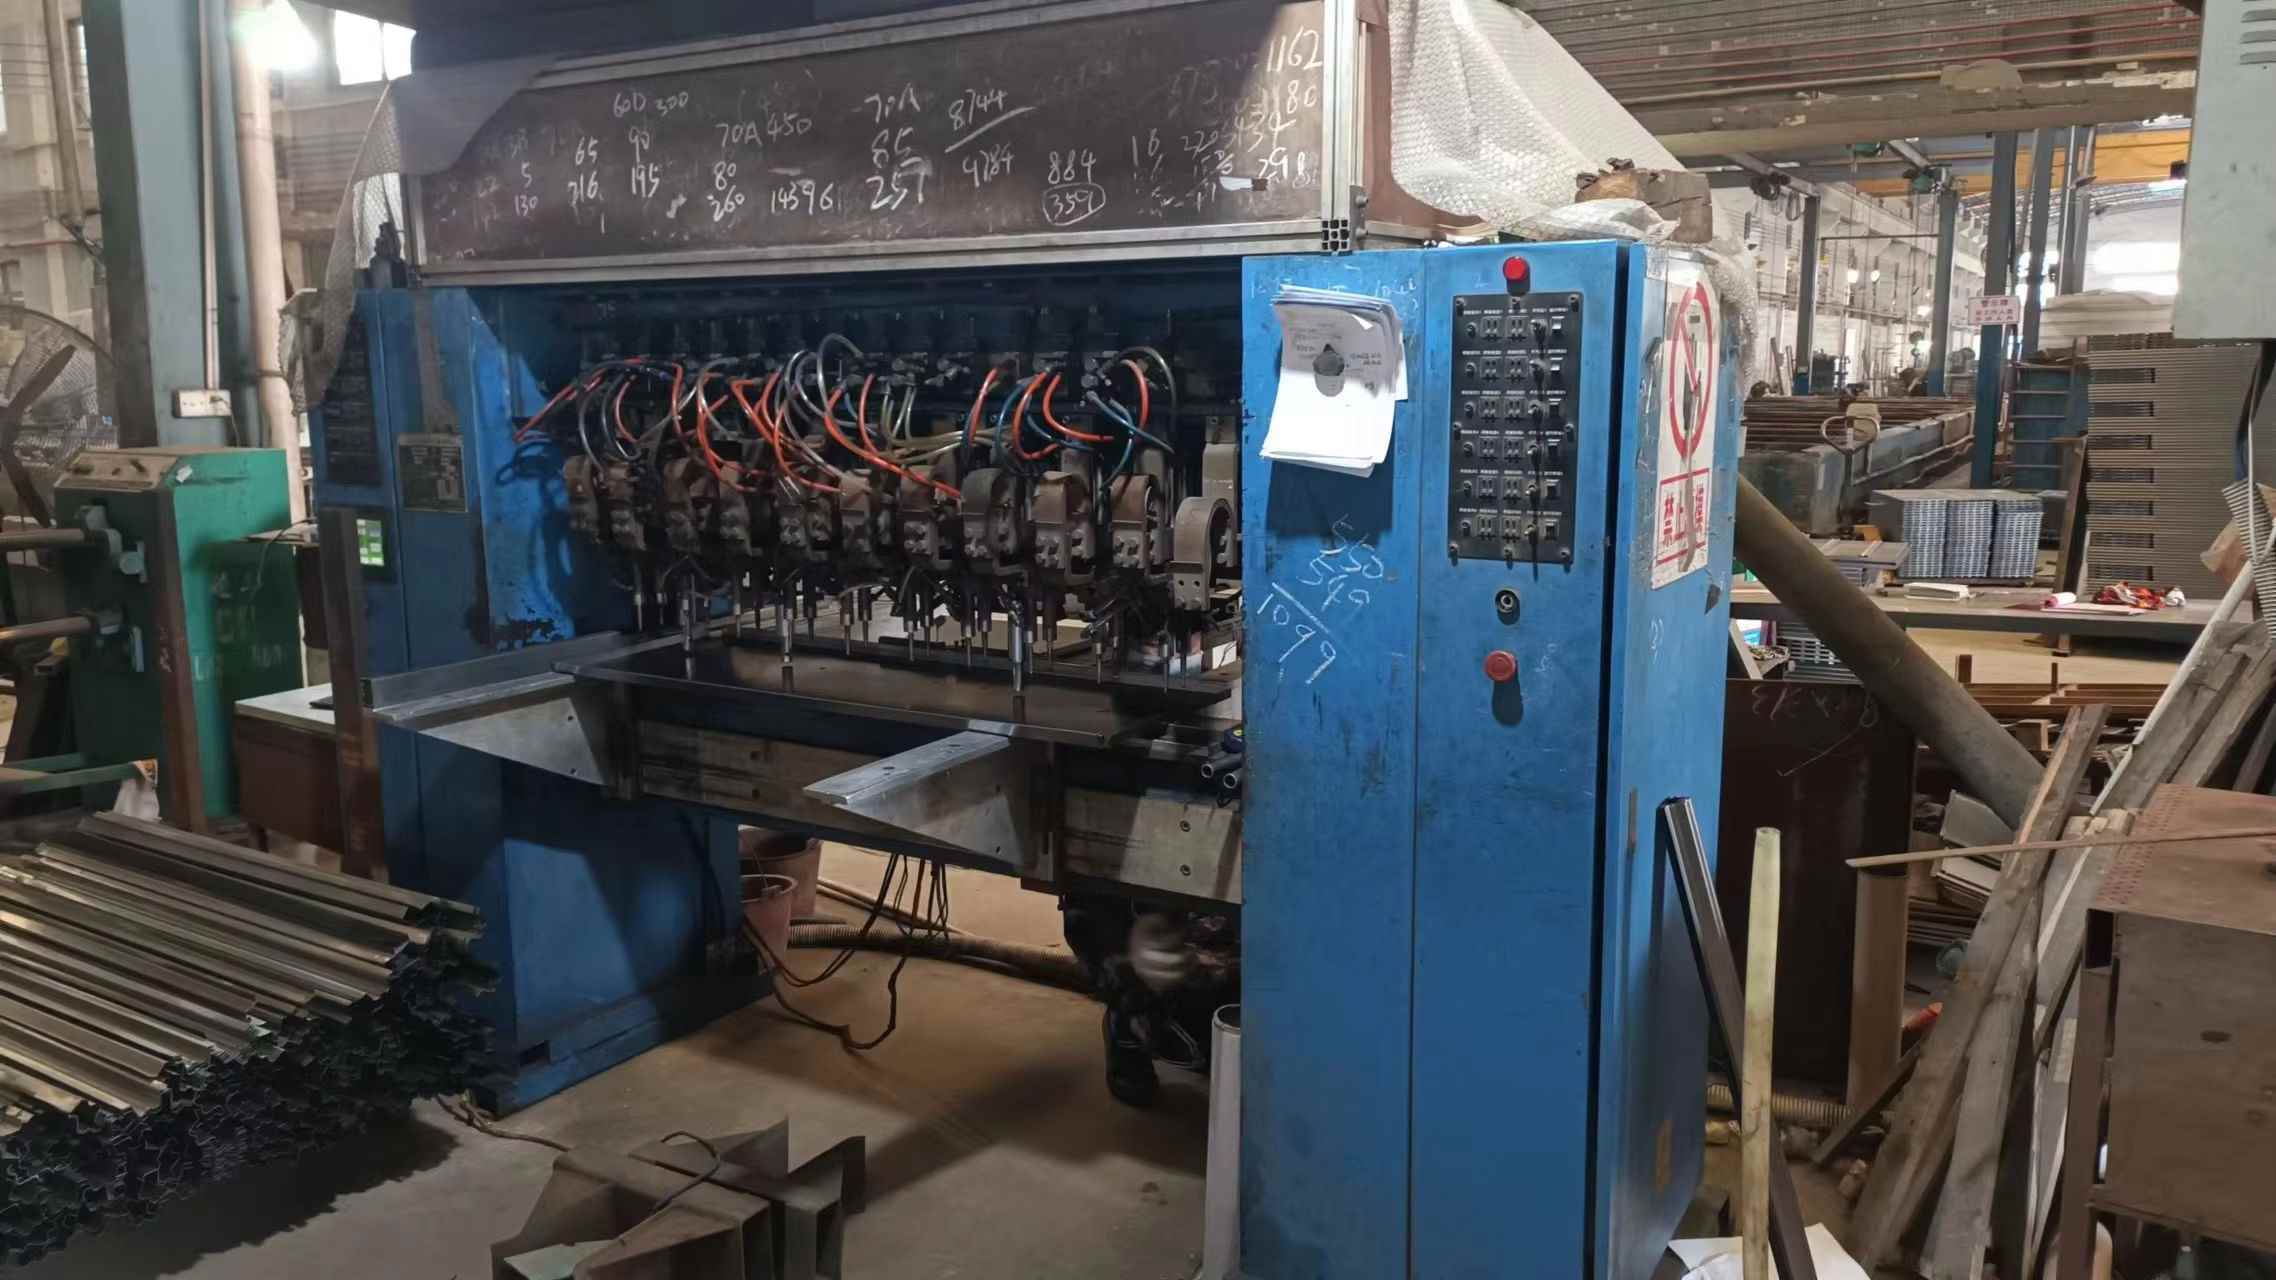
Different industrial sectors require distinct bin rack geometries, load-bearing thresholds, and operational clearance profiles. Heda engineers custom-tailored layout architectures to solve complex operational challenges:
Utilizing multi-tier mezzanine bin shelving structures paired with integrated gravity roller channels. High-density bin layouts divide fast-moving SKUs into ergonomic picking zones, dramatically accelerating order fulfillment throughput while cutting operator travel distances by up to 50%.
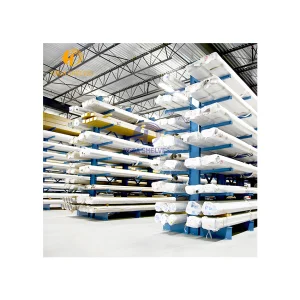
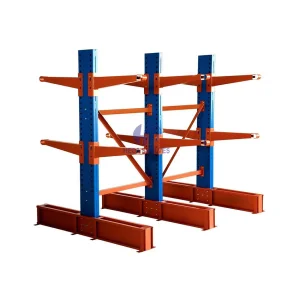
Heavy-duty steel bin racks engineered with customized drop-in dividers, removable plastic bin partitions, and reinforced cantilever arms. Designed to hold heavy motor assemblies, body stampings, and small hardware bins with dynamic weight capacities up to 3,000 kg per shelf layer.
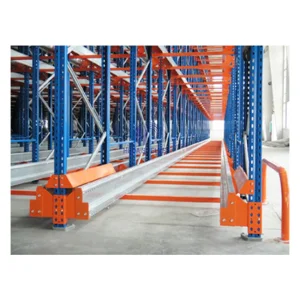
High-density 4-Way Radio Shuttle racking and Drive-In pallet systems optimized for FIFO (First-In, First-Out) and LIFO (Last-In, First-Out) inventory modes. Designed with cold-resistant powder coatings to withstand continuous freeze-thaw cycles without surface flaking.
Safety in high-bay industrial warehousing is paramount. Structural racking failures can cause disastrous inventory damage and operational downtime. Shenzhen Heda adheres to international structural safety codes, maintaining comprehensive quality oversight throughout design and fabrication.
Our upright profiles and load beams are calculated in strict compliance with FEM 10.2.02 (European Federation of Materials Handling) and RMI (Rack Manufacturers Institute) standards, ensuring safe elastic deformation thresholds under full load capacity.
For installations located in active seismic zones, Heda structural engineers design heavy-duty extended baseplates, footplate anchors, and cross-bracing frameworks engineered to absorb dynamic seismic energy loads.
Every steel coil received from tier-1 steel mills comes with certified Mill Test Certificates (MTC). Our internal QC team conducts routine chemical spectrometry, yield strength testing, and weld integrity verification.
As warehousing transitions toward full automation, Shenzhen Heda is pioneering structural innovations that fuse physical steel racking with intelligent IoT and digital twin monitoring systems.
Developing next-generation bin shelves and pallet rack uprights integrated with low-power IoT strain gauges. These sensors monitor load distribution in real time, alerting facility managers to overload risks or fork-truck impact damage before structural failures occur.
Transitioning 100% of our powder coating lines to zero-VOC, energy-efficient thermosetting formulations. Combined with closed-loop wastewater recovery during Parkerising, Heda reduces environmental carbon footprints while providing superior finish durability.
Expert technical answers to technical inquiries surrounding industrial bin shelf design, customization, international shipping, and load certification.
We primarily utilize high-tensile cold-rolled steel grades Q235B and Q355B (equivalent to ASTM A36 and Grade 50). These steels provide optimal ductile strength, superior load-bearing capacity, and outstanding weldability under severe industrial conditions.
Yes. Backed by our 28-member engineering R&D team, we offer full OEM/ODM engineering customization. We customize upright heights, beam lengths, shelf depths, bin divider partitions, and weight capacities ranging from 100 kg per layer up to 3,000 kg per heavy-duty pallet beam level.
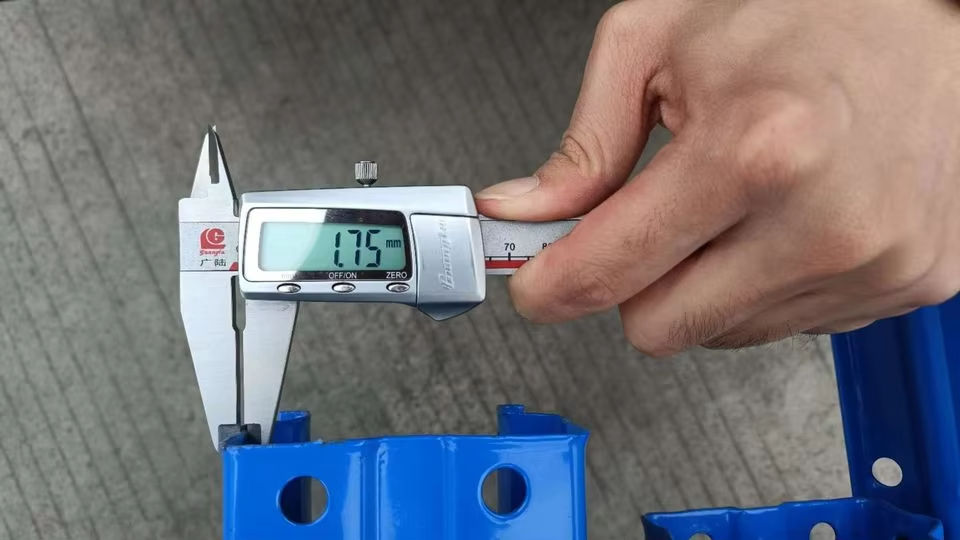
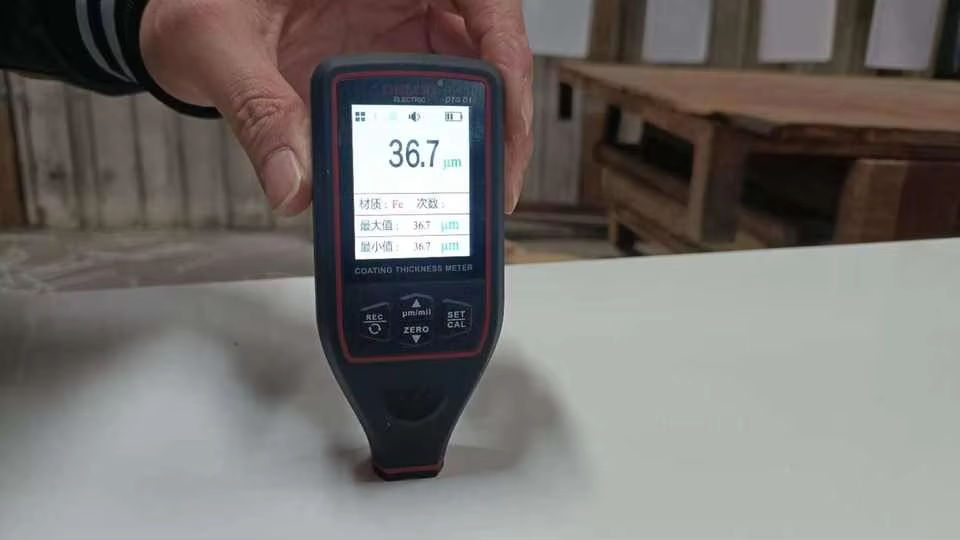
Our 45 dedicated QC inspectors perform 100% stage-gate testing: raw material tensile analysis, post-stamping pitch alignment, ultrasonic weld defect inspection, caliper dimension testing, and digital film coating thickness measurement.
We offer a multi-stage pre-treatment chemical washing process (degreasing, acid pickling, Parkerising phosphating) followed by an electrostatic epoxy-polyester powder coating. For extreme humidity or cold storage environments down to -30°C, we provide hot-dip galvanizing options.
Standard customized orders typically require 15 to 25 manufacturing days depending on overall tonnage and coating specifications. Standard stock components can ship within 7 to 10 days from our Shenzhen port logistics hub.
Yes, we provide complimentary CAD layout proposals, structural load calculations, and 3D warehouse visualization renders within 24–48 hours of receiving your warehouse blueprint dimensions and operational requirements.
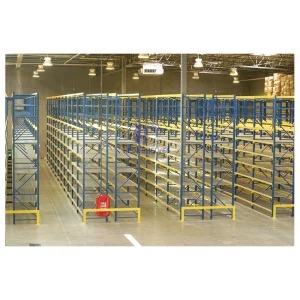
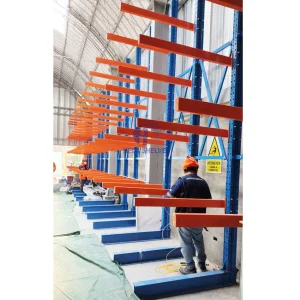
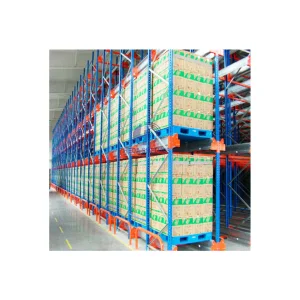
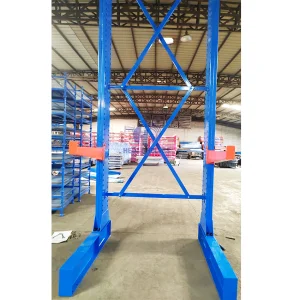
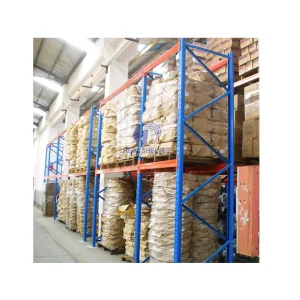
Browse our extended line of specialized industrial drive-in racking, cantilever storage frames, and high-capacity steel pallet structures.
 Hedaracking